

Content
- 1 1. The Role of a Big Chamber Blender in Nonwoven Production
- 2 2. Main Applications
- 3 3. Working Principle
- 4 4. Structural Design
- 5 5. Product Advantages
- 6 6. Comparison with Conventional Fiber Storage and Blending Methods
- 7 7. Technical Specifications
- 8 8. Manufacturing Strengths of the Supplier
- 9 9. Installation and Commissioning
- 10 10. Maintenance and Operational Recommendations
- 11 11. Selecting the Correct Configuration
- 12 12. Benefits for Different Nonwoven Production Lines
- 13 13. Safety Considerations
- 14 14. Commercial and Service Information
- 15 15. Frequently Asked Questions
- 15.1 Q1: What is the main function of the HYDC Big Chamber Blender?
- 15.2 Q2: Which raw materials can be processed?
- 15.3 Q3: How does the machine control the fiber level?
- 15.4 Q4: Why is a large chamber useful?
- 15.5 Q5: What working widths are available?
- 15.6 Q6: What storage volumes are available?
- 15.7 Q7: What are the listed capacity options?
- 15.8 Q8: Does the machine support different fiber formulas?
- 15.9 Q9: What makes the machine different from a simple fiber hopper?
- 15.10 Q10: Is the stripper and evener roller transmission independent?
- 15.11 Q11: How is cleaning performed?
- 15.12 Q12: Can the blender be integrated into a complete nonwoven line?
- 15.13 Q13: Is customization available?
- 15.14 Q14: What certification information is listed?
- 15.15 Q15: What is the warranty period?
- 16 16. Conclusion
- 17 References
- 18 Product: HYDC Big chamber blender
Modern nonwoven fabric production depends on stable fiber preparation. Before fibers reach the card, airlay, thermal bonding, or needle punching stages, they must be opened, blended, stored, and delivered at a controlled rate. Variations in fiber composition, density, moisture, or feed volume can affect web uniformity, tensile strength, thickness, appearance, and overall production efficiency. The HYDC Big Chamber Blender is designed to address these requirements by combining fiber mixing, temporary storage, photoelectric control, and continuous feeding in one integrated machine.
The equipment is suitable for a wide selection of opened fibers, including polyester fiber, polypropylene staple fiber, wool, cotton, coir fiber, jute fiber, ES fiber, waste fiber, and other materials used in nonwoven manufacturing. By distributing opened fibers through a large chamber and delivering them continuously to the next process, the machine helps manufacturers create a more stable feed for carding and web-forming equipment.
Its modular construction, configurable working widths, multiple storage volumes, automatic monitoring, and adjustable production capacities make it suitable for both individual production units and complete nonwoven production lines. It can be installed as part of a needle-punched geotextile line, carpet line, airlaid waste-felt line, automotive interior material line, cleaning cloth line, wool felt line, jute felt line, or other fiber-based manufacturing system.
1. The Role of a Big Chamber Blender in Nonwoven Production
Fiber preparation is one of the most important stages in a nonwoven process. Opened fibers are rarely ready to move directly into carding or web formation. Different bales may contain variations in fiber length, color, density, moisture, and material composition. When several fiber types are used in a formula, they must be combined evenly to prevent local differences in the finished web.
A big chamber blender provides a controlled intermediate stage between opening and carding. Opened fiber is conveyed into the chamber, distributed across the available storage space, blended as it moves through the machine, and then discharged at a regular rate. The chamber also acts as a buffer. If the bale-opening process operates with a different rhythm from the card line, the blender helps maintain continuous production by storing a suitable quantity of prepared fiber.
This function is especially valuable in factories processing large volumes of material. Without adequate storage and blending capacity, the card line may experience interruptions whenever the upstream opener changes bales, adjusts its working conditions, or temporarily produces a different quantity of fiber. The result may be uneven web formation, unstable production speed, or unnecessary manual intervention.
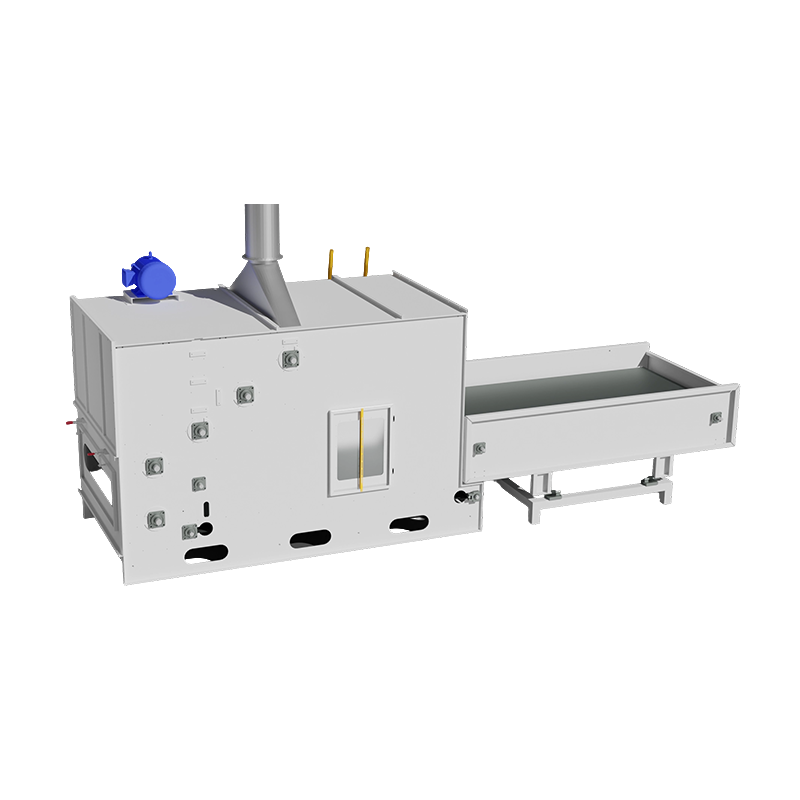
The HYDC design combines these functions in a single mechanical system. The horizontal delivery lattice transfers fiber, the spike lattice elevates and handles the material, and the rotary separator distributes the fiber in the chamber. Photoelectric sensors monitor the material level and help control feeding conditions. The result is a more consistent material flow from opening to carding.
2. Main Applications
2.1 Polyester and Polypropylene Staple Fiber
Polyester and polypropylene staple fibers are widely used in needle-punched nonwovens, thermal-bonded products, automotive materials, filtration media, insulation, furniture padding, and geotextiles. These fibers may be blended with different deniers, lengths, colors, or functional additives. A big chamber blender helps distribute the opened materials before they reach the card.
For production lines using recycled polyester or mixed recycled fibers, the blender can also support more stable feeding. Recycled raw materials may have greater variation than virgin fibers, so consistent mechanical blending is important for maintaining the quality of the web.
2.2 Wool, Cotton, Coir, and Jute Fiber
Natural fibers such as wool, cotton, coir, and jute can be used in felt, floor covering, insulation, packaging, erosion-control products, and other nonwoven applications. Their physical characteristics differ from those of synthetic fibers. They may have different bulk, moisture content, fiber length, and opening behavior.
The chamber-based design gives manufacturers the flexibility to process different material formulas while providing an intermediate storage area. Operators can configure the equipment according to the fiber type, required capacity, chamber volume, and downstream line width.
2.3 ES Fiber and Thermal-Bonded Products
ES fiber is often used as a bonding component in thermal-bonded wadding, filtration materials, hygienic products, and automotive interior products. When ES fiber is blended with polyester or other staple fibers, uniform mixing is important because the binder fiber must be distributed throughout the web.
A more consistent blend supports more uniform heating and bonding in the downstream oven. This can help reduce areas of weak bonding, excessive hardness, or uneven thickness. The final result depends on the entire production process, but stable preparation is an important foundation.
2.4 Waste and Recovered Fiber
The HYDC Big Chamber Blender can be used with waste fiber and other recovered materials, provided that the material is suitably opened and prepared for the line. Waste-based production often involves fluctuations in bulk density and fiber composition. The storage and blending functions can help moderate these variations before the material enters the carding process.
When processing waste fiber, the complete line should include suitable cleaning, separation, dust-control, and safety provisions. The blender is an important part of material preparation, but it should be selected together with the bale opener, opener, card, dust-removal system, and final web-forming equipment.
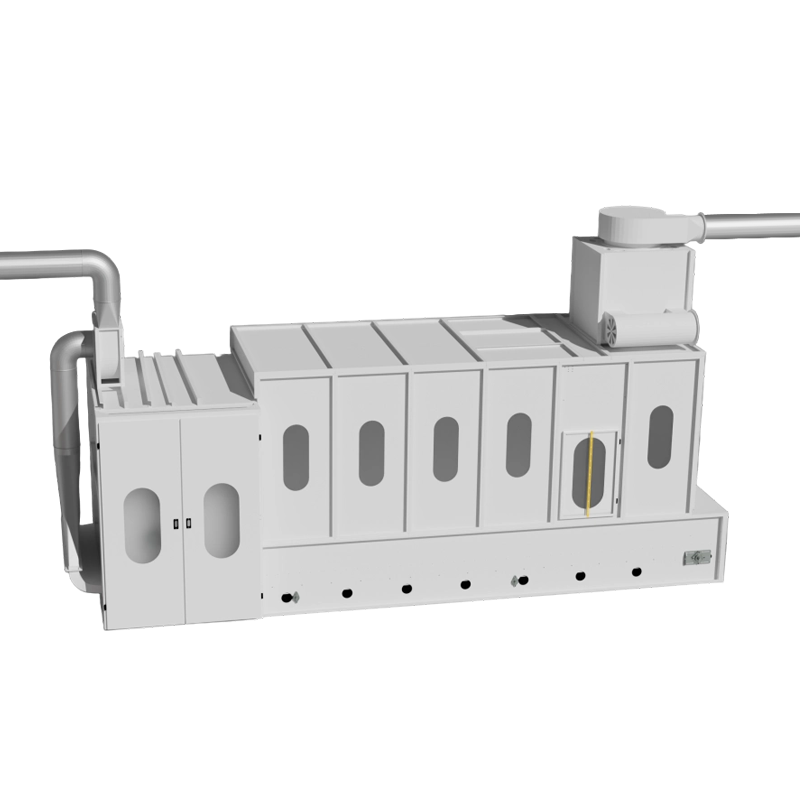
HYDC Big chamber blender
3. Working Principle
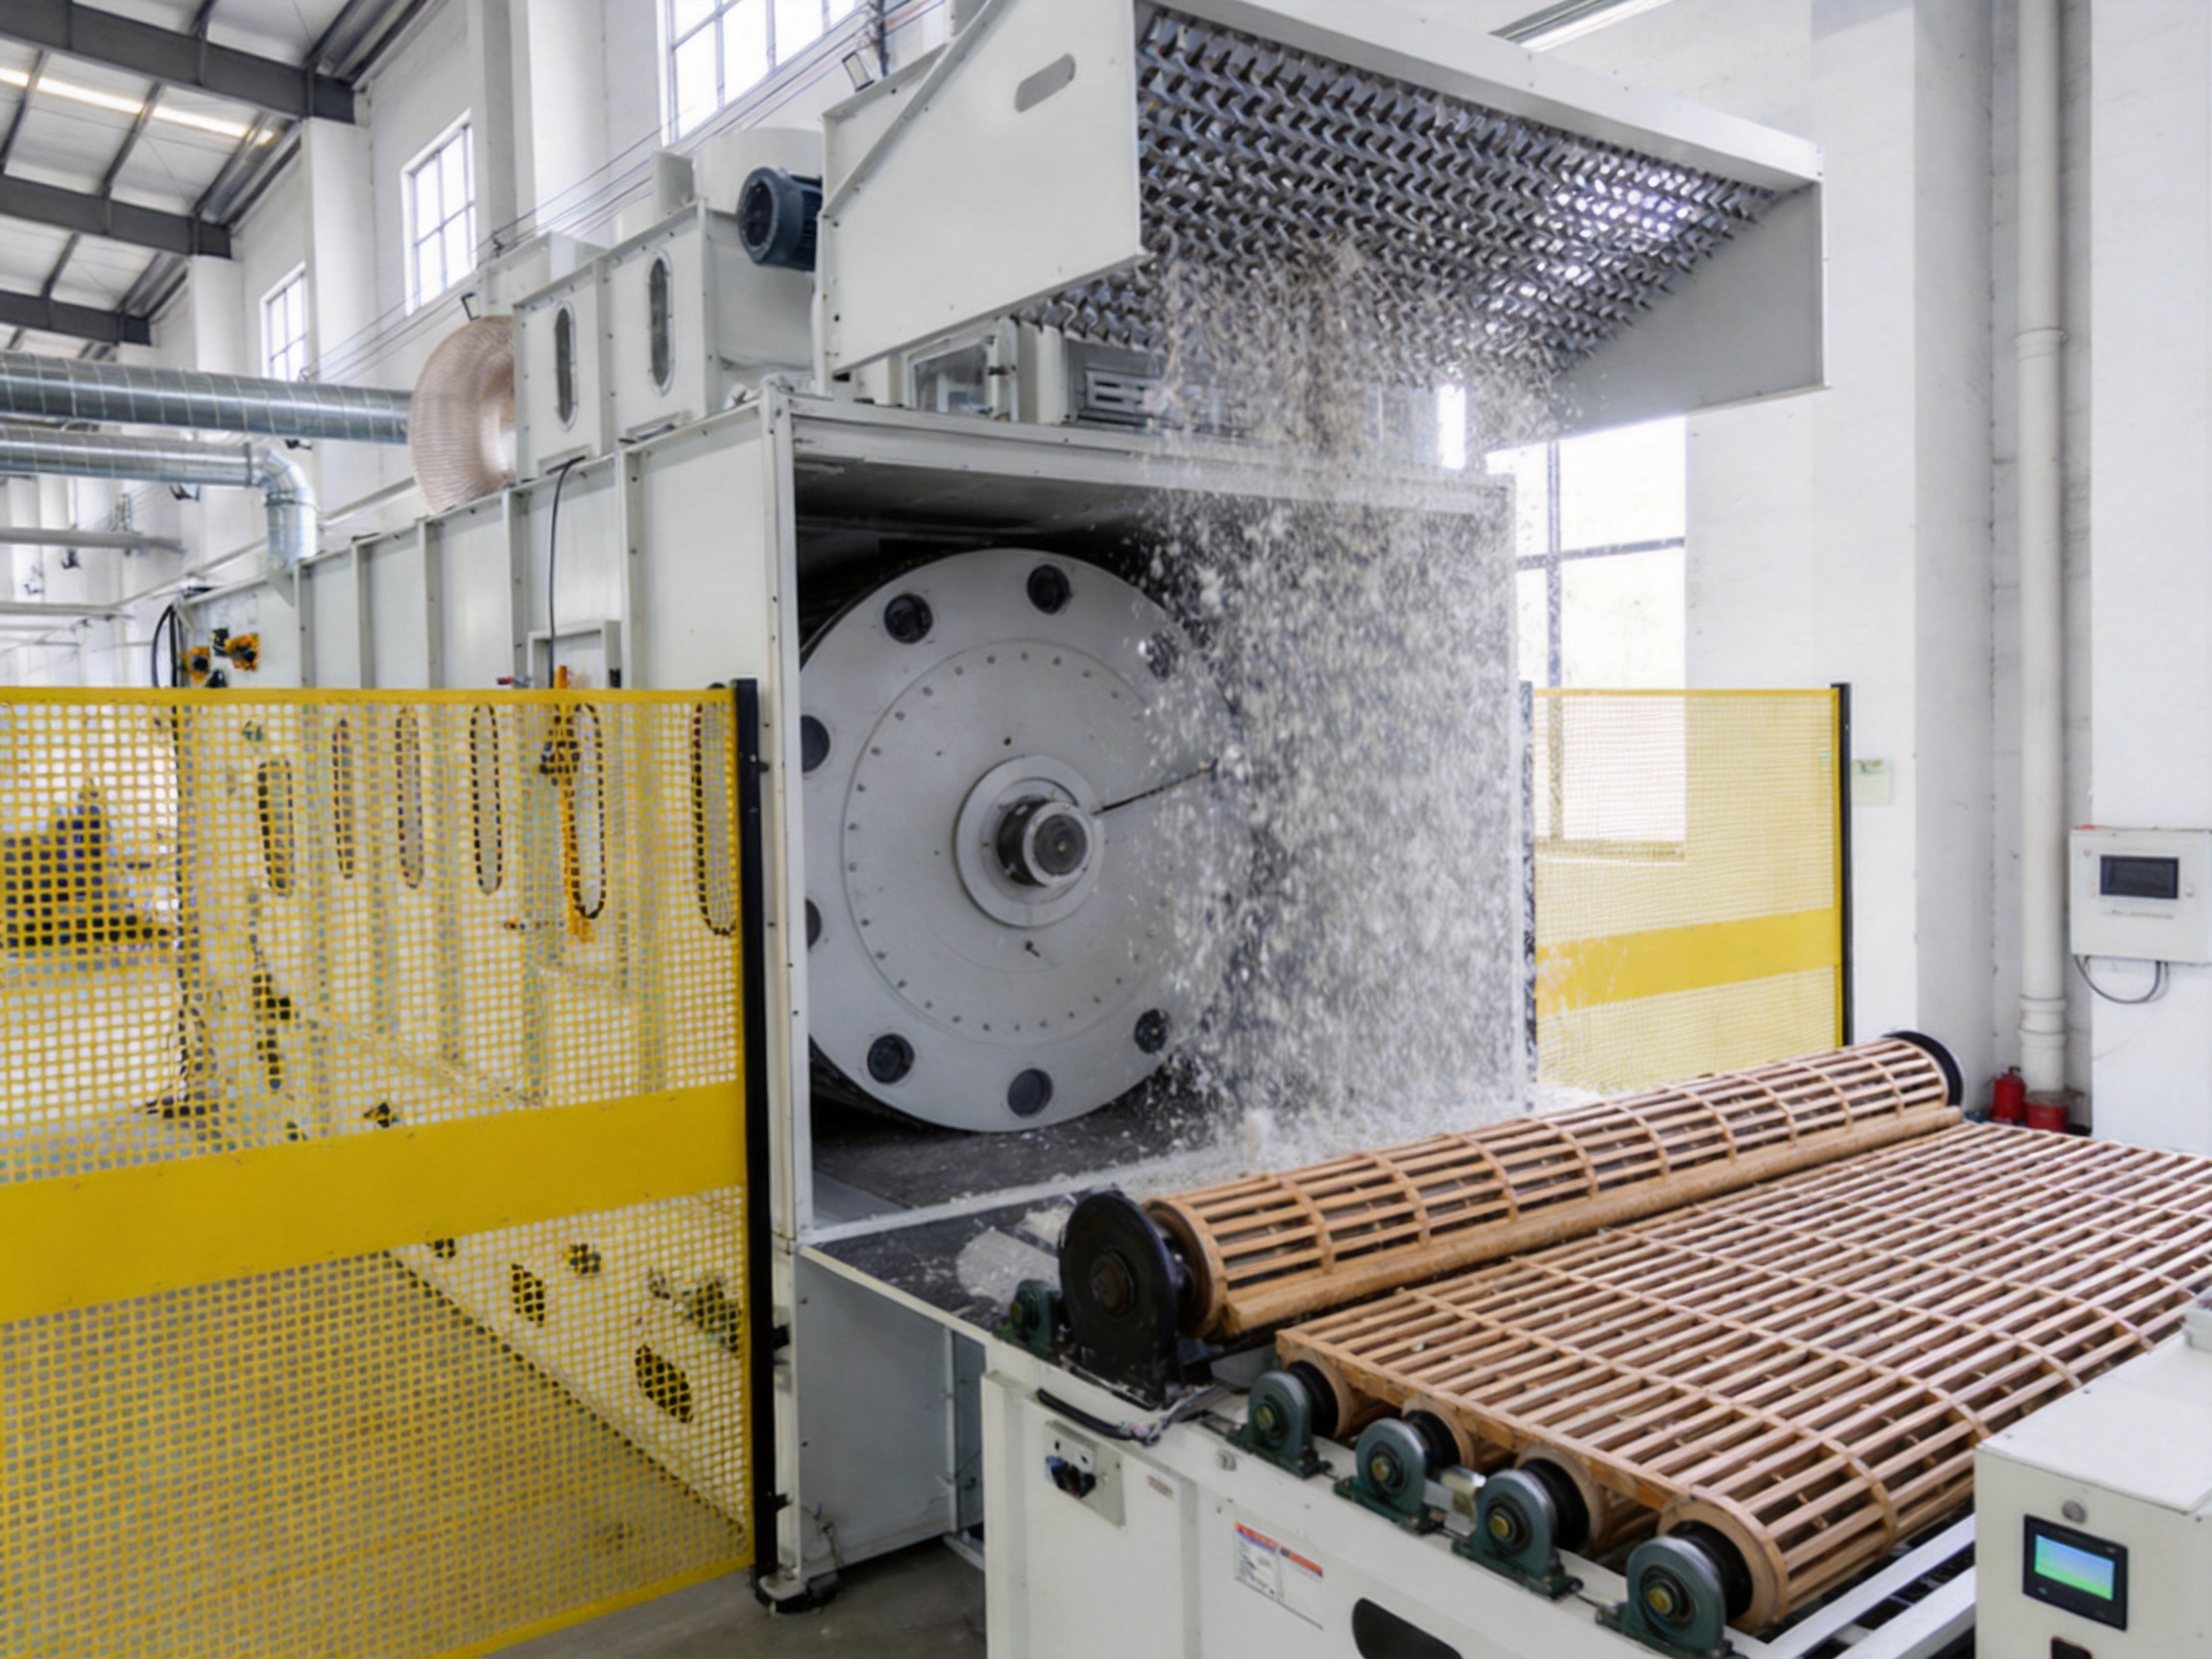
The HYDC Big Chamber Blender receives opened fiber from upstream opening equipment. The material is transferred through the horizontal delivery lattice and moved into the blending chamber. The spike lattice then carries the fiber upward. During this movement, the fiber is distributed and blended rather than simply placed in one concentrated area.
A rotary separator helps spread the fiber evenly across the chamber. This is a key part of the machine because uneven distribution inside the storage cabinet may cause differences in density and composition when the material is discharged. By distributing the fiber more consistently, the separator supports a stable downstream feed.
The chamber stores the prepared material until it is required by the next process. Photoelectric sensors monitor the feeding status. Depending on the material level, the sensors can control the operation of the relevant feeding components and help prevent excessive accumulation or insufficient supply.
At the discharge side, the feeding mechanism delivers fiber toward the card line or another downstream machine. The machine behind the spike lattice uses photoelectric control to regulate feeding. This arrangement allows the blender to respond to the production demand of the next process and maintain a more continuous material flow.
The system is not designed merely as a passive storage box. It performs several coordinated functions: receiving opened fiber, distributing it, blending it, storing it, and delivering it in a controlled manner. This integrated operation distinguishes a purpose-built chamber blender from a simple conveyor or temporary hopper.
4. Structural Design
4.1 Machine Frame
The machine frame is constructed from several wall boards welded from Q235-A armor plate and assembled with bolts. This combination provides a practical balance between structural strength, manufacturing flexibility, and installation convenience.
A bolted modular structure can simplify transportation and on-site assembly. It also makes it easier to adapt the equipment to different line layouts or working widths. The frame must withstand repeated mechanical movement, fiber pressure, vibration, and the operating forces generated by the lattice and roller systems.
4.2 Horizontal Delivery Lattice
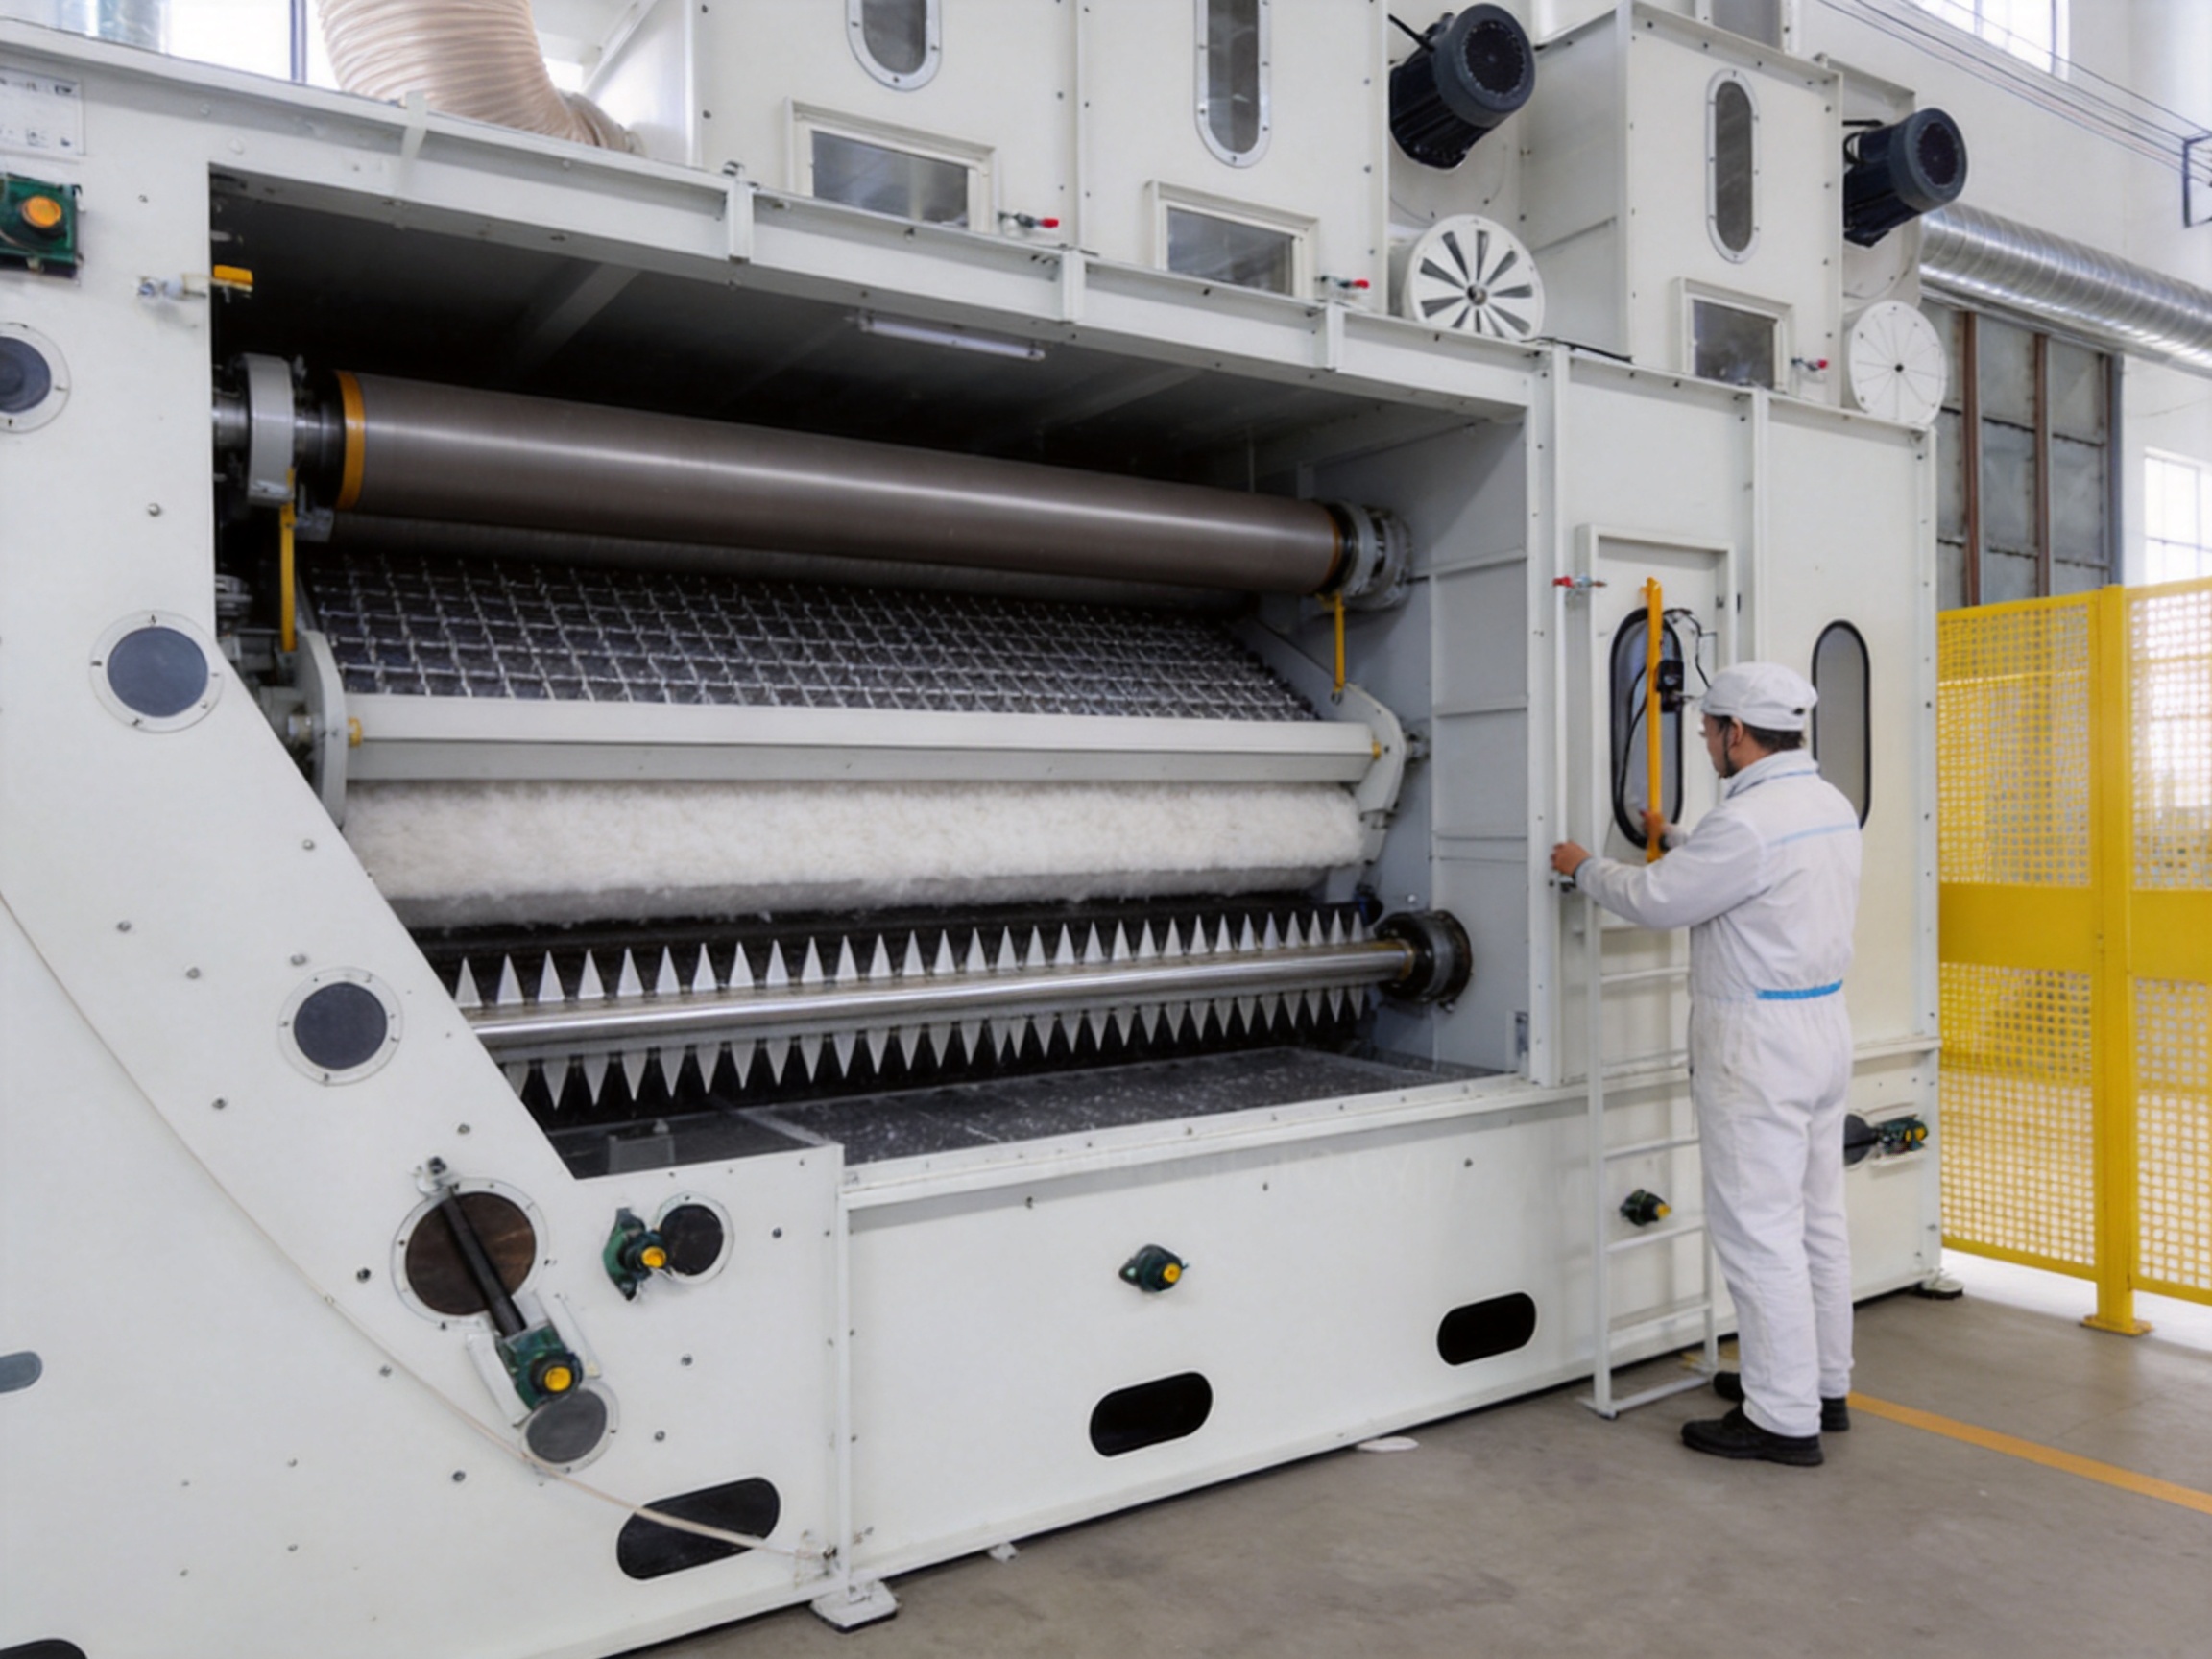
The horizontal delivery lattice uses an anti-skidding leather belt. Multiple layers of rollers reinforce the central area, while wooden battens are installed on both sides. This structure supports reliable fiber transfer and helps keep the material moving in the intended direction.
An anti-skidding surface is useful when the machine handles bulky or irregularly distributed opened fibers. The belt must maintain traction during continuous operation, especially when the material contains long fibers, dense clumps, or a mixture of different raw materials. Reinforcing rollers help support the belt and reduce deformation under load.
4.3 Spike Lattice
The spike lattice is made from high-quality wood with canvas interlining and is supported around the outside by angle steel. The spike arrangement engages with the opened fiber and transports it upward into the chamber.
Mechanical components that contact fiber must be designed for reliable material handling without causing excessive accumulation or uncontrolled discharge. The spike lattice provides the lifting action required for the vertical movement of fiber. Its supporting structure contributes to stable operation and helps maintain the alignment of the lattice during production.
4.4 Rotary Separator
The rotary separator is responsible for distributing fiber evenly in the blending chamber. Without a separator, material may fall into localized piles, producing an uneven chamber density and inconsistent discharge. The rotary action creates a broader distribution pattern and improves the use of the available storage volume.
Uniform distribution is particularly important when a production line uses a mixture of fibers with different densities. Heavy or compact material may otherwise settle in one area while lighter fibers accumulate elsewhere. The separator helps reduce this tendency and supports more repeatable blending conditions.
4.5 Photoelectric Sensors
Two photoelectric sensors control the feeding status. They provide non-contact detection of the material level or feeding condition and support automatic operation during production. Compared with manual observation, photoelectric monitoring can reduce operator workload and improve response speed.
Automatic level monitoring is also useful when the blender is connected to a card line. The downstream machine requires a relatively stable supply, while the upstream opener may not provide material at exactly the same rate at every moment. Sensor-based control helps coordinate these sections of the line.
4.6 Cleaning Gate and Safety Switch
A dodge gate is installed at the end of the box to provide access for cleaning the interior. Fiber dust and residual material can accumulate in any opening and blending system, particularly when the machine handles short fibers, recycled materials, or natural fibers.
The cleaning gate allows operators to remove residual material more conveniently. It is also equipped with a safety switch. The safety switch is an important protective feature because access should be controlled when the machine is running. Cleaning, inspection, and maintenance should always follow the supplier’s safety procedures and the plant’s lockout and isolation requirements.
5. Product Advantages
5.1 Stable Continuous Feeding
One of the main advantages of the HYDC Big Chamber Blender is its ability to support continuous feeding to the card line. The chamber provides a reserve of opened and blended fiber, reducing the impact of short-term fluctuations in upstream supply.
Stable feeding helps the card operate under more consistent conditions. It can contribute to improved web uniformity and fewer interruptions caused by an empty or irregular feed. For high-output nonwoven production, this buffering effect can be as important as the nominal capacity of the opening machine itself.
5.2 More Even Fiber Density
The rotary separator, spike lattice, and controlled feeding arrangement work together to spread the fiber more evenly. Even density inside the chamber supports more consistent discharge and helps reduce local variations in the material blend.
More uniform fiber density is valuable in applications where the final product must meet strict requirements for basis weight, thickness, strength, absorbency, insulation performance, or surface appearance. The blender does not replace process control at the card or web-forming stage, but it provides a more stable raw-material condition for those stages.
5.3 Independent Transmission of Stripper and Evener Roller
The stripper and evener roller use independent transmission. This arrangement provides greater flexibility during adjustment because the two components can be controlled or tuned separately rather than being forced to operate through a single fixed transmission relationship.
Independent transmission can also support easier maintenance. If a component requires adjustment, inspection, or replacement, the operator has more direct access to its individual drive arrangement. The supplied product information identifies this configuration as a benefit for dependability, adjustment, and maintenance.
5.4 Automatic Photoelectric Control
Photoelectric control reduces the need for constant manual monitoring of the chamber. The sensors help the machine respond to the material level and feeding status. This can improve operational consistency, particularly in a production environment where the blender is integrated with several other machines.
Automatic control also creates a foundation for further line integration. Depending on the customer’s control configuration, the machine can be connected with upstream opening equipment, downstream carding equipment, and the central production control system.
5.5 Flexible Configuration
The equipment is available in several working widths, storage volumes, and capacity ranges. The listed working widths include 1,700 mm, 2,000 mm, 2,500 mm, and 3,000 mm. Storage volumes include approximately 15 cubic meters, 20 cubic meters, 30 cubic meters, and 37 cubic meters. Listed capacity options include 300 kg/h, 500 kg/h, 800 kg/h, and 1,000 kg/h.
This selection enables manufacturers to choose a configuration according to their card width, raw-material formula, production target, available floor space, and upstream equipment. A smaller chamber may be suitable for a compact line or moderate output, while a larger chamber can provide greater buffer capacity for a high-volume plant.
5.6 Modular Installation
The product information identifies modular design and easy installation as important advantages. A modular system can be manufactured, transported, assembled, and adjusted in sections. This is practical for overseas projects, where the machine must be packed, shipped, installed, and commissioned at the customer’s factory.
Modular installation may also help customers expand a line later. The final configuration should always be confirmed against the customer’s building dimensions, material flow, electrical standards, and the interface requirements of the connected machines.
6. Comparison with Conventional Fiber Storage and Blending Methods
A simple fiber storage bin may hold material, but it normally does not provide the same combination of distribution, blending, sensor-based control, and continuous feeding. Manual mixing can be labor-intensive and inconsistent. A basic conveyor can move fiber but cannot necessarily create an even material distribution across a large chamber.
The HYDC system is designed specifically for the connection between opening and carding. Its components are selected around the behavior of opened fiber. The horizontal delivery lattice handles the incoming material, the spike lattice lifts it, the separator distributes it, and the sensors help regulate the feeding condition.
Compared with a manually managed storage process, automatic photoelectric control can reduce dependence on operator timing. Compared with a small hopper, the large chamber provides greater storage volume and a better buffer for continuous production. Compared with a single-drive arrangement, independent stripper and evener roller transmission allows more precise adjustment and easier service.
Competitor equipment may offer similar general functions, but buyers should evaluate the complete mechanical design rather than comparing only the nominal chamber volume. Important comparison points include the strength of the frame, the construction of the lattice, belt traction, separator design, sensor arrangement, access for cleaning, drive configuration, maintenance requirements, and the supplier’s ability to integrate the machine into a complete nonwoven line.
7. Technical Specifications
The following table summarizes the principal specifications provided for the HYDC Big Chamber Blender. Some specifications vary according to the selected model and project configuration. Final values should be confirmed in the technical agreement before ordering.
| Item | Available or Listed Specification |
| Model | HYDC; example model HYDC-170 |
| Product type | Big chamber blender and fiber mixing machine |
| Application | Opening, blending, storage, and continuous feeding of opened fibers |
| Working width | 1,700 mm, 2,000 mm, 2,500 mm, or 3,000 mm |
| Storage volume | Approximately 15 m³, 20 m³, 30 m³, or 37 m³ |
| Capacity range | Approximately 300 kg/h, 500 kg/h, 800 kg/h, or 1,000 kg/h |
| Example capacity | Up to 650 kg/h per set for a listed configuration |
| Raw materials | Polyester, polypropylene staple fiber, wool, cotton, coir, jute, ES fiber, waste fiber, and similar materials |
| Control method | Photoelectric control and automatic feeding-status monitoring |
| Frame construction | Q235-A armor plate wall boards, welded and assembled with bolts |
| Horizontal lattice | Anti-skidding leather belt with reinforced rollers and side wooden battens |
| Spike lattice | Wood construction with canvas interlining and angle-steel support |
| Transmission | Independent transmission for stripper and evener roller |
| Certification listed | CE and ISO9001-related certification information |
| Electrical frequency | 50 Hz listed |
| Installed power | Values listed include 8.8 kW and 15.7 kW, depending on configuration |
| Working width options | Customized according to line requirements |
| Trade terms | FOB, CNF, or CIF |
| Typical lead time | Approximately 90 days after deposit, or two to three months depending on the project |
| Warranty | Twelve months after mechanical and electrical commissioning |
The differences between listed power and capacity values reflect the fact that the machine is offered in several configurations. Working width, storage volume, conveyor length, number of connected machines, material type, and automation requirements can all affect the final specification.
8. Manufacturing Strengths of the Supplier
Changshu Hongyi Nonwoven Machinery Co., Ltd. is a China-based nonwoven machinery manufacturer and supplier with more than 20 years of experience in the nonwoven machinery field. Its experience covers both individual machines and complete production lines.
The company’s product range includes bale openers, carding machines, airlay machines, needle punching machines, ironing machines, thermal bonding wadding oven machines, winding and cutting equipment, and auxiliary systems for nonwoven production. It also supplies complete lines for needle-punched geotextiles, nonwoven carpets, airlaid waste felt, automotive interior materials, needle-punched cleaning cloth, wool felt, and jute felt.
This broad product portfolio is relevant when purchasing a big chamber blender because the machine rarely operates as an isolated unit. Its performance depends on the characteristics of the bale opener, pre-opener, fine opener, card, cross lapper, needle loom, thermal bonding oven, winding machine, and cutting machine connected to it.
8.1 Complete-Line Understanding
A supplier that manufactures multiple types of nonwoven equipment can evaluate the interaction between upstream and downstream machines. For example, the correct chamber volume depends not only on the target output but also on the time required for bale opening, the card’s feeding demand, the fiber formula, and the desired production buffer.
Complete-line experience also helps with layout planning. Material should move through the factory with minimal unnecessary handling. The blender position, conveyor direction, service access, electrical control panel, cleaning access, and connection points must all be considered during design.
8.2 Engineering and Customization
The company provides customized machine solutions for different customer requirements. Customization may involve working width, storage volume, conveyor length, line arrangement, color, control system, electrical voltage, transport dimensions, and the interface with existing equipment.
Customization is especially important for factories replacing an older blender or adding a machine to an existing production line. The available floor space may be limited, the card may have a fixed working width, and the factory may use a particular voltage or automation standard.
8.3 Mechanical Manufacturing
The product structure demonstrates a practical mechanical manufacturing approach. Q235-A steel plate is used for the main wall-board structure, while bolted assembly supports modular installation. The horizontal lattice, rollers, spike lattice, separator, gates, and sensor supports are manufactured as coordinated mechanical assemblies.
Reliable manufacturing requires control of frame dimensions, roller alignment, belt tension, lattice positioning, drive installation, and access-panel fitting. These details influence whether the machine runs smoothly and whether operators can maintain it efficiently over time.
8.4 Quality and Process Control
The supplied information lists ISO9001 and CE certification references. These indicate that the supplier has established quality-management and equipment-compliance procedures relevant to its products. Customers should request the exact certification documents and confirm which model and configuration they cover.
Quality control for a chamber blender should include inspection of raw materials, welding quality, surface treatment, assembly accuracy, electrical components, sensor operation, drive alignment, and test running before shipment. A factory acceptance test can be arranged to verify the main functions and operating sequence before delivery.
8.5 International Project Experience
The company reports that its products have been supplied to more than 20 countries, including Mexico, Argentina, Brazil, Turkey, Algeria, Egypt, Bangladesh, Vietnam, Thailand, and other Asian markets. International experience is useful because overseas projects often involve different electrical standards, languages, site conditions, shipping requirements, and installation procedures.
The supplier provides trade terms including FOB, CNF, and CIF. Transport packaging may use nude packing or PE film, depending on the equipment and shipment requirements. The supplier’s reported after-sales arrangement includes installation and debugging support, while the buyer provides local cooperation such as workers, translation, electrical cables, tools, accommodation, and transportation for engineers.
9. Installation and Commissioning
Installation should begin with a review of the approved layout, foundation or floor requirements, machine orientation, material-flow direction, and service clearances. The customer should ensure that the building can support the equipment and that there is adequate space for inspection, cleaning, belt adjustment, and component replacement.
The machine should be positioned accurately before the connecting bolts are fully tightened. The horizontal delivery lattice, spike lattice, separator, rollers, and drives must be aligned according to the installation instructions. Incorrect alignment may lead to belt deviation, abnormal noise, uneven material movement, or premature wear.
Electrical installation should follow the approved wiring diagram and local regulations. The customer is responsible for providing the required cables between the machines, the control panel, and the power source unless another arrangement is agreed in writing. Voltage, frequency, motor protection, emergency-stop circuits, sensor connections, and grounding should be checked before commissioning.
During commissioning, the supplier’s engineer can inspect mechanical movement, sensor response, feeding logic, belt tracking, safety-switch operation, and the coordination between the blender and connected equipment. Initial testing should begin at low speed or without full material loading where appropriate. The line can then be gradually increased to the target operating condition.
The reported installation period is approximately 30 to 40 days, depending on the project and the cooperation of the buyer. The actual duration may vary according to the number of machines, line complexity, local preparation, worker availability, and the readiness of utilities and foundations.
10. Maintenance and Operational Recommendations
10.1 Daily Inspection
Operators should inspect the machine before starting production. The inspection should include the condition of the belt, spike lattice, rollers, separator, guards, safety switch, photoelectric sensors, and access gates. Any loose fastener, abnormal noise, material blockage, or damaged protective component should be addressed before operation.
The chamber and surrounding area should be kept clean. Accumulated fiber can interfere with sensor detection, increase dust levels, obstruct moving parts, and create additional fire risk. The cleaning frequency should be adjusted according to the raw material and production environment.
10.2 Belt and Lattice Adjustment
The horizontal belt should run centrally and maintain suitable tension. Excessive tension may increase the load on bearings and drives, while insufficient tension may cause slipping or poor material transfer. The lattice and roller alignment should be checked whenever abnormal tracking or vibration is observed.
The spike lattice should be inspected for damaged spikes, loose sections, excessive wear, or fiber accumulation. Because the spike lattice is a major material-handling component, its condition has a direct effect on lifting performance and feeding stability.
10.3 Sensor Maintenance
Photoelectric sensors must remain clean and correctly aligned. Fiber dust on the sensor surface can affect detection. Operators should follow the supplier’s instructions for cleaning and should not adjust the sensor position without understanding the control sequence.
Sensor testing should form part of regular maintenance. A failure to detect high or low material levels may cause overfilling, insufficient feeding, or an unexpected line stop. The safety switch at the cleaning gate should also be tested periodically to ensure that it performs its protective function.
10.4 Lubrication and Drive Inspection
Bearings, transmission components, and other lubrication points should be serviced according to the manufacturer’s maintenance schedule. Motors, gearboxes, chains, belts, couplings, and fasteners should be checked for wear, overheating, looseness, or unusual vibration.
The independent transmission of the stripper and evener roller should be inspected separately. This makes it possible to identify which drive or component requires attention and helps prevent a small adjustment issue from affecting the entire material-feeding system.
11. Selecting the Correct Configuration
Customers should begin selection by defining the raw-material recipe and the intended production output. A line processing lightweight polyester may require a different chamber volume from a line processing dense natural fiber or recycled material. The bulk density of the opened fiber has a direct effect on storage behavior.
The working width should correspond to the card or the next major processing machine. The selected width must also fit the factory layout and allow access for maintenance. If a customer expects future expansion, it may be beneficial to discuss a larger chamber, a longer conveyor, or a control system prepared for additional equipment.
Storage volume should be evaluated according to the desired buffer time. A larger volume can provide greater separation between upstream and downstream production fluctuations, but it may require more floor space and potentially greater structural or drive capacity.
Capacity should not be selected only from the maximum value in a brochure. The customer should consider the actual material type, fiber blend, moisture, bale-opening performance, required web quality, carding capacity, and operating hours. A practical operating range is often more useful than a theoretical maximum.
Electrical requirements should be confirmed early. The supplied information lists 50 Hz operation and indicates that voltage can be customized, including a listed 220-volt option. International customers should confirm the local voltage, phase, frequency, motor standards, control-panel requirements, and safety regulations before manufacturing begins.
12. Benefits for Different Nonwoven Production Lines
12.1 Needle-Punched Geotextile Lines
Geotextile production often requires consistent fiber feeding over long operating periods. A big chamber blender can support the preparation of polyester, polypropylene, recycled fiber, or mixed raw materials before carding and cross-lapping. Stable feeding contributes to more consistent web formation before needle punching.
For heavy geotextiles, the customer should select a capacity and chamber volume appropriate for the target basis weight and line speed. The blender should be integrated with the complete opening and carding section so that the feed rate remains compatible with the needle-punching line.
12.2 Carpet and Felt Lines
Nonwoven carpet, wool felt, and jute felt lines may use natural fibers, synthetic fibers, recycled fibers, or combinations of these materials. The blender provides a practical solution for storing and distributing the opened material before web formation.
When color or fiber composition is important, even blending becomes especially valuable. Consistent preparation can help reduce visible variation in the final carpet or felt product, although the final appearance also depends on carding, web laying, needle punching, finishing, and product design.
12.3 Automotive Interior Materials
Automotive interior materials often require controlled thickness, weight, resilience, and acoustic or thermal properties. Production recipes may combine polyester, recycled fibers, binder fibers, or special additives. The blender can provide an intermediate stage that helps stabilize these combinations before carding and thermal bonding.
Automotive suppliers typically require traceable production control and repeatable material quality. A well-maintained sensor-controlled blending stage can support more consistent operation and reduce manual variation in the fiber-feeding process.
12.4 Cleaning Cloth and Industrial Felt
Needle-punched cleaning cloth and industrial felt may use waste textile fibers, cotton, polyester, viscose, or other materials. These raw materials can vary considerably in length and density. The large chamber and separator help distribute the material before it reaches the carding process.
For dusty or short-fiber materials, the customer should evaluate the factory’s dust-removal system and cleaning schedule. The blender’s cleaning gate simplifies access, but safe housekeeping and suitable ventilation remain essential parts of the production environment.
12.5 Thermal-Bonded Wadding
Thermal-bonded wadding lines often use polyester and ES fiber combinations. Uniform blending helps ensure that binder fiber is available throughout the web. After carding and web forming, the material passes through a thermal bonding oven where the binder component is activated.
The big chamber blender does not perform the bonding operation, but it supports the material preparation required for a stable thermal-bonding process. The final machine configuration should be selected according to the oven width, line speed, fiber blend, and target product weight.
13. Safety Considerations
Fiber-opening and blending equipment contains moving belts, lattices, rollers, shafts, and transmission components. Operators must not reach into the machine while it is running. Guards must remain installed, and access gates must be closed during operation unless the machine has been safely isolated.
The cleaning gate safety switch should never be bypassed. Before opening the gate, operators should stop the machine, isolate the power source, and follow the plant’s lockout and tagout procedure. Residual movement and stored mechanical energy must be considered.
Fiber dust can create respiratory, housekeeping, and fire hazards. The customer should provide suitable ventilation, dust extraction, fire-prevention equipment, and regular cleaning procedures. The exact safety measures depend on the raw materials, production environment, local regulations, and complete line design.
Only trained personnel should operate, adjust, or maintain the equipment. Training should cover start-up and shutdown, sensor operation, emergency stops, cleaning, belt adjustment, lubrication, fault reporting, and safe isolation procedures.
14. Commercial and Service Information
The listed trade terms are FOB, CNF, or CIF. Customers can discuss the most suitable arrangement according to destination, shipping method, insurance, and project responsibilities. The lead time is listed as approximately 90 days after receipt of the deposit, with another listing indicating two to three months. The final schedule should be confirmed in the sales contract.
The listed payment arrangement is 30 percent advance payment and 70 percent before delivery. Commercial conditions may vary depending on the order size, customization level, shipping terms, and customer requirements.
The warranty is listed as twelve months after mechanical and electrical commissioning. Customers should confirm which parts are covered, how service requests are handled, and what exclusions apply. Proper installation, operation, maintenance, and use of approved replacement parts are normally important conditions for warranty support.
The supplier reports that it is responsible for installation and debugging, while the buyer is responsible for round-trip air tickets, accommodation, medical treatment, safety, and related expenses for installation engineers. The buyer is also expected to provide translators, workers, electrical cables, and installation tools. These responsibilities should be clearly stated in the project contract to avoid delays.
15. Frequently Asked Questions
Q1: What is the main function of the HYDC Big Chamber Blender?
The machine blends and stores opened fiber, then provides a continuous and controlled feed to a carding line or another downstream process. It acts as both a fiber-mixing unit and a production buffer.
Q2: Which raw materials can be processed?
The listed materials include polyester fiber, polypropylene staple fiber, wool, cotton, coir fiber, jute fiber, ES fiber, waste fiber, and similar opened fibers. The final suitability should be confirmed according to fiber length, bulk density, moisture, contamination, and the complete line design.
Q3: How does the machine control the fiber level?
Two photoelectric sensors monitor the feeding status. Their signals help control the operation of the feeding system and maintain an appropriate material level in the chamber.
Q4: Why is a large chamber useful?
A large chamber provides storage capacity between the opening and carding sections. It reduces the effect of short-term differences in upstream and downstream production rates and supports continuous operation.
Q5: What working widths are available?
The listed working widths are 1,700 mm, 2,000 mm, 2,500 mm, and 3,000 mm. Customized dimensions may be available depending on the project requirements.
Q6: What storage volumes are available?
The listed storage volumes are approximately 15 cubic meters, 20 cubic meters, 30 cubic meters, and 37 cubic meters. The appropriate volume depends on the required buffer time, material type, line speed, and available factory space.
Q7: What are the listed capacity options?
The technical information lists approximately 300 kg/h, 500 kg/h, 800 kg/h, and 1,000 kg/h. Another listed configuration indicates a maximum capacity of approximately 650 kg/h per set. The final capacity must be confirmed for the selected model and material.
Q8: Does the machine support different fiber formulas?
Yes. It is intended for blending different opened fibers, including combinations of synthetic, natural, ES, and waste fibers. The actual blend ratio and process conditions should be determined through production trials and line engineering.
Q9: What makes the machine different from a simple fiber hopper?
The machine combines storage with active distribution, mechanical blending, photoelectric monitoring, and continuous feeding. A simple hopper generally provides storage but may not deliver the same level of distribution and automatic control.
Q10: Is the stripper and evener roller transmission independent?
Yes. The product description specifies independent transmission for the stripper and evener roller. This supports separate adjustment and can simplify maintenance.
Q11: How is cleaning performed?
A dodge gate is installed at the end of the box to provide convenient access to the interior. The gate includes a safety switch. Operators must stop and isolate the machine before cleaning or entering any access area.
Q12: Can the blender be integrated into a complete nonwoven line?
Yes. It is designed to connect with opening and carding equipment and can be specified as part of complete lines for geotextiles, carpets, felt, automotive materials, cleaning cloth, thermal-bonded wadding, and other nonwoven products.
Q13: Is customization available?
The supplied information indicates customization of working width, color, voltage, conveyor length, and other project elements. Customers should provide detailed production, material, layout, and electrical requirements for a formal proposal.
Q14: What certification information is listed?
The product information lists CE and ISO9001-related certification. Buyers should request the applicable certificates and technical documents for the exact machine configuration.
Q15: What is the warranty period?
The listed warranty period is twelve months after mechanical and electrical commissioning. The detailed warranty scope should be confirmed in the purchase agreement.
16. Conclusion
The HYDC Big Chamber Blender is a practical solution for nonwoven manufacturers that need reliable fiber blending, intermediate storage, and continuous feeding. Its design combines an anti-skidding horizontal delivery lattice, a supported spike lattice, a rotary separator, photoelectric sensors, independent stripper and evener roller transmission, and a cleaning gate with a safety switch.
The machine is suitable for a wide range of synthetic, natural, ES, recycled, and waste fibers. Its available working widths, chamber volumes, and capacity options allow it to be adapted to different carding lines and production targets. More importantly, it is designed as part of an integrated nonwoven process rather than as an isolated storage unit.
Changshu Hongyi Nonwoven Machinery Co., Ltd. strengthens the product with more than two decades of nonwoven machinery experience, a broad equipment portfolio, complete-line engineering capability, customization support, international project experience, and installation and commissioning service. These capabilities are valuable for customers seeking a coordinated solution from fiber opening through carding, web forming, needle punching, thermal bonding, winding, and cutting.
Before purchase, buyers should confirm the raw-material formula, expected output, card width, chamber volume, electrical standard, layout, dust-control requirements, installation responsibilities, warranty conditions, and final technical specifications. When correctly selected, installed, and maintained, a big chamber blender can provide a stable foundation for efficient, consistent, and scalable nonwoven production.
References
1. Product technical description for the HYDC Big Chamber Blender, including structural design, operating functions, and application information.
2. HYDC technical parameter sheet covering working width, storage volume, capacity, installed power, and configuration options.
3. Changshu Hongyi Nonwoven Machinery Co., Ltd. company information and nonwoven machinery product portfolio.
4. Supplied trade information covering lead time, payment terms, warranty, installation, commissioning, and after-sales responsibilities.
5. General engineering principles for fiber opening, blending, card feeding, web formation, needle punching, thermal bonding, and nonwoven production-line integration.