

Content
- 1 1. The Role of a Bale Opener in Nonwoven Manufacturing
- 2 2. Main Construction and Working Principle
- 3 3. Key Advantages of the Automatic Bale Opener
- 4 4. Comparison with Manual and Less Integrated Systems
- 5 5. Applications in Nonwoven Fabric Production
- 6 6. Manufacturing Strengths and Engineering Capabilities
- 7 7. Production Quality and Process Control
- 8 8. Specification Overview
- 9 9. Installation, Commissioning, and After-Sales Support
- 10 10. Maintenance and Safe Operation
- 11 11. How to Select the Correct Configuration
- 12 12. Purchasing Considerations for International Buyers
- 13 13. Why the Bale Opener Matters to Overall Product Quality
- 14 14. Company Manufacturing and Service Strengths
- 15 15. Frequently Asked Questions
- 15.1 Q1: What is the main function of the bale opener?
- 15.2 Q2: Can the machine process more than one fiber type?
- 15.3 Q3: What fibers can be used?
- 15.4 Q4: How does automatic weighing improve production?
- 15.5 Q5: What working widths are available?
- 15.6 Q6: What is the stated capacity?
- 15.7 Q7: Can the bale opener be connected to an existing production line?
- 15.8 Q8: Is the equipment customized?
- 15.9 Q9: What certification is listed for the machine?
- 15.10 Q10: What warranty is offered?
- 15.11 Q11: Does the supplier provide installation support?
- 15.12 Q12: What should be prepared before installation?
- 15.13 Q13: Is the bale opener suitable for a complete nonwoven production line?
- 15.14 Q14: How should the machine be maintained?
- 15.15 Q15: Why choose an automatic system instead of manual blending?
- 16 16. Conclusion
- 17 References
- 18 Product: HYKB Bale Opener
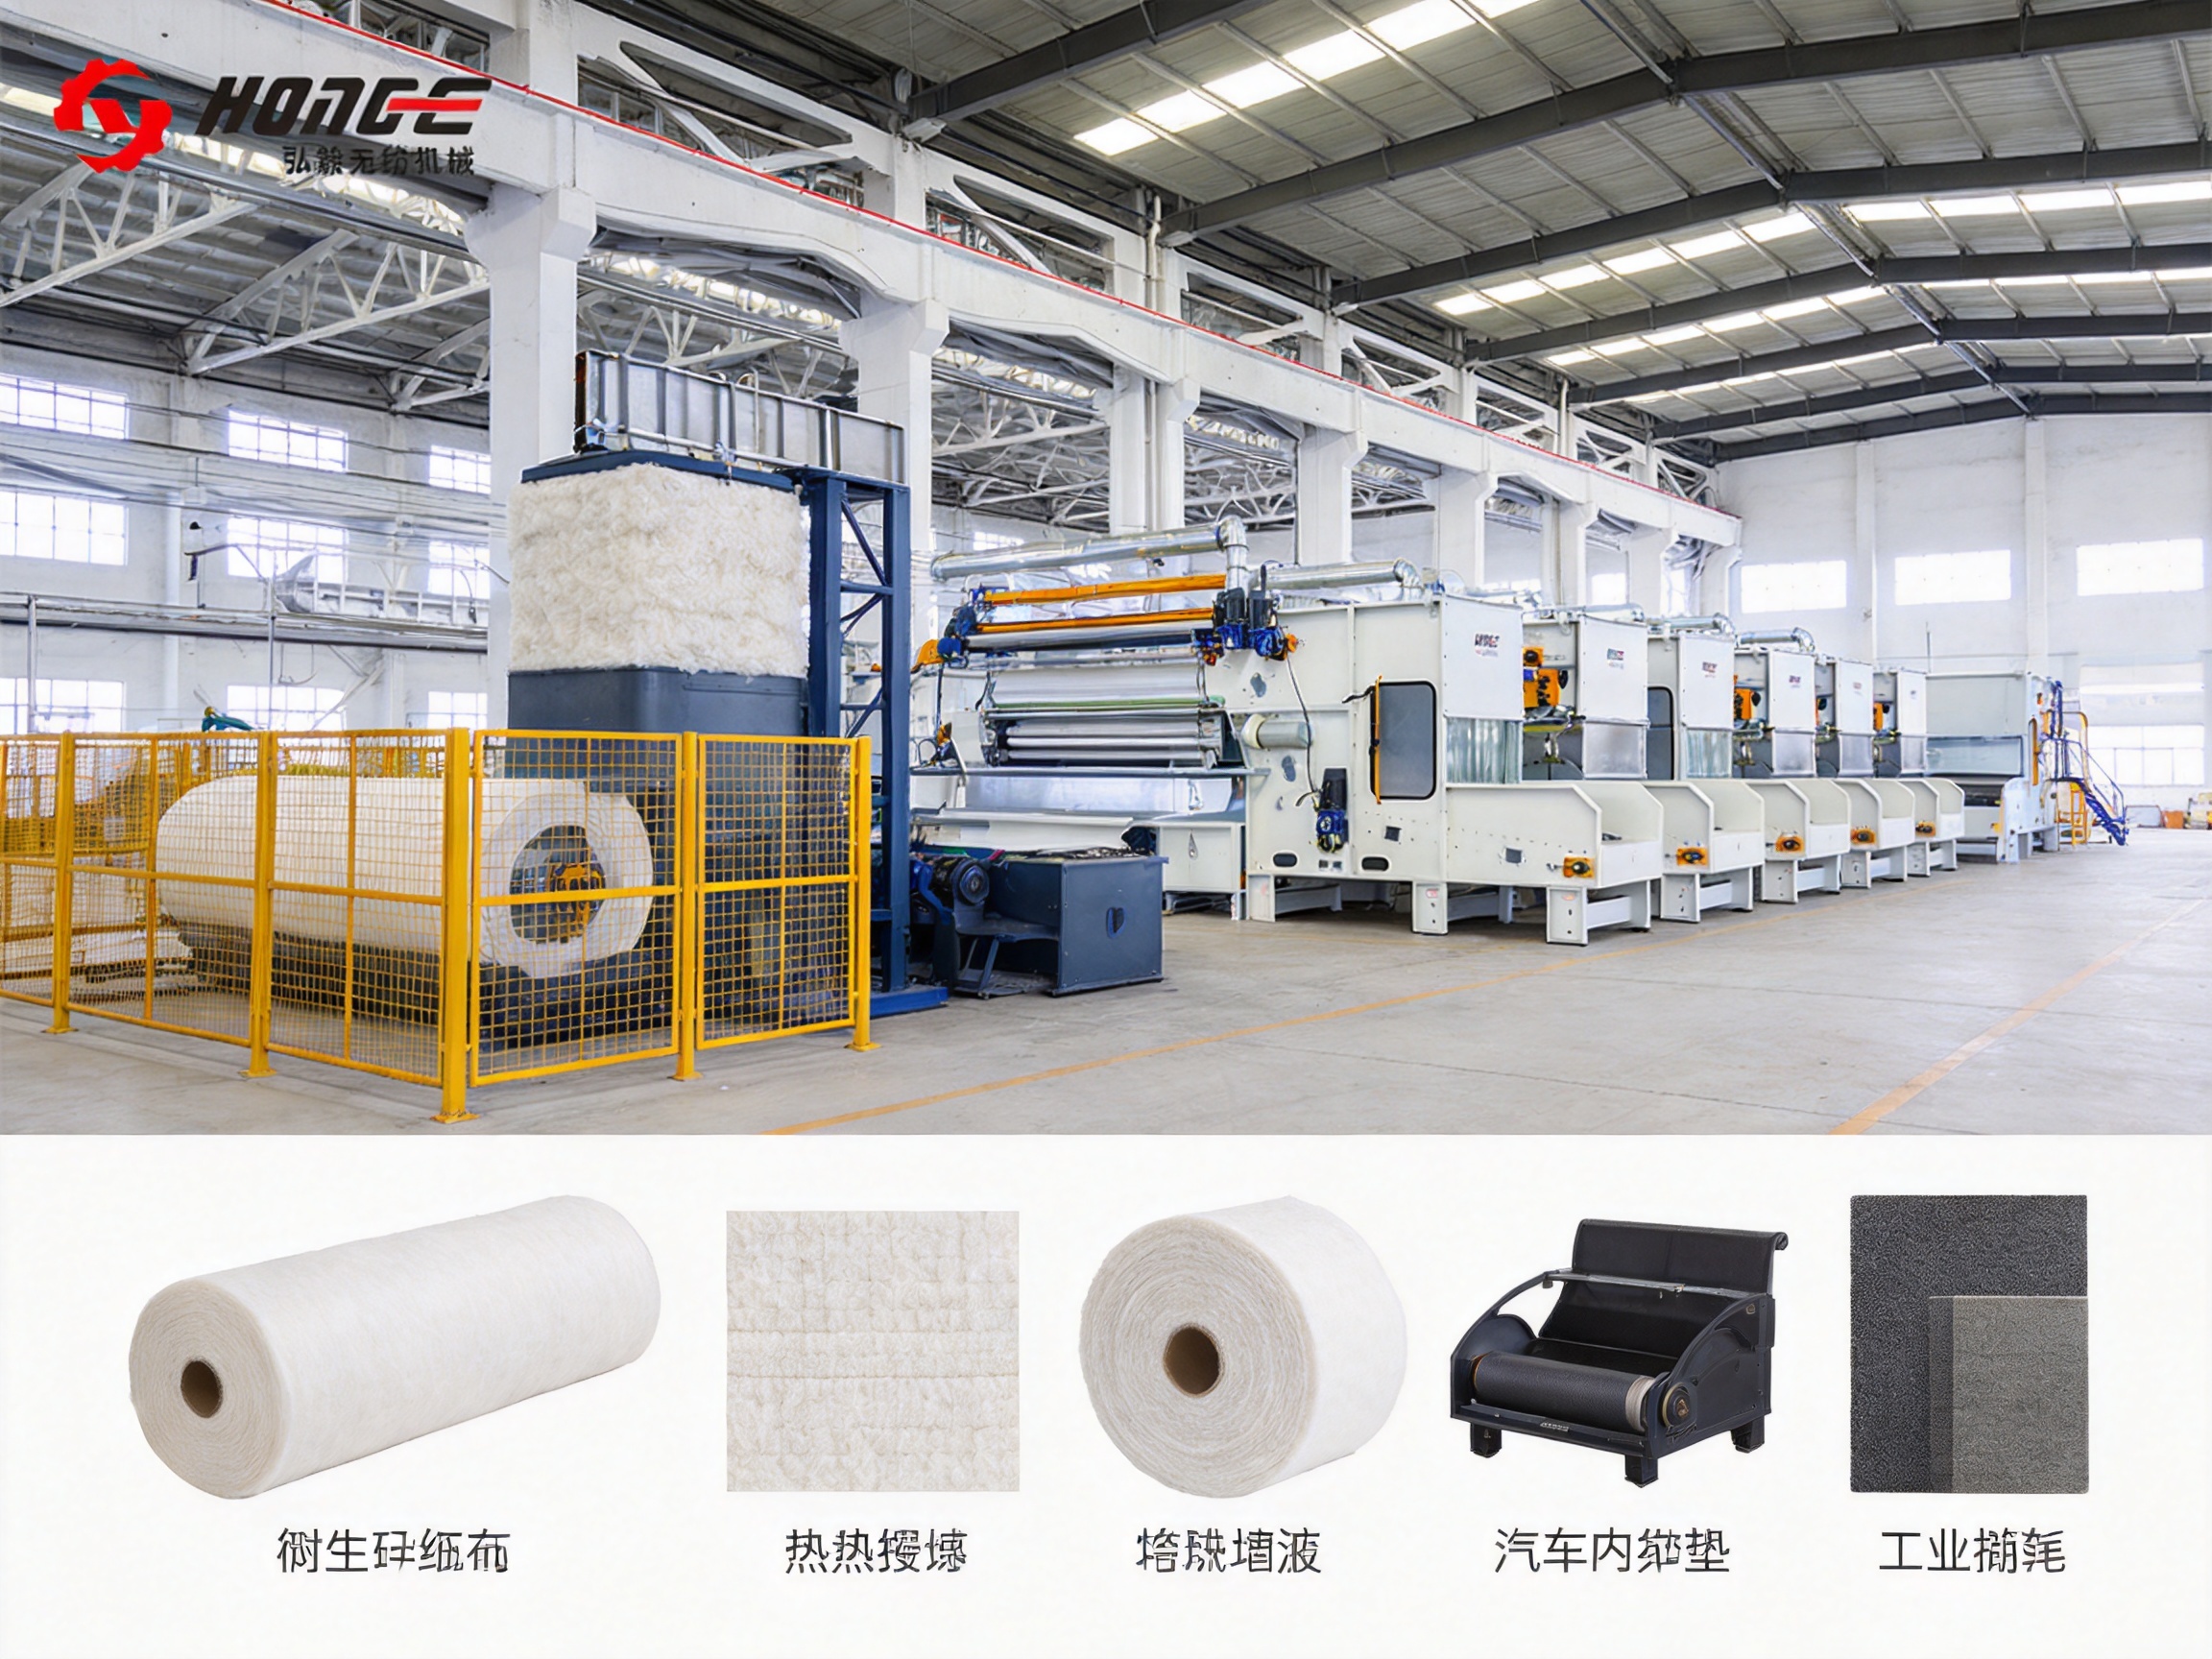
Modern nonwoven fabric production depends on consistent raw-material preparation. Before fibers reach a carding machine, airlay system, thermal bonding oven, needle punching line, or other forming equipment, they must be opened, proportioned, and blended as evenly as possible. Inadequate opening can leave compressed tufts, while inaccurate blending may cause variations in web weight, strength, color, softness, absorbency, and finished-product appearance. The bale opener is therefore one of the most important preparation machines in a complete nonwoven production line.
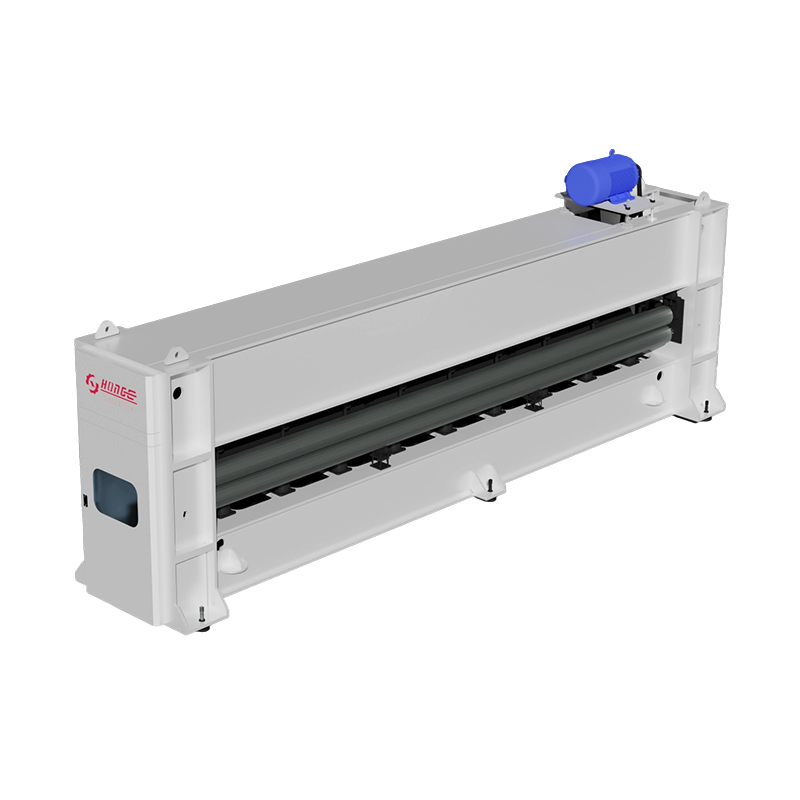
The HYKB Bale Opener is designed to pre-open fibers from bales, weigh predetermined quantities, and transfer the prepared material through a cross conveyor toward the next stage of production. Its automatic weighing function and modular configuration make it suitable for operations that process one fiber type or combine several materials in a controlled blend. The system is available in multiple working widths and can be adapted to the requirements of different nonwoven production lines.
Manufactured by Changshu Hongyi Nonwoven Machinery Co., Ltd., the equipment reflects the company’s long-term specialization in nonwoven machinery, complete production lines, and individual processing units. The manufacturer combines mechanical engineering, electrical control, customized design, installation support, and after-sales service to provide practical solutions for customers in different regions and applications.
1. The Role of a Bale Opener in Nonwoven Manufacturing
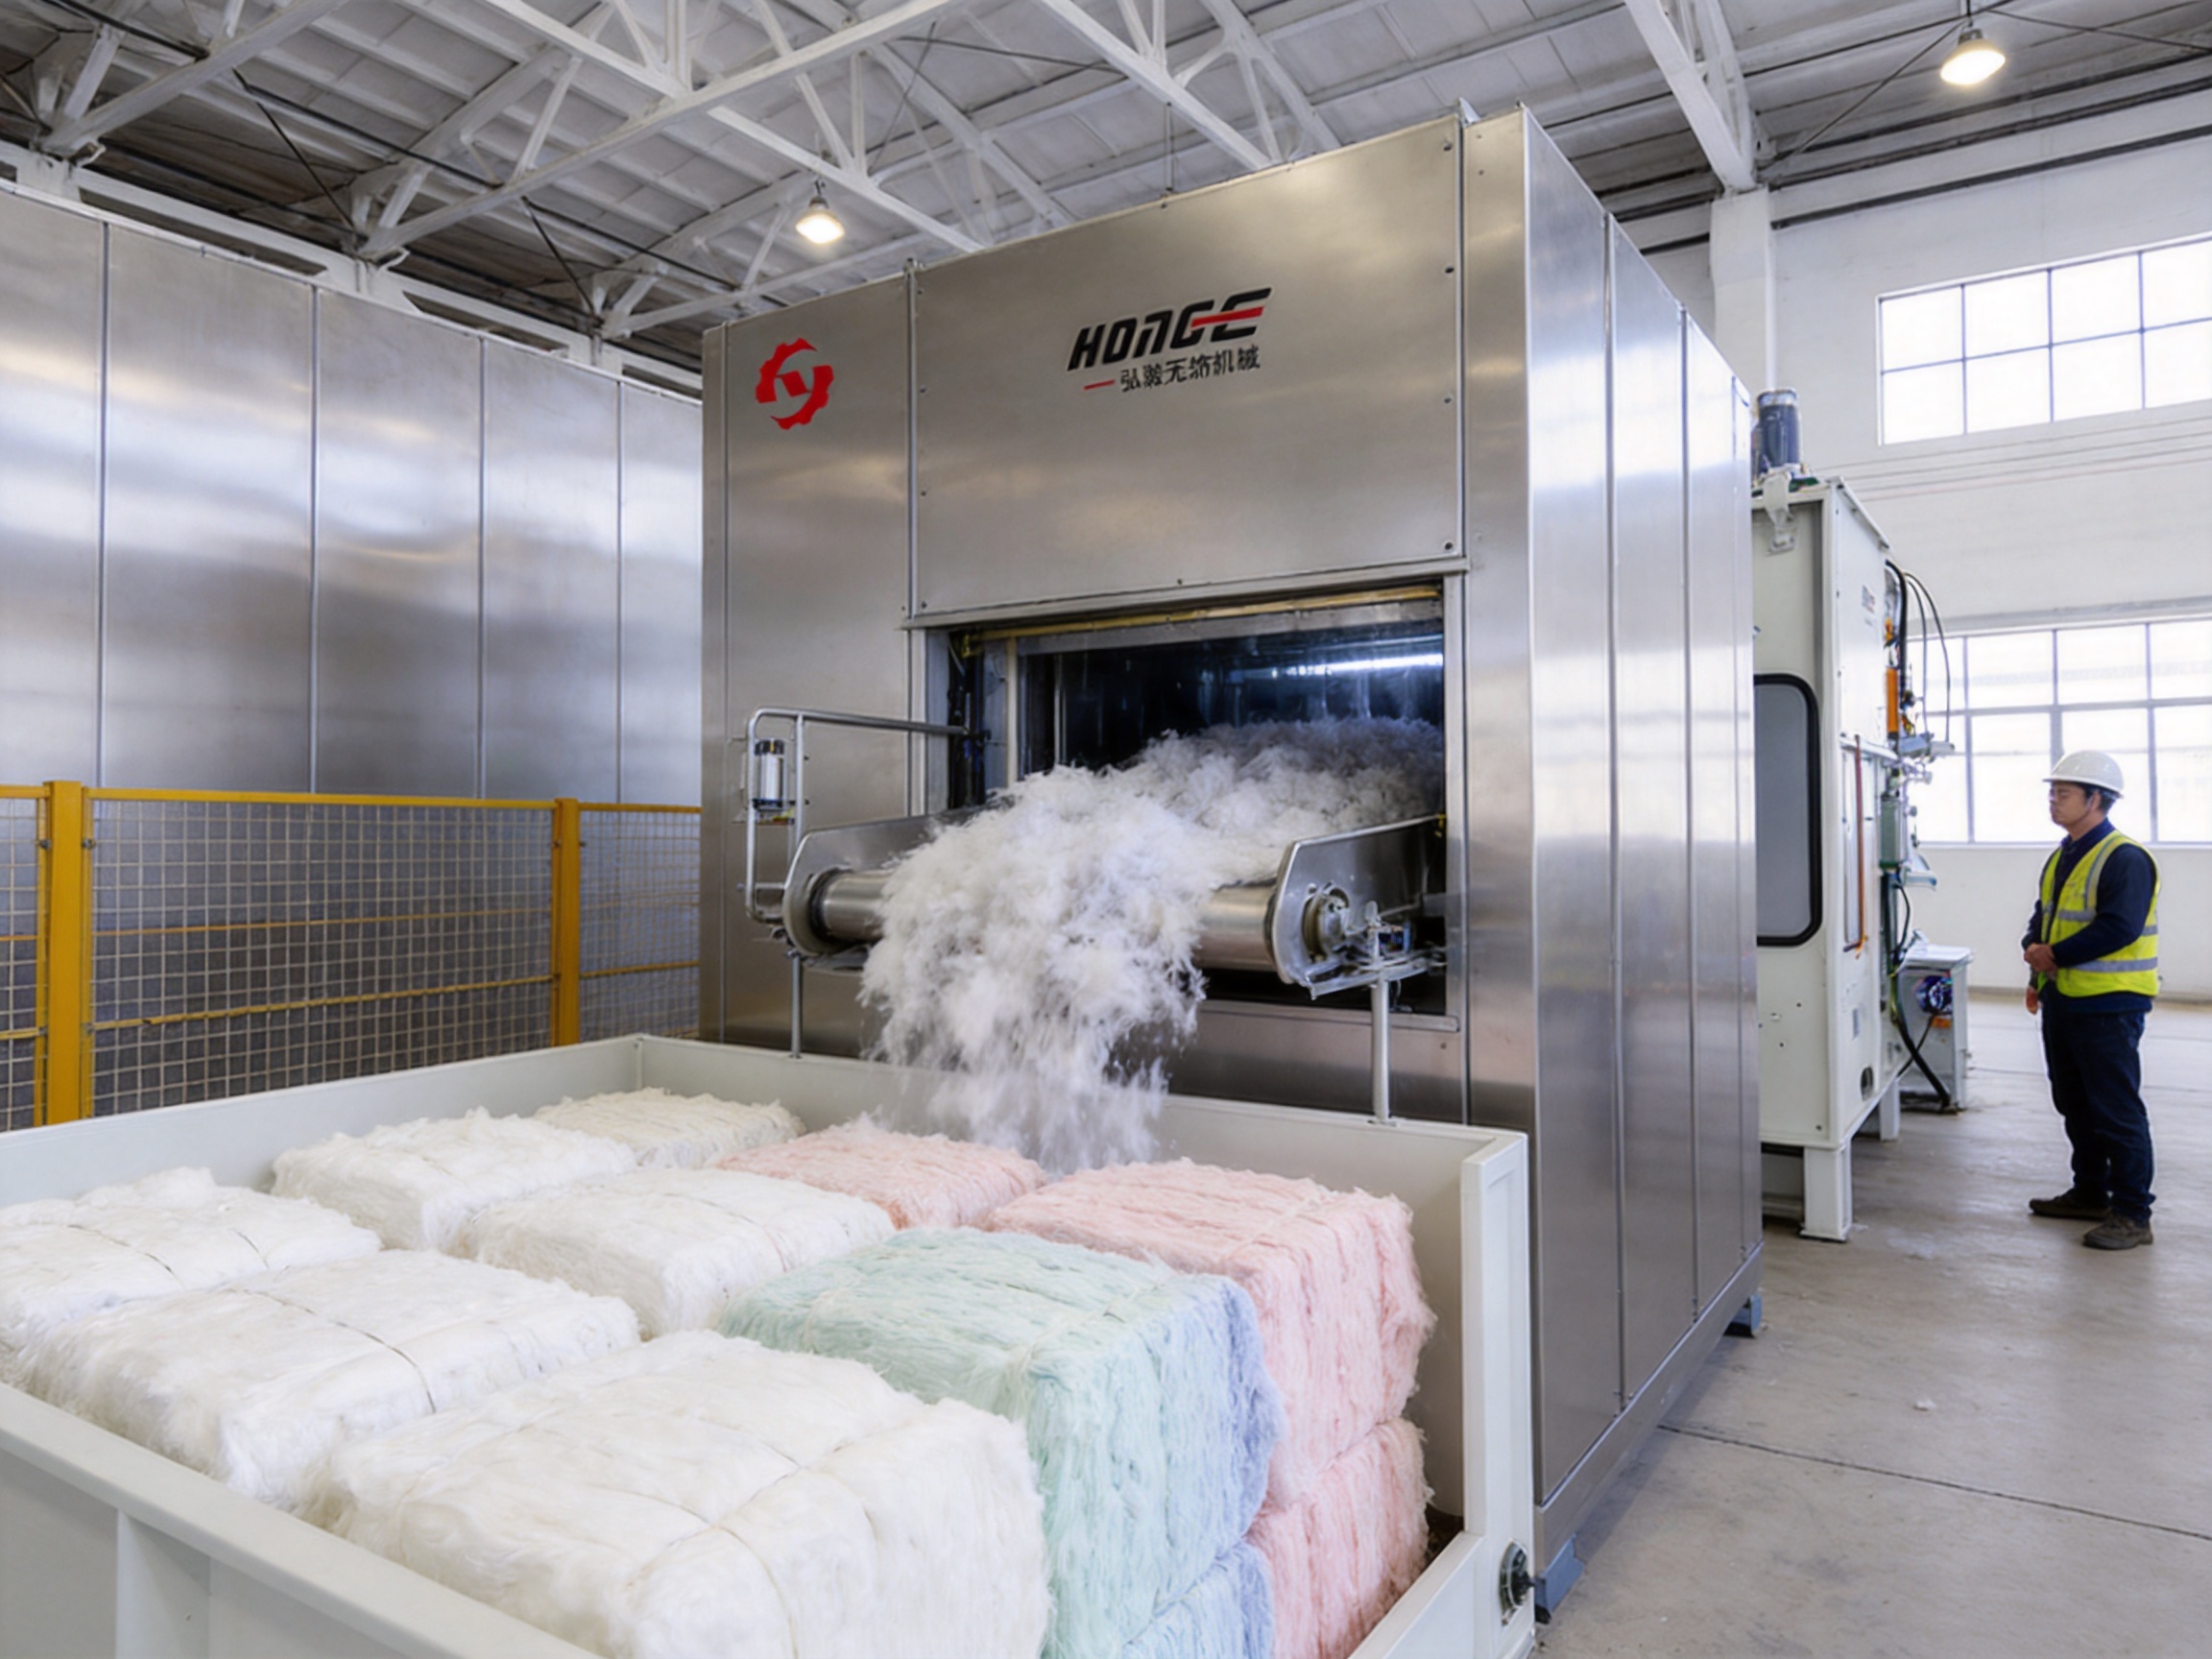
Most textile and nonwoven fibers are delivered in compressed bales. Compression reduces transportation and storage costs, but it also creates a dense mass that cannot be fed directly into downstream equipment with reliable consistency. The first task of a bale opener is to loosen this compact material and restore the fiber to a more open condition.
Pre-opening is not the same as final fiber opening. A bale opener prepares the material for subsequent machines by separating large compressed sections, removing excessive density, and creating a more manageable flow. Depending on the process, the opened material may then pass to a fine opener, blending chamber, carding machine, airlay machine, or another fiber preparation unit.
A bale opener also contributes to blend accuracy. Nonwoven manufacturers commonly process combinations of polyester, polypropylene, viscose, recycled fibers, low-melt fibers, natural fibers, and other raw materials. Each material may have a different proportion in the final product. When the percentage of each fiber is established by manual estimation alone, production results may vary from batch to batch. An automatic weighing system provides a more controlled basis for proportioning.
The HYKB system is developed to combine these functions in one coordinated machine. It pre-opens fiber, controls the quantity of material, weighs the required amount, and transfers the prepared blend through a cross conveyor. Several bale openers may also be used together when a production recipe contains multiple fiber types.
2. Main Construction and Working Principle
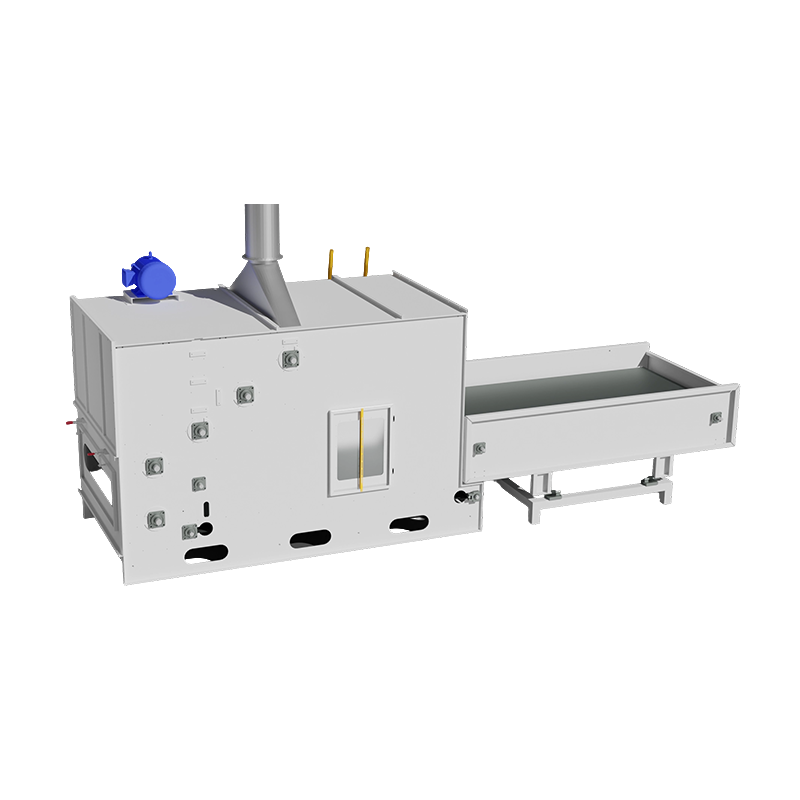
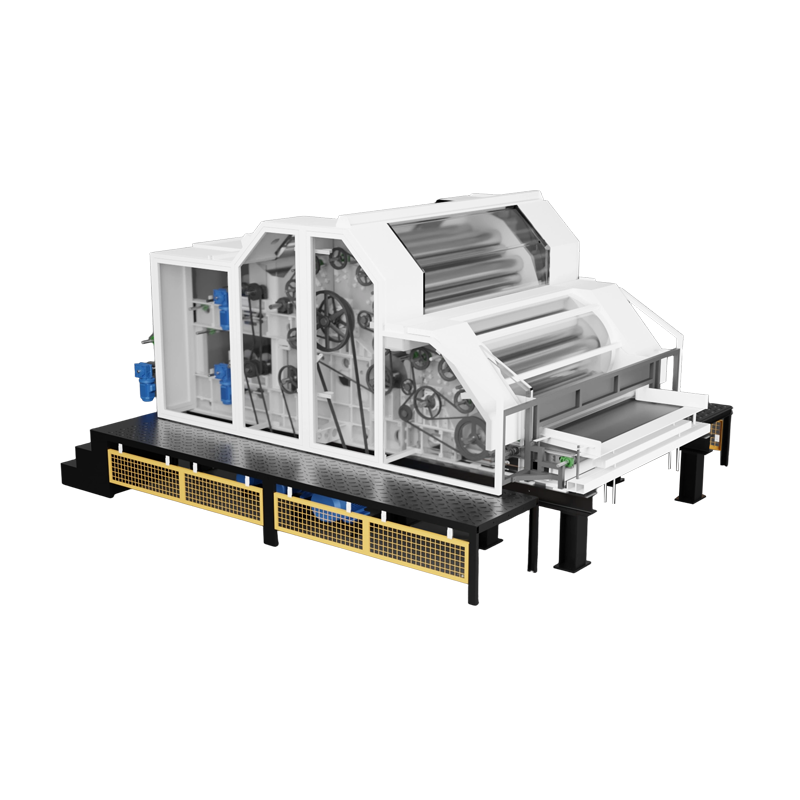
The machine is arranged in three principal sections. Each section performs a different function within the opening and blending process. This layout creates a continuous workflow from bale loading to measured material transfer.
2.1 Front Fiber Storage Section
The front section provides space for placing and storing the fiber bales. Operators can arrange the raw material according to the production recipe, material type, or feeding sequence. This storage area supports continuous operation by allowing a suitable quantity of fiber to be prepared before the material enters the feeding and opening zone.
The storage design is important because bale preparation should not interrupt the production line unnecessarily. A well-organized storage area also helps operators distinguish between different fiber types, colors, grades, and batch numbers. This is especially useful when the production recipe includes several raw materials with different physical properties.
2.2 Middle Feeding and Pre-Opening Section
The middle section feeds compressed fiber toward the pre-opening mechanism. During this stage, the machine separates material from the bale and loosens the compacted mass. The objective is to produce an even and controllable feed rather than large, irregular chunks.
Controlled feeding protects downstream equipment from sudden surges. A carding machine, airlay machine, or fine opener performs more consistently when the incoming material has a stable density and flow. Pre-opening also improves the opportunity for different fibers to mix with one another before the final web-forming process.
The machine is designed for the opening of various fiber types. The exact operating settings should be selected according to fiber length, fineness, crimp, moisture content, bale density, and the intended end product. Softer or more delicate fibers may require gentler treatment, while heavily compressed or more resistant materials may need a different feeding adjustment.
2.3 Rear Weighing and Proportioning Section
The latter section weighs the material according to the required proportion. Electronic weighing provides a measurable reference for fiber input quantity. Instead of relying entirely on manual judgment, operators can establish a production recipe and use the control system to manage the target quantity of each material.
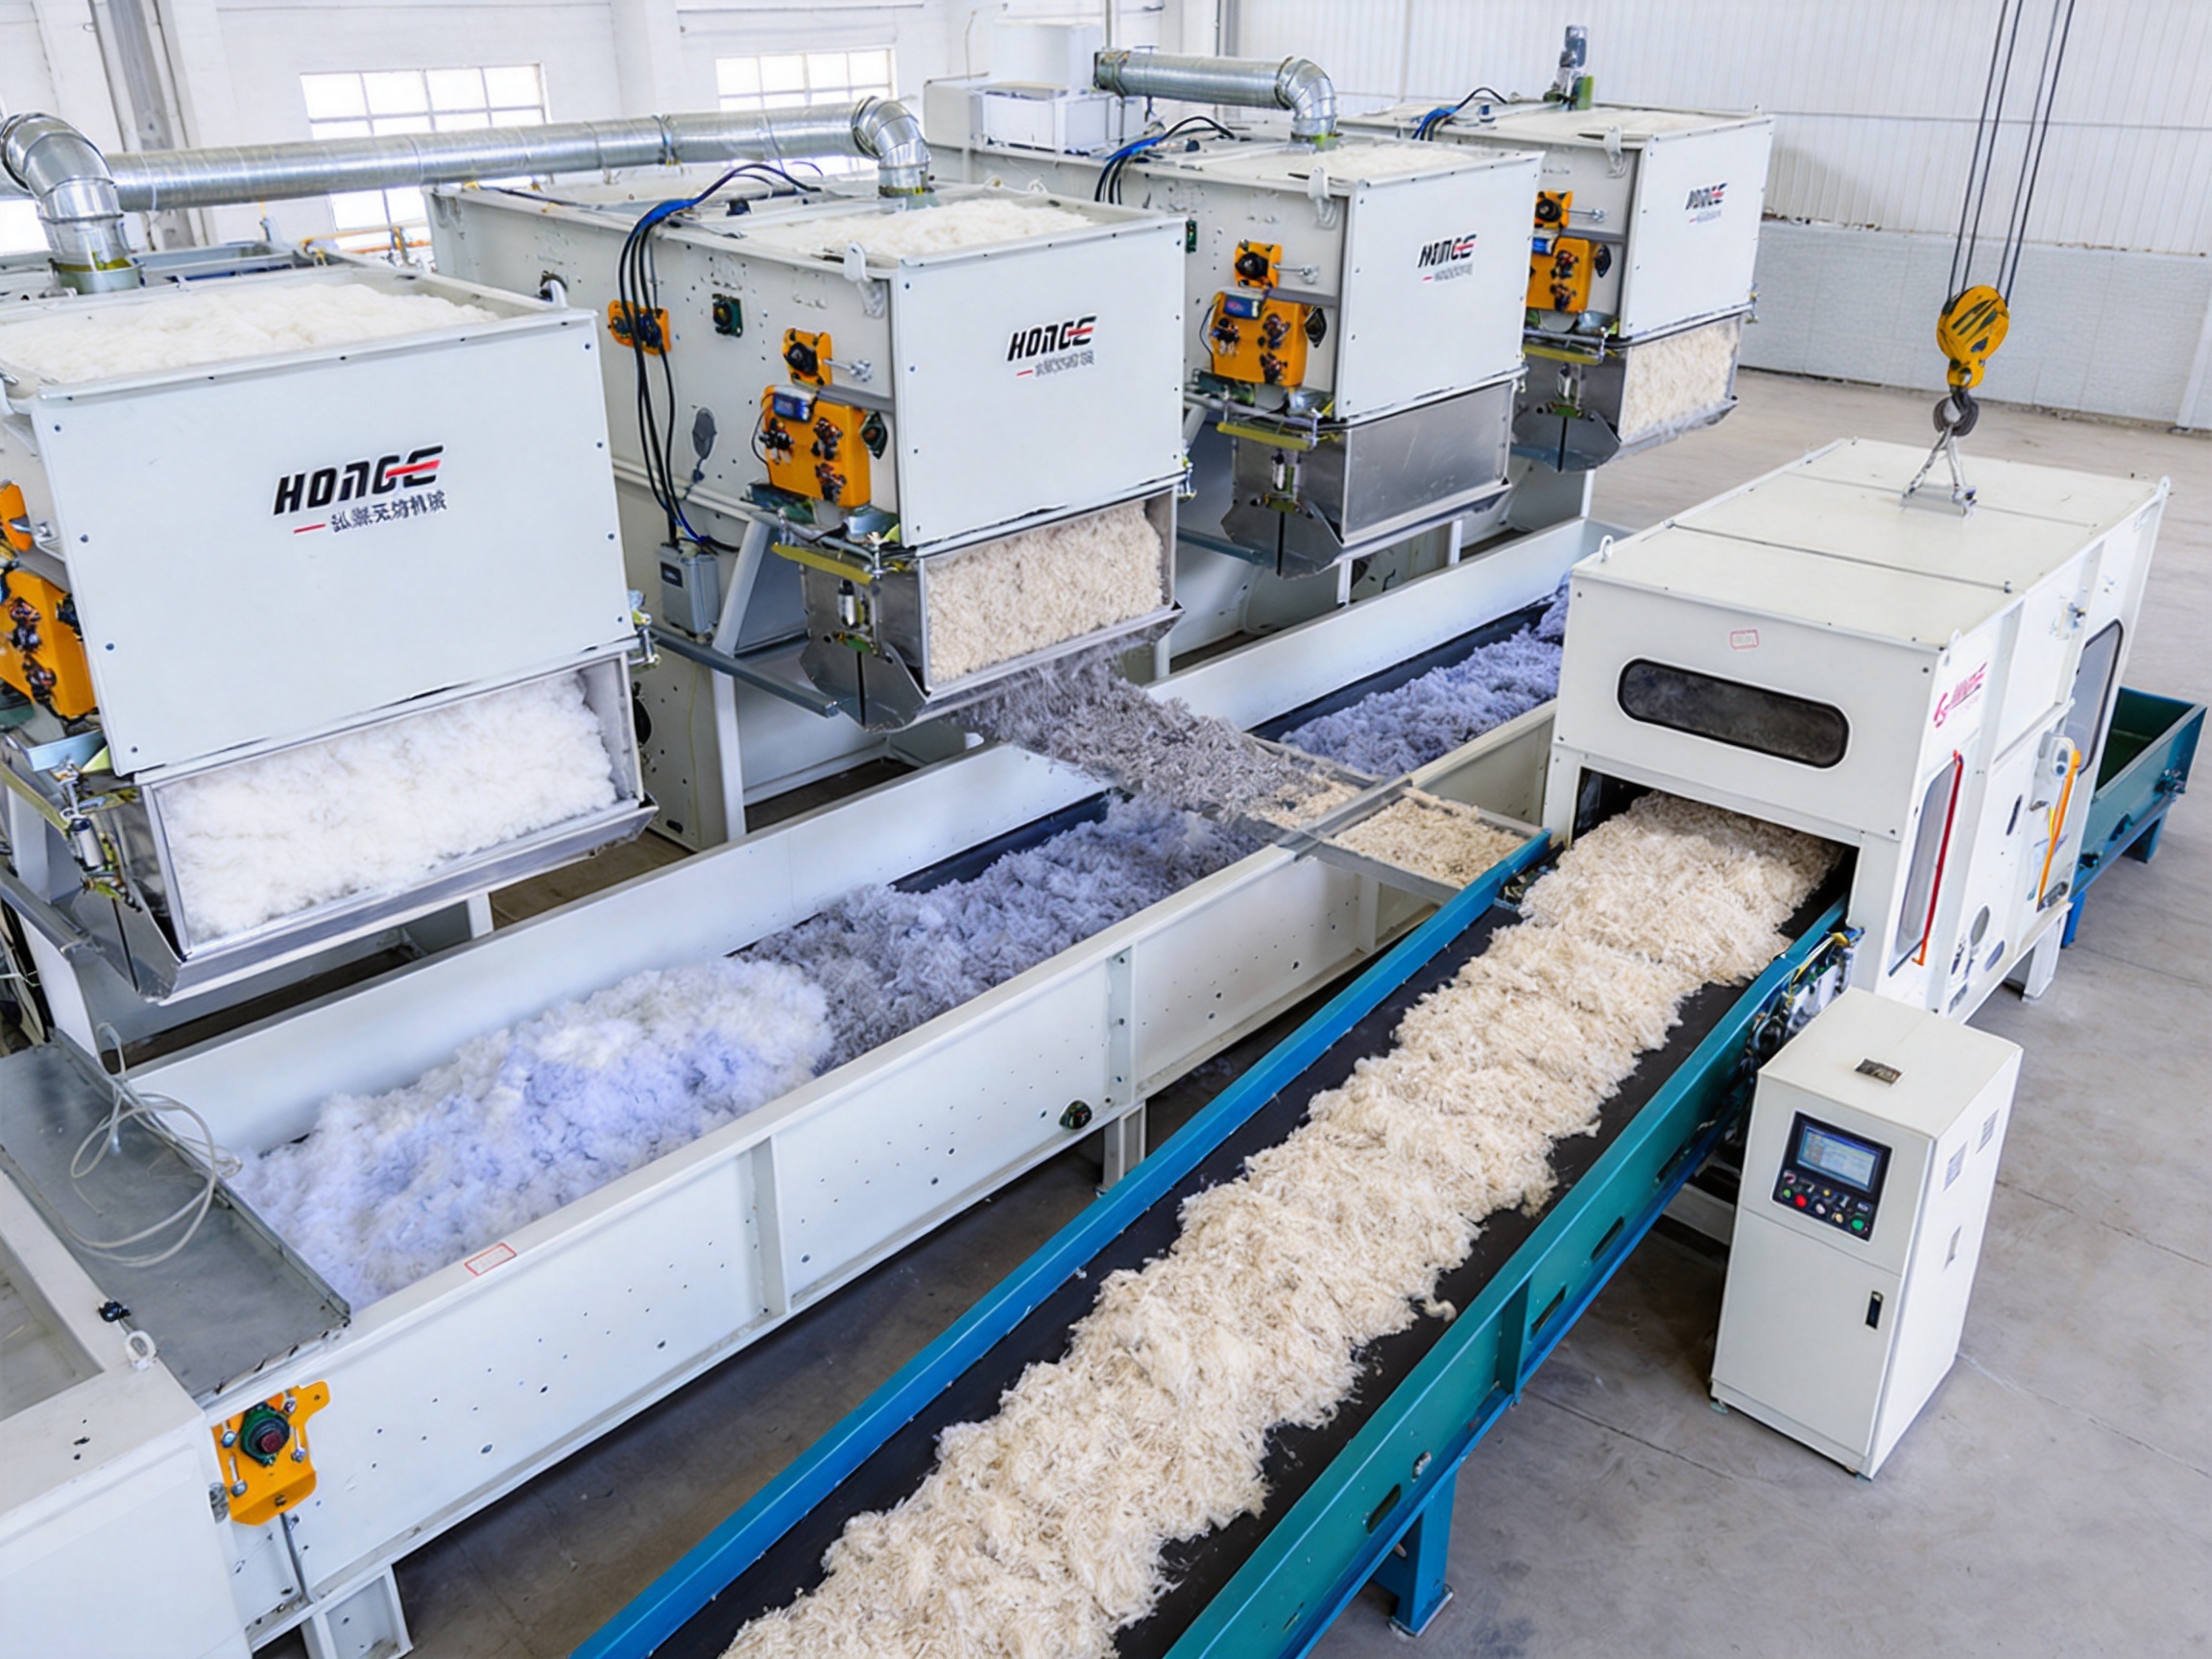
When several bale openers work together, each unit can be assigned a particular fiber or proportion. The resulting material streams can then be combined through the transfer system. This configuration allows manufacturers to produce blends with greater repeatability and to change the recipe when the product specification changes.
2.4 Cross Conveyor Transfer
After weighing, the prepared fiber is transferred by a cross conveyor toward the opener or the next machine in the line. This arrangement supports a coordinated material flow and helps connect multiple bale openers with downstream equipment.
The transfer function is particularly valuable in complete nonwoven production lines, where available floor space, machine arrangement, and process direction must be considered together. Conveyor positioning can be integrated into the overall line design so that the opening and blending equipment operates as part of a continuous production system rather than as an isolated unit.
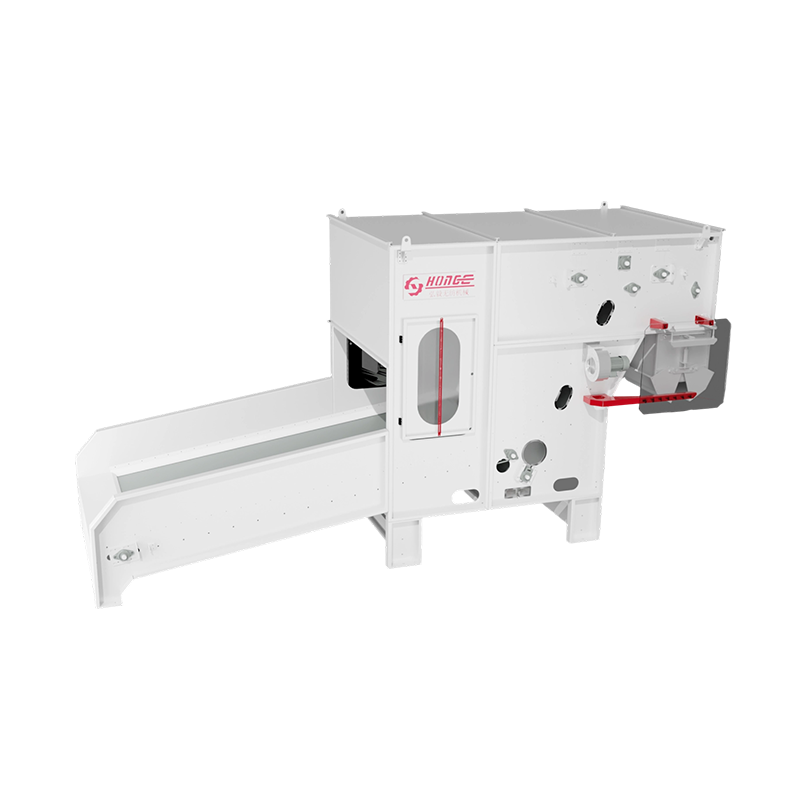
HYKB Bale Opener
3. Key Advantages of the Automatic Bale Opener
3.1 More Consistent Fiber Proportioning
The most important advantage of an automatic weighing bale opener is improved control over material proportioning. Fiber blends influence many finished-product properties, including tensile strength, tear resistance, thermal insulation, bulk, softness, filtration performance, absorbency, and bonding behavior.
If the proportion of a low-melt fiber is too high, the finished web may become excessively stiff after thermal bonding. If the proportion is too low, bonding strength may be insufficient. A variation in recycled fiber content may affect color, bulk, and mechanical performance. The ability to set a defined input quantity helps reduce these fluctuations.
Automatic weighing does not eliminate the need for process management. Operators must still select appropriate settings, verify the scale, monitor the condition of the raw material, and inspect the output. However, the system provides a reliable control point that is difficult to achieve through manual feeding alone.
3.2 Multi-Fiber Compatibility
The equipment is intended for a broad range of fiber materials, including PET fiber and other fibers used in nonwoven production. The multi-machine configuration makes it possible to process several raw materials within one production plan.
This flexibility is valuable for manufacturers that produce multiple grades of nonwoven fabric. One production line may be used for automotive interior materials, geotextiles, filtration media, cleaning cloths, carpet substrates, thermal insulation, mattress materials, or other products. Each application may require a different combination of fiber types and percentages.
Rather than installing a separate opening system for every product, a manufacturer can configure the bale-opening section around its recipe requirements. This improves production flexibility and can make better use of available factory space.
3.3 Improved Downstream Feeding
Large, compressed fiber lumps can cause unstable feeding, machine blockage, uneven carding, and web-weight variation. Pre-opening creates a more uniform material condition before the fiber reaches downstream machinery.
A steadier fiber flow allows the carding machine to perform more effectively. In an airlaid process, it can support more stable fiber distribution. In a needle punching line, consistent preparation contributes to more uniform web formation before the needle loom. In thermal bonded products, an even blend helps the bonding oven produce a more predictable result.
The bale opener should therefore be evaluated not only by its own output but also by its contribution to the performance of the complete production line.
3.4 Automatic Operation and Reduced Manual Handling
The automatic grade of the machine reduces the amount of repetitive manual feeding and measuring required from operators. This can improve workplace organization and reduce the possibility of inconsistent human estimation.
Automatic operation also makes it easier to repeat a production recipe. When a product is manufactured regularly, the operating parameters can be documented and used as a reference for future batches. Standardized settings support quality control and simplify operator training.
3.5 Modular Expansion
The system allows several sets to be combined. This modular approach is one of its practical advantages over a fixed single-material opener. A basic configuration may be suitable for a simple product, while a larger arrangement can support a blend containing multiple fiber types.
Modular expansion also helps manufacturers plan investment in stages. A company may initially install the equipment for a limited number of materials and later add additional units when product variety or production capacity increases. Final feasibility depends on the factory layout, control architecture, and line design, but the modular concept provides useful flexibility.
3.6 Multiple Working Widths
The bale opener is available in working widths of 1 meter, 1.2 meters, 1.4 meters, 1.6 meters, and 2 meters. This range allows the equipment to be selected according to the desired production width and the configuration of the downstream nonwoven machinery.
Choosing the correct working width is important. A machine that is too narrow may restrict production capacity or require unsuitable material distribution. A machine that is unnecessarily wide may increase investment and occupy more floor space than required. The width should therefore be selected together with the target output, fiber type, downstream machine width, and future expansion plans.
4. Comparison with Manual and Less Integrated Systems
Traditional manual opening and blending methods may require workers to break bales, estimate quantities, transfer materials, and mix fibers by hand. Such methods can be appropriate for laboratory trials, very small production runs, or applications with simple material requirements. However, they become increasingly difficult to control as output, blend complexity, and quality expectations increase.
Evaluation Area | Manual Bale Preparation | Basic Single-Feed Opener | Automatic Multi-Fiber Bale Opener |
Fiber pre-opening | Dependent on operator technique | Available, usually for one feed stream | Controlled pre-opening for production feeding |
Material proportioning | Estimated or manually measured | Limited | Electronic weighing and recipe-based quantity control |
Multiple fiber types | Possible but labor-intensive | Often restricted | Several units can be combined for different materials |
Repeatability | Can vary between batches | Moderate | Improved through automatic weighing and documented settings |
Downstream integration | Limited | Depends on layout | Cross-conveyor transfer supports complete line integration |
Production flexibility | High in theory, but slow in practice | Suitable for simpler recipes | Suitable for changing recipes and multi-fiber production |
The automatic system offers a stronger balance between flexibility and control. It is not merely a larger version of a manual bale-opening station. Its value comes from the combination of mechanical opening, electronic weighing, conveyor transfer, and the ability to coordinate several machines.
Compared with a basic single-feed opener, the multi-fiber arrangement offers a more suitable platform for manufacturers that need several material streams. The production line can be designed around the required recipe rather than forcing all products into one fixed feeding method.
5. Applications in Nonwoven Fabric Production
5.1 Needle-Punched Geotextiles
Geotextile production often requires stable fiber preparation because the finished material must provide predictable strength, elongation, filtration, drainage, or separation performance. Polyester and polypropylene are frequently considered for different geotextile specifications. A controlled bale-opening and blending process helps maintain consistent raw-material input before carding and needle punching.
For products with recycled content or blended fiber grades, automatic weighing is particularly useful. The manufacturer can establish a repeatable blend and monitor the material preparation stage as part of the overall quality system.
5.2 Nonwoven Carpet Substrates
Carpet backing and related nonwoven substrates may require a combination of fibers chosen for bulk, stability, bonding, resilience, and cost. The bale opener can support the preparation of these blends before the material proceeds to carding, cross-lapping, needle punching, or thermal bonding equipment.
Consistent opening helps distribute the fibers more evenly and reduces the possibility of dense lumps entering the web-forming process. This can support a more uniform substrate structure and a more stable finishing operation.
5.3 Automotive Interior Materials
Automotive interior products often demand controlled weight, acoustic performance, resilience, dimensional stability, and compatibility with thermal bonding. Production recipes may contain several fiber types, including structural fibers and bonding fibers.
The automatic bale opener provides a practical preparation stage for these complex blends. By weighing fibers before they enter the downstream line, the manufacturer gains better control over the material composition and can more easily reproduce a validated formulation.
5.4 Cleaning Cloths and Industrial Felts
Needle-punched cleaning cloths and industrial felts may use polyester, viscose, recycled fibers, or other materials depending on the desired absorbency, strength, surface texture, and durability. Pre-opening and blending are essential for transforming compressed bales into a suitable feed for the carding and needling stages.
The equipment can help manufacturers manage different product recipes while maintaining a common preparation platform. This supports efficient production where several grades are manufactured on the same line.
5.5 Wool Felt and Jute Felt
Natural fibers such as wool and jute can have distinct physical characteristics, including variation in length, moisture response, bulk, and fiber cohesion. A suitable opening and blending process helps create a more even input for subsequent web formation.
Because natural fibers may respond differently from synthetic fibers, the machine should be configured and operated according to the characteristics of the selected material. The manufacturer’s technical team can review the raw material and production objective before confirming the final design.
5.6 Thermal Bonded Wadding and Insulation
Thermal bonded wadding commonly uses combinations of carrier fibers and low-melting bonding fibers. The blend ratio directly affects bonding behavior, loft, softness, resilience, and thermal performance. Automatic weighing gives the operator a stronger foundation for maintaining the intended recipe before the web enters a thermal bonding oven or heat-setting unit.
In insulation production, uniformity is essential. Variations in fiber distribution can produce local differences in thickness, density, or thermal resistance. Controlled preparation reduces one important source of variation.
6. Manufacturing Strengths and Engineering Capabilities
Changshu Hongyi Nonwoven Machinery Co., Ltd. has more than 20 years of experience in the nonwoven machinery field. Its product range includes complete production lines and individual machines for opening, carding, airlay forming, needle punching, thermal bonding, ironing, winding, cutting, and related operations.
This breadth of experience is valuable when designing a bale opener because the equipment must work correctly with the machines installed before and after it. A supplier that understands only one machine may provide a unit that functions independently but does not integrate efficiently into the complete process. A manufacturer with experience in complete nonwoven lines can evaluate material flow, working width, production capacity, control requirements, and the relationship between each machine.
6.1 Complete Line and Unit-Machine Experience
The company supplies equipment for needle-punched geotextiles, nonwoven carpets, airlaid waste felt, automotive interior materials, cleaning cloths, wool felt, jute felt, and other nonwoven products. This application experience gives the engineering team exposure to different fiber types, product specifications, and production challenges.
The bale opener can therefore be supplied as an individual machine or as part of a larger nonwoven fabric production line. Customers that are expanding an existing factory may require only an opening and blending unit, while new projects may need a full line including carding, web forming, needle punching, thermal bonding, winding, and cutting equipment.
6.2 Customized Engineering
The equipment is listed as customizable. Customization may involve working width, voltage, machine arrangement, conveyor direction, control requirements, connection with existing machinery, and the number of bale-opening units used in a blend.
Proper customization begins with technical information. The buyer should provide the fiber type, fiber length, bale density, target production capacity, blend ratio, finished-product width, downstream machine details, factory layout, and local electrical standards. The supplier can then determine whether the standard configuration is suitable or whether engineering modifications are needed.
6.3 Electrical and Automatic Control
Automatic weighing is a central feature of the design. Electrical controls coordinate feeding, weighing, and material transfer. The supplied specifications identify the machine as automatic and indicate that the voltage can be 220 volts or customized according to customer requirements.
Control-system design should be assessed together with the complete production line. A well-integrated control arrangement allows operators to monitor the material preparation stage and coordinate it with downstream equipment. It can also simplify fault identification and production adjustment.
6.4 Quality and Certification Orientation
The product information identifies CE and ISO9001:2000 certification. These references indicate an orientation toward documented manufacturing and quality-management practices. Certification should always be confirmed for the exact configuration supplied, but the presence of such standards is an important consideration when comparing machinery suppliers.
Quality in machinery manufacturing includes more than the final assembly. It involves material selection, component inspection, machining accuracy, welding quality, electrical installation, protective guarding, factory testing, packaging, documentation, and after-sales support.
6.5 Factory Testing and Inspection
Video outgoing inspection is listed as available. Factory inspection is useful because it gives the buyer an opportunity to review the appearance, operation, control functions, and basic material-transfer performance before shipment.
For a customized line, the inspection process should cover the agreed working width, motor and electrical specifications, weighing operation, conveyor direction, safety devices, control-panel functions, and connection points for downstream equipment. A clear inspection checklist helps both parties confirm that the supplied machine corresponds to the technical agreement.
7. Production Quality and Process Control
The performance of a bale opener depends on both machine construction and process discipline. Even an advanced system requires appropriate operating procedures. The following controls are important for stable production.
7.1 Raw-Material Identification
Different fibers should be clearly identified before they are loaded into the machine. Labels should include material type, grade, color, batch number, and any relevant production information. Mixing the wrong bale into a recipe can affect the entire production batch.
7.2 Bale Preparation
Bales should be inspected for excessive contamination, moisture, foreign objects, abnormal compression, or damaged packaging. Removing straps, wrapping, and other foreign material before feeding protects the machine and improves product quality.
7.3 Weighing Verification
The electronic scale should be checked according to the factory’s maintenance and calibration procedure. A weighing system that is mechanically sound but not properly verified may still produce inaccurate proportions. Periodic checks should be documented and performed using an appropriate reference method.
7.4 Fiber Flow Observation
Operators should observe the material as it moves through the pre-opening and transfer stages. Uneven flow, bridging, excessive dust, unusual noise, or repeated blockages may indicate a problem with bale condition, machine adjustment, or downstream demand.
7.5 Downstream Feedback
The bale opener should be evaluated through the quality of the web and finished product. If carding becomes unstable, if web weight varies, or if bonding performance changes, the opening and blending stage should be included in the investigation. Process feedback makes it possible to identify problems before large quantities of product are affected.
8. Specification Overview
Item | Specification |
Model | HYKB |
Machine type | Automatic bale opener and fiber blending equipment |
Primary application | Nonwoven fabric production |
Working widths | 1 m, 1.2 m, 1.4 m, 1.6 m, and 2 m |
Stated capacity options | Approximately 200 kg/h and 300 kg/h |
Installed power reference | 3.75 kW |
Raw-material example | PET fiber and other compatible fibers |
Control grade | Automatic |
Voltage | 220 V or customized |
Certification information | CE and ISO9001:2000 listed in product information |
Warranty | One year or 12 months |
Lead time reference | Approximately 2 to 3 months; delivery information also indicates about 60 working days after the required payment arrangement |
Production capacity of supplier | Listed as 100 sets per year |
HS code reference | 84490090 and 8449009000 as listed |
Technical data should be confirmed in the final quotation because capacity, installed power, electrical configuration, and machine arrangement may change according to working width, fiber type, number of units, and integration requirements. The stated 200 kg/h and 300 kg/h values should be treated as reference capacities rather than guaranteed output for every material.
9. Installation, Commissioning, and After-Sales Support
Correct installation is essential for equipment that must connect with conveyors, openers, carding machines, or complete nonwoven lines. The buyer should prepare a level foundation, sufficient working space, suitable electrical service, safe access for operators, and an appropriate route for raw-material movement.
The supplied trade information states that the manufacturer can send two or three workers for installation and commissioning at the buyer’s request. Under the stated arrangement, the buyer provides round-trip air tickets, accommodation, and an allowance of 180 United States dollars per person per day. These commercial conditions should be confirmed before signing the purchase contract.
Commissioning normally includes mechanical inspection, electrical connection, control-system checking, scale verification, conveyor alignment, trial feeding, and coordination with downstream equipment. The commissioning team can also provide operator guidance regarding startup, shutdown, routine cleaning, adjustment, and basic troubleshooting.
The listed warranty period is 12 months. Buyers should request a written warranty statement describing covered components, exclusions, response procedures, spare-parts policy, and the starting date of warranty coverage. Clear documentation helps avoid misunderstandings during long-distance international cooperation.
For overseas customers, after-sales support is especially important. The company has supplied equipment to more than 20 countries, including markets in Latin America, Africa, Asia, and other regions. International supply experience can assist with export packaging, documentation, voltage customization, installation planning, and communication during commissioning.
10. Maintenance and Safe Operation
Routine maintenance helps preserve opening performance, weighing accuracy, and conveyor reliability. Before maintenance begins, the machine should be stopped, isolated from its power supply, and secured against accidental startup. Only trained personnel should work on electrical systems, moving mechanisms, and protective devices.
10.1 Daily Checks
Operators should inspect the working area for accumulated fiber, foreign objects, loose fasteners, abnormal noise, and visible damage. Fiber buildup should be removed using an approved cleaning method. Compressed air should be used cautiously because it may spread dust into bearings, electrical cabinets, or the surrounding workplace.
10.2 Mechanical Inspection
Feeding and opening components should be checked for wear and correct alignment. Conveyor belts, rollers, guards, bearings, and drive elements should be inspected according to the maintenance schedule. Any unusual vibration or sound should be investigated before continued production.
10.3 Scale and Control-System Checks
The weighing system should be kept clean and protected from material accumulation that could affect measurement. Zeroing, calibration checks, sensor condition, cable connections, and control-panel indications should be reviewed regularly.
10.4 Environmental Control
Fiber-processing areas should be managed with appropriate ventilation, housekeeping, and fire-prevention procedures. Depending on the fiber type, the process may produce dust or airborne particles. The factory should evaluate local occupational safety requirements and install suitable dust-control measures where necessary.
11. How to Select the Correct Configuration
A bale opener should be selected according to the complete production objective rather than by capacity alone. A buyer should begin by defining the finished product and then work backward through the process.
Important questions include: What fibers will be used? What is the target blend ratio? What is the required production width? What is the desired output per hour? Will the material be carded, airlaid, needle punched, thermally bonded, or processed through another route? How many fiber types must be handled at the same time? What is the available factory space? What voltage and safety standards apply at the installation site?
Working width should match the downstream web-forming equipment. A 1-meter line may be appropriate for a compact or specialized product, while wider lines may be required for geotextiles, carpets, insulation, or industrial fabrics. The number of bale openers should correspond to the number of materials and the complexity of the recipe.
Capacity should also be evaluated carefully. A nominal capacity may vary according to fiber length, fiber density, moisture, bale compression, feeding rate, blend ratio, and operator settings. Buyers should request a technical confirmation based on their actual raw materials whenever possible.
Future production plans should be considered as well. If the company expects to add new fiber types or increase product variety, a modular configuration may provide more value than a narrowly optimized single-material arrangement.
12. Purchasing Considerations for International Buyers
International buyers should request a complete technical and commercial offer. The offer should identify the exact model, working width, production capacity, installed power, electrical voltage, control configuration, included conveyor sections, number of bale-opening units, spare parts, packaging method, delivery term, warranty, installation conditions, and commissioning scope.
The supplied trade information indicates payment terms of 30 percent deposit by telegraphic transfer and 70 percent before delivery. The stated package may be nude packing or a wooden case, while another specification identifies nude packing or PE film. The final packaging method should be selected according to the transport route, weather exposure, port handling, and destination requirements.
Delivery is listed as approximately 60 working days after the relevant payment arrangement, while another entry refers to a lead time of two to three months. Because customized machines may require engineering, fabrication, assembly, testing, and export preparation, the buyer should obtain a confirmed schedule in the contract.
Documents commonly requested for an international machinery purchase may include the commercial invoice, packing list, certificate of origin where applicable, electrical diagrams, operation manual, spare-parts list, inspection record, and shipping documents. The buyer should confirm which documents are included before production begins.
13. Why the Bale Opener Matters to Overall Product Quality
Nonwoven fabric quality is determined by a chain of connected operations. If the raw material is not opened correctly, the carding machine may receive an unstable feed. If the blend is inaccurate, the web may have inconsistent physical properties. If the material transfer is irregular, production interruptions may increase. The bale opener influences each of these early-stage conditions.
A high-quality bale opener does not replace good process management, but it gives the manufacturer a stronger foundation. Better preparation supports stable production, more consistent web formation, improved recipe repeatability, and more efficient use of downstream equipment.
The advantages become more significant as product specifications become stricter. Technical nonwovens, automotive materials, filtration media, insulation, geotextiles, and industrial felts may be required to meet defined weight, thickness, strength, or performance targets. Accurate preparation helps the manufacturer control one of the most important variables in the production process: the composition and condition of the incoming fiber.
14. Company Manufacturing and Service Strengths
Changshu Hongyi Nonwoven Machinery Co., Ltd. is based in Changshu, Jiangsu Province, China, and specializes in the development and supply of nonwoven machinery. Its product portfolio covers complete production lines as well as standalone machines. This includes bale openers, carding machines, airlay machines, needle punching machines, thermal bonding ovens, ironing machines, winding machines, cutting machines, and auxiliary equipment.
The company’s experience in different nonwoven applications supports practical equipment selection. A bale opener for a geotextile line may require a different configuration from a bale opener for automotive padding, cleaning cloth, or airlaid waste felt. Understanding these differences is important for creating a reliable machine proposal.
The company emphasizes efficiency, reliability, advanced technology, precision engineering, energy-saving possibilities, automatic control, and customization. These strengths are relevant to buyers that need more than a standard catalog machine. They are also important for customers seeking complete line responsibility from one machinery partner.
Export experience is another consideration. Equipment has been supplied to customers in Mexico, Argentina, Brazil, Turkey, Algeria, Egypt, Bangladesh, Vietnam, Thailand, and other countries. International project experience can improve communication regarding factory layout, local power requirements, shipping, installation, training, and long-term cooperation.
15. Frequently Asked Questions
Q1: What is the main function of the bale opener?
The main function is to pre-open compressed fiber bales, control the quantity of material through automatic weighing, and transfer the prepared fiber toward the next stage of the nonwoven production line.
Q2: Can the machine process more than one fiber type?
Yes. Several bale openers can be combined so that different fiber types are handled in one blending operation. The exact number of machines depends on the production recipe and the required material proportions.
Q3: What fibers can be used?
The product information gives PET fiber as an example and describes the machine as suitable for all kinds of fiber subject to proper configuration. Buyers should provide detailed information about fiber length, density, moisture, bale compression, and other characteristics before ordering.
Q4: How does automatic weighing improve production?
Automatic weighing provides a measurable method for controlling the quantity of each fiber. It helps reduce the variation associated with manual estimation and supports more repeatable blending from one batch or production run to another.
Q5: What working widths are available?
The listed working widths are 1 meter, 1.2 meters, 1.4 meters, 1.6 meters, and 2 meters. The appropriate selection depends on the downstream machine width, production target, factory layout, and future expansion plans.
Q6: What is the stated capacity?
The available information lists reference capacities of approximately 200 kg/h and 300 kg/h. Actual output depends on the fiber material, bale condition, working width, operating settings, and complete line configuration. Capacity should be confirmed for the buyer’s actual application.
Q7: Can the bale opener be connected to an existing production line?
It may be possible to integrate the bale opener with existing carding, airlay, needle punching, thermal bonding, or other equipment. The supplier should review the existing machine width, feed height, conveyor direction, control interface, material demand, and factory layout before confirming compatibility.
Q8: Is the equipment customized?
Customized configurations are available. Typical customization areas may include working width, voltage, number of bale openers, conveyor arrangement, control requirements, and connection with other machines. The final design should be based on technical information supplied by the buyer.
Q9: What certification is listed for the machine?
The product information lists CE and ISO9001:2000. Buyers should request confirmation of the certification documents and verify that they apply to the exact machine configuration being purchased.
Q10: What warranty is offered?
The listed warranty is one year or 12 months. The final warranty scope, exclusions, spare-parts responsibilities, and service procedures should be included in the purchase agreement.
Q11: Does the supplier provide installation support?
Yes. The stated after-sales arrangement indicates that two or three workers can be sent to install and commission the line at the buyer’s request. Travel tickets, accommodation, and the specified daily allowance are provided by the buyer under the listed terms.
Q12: What should be prepared before installation?
The buyer should prepare a suitable foundation, electrical supply, factory access, material storage area, safe operating space, lifting equipment if required, and connection points for upstream or downstream machinery. The final foundation and utility requirements should be confirmed from the approved technical drawing.
Q13: Is the bale opener suitable for a complete nonwoven production line?
Yes. It can serve as the raw-material preparation section of a line containing carding, web forming, needle punching, thermal bonding, winding, cutting, and auxiliary equipment. Its exact role depends on the product and process route.
Q14: How should the machine be maintained?
Maintenance includes cleaning, inspection of moving parts and guards, checking conveyor and drive components, verifying the weighing system, inspecting electrical connections, and following the supplier’s lubrication and replacement schedule. Maintenance must be performed safely with the machine isolated from power.
Q15: Why choose an automatic system instead of manual blending?
An automatic system offers better repeatability, reduced manual measurement, improved control of multiple fiber types, and easier integration with continuous production. Manual methods may still be useful for small or experimental operations, but automatic equipment is generally more suitable for consistent industrial output.
16. Conclusion
The bale opener is a critical foundation for stable nonwoven fabric production. By loosening compressed fiber, controlling material input, weighing predetermined quantities, and transferring the blend through a cross conveyor, the HYKB Bale Opener addresses several common challenges in raw-material preparation.
Its principal advantages include automatic weighing, compatibility with different fiber types, support for multi-fiber recipes, multiple working widths, modular expansion, and integration with complete nonwoven production lines. These features make it suitable for geotextiles, carpets, automotive interiors, cleaning cloths, felts, insulation, thermal bonded wadding, and other nonwoven products.
The equipment is supported by the manufacturing and engineering experience of Changshu Hongyi Nonwoven Machinery Co., Ltd., a specialist supplier with more than 20 years of experience in nonwoven machinery. The company’s ability to provide both individual machines and complete production lines allows customers to develop solutions around their material, capacity, product, and factory requirements.
For buyers comparing bale-opening systems, the most important evaluation points are not only the machine’s nominal capacity. They should also consider weighing accuracy, blend flexibility, working width, downstream compatibility, control-system design, factory testing, installation support, spare parts, warranty terms, and the supplier’s ability to provide long-term technical service. When these factors are addressed together, an automatic bale opener can improve production consistency and create a stronger foundation for efficient, high-quality nonwoven manufacturing.
References
1. Product information supplied for the HYKB Bale Opener, including machine structure, working widths, capacity references, automatic weighing, and application data.
2. Technical and commercial information supplied for Changshu Hongyi Nonwoven Machinery Co., Ltd., including manufacturing experience, product range, certification references, warranty, installation, and export service.
3. General principles of fiber opening, blending, carding, web formation, needle punching, and thermal bonding in nonwoven textile production.
4. General industrial practices for automatic weighing, raw-material traceability, machinery commissioning, preventive maintenance, and nonwoven process control.