

Content
- 1 Purpose of a Thermal Bonded Nonwoven Oven
- 2 Working Principle of the HYHX Nonwoven Fabric Oven
- 3 Main Structural Configuration
- 4 Key Technical Specifications
- 5 Advantages for Nonwoven Manufacturers
- 6 Comparison with Other Bonding Methods
- 7 Manufacturing Strengths of the Equipment Supplier
- 8 Applications of Thermal-Bonded Wadding
- 9 Installation and Production Considerations
- 10 Maintenance and Operational Reliability
- 11 Quality Control of Finished Material
- 12 Why Choose a Customized Oven Solution
- 13 Frequently Asked Questions
- 13.1 What is the main function of the HYHX Nonwoven Fabric Oven?
- 13.2 What raw materials can be processed?
- 13.3 What is the maximum working width?
- 13.4 What product thickness can the oven handle?
- 13.5 What product weights are supported?
- 13.6 What heating methods are available?
- 13.7 Can the machine be customized?
- 13.8 What are the benefits of a double-belt structure?
- 13.9 How does inverter control help production?
- 13.10 Why is automatic belt correction important?
- 13.11 What certifications are listed for the machine?
- 13.12 What after-sales support is provided?
- 13.13 Can the oven be integrated into a complete production line?
- 13.14 What information should be provided when requesting a quotation?
- 14 Conclusion
- 15 References
- 16 Product: HYHX Nonwoven Fabric Oven
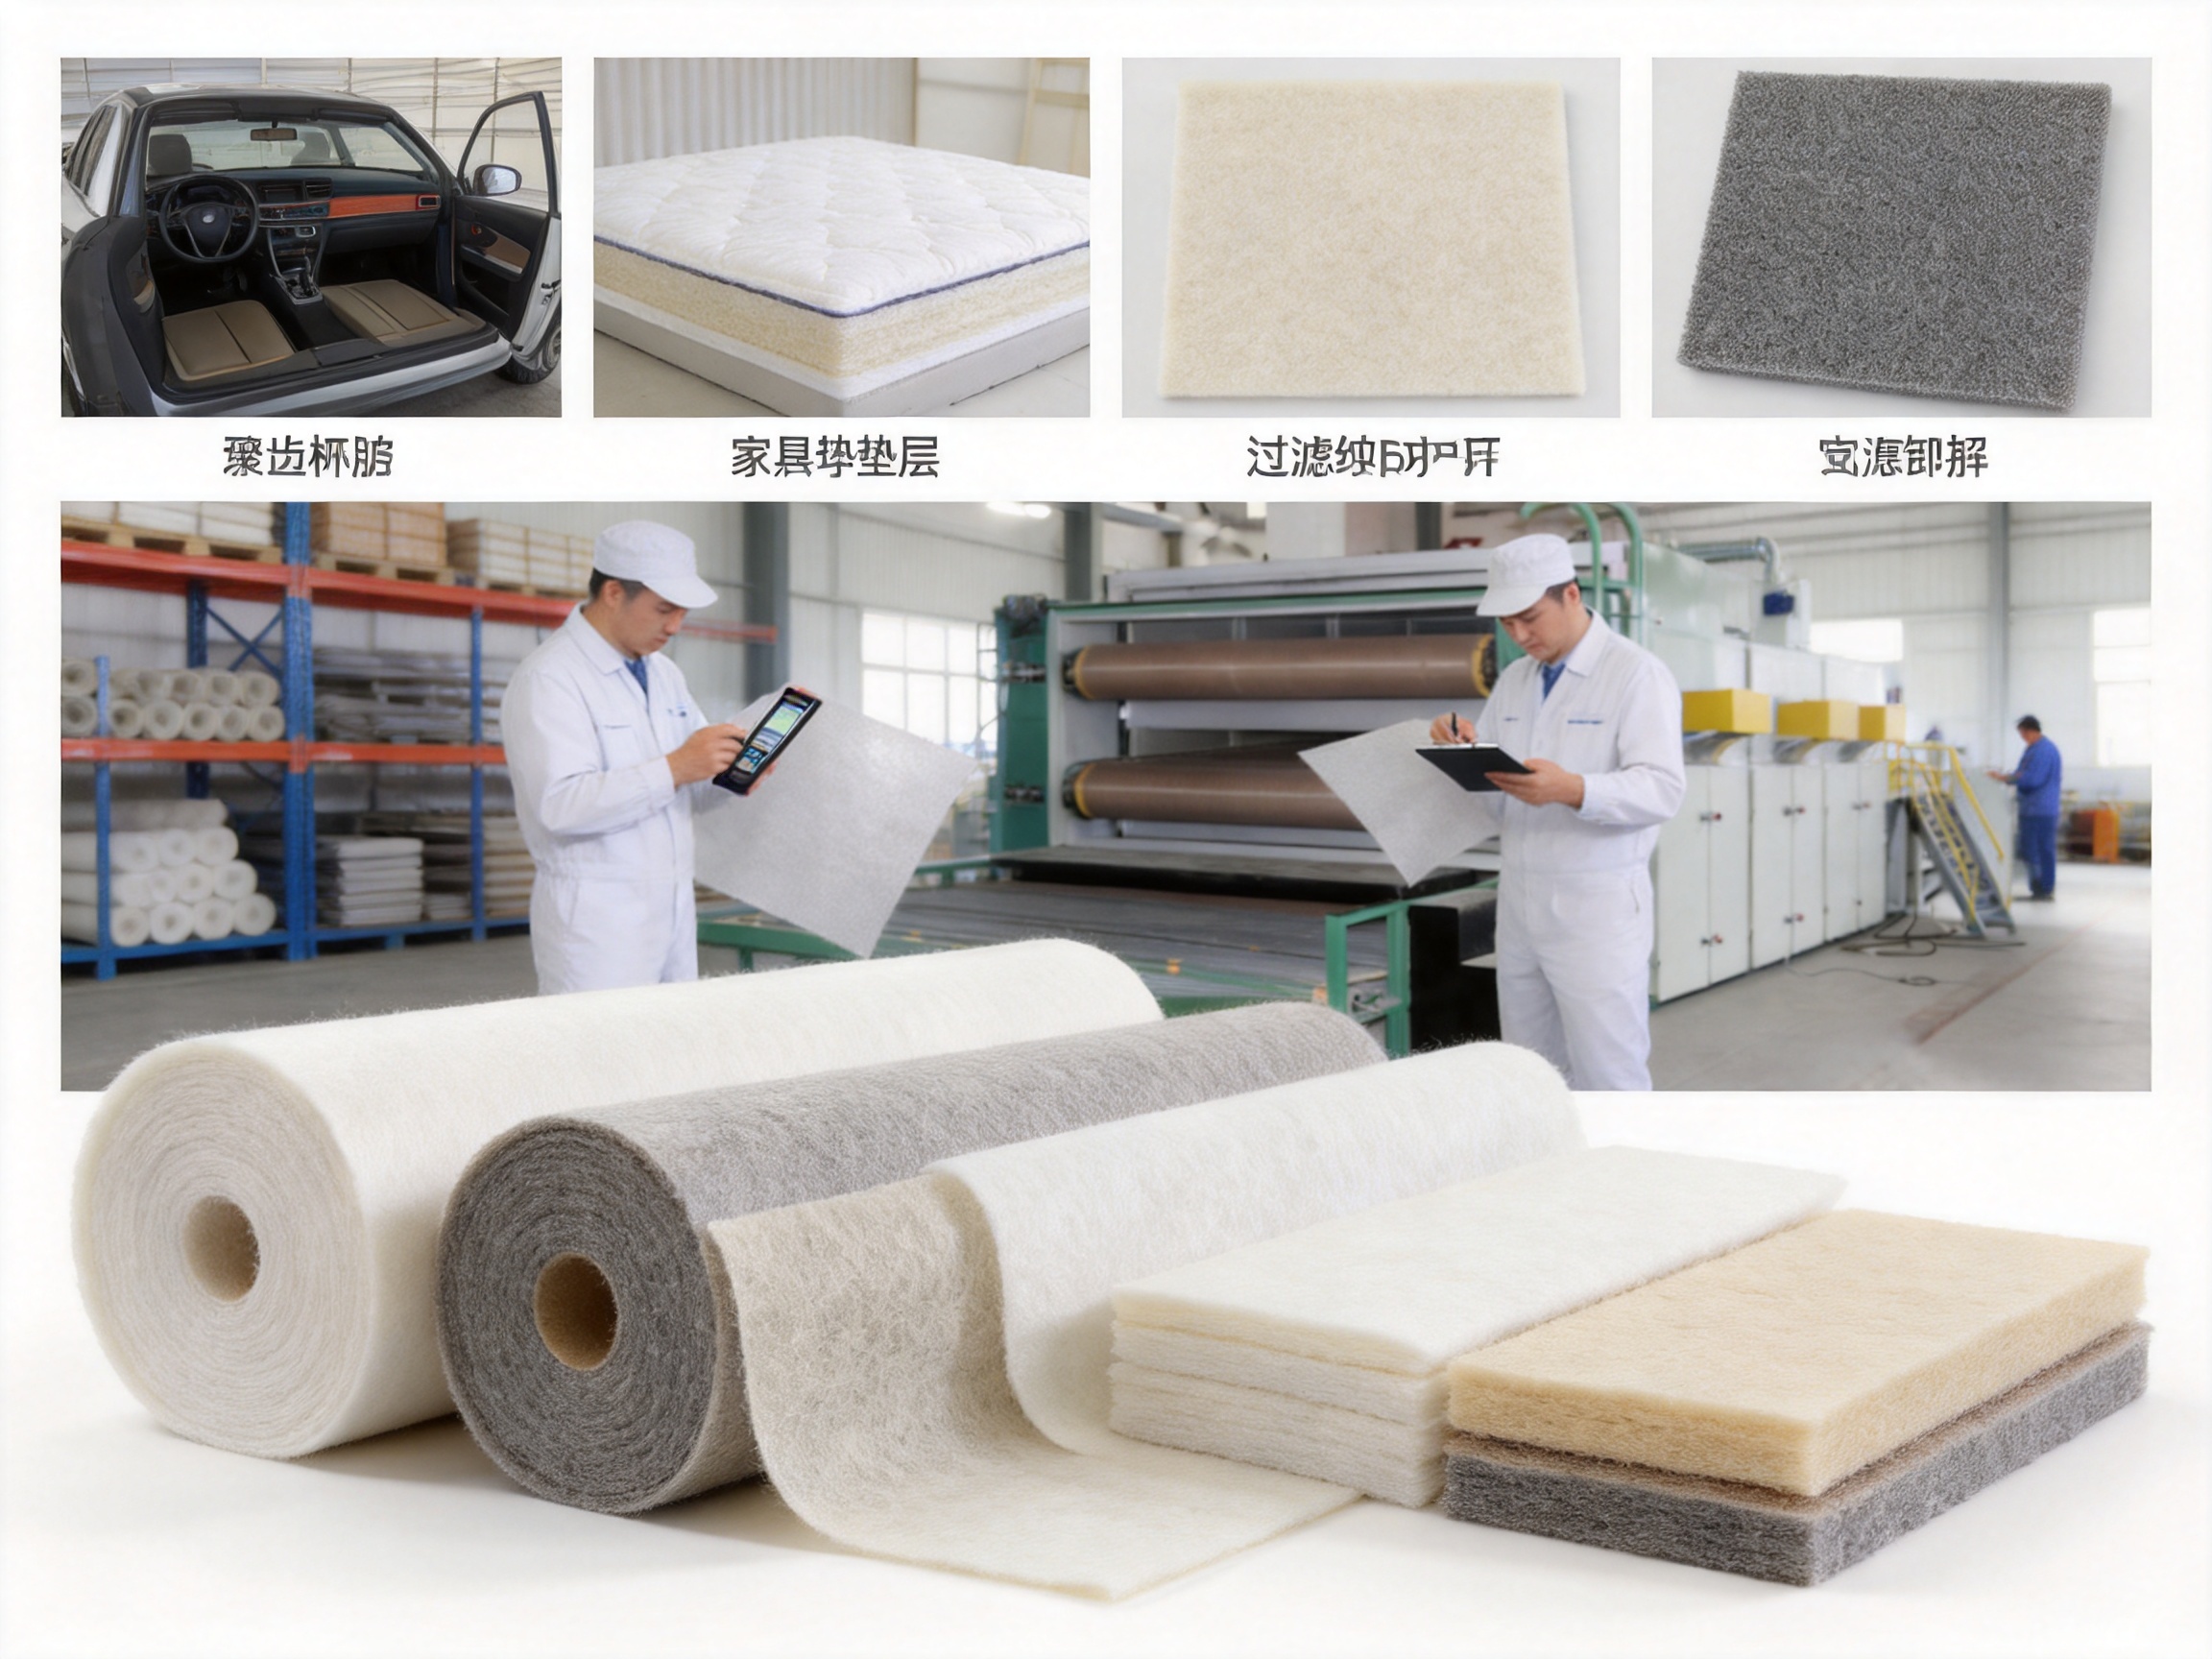
Thermal bonding is one of the most important methods for manufacturing thick, stable, and durable nonwoven materials. In this process, a carefully prepared fiber web passes through a controlled heating zone where low-melt fibers soften, flow, and bond neighboring fibers together. The result is a consolidated wadding or batt with improved strength, thickness retention, dimensional stability, and surface integrity. The quality of the oven used for this stage directly influences the appearance, density, bonding uniformity, productivity, energy consumption, and final performance of the nonwoven fabric.
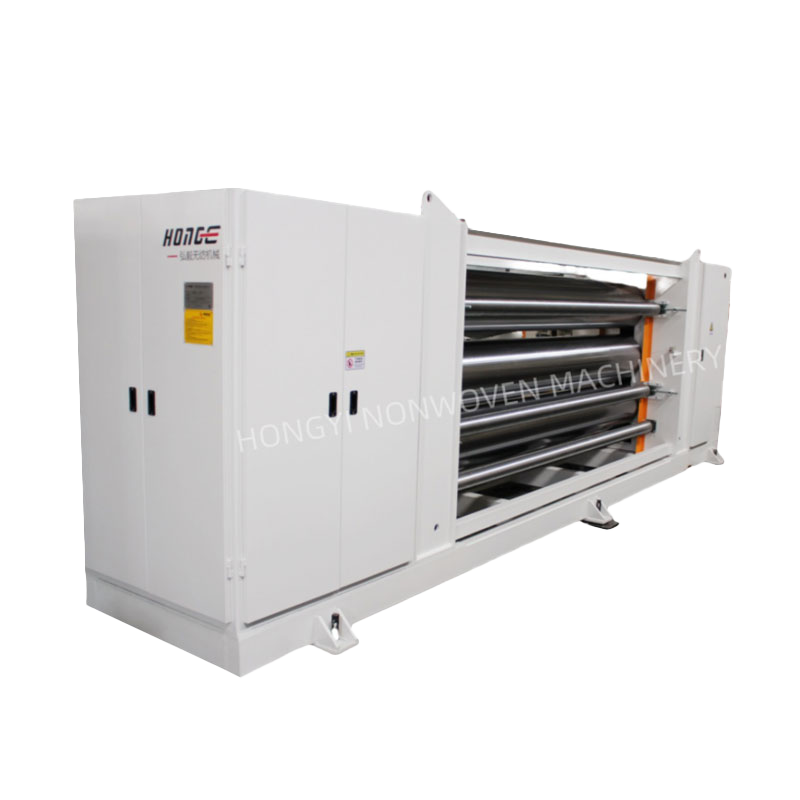
The HYHX Nonwoven Fabric Oven is designed for hot-air penetration and thermal bonding of fiber webs supplied by a cross lapper or other web-forming equipment. It is suitable for applications that require a hard, thick, and reinforced thermal-bonded wadding. The machine uses heated air to transfer thermal energy throughout the web, allowing the low-melt component to combine with polyester fiber, polypropylene staple fiber, or other compatible raw materials.
With a working width of up to 5,000 millimeters, configurable 6-meter, 8-meter, and 10-meter specifications, automatic operation, inverter-controlled drives and fans, and a maximum heat-setting temperature of 220°C, the oven can be adapted to a broad range of production requirements. Its single-layer, single-belt, or double-belt configuration provides flexibility for different material thicknesses, weights, and forming conditions.
Manufactured by Changshu Hongyi Nonwoven Machinery Co., Ltd., the equipment is supported by more than 20 years of experience in nonwoven machinery. The company provides both individual machines and complete production lines for needle-punched, thermal-bonded, airlaid, automotive, geotextile, carpet, cleaning cloth, felt, and other nonwoven applications.
Purpose of a Thermal Bonded Nonwoven Oven
A thermal bonded nonwoven oven is used to consolidate a loose fiber web without relying exclusively on mechanical needling, chemical binders, or woven structures. The web typically contains a blend of high-melt fibers and low-melt fibers. When the material enters the heating zone, the low-melt component reaches its softening or melting range while the main structural fibers remain sufficiently stable.
Hot air is circulated through the web to provide even heating. Once the low-melt fibers soften, they form bonding points around the other fibers. A controlled cooling stage then stabilizes the structure and helps the newly formed bonds retain their shape. This produces a coherent nonwoven material that can be wound, cut, laminated, shaped, or processed in subsequent operations.
The oven is especially suitable for producing thermal-bonding wadding that requires a relatively high thickness and a firm structure. Depending on the fiber blend and operating parameters, the finished product may be used in automotive interiors, furniture padding, mattress components, insulation layers, filtration materials, protective products, sound-absorbing materials, and industrial textiles.
Compared with a loosely formed batt, the thermally bonded product has improved handling properties. It is less likely to separate during transport, cutting, lamination, or assembly. The bonding method can also provide a clean production route because it reduces or eliminates the need for liquid chemical adhesives in many applications.
Working Principle of the HYHX Nonwoven Fabric Oven
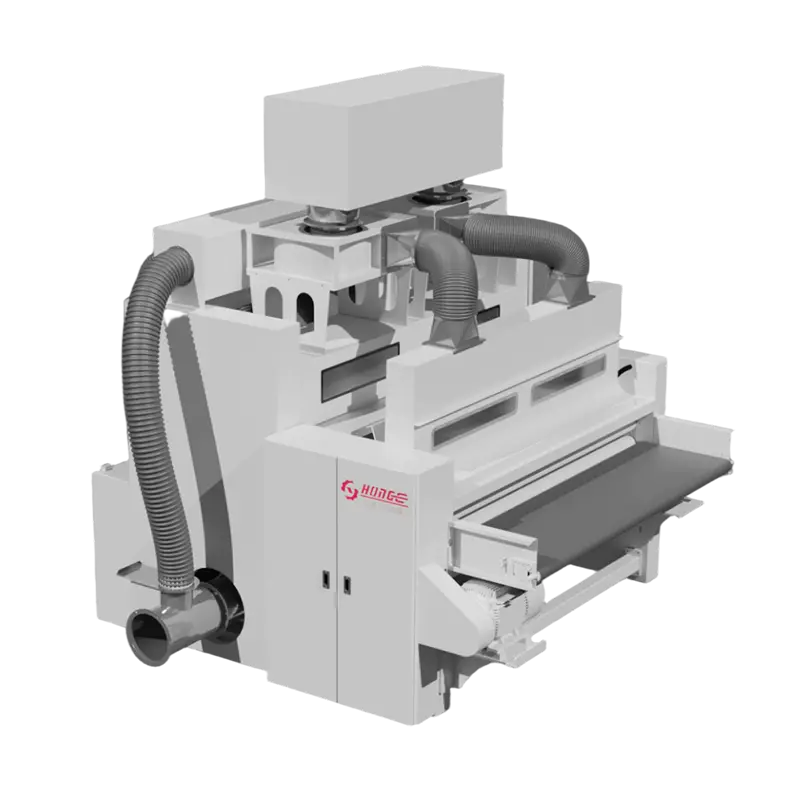
The production process begins when a cross lapper or similar web-forming machine creates a fiber batt. The batt is arranged into overlapping layers to achieve the required width, weight, and thickness. It is then transferred into the oven by a continuous belt system.
At the entrance, the upper and lower belts help guide and hold the web. This controlled movement prevents excessive disturbance of the fiber arrangement and supports stable transport through the heating zone. In a double-belt configuration, the belts can help control the material thickness while maintaining contact with the web during heating and cooling.
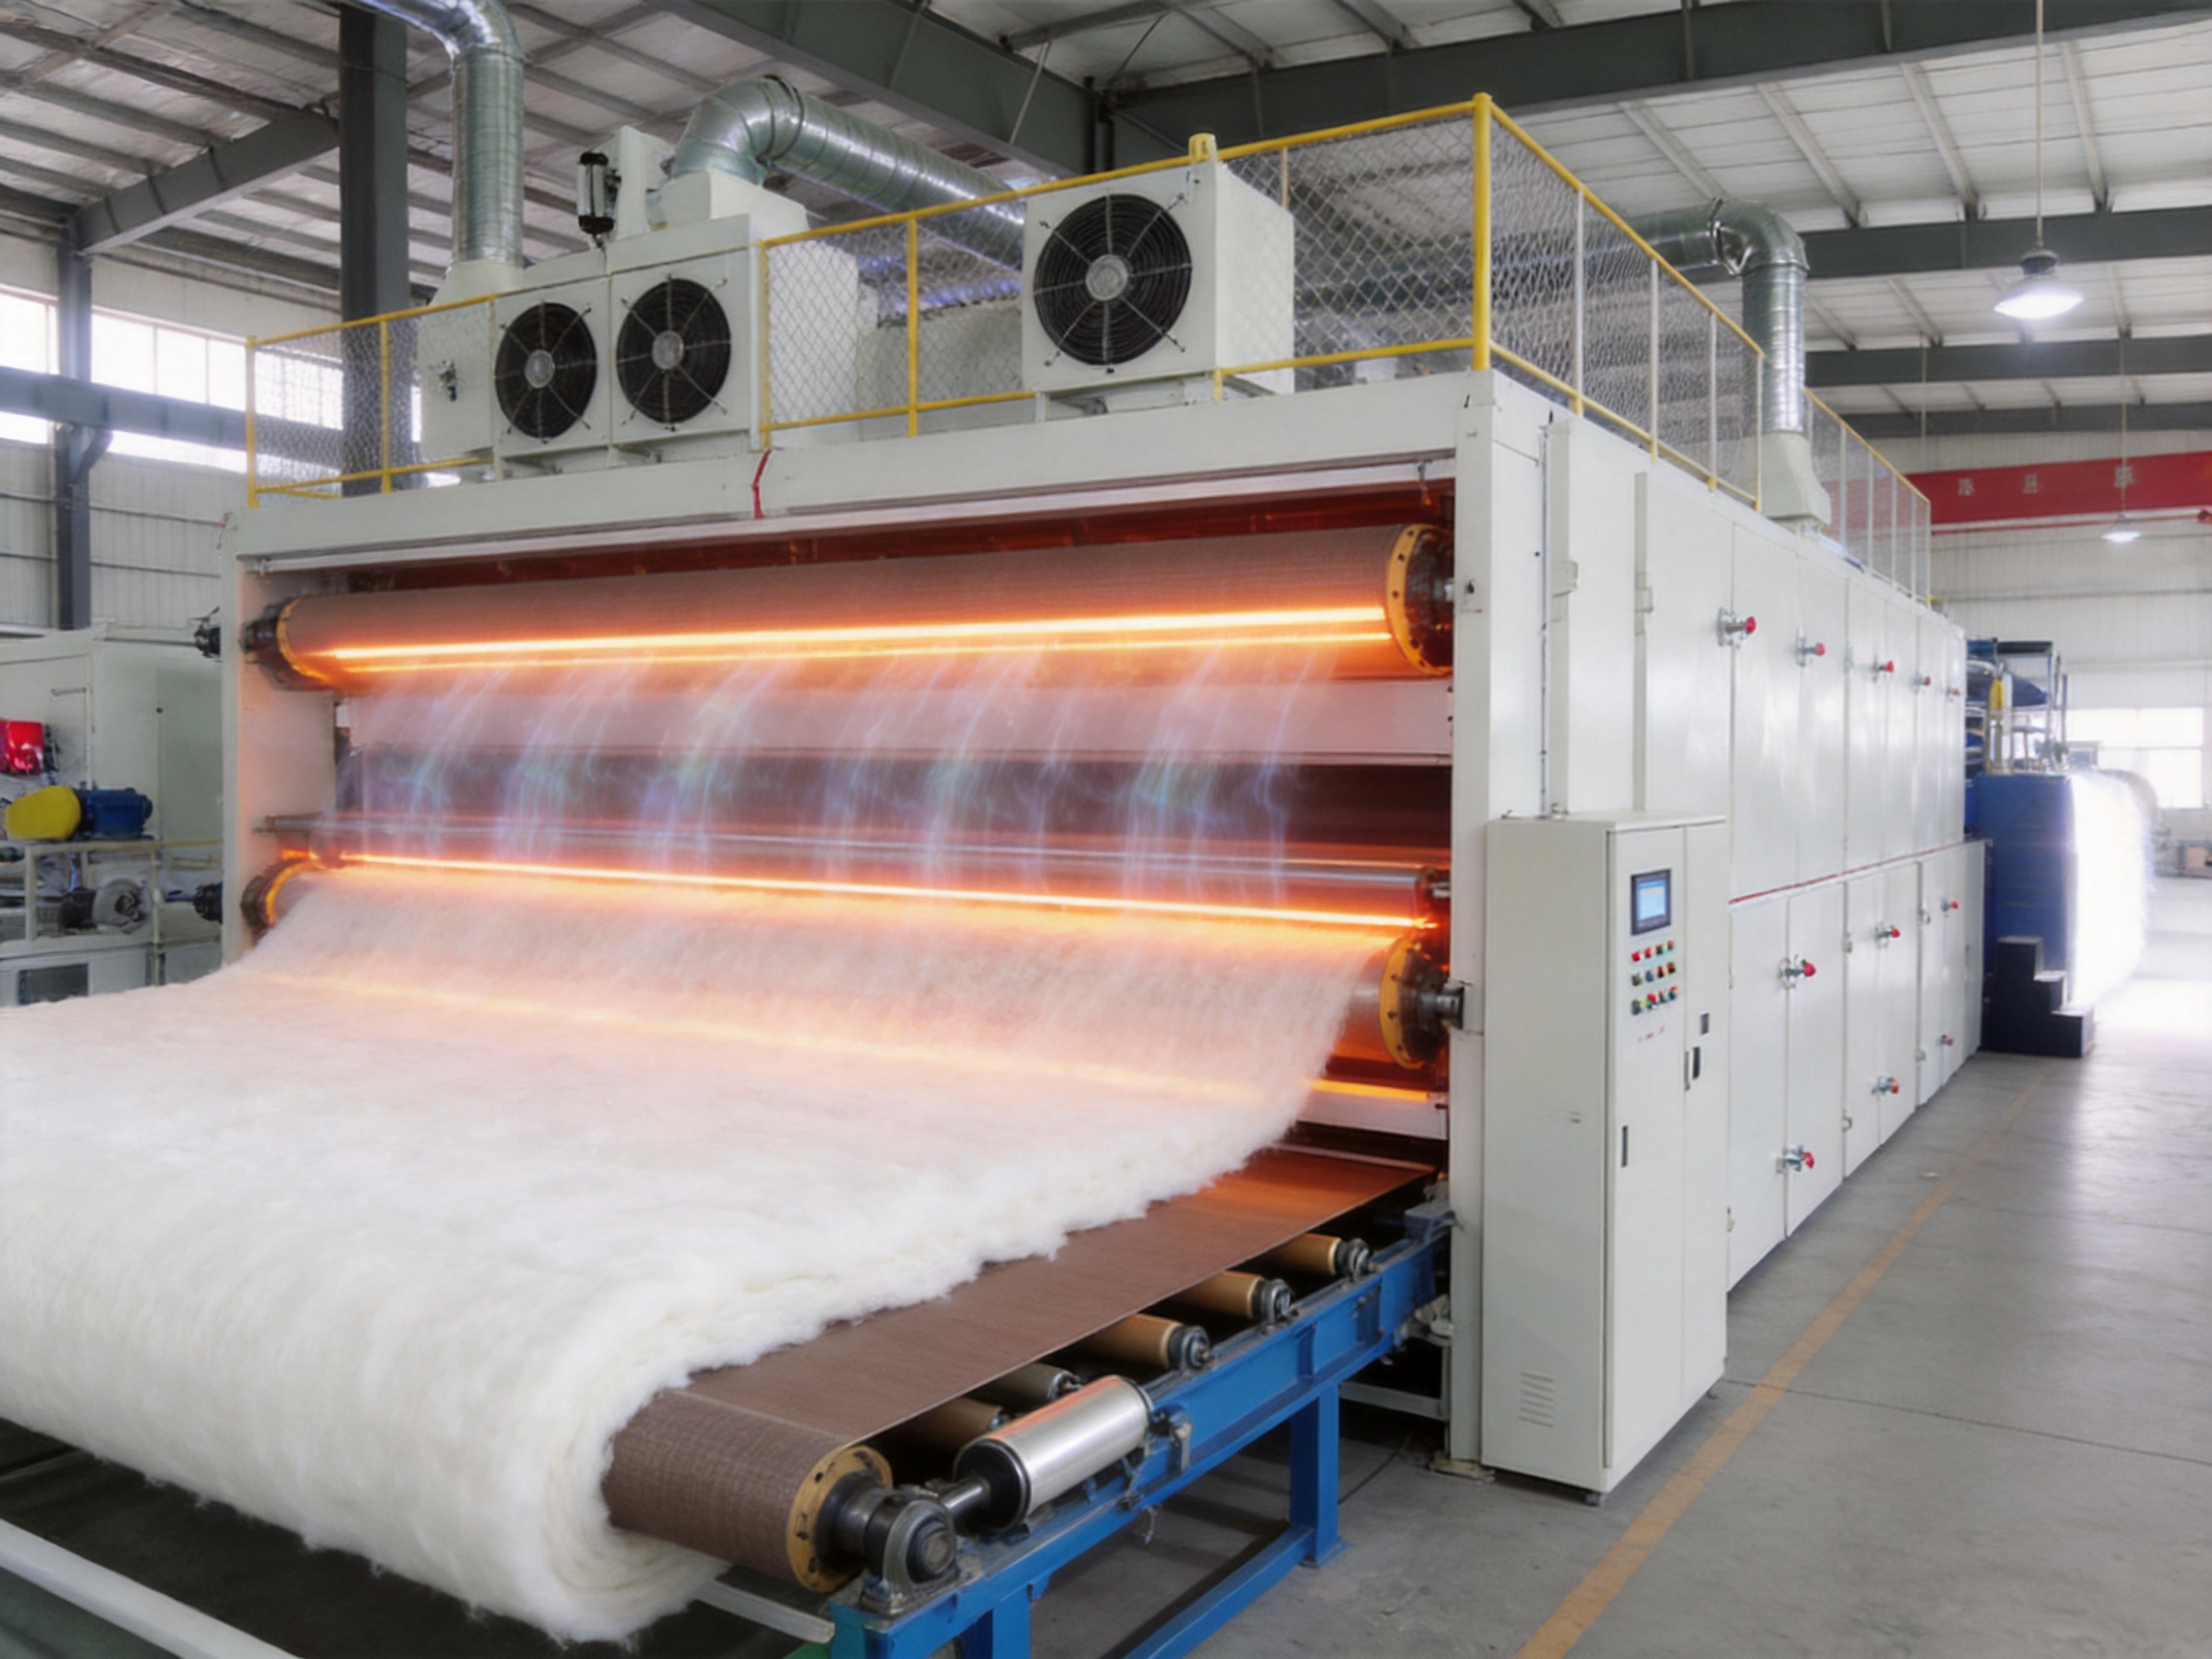
Inside the oven, circulating hot air passes through the fiber structure. Heat transfer is not limited to the surface. Proper air penetration allows thermal energy to reach the interior of the batt, which is essential for obtaining consistent bonding through the full thickness of a heavy or thick product.
The heating temperature, air circulation, line speed, and material compression must be matched to the fiber type and product specification. Polyester and polypropylene staple fibers may require different processing conditions, while blends containing low-melt fibers need a controlled thermal profile to achieve sufficient bonding without damaging the main fibers.
After thermal bonding, the material passes through a cooling or stabilization section. Cooling is important because it helps the softened bonding component solidify in the desired configuration. It also reduces the risk of deformation, excessive shrinkage, or uneven thickness after the material leaves the machine.
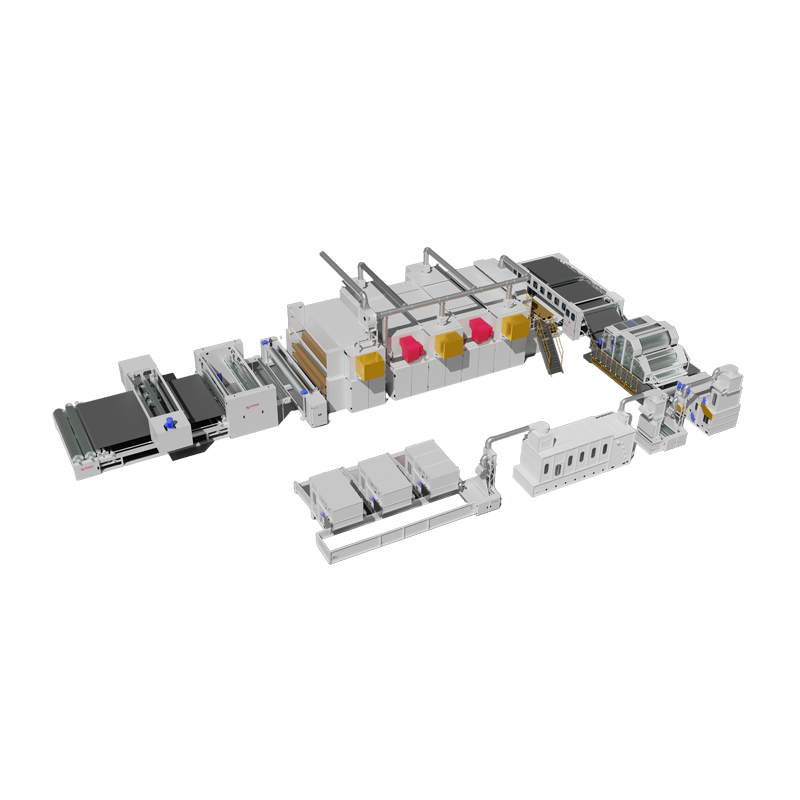
The finished web exits as a consolidated wadding that can be transferred to a winding machine, cutting machine, laminating unit, or other downstream equipment. The complete line configuration can be customized according to the product width, basis weight, thickness, fiber composition, and production capacity required by the customer.
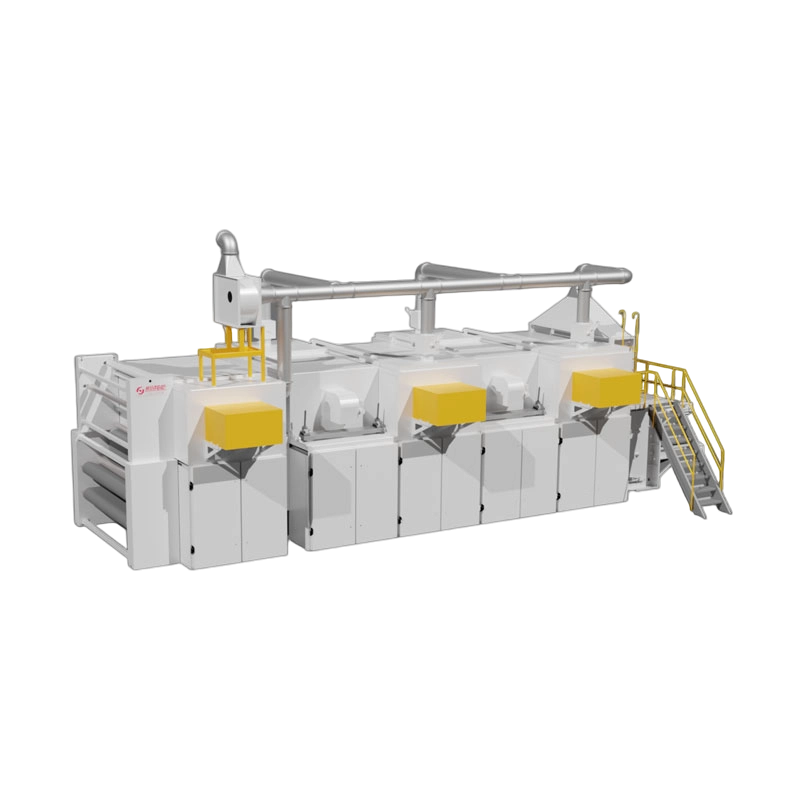
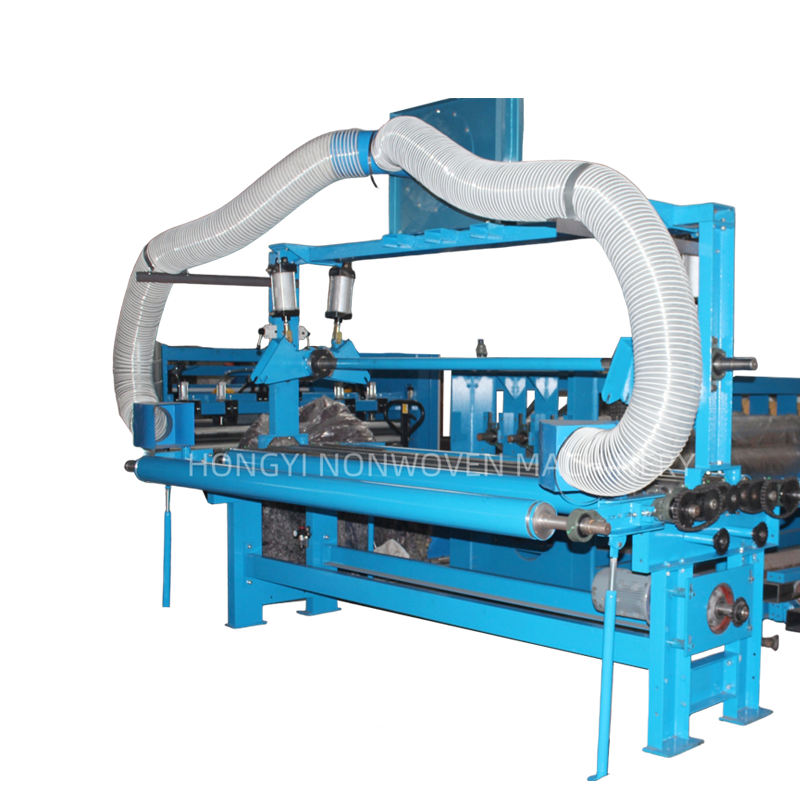
HYHX Nonwoven Fabric Oven
Main Structural Configuration
Single-Layer Construction
The single-layer configuration is suitable for applications where the product structure and thickness can be controlled by the web-forming process and the transport belts. It provides a relatively direct material path and can be selected for products with moderate thickness or straightforward thermal-bonding requirements.
This arrangement can be advantageous when the production line must remain compact or when the customer prefers a simpler machine layout. The exact configuration depends on the material specification, target output, and required level of thickness control.
Single-Belt and Double-Belt Options
The machine may be supplied with a single-belt or double-belt structure. A single-belt design can provide efficient transport through the heating and cooling sections while allowing the web to expand or consolidate according to the process requirements.
A double-belt design places the web between upper and lower belts. This helps stabilize the material as it moves through the oven and can provide improved control over thickness, surface formation, and dimensional consistency. It is particularly useful when the product must maintain a defined thickness or when the web is relatively thick and needs support on both sides.
The choice between single-belt and double-belt construction should be made after evaluating the raw material, basis weight, final thickness, bonding temperature, line speed, and required surface appearance. Changshu Hongyi Nonwoven Machinery Co., Ltd. can configure the equipment according to the customer’s production plan rather than forcing every application into one standard design.
Upper and Lower Web-Holding Belts
The upper and lower belts guide the web into the heating area and help maintain a stable material path. This is important because thermal bonding is sensitive to changes in web position, compression, and residence time.
Stable belt transport reduces the possibility of wrinkles, lateral movement, uneven compression, and localized overheating. It also makes it easier for operators to maintain consistent quality when the production line is running continuously.
High-Temperature-Resistant Belts
The oven is equipped with belts designed for operation in a high-temperature environment. The belt material and construction must withstand repeated heating and cooling cycles, continuous movement, tension, and contact with the fiber web.
A high-temperature-resistant belt supports reliable production and helps reduce unplanned stoppages caused by premature belt damage. Its service life also depends on correct tension, alignment, cleaning, operating temperature, and maintenance practices.
Automatic Belt Correction
Automatic belt correction helps maintain the belt in the correct lateral position during operation. Belt deviation can result from uneven tension, material loading, thermal expansion, contamination, or mechanical misalignment. If it is not corrected, it may cause edge damage, unstable web transport, or excessive wear.
The automatic correction device provides an important advantage for continuous production. It reduces the need for frequent manual adjustments and helps protect both the belt and the material. It also supports more reliable operation when the machine is working at a high production width.
Inverter-Controlled Main Drive and Fans
The main drive and fans use inverter control. This enables the operator to adjust transport speed and air circulation according to the characteristics of the product. Different fiber blends and material weights require different residence times and heat-transfer conditions.
Inverter control allows smoother starting and stopping than fixed-speed operation. It can reduce mechanical stress, improve process adjustment, and support energy management. Fan speed can be matched more closely to the actual production requirement, helping avoid unnecessary air circulation and power consumption.
Key Technical Specifications
The HYHX Nonwoven Fabric Oven is available in a range of configurations. The following table summarizes the principal specifications supplied for the product.
| Item | Specification |
|---|---|
| Model | HYHX |
| Equipment type | Thermal bonded and heat-setting oven |
| Operating mode | Automatic |
| Working width | Up to 5,000 mm |
| Product thickness | 3–200 mm |
| Product weight | 60–1,500 GSM |
| Maximum heat-setting temperature | Up to 220°C |
| Typical specifications | 6 m, 8 m, and 10 m |
| Raw materials | Polyester fiber or PP staple fiber |
| Heating methods | Hot-oil circulation or electric heating |
| Configuration | Customized according to customer requirements |
| Certification | CE and ISO9001:2000 |
| After-sales service | One-year warranty |
| Production capacity | Up to 100 sets per year |
Actual production performance depends on the selected fiber composition, low-melt fiber percentage, basis weight, target thickness, moisture content, heating method, line speed, and final bonding requirements. Technical parameters should therefore be confirmed during the engineering and quotation stage.
Advantages for Nonwoven Manufacturers
Uniform Hot-Air Penetration
One of the primary advantages of the oven is its hot-air penetration method. In thick webs, heating only the surface is not sufficient. The inside of the web must receive enough thermal energy for the low-melt fiber to bond throughout the structure.
Controlled air circulation promotes more consistent heating across the working width and through the product thickness. This helps reduce differences between the surface and center of the web, which can otherwise lead to weak internal bonding, variable compression recovery, or inconsistent product performance.
Wide Product Range
The specified product range covers approximately 60 to 1,500 GSM and thicknesses from 3 to 200 millimeters. This allows the equipment to serve both relatively light thermal-bonded materials and heavy, thick waddings.
Such flexibility is useful for manufacturers that produce several products on one line. Instead of investing in separate machines for every basis weight, a configurable oven can support a broader product portfolio when the correct belts, heating zones, forming equipment, and operating parameters are selected.
Large Working Width
A working width of up to 5,000 millimeters supports wide-format production. Wider equipment can improve output per operating hour and reduce the number of longitudinal joints or narrow strips required in downstream applications.
Large-width equipment must be designed carefully because belt alignment, air distribution, heating balance, and mechanical rigidity become more demanding as the machine becomes wider. The oven’s automatic belt correction and configurable structure are important features for maintaining stable operation across a broad working width.
Adaptability to Different Heating Sources
The heating system can be configured for hot-oil circulation or electric heating. This gives customers the opportunity to select a heating method based on plant utilities, energy availability, production scale, environmental conditions, and operating preferences.
Hot-oil circulation may be suitable for plants that already have a thermal-oil system or require a stable heat source for continuous operation. Electric heating can be convenient where electrical power is readily available and a compact heating arrangement is preferred. The final choice should be evaluated through a complete energy and installation assessment.
Improved Thickness Control
For thick waddings and thermal-bonded materials, maintaining a consistent thickness is a major quality objective. Variations can affect weight, softness, compression behavior, insulation properties, and downstream assembly.
The belt arrangement helps guide and support the web through the heating and cooling process. A double-belt structure can provide additional control where the product must retain a more defined thickness. Stable transport, consistent air circulation, and appropriate web formation work together to improve thickness uniformity.
Reduced Dependence on Chemical Binders
Thermal bonding uses the melting behavior of low-melt fibers instead of depending primarily on liquid adhesives. This can simplify the production process and may help manufacturers develop products with specific chemical, odor, recycling, or handling requirements.
The suitability of thermal bonding depends on the application and fiber selection. However, when a compatible low-melt fiber is incorporated into the web, the oven provides a direct method for forming bonds without applying a separate wet binder system.
Efficient Process Adjustment
Inverter-controlled drives and fans enable adjustment of line speed and air circulation. This is important when changing from a light web to a heavy web, from a thin product to a thick product, or from one fiber blend to another.
More precise adjustment can help manufacturers reduce trial-and-error operation. It also makes it easier to establish repeatable production recipes for different product grades. A consistent recipe may include belt speed, heating temperature, fan frequency, cooling conditions, and material feed rate.
Customized Engineering
The equipment configuration can be customized according to customer needs. Customization may involve working width, oven length, belt arrangement, heating method, cooling design, control system, product thickness range, and integration with upstream or downstream equipment.
Customized engineering is especially valuable for manufacturers with specialized products. A producer of automotive insulation may need different conditions from a producer of furniture wadding or industrial filter media. A properly engineered line can be matched to the actual production objective rather than based only on general catalog specifications.
Comparison with Other Bonding Methods
Nonwoven webs can be consolidated through mechanical, chemical, thermal, or combined processes. Each method has advantages, and the best choice depends on the required strength, softness, thickness, surface appearance, chemical resistance, cost, and production capacity.
Thermal Bonding Compared with Needle Punching
Needle punching consolidates a web by repeatedly entangling fibers with barbed needles. It is widely used for geotextiles, carpets, felts, automotive materials, and cleaning cloths. Thermal bonding, by contrast, uses heat and low-melt fibers to create bonding points.
Thermal bonding can provide a clean and relatively uniform structure, especially when a firm thick wadding is needed. It does not require needle penetration through the web, which may be beneficial for certain delicate or highly compressible materials. Needle punching may remain preferable where mechanical fiber entanglement, high tear resistance, or a specific felt appearance is required.
Thermal Bonding Compared with Chemical Bonding
Chemical bonding applies a binder to the web and then dries or cures the material. This method can be suitable for certain lightweight webs and specialty products. However, it requires binder preparation, application, drying, and process control.
A thermal bonding oven can reduce the need for wet chemical handling when the fiber blend is designed for thermal consolidation. This may simplify material storage and reduce process stages. It can also help manufacturers produce a dry-formed product with controlled thermal bonding characteristics.
Thermal Bonding Compared with Direct Compression
Compression alone may shape a web temporarily, but without sufficient bonding, the structure can recover, separate, or lose thickness after handling. The HYHX oven combines heat, air penetration, controlled transport, and cooling to create a more stable bonded structure.
The result is not merely compressed fiber. It is a web in which low-melt fibers have formed bonds with neighboring fibers. This distinction is important for products that must retain their structure during cutting, assembly, storage, and service.
Manufacturing Strengths of the Equipment Supplier
Changshu Hongyi Nonwoven Machinery Co., Ltd. is a professional nonwoven machinery manufacturer and trader based in China. The company has more than 20 years of experience in the nonwoven machinery field and supplies both complete lines and individual processing units.
This background is relevant to the design of a thermal-bonded oven because the oven does not operate independently. Its performance depends on the cross lapper, carding machine, fiber preparation system, cooling section, winding equipment, cutting equipment, and control system connected to it. Experience across several parts of the nonwoven process helps the manufacturer understand how each unit affects final product quality.
Experience with Complete Production Lines
The company provides complete nonwoven production lines for needle-punched geotextiles, carpets, airlaid waste felt, automotive interior materials, cleaning cloths, wool felt, jute felt, and other applications. It also supplies carding machines, needle-punching machines, airlaid machines, ironing machines, thermal-bonding ovens, and auxiliary equipment.
This broad product range supports more integrated project planning. A customer can evaluate the oven as part of a complete manufacturing system rather than as an isolated heating chamber. This is useful when the customer needs assistance with line matching, material flow, production layout, control integration, or future expansion.
Engineering and Customization
Nonwoven production lines vary substantially according to raw material, product density, width, thickness, speed, and finishing requirements. Standard equipment may not be sufficient for every application. The supplier’s customization capability allows the design to be adapted to customer-specific conditions.
Engineering work may include determining the heating zone length, selecting the appropriate belt system, configuring the hot-air circulation arrangement, matching the oven to the cross lapper, and reserving suitable connections for winding or cutting equipment.
Customization must be based on actual production data. Important information includes fiber type, denier, low-melt fiber ratio, web weight, target thickness, desired output, available power, available heating medium, factory dimensions, and expected operating schedule.
Quality and Process Control
The equipment is identified as CE certified and manufactured under an ISO9001:2000-certified quality framework. These certifications indicate that the supplier has established documented approaches to product quality and equipment compliance. Customers should still confirm the exact certification scope, supplied documentation, and applicable installation requirements for their destination country.
Manufacturing quality in a thermal oven depends on more than the heating elements. The frame must maintain rigidity, the belt system must run smoothly, the air ducts must be properly arranged, the fan system must be balanced, and the control components must be integrated correctly. Attention to these details helps reduce operating instability and maintenance problems.
International Supply Capability
The company has supplied products to more than 20 countries, including markets in Latin America, the Middle East, Africa, Southeast Asia, and other regions. International project experience can be useful when equipment must be prepared for overseas transport, local electrical standards, different plant conditions, and remote technical communication.
The equipment may be delivered with nude packing or PE film packaging, depending on the shipping plan and customer requirements. Transport arrangements should be confirmed according to machine dimensions, export regulations, container availability, and site access conditions.
After-Sales Support
The product information specifies a one-year warranty. A practical after-sales program should cover installation guidance, commissioning support, operating instructions, maintenance recommendations, troubleshooting assistance, and the availability of replacement parts.
Customers should discuss the scope of technical support before ordering. Topics may include whether installation is supervised, which utilities must be prepared by the buyer, how operators are trained, what spare parts are recommended, and how warranty claims are handled.
Applications of Thermal-Bonded Wadding
Automotive Interior Materials
Thermal-bonded nonwoven materials are used in automotive interior applications such as acoustic layers, trunk liners, door components, roof materials, seat-related structures, and insulation products. These applications may require a combination of low weight, thickness stability, sound absorption, thermal insulation, and formability.
The oven can be configured to produce a wide range of weights and thicknesses for automotive material development. The correct fiber blend and bonding level must be selected according to the required flame performance, odor requirements, compression behavior, and forming process.
Furniture and Mattress Components
Thick bonded waddings are widely used in furniture padding, mattress layers, cushion materials, and upholstery products. The material may need to provide resilience, bulk, softness, structural support, and resistance to handling damage.
Thermal bonding can stabilize the batt while preserving a relatively open structure. Production settings can be adjusted to balance firmness and recovery. The final result depends on the raw material, bonding temperature, web density, cooling conditions, and any later lamination or quilting process.
Insulation and Sound-Absorbing Products
Nonwoven fiber structures can trap air and reduce the transmission of heat or sound. Thermal-bonded materials are used in building insulation, equipment insulation, acoustic panels, duct components, and other products where a controlled thickness and stable shape are necessary.
For these applications, consistent density and thickness are important. Excessive bonding may close the structure and reduce the desired air volume, while insufficient bonding may cause deformation or fiber migration. The oven must therefore be operated according to the performance target of the finished product.
Filtration Media
Some filtration products use thermally bonded fiber webs as support layers, prefilters, or depth-filtration materials. The web structure can be designed to provide a balance of permeability, strength, dust-holding capacity, and dimensional stability.
When the oven is used for filtration applications, air distribution and product cleanliness become particularly important. The production environment, raw material quality, belt condition, and cooling design should be managed to avoid contamination and uncontrolled fiber release.
Protective and Industrial Materials
Thermal-bonded waddings may also be used in protective packaging, industrial pads, agricultural materials, construction products, and specialty composite substrates. The broad weight and thickness range allows manufacturers to explore different products on the same basic platform.
Further processing may include hot pressing, laminating, coating, die cutting, slitting, sewing, or molding. The oven’s output should be designed with the downstream process in mind so that the bonded web has the required surface, flexibility, and dimensional stability.
Installation and Production Considerations
Factory Layout
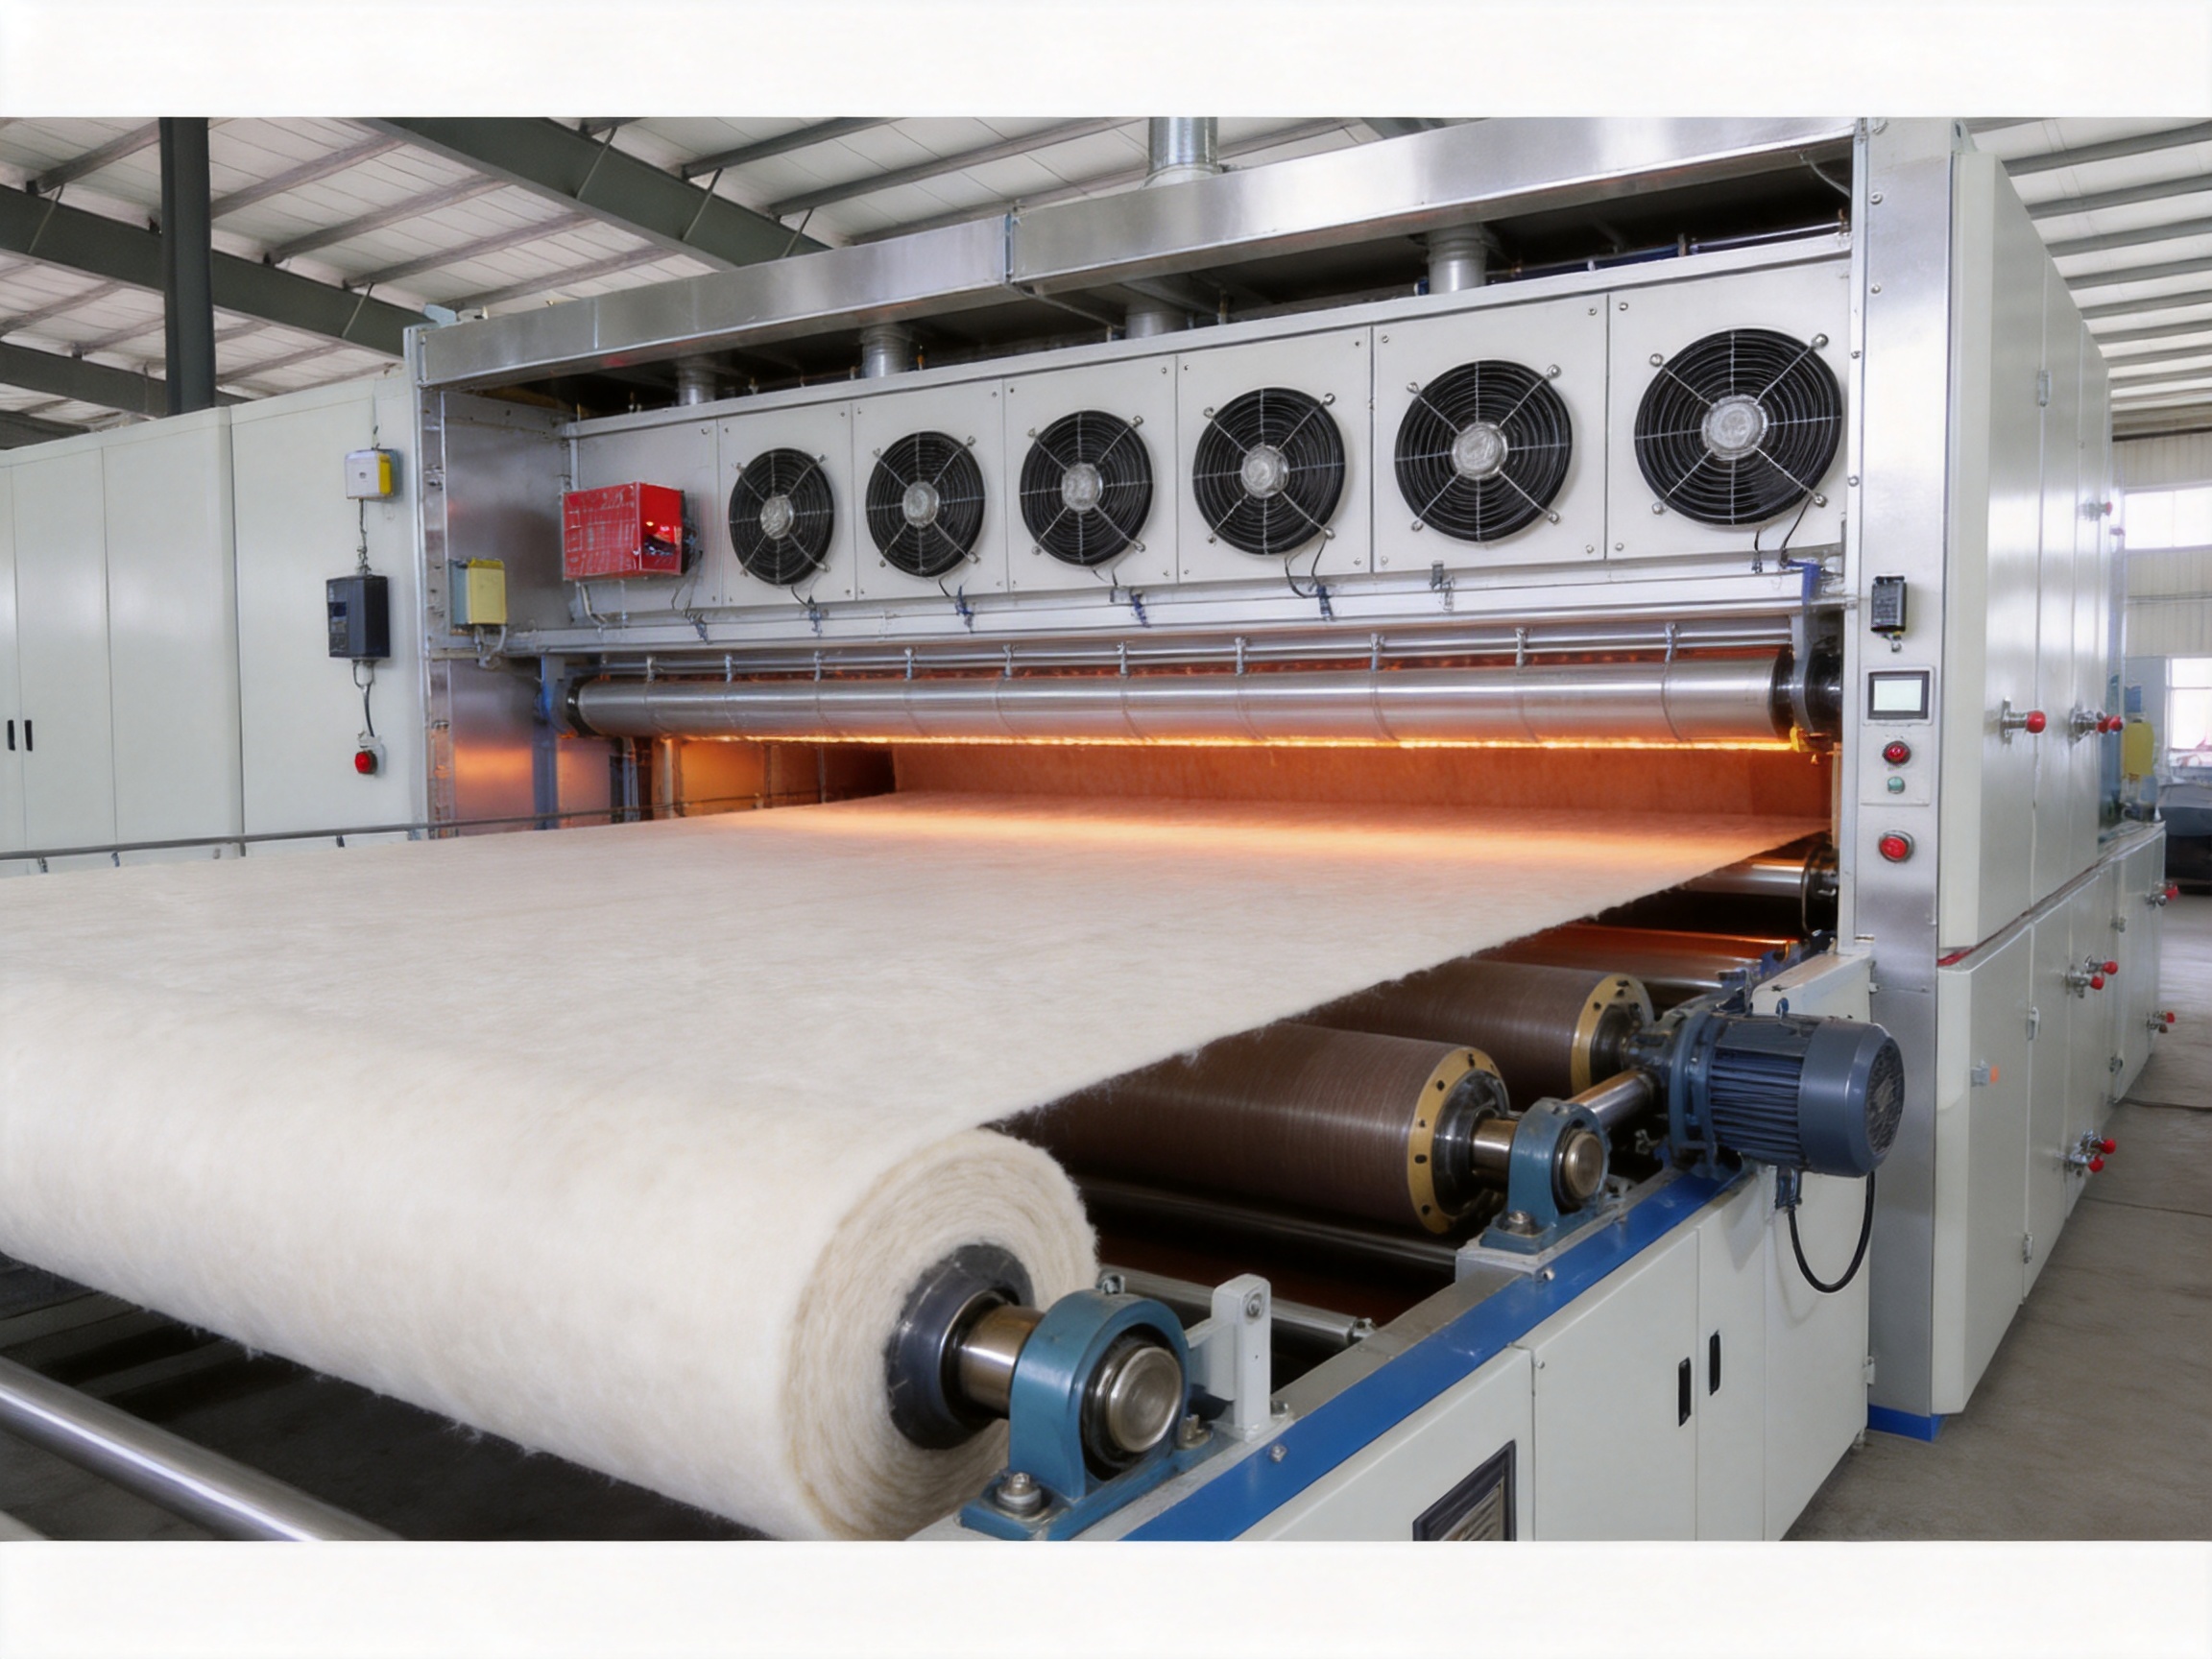
A thermal-bonded oven is a substantial piece of production equipment and requires adequate floor space. The layout must allow room for the cross lapper, feeding section, oven, cooling area, winding or cutting equipment, electrical cabinets, heating system, maintenance access, and material handling.
Operators should be able to access inspection points, belt adjustment components, fan assemblies, filters, control cabinets, and emergency-stop devices. Sufficient clearance is also needed for belt replacement, cleaning, component removal, and future maintenance work.
Utility Requirements
The required utilities depend on whether the machine uses hot-oil circulation or electric heating. Electrical supply, control voltage, fan power, heating capacity, ventilation, cooling requirements, and compressed air requirements should be confirmed during engineering.
If hot-oil circulation is selected, the plant may need a thermal-oil heater, circulation pump, expansion tank, piping, safety devices, and suitable insulation. If electric heating is selected, the facility must provide sufficient electrical capacity and appropriate protection systems.
Raw Material Preparation
Stable oven performance begins with consistent fiber preparation. Fiber length, fineness, moisture, contamination level, low-melt fiber content, and blend uniformity all influence the thermal-bonding result.
The web-forming process must also deliver consistent basis weight across the width. If the batt enters the oven with large variations in thickness or density, even the best air-circulation system cannot fully compensate for those variations. Carding, blending, feeding, and cross-lapping should therefore be synchronized with the oven.
Temperature and Speed Settings
The oven temperature should be high enough to soften the low-melt fiber but not so high that the structural fibers degrade, shrink excessively, discolor, or lose their intended properties. Line speed determines residence time, while air velocity affects the rate and uniformity of heat transfer.
Operators should establish production recipes through controlled trials. A recipe may begin with conservative temperature and speed settings, followed by inspection of bonding strength, thickness, appearance, density, and shrinkage. Adjustments should be made gradually rather than changing several variables simultaneously.
Cooling and Stabilization
Cooling is an essential part of the thermal-bonding process. If the material exits the heating zone while the bonding component is still soft, the web may deform under its own weight or during winding. A controlled cooling section helps stabilize the structure before downstream handling.
The correct cooling condition depends on product thickness, line speed, fiber type, and target temperature at the oven exit. Thick materials generally require more time for internal heat to dissipate than lightweight materials.
Maintenance and Operational Reliability
Routine maintenance is necessary to preserve product quality and extend equipment service life. Operators should inspect belt tracking, belt tension, belt surface condition, fan vibration, motor temperature, bearing condition, air ducts, filters, sensors, and control alarms.
Automatic belt correction reduces manual intervention, but it does not eliminate the need to inspect alignment and tension. A belt that repeatedly moves toward one side may indicate a mechanical alignment issue, uneven loading, contamination, worn components, or incorrect tension.
Cleaning is also important. Accumulated fiber can affect air distribution, reduce heat-transfer efficiency, obstruct sensors, and create a safety risk. Cleaning frequency should be based on the material being processed, operating hours, fiber shedding, and the condition of the air-circulation system.
Heating systems require special attention. Electric heating components should be checked for electrical connections, insulation condition, temperature-control accuracy, and signs of overheating. Hot-oil systems should be inspected for leaks, oil quality, pressure, circulation, expansion, and thermal insulation.
Preventive maintenance is normally more economical than waiting for a belt failure, fan breakdown, or uncontrolled temperature event. A documented maintenance schedule should identify daily, weekly, monthly, and annual inspection tasks.
Quality Control of Finished Material
Finished nonwoven material should be evaluated against the customer’s technical requirements. Common quality-control items include basis weight, thickness, width, tensile strength, tear strength, compression recovery, density, moisture content, shrinkage, surface appearance, and bonding uniformity.
For thick products, testing should consider both surface and internal structure. A material may appear well bonded on the outside while remaining weak in the center if hot-air penetration is insufficient. Cross-sectional inspection, peel testing, compression testing, or internal-bond evaluation may therefore be appropriate.
Process records should include the raw material batch, fiber blend, machine speed, heating temperature, fan setting, cooling condition, product weight, and operator observations. These records help identify the cause of quality variation and make it easier to reproduce successful production settings.
Width consistency should also be monitored. Edge shrinkage or lateral movement can reduce usable width and create problems for winding, cutting, lamination, or molding. The belt correction system, web alignment, and cross-lapper settings should be reviewed when width variation occurs.
Why Choose a Customized Oven Solution
A thermal-bonded oven is not simply a heated conveyor. Its performance is determined by the interaction of heat, air, fiber composition, web structure, pressure, line speed, cooling, and downstream handling. For this reason, selecting an oven based only on nominal width or maximum temperature can lead to unsatisfactory results.
A customized solution begins with the intended product. The manufacturer should understand whether the customer plans to produce lightweight wadding, high-bulk insulation, automotive material, mattress padding, filtration media, or another type of nonwoven. Each product may require a different balance of air penetration, thickness control, heating uniformity, and cooling capacity.
Customization can also reduce future limitations. A line designed with adequate width, suitable control capacity, and flexible heating arrangements may support additional product grades as the business develops. This can improve the long-term value of the investment.
Changshu Hongyi Nonwoven Machinery Co., Ltd. offers customized configurations and can supply individual machines or integrated nonwoven production lines. Its product portfolio and international project experience provide a foundation for discussing different production objectives with customers.
Frequently Asked Questions
What is the main function of the HYHX Nonwoven Fabric Oven?
The main function is to thermally bond a fiber web from a cross lapper by using hot-air penetration. The low-melt fiber softens and combines the other fibers, while the cooling system helps reinforce and stabilize the final wadding.
What raw materials can be processed?
The listed raw materials include polyester fiber and polypropylene staple fiber. The exact fiber blend should include a compatible low-melt component when thermal bonding is required. Final compatibility should be confirmed through material testing and process trials.
What is the maximum working width?
The specified working width is up to 5,000 millimeters. The actual usable width depends on the selected configuration, edge allowance, product type, and line design.
What product thickness can the oven handle?
The listed product thickness range is 3 to 200 millimeters. Actual performance depends on basis weight, fiber density, low-melt fiber content, belt arrangement, heating profile, and cooling conditions.
What product weights are supported?
The stated product weight range is approximately 60 to 1,500 GSM. Customers should confirm the expected output and quality requirements for each specific product grade because maximum range and maximum production speed may not be available simultaneously.
What heating methods are available?
The oven can be configured for hot-oil circulation or electric heating. The most suitable option depends on plant utilities, energy costs, available space, production schedule, and customer preference.
Can the machine be customized?
Yes. The configuration can be customized according to customer requirements. Possible customization areas include working width, oven length, belt structure, heating method, cooling arrangement, control system, and integration with other nonwoven machinery.
What are the benefits of a double-belt structure?
A double-belt structure supports the web from above and below as it passes through the oven. This can improve transport stability and thickness control, particularly for thick or high-weight products. The correct structure should be selected according to the product and process requirements.
How does inverter control help production?
Inverter control allows the operator to adjust the main drive and fan speed. This supports better control of residence time and air circulation, smoother machine operation, and more efficient adjustment for different material grades.
Why is automatic belt correction important?
Automatic belt correction helps maintain the belt’s lateral position during continuous operation. It reduces manual intervention and helps prevent edge damage, unstable web transport, and excessive belt wear caused by belt deviation.
What certifications are listed for the machine?
The supplied product information lists CE and ISO9001:2000 certification. Buyers should request current certification documents and confirm that the equipment complies with the regulations applicable at the installation location.
What after-sales support is provided?
The product information specifies a one-year warranty. The exact scope of installation, commissioning, operator training, spare parts, and remote technical support should be confirmed in the commercial and technical agreements.
Can the oven be integrated into a complete production line?
Yes. It is designed to process a web from a cross lapper and can be integrated with opening, blending, feeding, carding, web-forming, winding, cutting, and other auxiliary equipment. The supplier also provides complete nonwoven production lines.
What information should be provided when requesting a quotation?
The customer should provide the raw material, fiber blend, low-melt fiber type, working width, product weight, thickness, target output, heating preference, factory conditions, power supply, product application, and downstream equipment requirements. More complete information allows more accurate engineering and pricing.
Conclusion
The HYHX Nonwoven Fabric Oven is a flexible thermal-bonding solution for manufacturers producing thick, stable, and reinforced nonwoven waddings. Its hot-air penetration process allows low-melt fibers to bond with other fibers throughout the web, while the controlled cooling stage helps stabilize the finished structure.
The single-layer, single-belt, and double-belt options provide configuration flexibility. High-temperature-resistant belts, automatic belt correction, inverter-controlled drives and fans, and selectable hot-oil or electric heating support reliable industrial operation. A working width of up to 5,000 millimeters and a stated product range of 60 to 1,500 GSM and 3 to 200 millimeters make the equipment suitable for a broad range of applications.
Its advantages are strengthened by the manufacturing capabilities of Changshu Hongyi Nonwoven Machinery Co., Ltd. With more than 20 years of experience, a portfolio covering complete production lines and individual machines, international supply experience, customization capability, and after-sales support, the company can provide equipment for both standard and specialized nonwoven projects.
For customers comparing thermal-bonding equipment, the most important evaluation criteria should include heating uniformity, air penetration, belt stability, thickness control, energy configuration, maintenance accessibility, automation, product flexibility, and the supplier’s ability to engineer the machine around the complete production process. When these factors are properly matched, a thermal-bonded oven can become a reliable foundation for efficient and consistent nonwoven fabric production.
References
1. Product technical information for the HYHX Nonwoven Fabric Oven, including operating range, structural configuration, heating methods, and control features.
2. Internal company profile and product portfolio information for Changshu Hongyi Nonwoven Machinery Co., Ltd.
3. General principles of thermal bonding, hot-air circulation, low-melt fiber consolidation, and nonwoven web stabilization.
4. General industrial practices for nonwoven machinery installation, belt maintenance, temperature control, process monitoring, and quality assurance.
5. General technical considerations for polyester fiber, polypropylene staple fiber, thermal-bonded wadding, automotive nonwovens, insulation products, and industrial textile applications.