

Content
- 1 1. The Role of Airlaid Waste Felt in Modern Nonwoven Manufacturing
- 2 2. Product Overview and Main Technical Range
- 3 3. Complete Process Flow from Waste Fiber to Finished Felt
- 4 4. Advantages over Conventional and Less Flexible Production Systems
- 4.1 4.1 Wider Raw-Material Compatibility
- 4.2 4.2 Reduced Fiber Damage Compared with Aggressive Processing
- 4.3 4.3 Efficient Waste Conversion
- 4.4 4.4 High Product Thickness and GSM Flexibility
- 4.5 4.5 Customizable Working Width
- 4.6 4.6 Better Suitability for Recycled PET and Mixed Fiber Products
- 4.7 4.7 Automatic Operation and Production Consistency
- 5 5. Applications of Airlaid Waste Felt
- 6 6. Manufacturing Strengths and Engineering Capabilities
- 7 7. Recommended Factory Planning and Installation Considerations
- 8 8. Operation, Maintenance, and Quality Control
- 9 9. How to Select the Correct Configuration
- 10 10. Commercial and Environmental Value
- 11 11. Why Work with an Experienced Nonwoven Machinery Manufacturer
- 12 12. Questions and Answers
- 12.1 Q1: What materials can the airlaid waste felt production line process?
- 12.2 Q2: What fiber length can be handled?
- 12.3 Q3: What is the production capacity?
- 12.4 Q4: What GSM range can be produced?
- 12.5 Q5: What finished thickness can be achieved?
- 12.6 Q6: Can the working width be customized?
- 12.7 Q7: Is the line suitable for automotive felt?
- 12.8 Q8: Does the line use carding technology?
- 12.9 Q9: Can low-melt fiber be used?
- 12.10 Q10: Is the line automatic?
- 12.11 Q11: What should be prepared before requesting a quotation?
- 12.12 Q12: What after-sales service is provided?
- 13 13. Conclusion
- 14 References
- 15 Product: HYL Airlaid Waste Felt Production Line
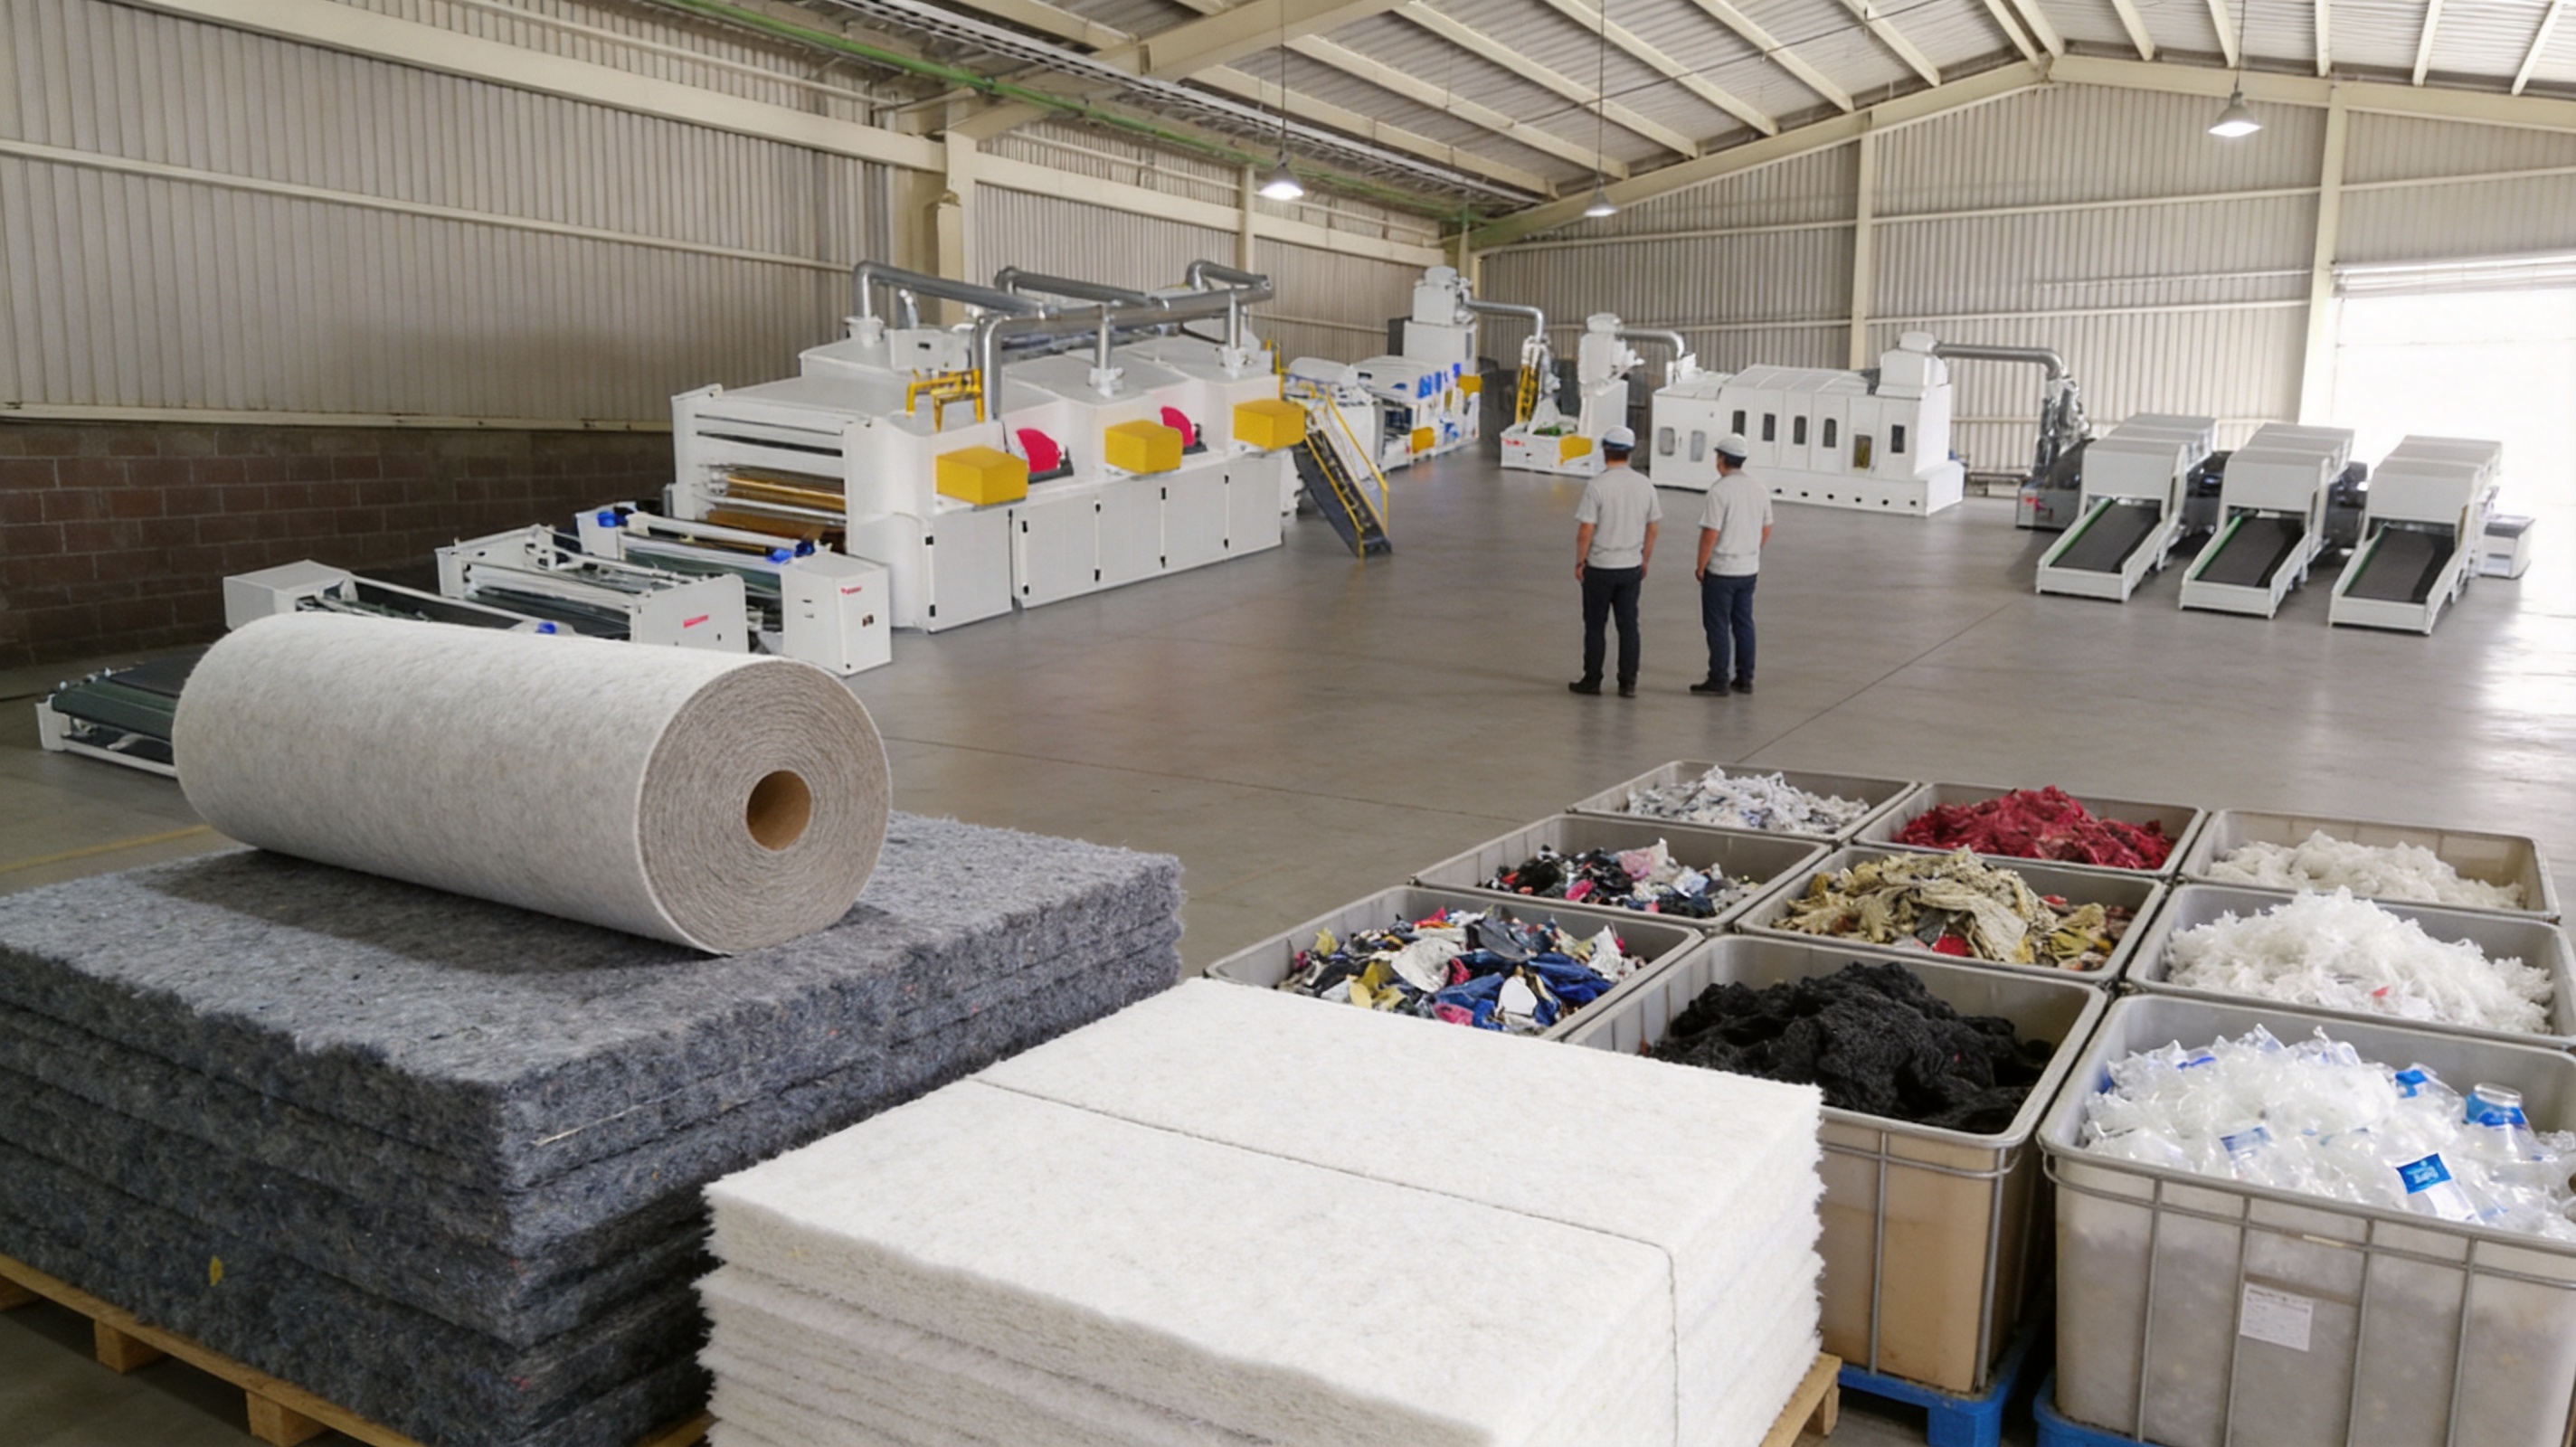
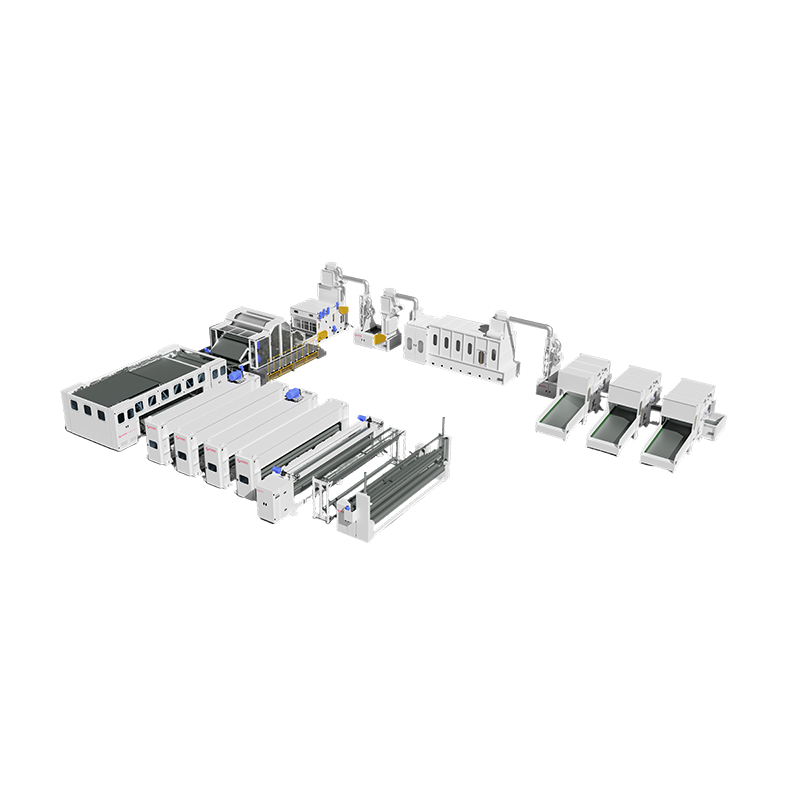
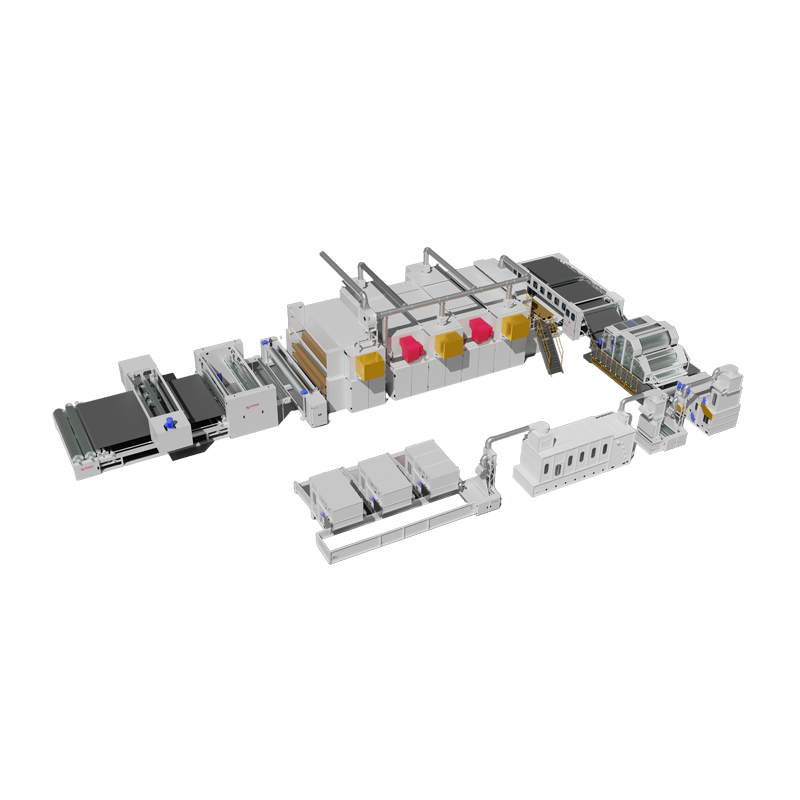
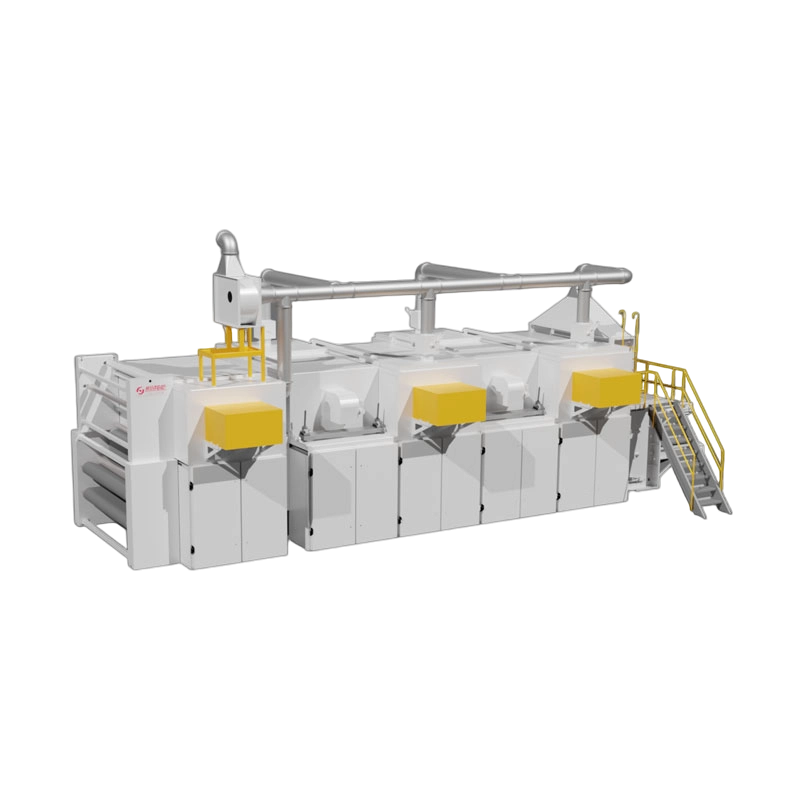
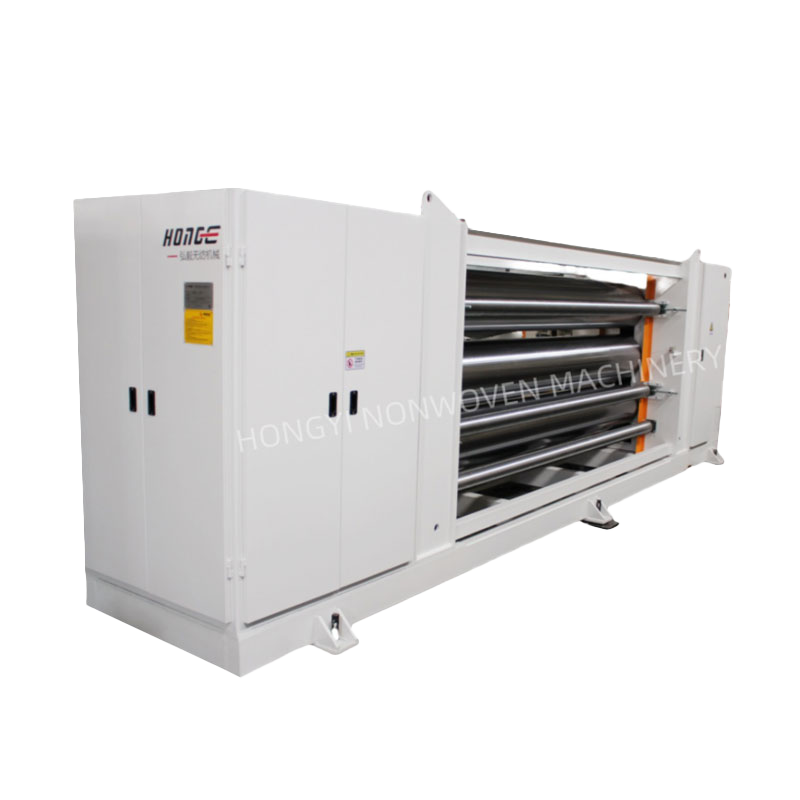
The airlaid waste felt production line is designed for manufacturers seeking to convert textile waste, discarded fiber felt, recycled polyester, and other fibrous residues into useful nonwoven products. By combining waste opening, fiber preparation, dust removal, airlaid web forming, reinforcement, thermal treatment, and winding or cutting operations, the line provides an integrated route from difficult-to-process waste materials to finished felt products.
Airlaid waste felt technology is increasingly important as nonwoven producers face rising raw material costs, stricter environmental expectations, and growing demand for recycled products. Conventional production systems may depend heavily on long, uniform virgin fibers and carding processes. In contrast, an airlaid system is capable of handling fibers with different lengths and compositions, including waste fibers ranging from approximately 5 to 85 millimeters. This flexibility allows manufacturers to make greater use of materials that might otherwise be sent to disposal or used only in low-value applications.
The HYL Airlaid Waste Felt Production Line supplied by Changshu Hongyi Nonwoven Machinery Co., Ltd. is configured for the production of automotive interior felts, insulation materials, packaging materials, furniture protection products, and related nonwoven articles. Its working width can be customized from approximately 1,500 to 2,800 millimeters, while the stated production capacity is approximately 500 to 1,000 kilograms per hour, depending on raw material, product weight, thickness, and line configuration.
With a product GSM range of approximately 500 to 7,500 grams per square meter and a finished thickness range of approximately 5 to 200 millimeters, the line can serve both medium-weight and heavy felt applications. Its design can also be adapted to meet customer requirements for working width, raw material composition, color, automation, reinforcement, and downstream handling.
1. The Role of Airlaid Waste Felt in Modern Nonwoven Manufacturing
Airlaid waste felt is produced by opening and distributing fibers through an air stream rather than relying exclusively on mechanical carding. The process creates a three-dimensional fiber web in which fibers are deposited onto a forming surface. This web can then be reinforced, compacted, thermally bonded, needle punched, or otherwise treated according to the required performance characteristics.
The basic principle is especially valuable when the raw material contains short fibers, mixed fibers, reclaimed textile scraps, or irregularly opened fragments. Carding machines generally perform best when fibers are relatively consistent in length, cleanliness, fineness, and orientation. Waste streams are often less uniform. They may contain fibers of various lengths, small fabric pieces, loosened bundles, and materials recovered from previous production stages.
An airlaid system offers a more adaptable method of forming a uniform bulk structure from these materials. Air transportation helps separate and distribute the fibers, while the forming system creates a web with controlled width and weight. This approach can reduce the limitations caused by fiber length and can make recycling more commercially practical.
For producers of automotive interior materials, the process is suitable for manufacturing felt layers used in trunk liners, headliners, door panels, wheel arch coverings, underbody components, acoustic parts, and interior protection structures. In building applications, the resulting products may be used for thermal insulation, acoustic absorption, cushioning, and protective separation. In packaging and furniture logistics, thick felt can help protect surfaces from impact, scratching, vibration, and abrasion during handling and transport.
2. Product Overview and Main Technical Range
The HYL line is an automatic, customizable production system. It is manufactured primarily from steel and iron mechanical components and is designed for continuous industrial operation. The line can be engineered around the customer’s raw materials and finished-product specifications instead of forcing every user to adopt one fixed configuration.
| Item | Available or Stated Range | Manufacturing Significance |
|---|---|---|
| Model | HYL | Airlaid waste felt production system |
| Working width | 1,500–2,800 mm | Suitable for different production scales and product widths |
| Production capacity | 500–1,000 kg/h | Depends on raw material, GSM, thickness, and configuration |
| Product GSM | 500–7,500 g/m² | Supports medium-weight to heavy felt products |
| Finished thickness | 5–200 mm | Suitable for insulation, packaging, automotive, and protection uses |
| Fiber length handled | Approximately 5–85 mm waste fibers | Broadens the usable waste-material range |
| Raw materials | Natural fiber, cotton, wool, polyester, recycled waste fiber, low-melt fiber | Enables blended and recycled product development |
| Automation | Automatic | Supports coordinated operation and stable production management |
| Configuration | Customizable | Allows the line to be matched to customer requirements |
| Certification | CE and ISO9001-related quality system information | Supports international project and quality requirements |
The figures in this table should be understood as a configuration range rather than a guarantee that every combination of GSM, thickness, raw material, width, and output can be achieved simultaneously. Actual performance depends on fiber cleanliness, moisture, fiber blend, opening quality, web density, reinforcement method, thermal conditions, and the final product specification.
3. Complete Process Flow from Waste Fiber to Finished Felt
3.1 Raw Material Feeding
The production process begins with the controlled feeding of waste fiber or other selected raw materials. Typical materials include textile scraps, waste fiber felt, cotton fiber, wool, polyester fiber, recycled PET fiber, natural fibers, and low-melt fibers used to support thermal bonding.
Consistent feeding is important because fluctuations in material flow can create variations in web weight, density, thickness, and tensile performance. The feeding section is therefore selected according to the size, bulk density, moisture content, and composition of the raw material. Where several fibers are blended, the feeding arrangement can be organized to achieve a more consistent mixture before opening and forming.
For recycled materials, preliminary sorting is recommended. Large foreign objects, metal pieces, stones, excessive moisture, and materials that are incompatible with the intended product should be removed before entering the machine. Good raw-material preparation protects the opening equipment, reduces dust-related problems, and improves finished-product consistency.
3.2 Waste Opening and Fiber Separation
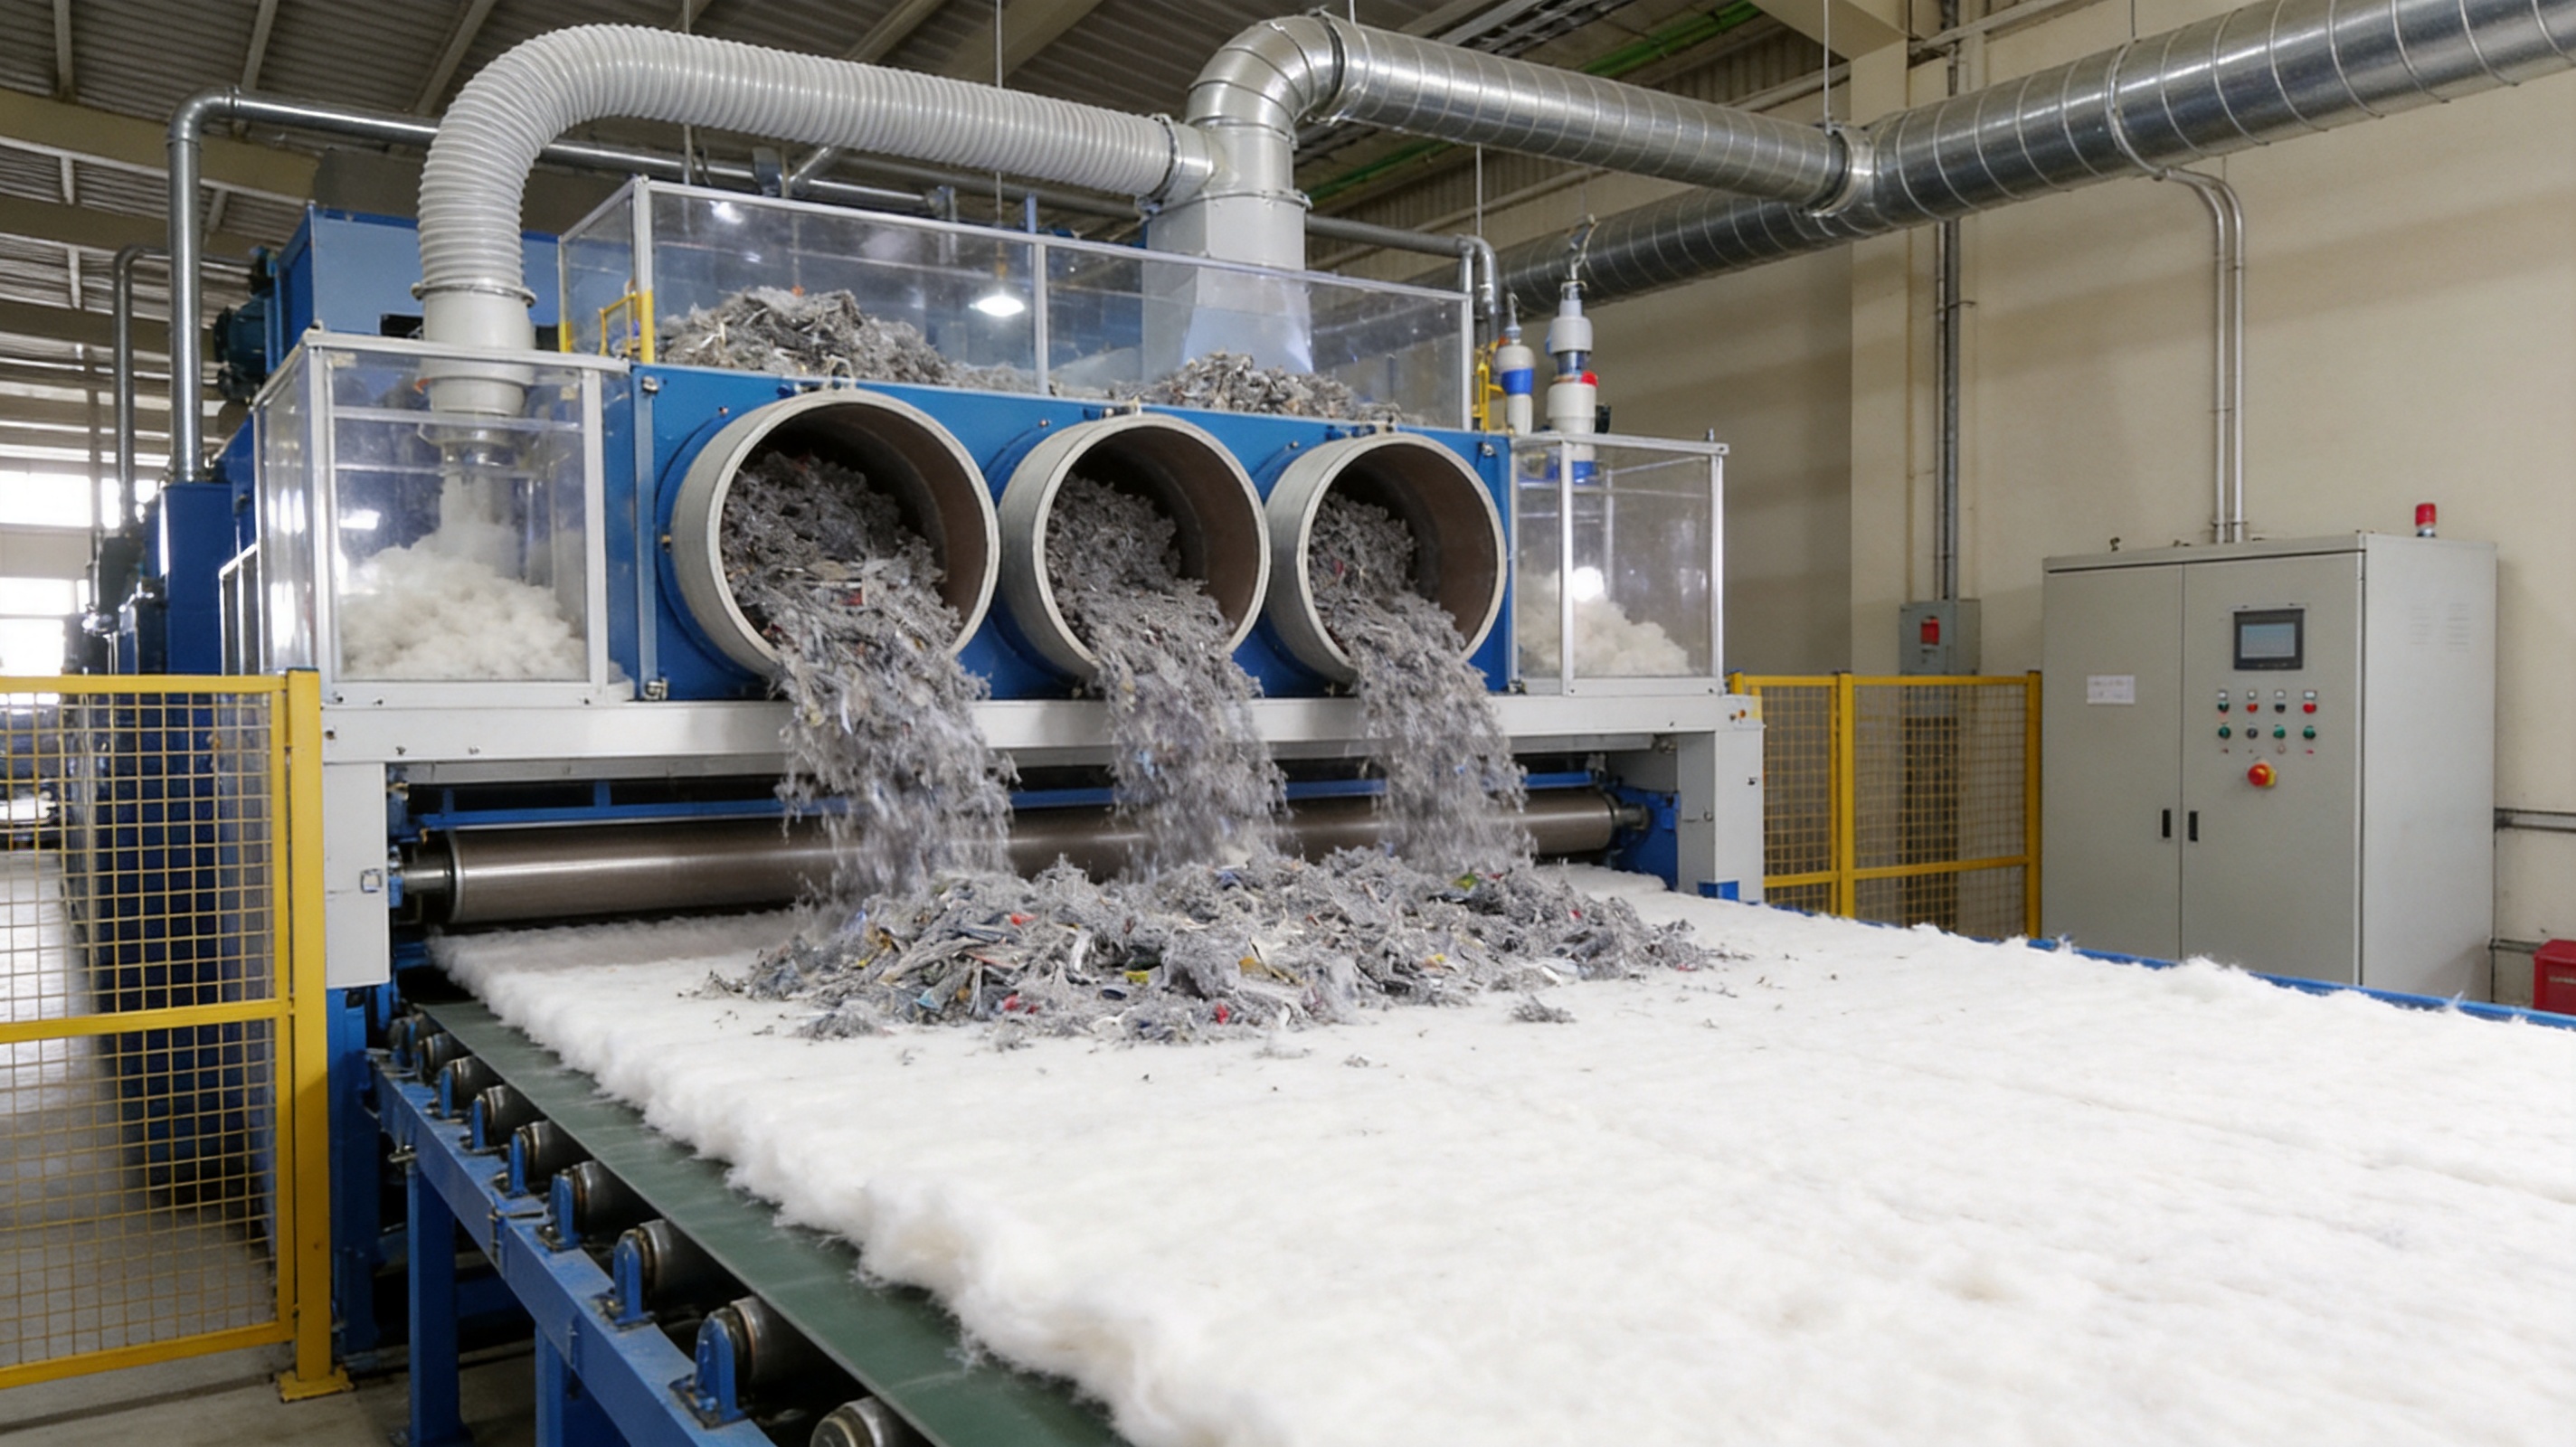
Waste fibers often arrive in compacted bundles, fabric pieces, felt fragments, or tangled clusters. The opening section breaks these structures into a more processable form. Mechanical opening separates the material, loosens fiber bundles, and prepares the fibers for pneumatic transportation and web forming.
Compared with a process designed only for carefully prepared virgin fiber, a waste-opening system must tolerate greater variation in size and structure. Its performance depends on the relationship between opening intensity, feed rate, fiber strength, and the intended degree of fiber separation. Excessive mechanical action may shorten or damage fibers, while insufficient opening may leave dense bundles in the airlaid web.
The HYL production concept places opening and recycling at the beginning of an integrated process. This is one of its principal advantages for manufacturers that want to use production waste as a regular raw material rather than treating recycling as a separate, low-capacity activity.
3.3 Dust Removal and Air Management
Waste fibers can contain dust, loose particles, short fiber fragments, and contaminants generated during cutting, tearing, or previous use. Dust removal helps improve the cleanliness of the processed fiber and contributes to a more stable working environment. It also supports more reliable operation of the forming section by reducing the quantity of unwanted fine material circulating through the system.
Air management is central to airlaid production. The air stream must transport the fibers without causing excessive turbulence, uneven deposition, or uncontrolled fiber loss. Properly designed air circulation allows the line to distribute fibers across the forming width while maintaining a stable relationship between feed rate and web weight.
In an industrial installation, dust collection and ventilation should be planned together with the production line. The final arrangement depends on the raw material, local environmental standards, factory layout, and customer requirements. Regular cleaning, filter maintenance, and inspection of air ducts are important parts of responsible operation.
3.4 Airlaid Web Formation
After opening and cleaning, the fibers are carried by air and deposited onto a forming surface. Unlike a conventional carding process, which tends to create a web with a more defined machine direction, airlaid formation can produce a comparatively random fiber orientation. This is beneficial when the finished felt requires balanced properties in more than one direction.
The forming system must control fiber distribution, web width, basis weight, and bulk. A stable web is essential for subsequent reinforcement because variation in the initial structure can become more visible after needle punching, thermal bonding, or compression. The forming section is therefore one of the most important areas for controlling product quality.
Airlaid formation also provides an effective route for processing fibers that are too short, too mixed, or too irregular for efficient carding. It does not eliminate the need for raw-material control, but it broadens the practical range of materials that can be used. This can reduce dependence on a narrow supply of uniform virgin fibers.
3.5 Web Reinforcement
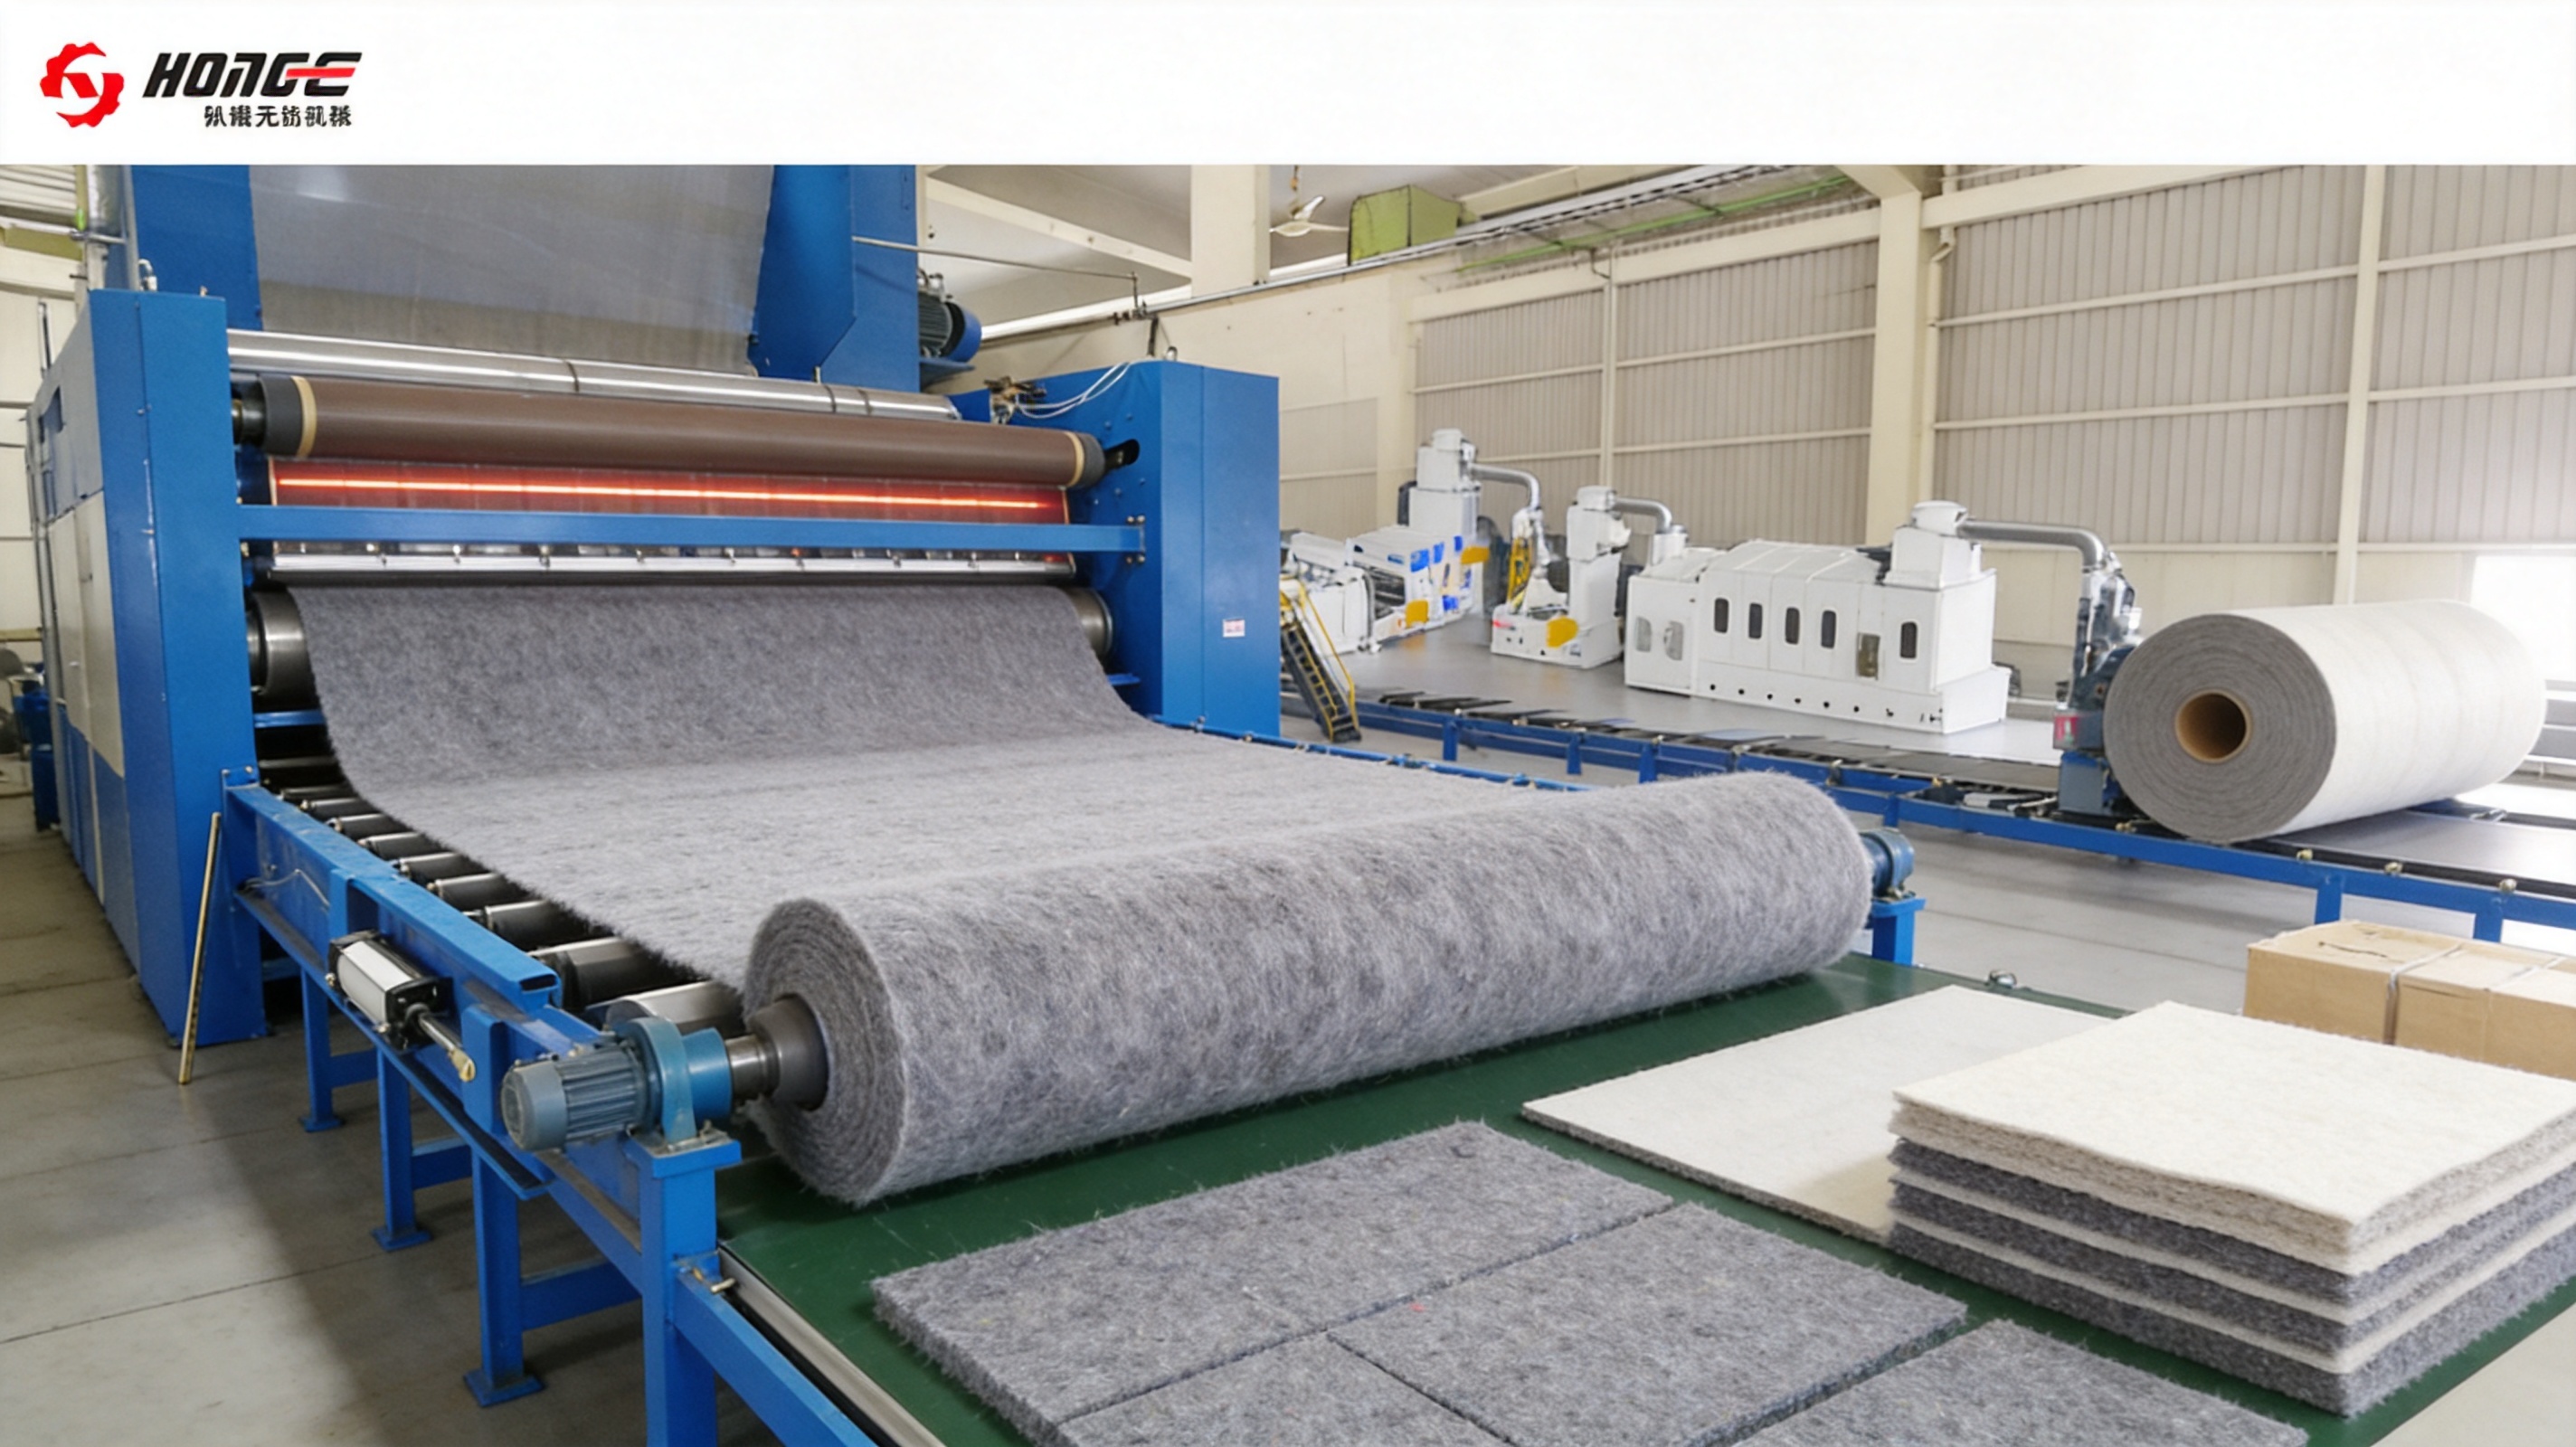
The freshly formed airlaid web has bulk but limited handling strength. Reinforcement converts the loose web into a stable nonwoven structure. Depending on the product design, reinforcement may involve needle punching, thermal bonding, the addition of low-melt fibers, or a combination of these methods.
Needle punching mechanically entangles fibers by repeatedly passing barbed needles through the web. It is commonly used where the final material must have thickness, resilience, abrasion resistance, and mechanical integrity. Thermal bonding uses heat to soften or melt bonding fibers, joining the surrounding fiber structure without requiring a separate adhesive in every application.
The correct reinforcement method depends on the target product. Automotive felts may require a balance of stiffness, sound absorption, shape retention, and low weight. Packaging felt may require compressibility and recovery. Insulation products may prioritize thickness, thermal resistance, acoustic absorption, and dimensional stability. The production line can be configured according to these different requirements.
3.6 Thermal Treatment and Heat Setting
When low-melt fibers or thermoplastic components are included in the blend, a thermal bonding or heat-setting stage can stabilize the web. Controlled temperature, dwell time, web speed, and pressure influence bonding strength, surface condition, thickness, and recovery.
A well-designed thermal stage should provide even treatment across the working width. Uneven heating can cause differences in bonding, shrinkage, density, or color. For this reason, temperature control, insulation, air circulation, and conveyor stability are important elements of the manufacturing system.
Heat setting may also be used to establish a more stable final thickness or shape. The exact thermal recipe must be developed through trials because different fibers respond differently to heat. Polyester, low-melt polyester, natural fiber, and blended structures cannot always be processed using the same temperature and residence time.
3.7 Winding, Cutting, and Finished-Product Handling
After reinforcement and thermal treatment, the material can be wound into rolls or cut into sheets, panels, pads, or specified lengths. The winding and cutting arrangement depends on the customer’s sales format and the requirements of downstream processing.
Continuous roll production is useful for customers supplying converters or automotive component manufacturers. Cut sheets may be more appropriate for furniture protection, packaging, insulation panels, or pre-cut interior components. Automated handling can reduce manual labor and help maintain repeatable roll tension, edge alignment, and product length.
Finished products should be inspected for width, GSM, thickness, visual uniformity, edge quality, moisture, and mechanical performance. Additional testing may be required for sound absorption, thermal conductivity, compression recovery, flammability, odor, or vehicle-interior specifications.
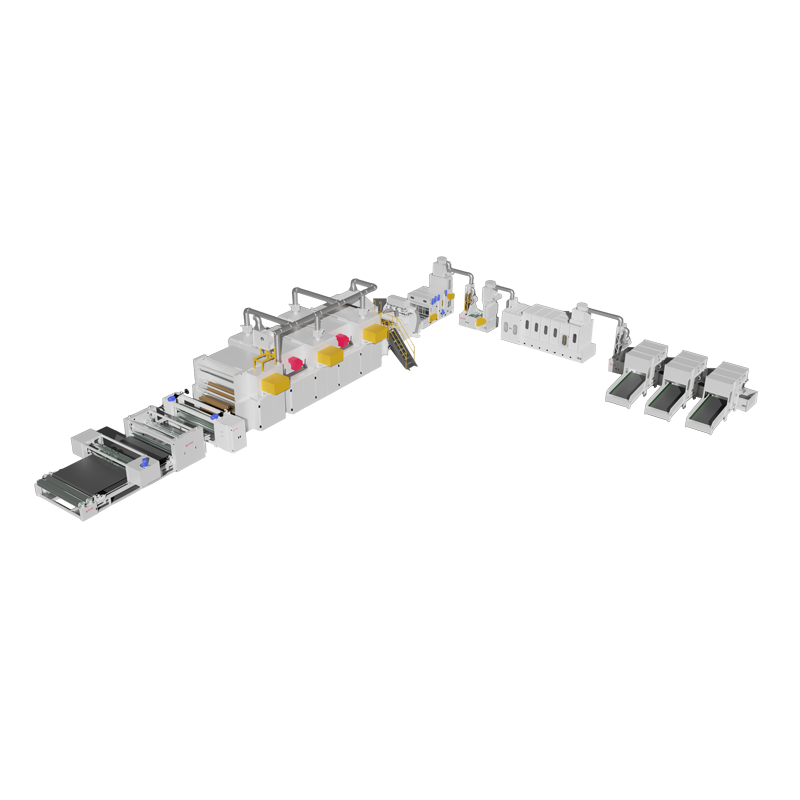
HYL Airlaid Waste Felt Production Line
4. Advantages over Conventional and Less Flexible Production Systems
4.1 Wider Raw-Material Compatibility
The most important advantage of an airlaid waste felt line is its ability to process a broad range of fibers and waste materials. The stated fiber-length range of approximately 5 to 85 millimeters is especially significant for recycling applications. Textile waste is rarely uniform, and a system that can accommodate different fiber lengths gives the manufacturer more freedom in selecting suppliers and blending materials.
A conventional carding-based system may require tighter control over fiber length, fiber openness, and material cleanliness. When waste material falls outside the preferred range, the producer may need additional preparation equipment or may be forced to purchase more virgin fiber. The airlaid approach reduces this limitation and provides a more direct path for converting waste into a saleable product.
4.2 Reduced Fiber Damage Compared with Aggressive Processing
Waste fibers can be vulnerable to further breakage. Excessive opening or repeated carding may shorten the fibers and reduce their contribution to strength. Airlaid forming uses airflow to distribute the opened fibers, which can help preserve the usable fiber population after preparation.
The degree of fiber protection depends on machine settings and material characteristics. However, the overall process concept is designed to avoid unnecessary restrictions associated with repeated mechanical carding. This is valuable when the goal is to maintain bulk, resilience, and usable fiber length in a recycled product.
4.3 Efficient Waste Conversion
The line integrates waste opening, dust removal, web forming, and reinforcement in one coordinated production route. This integration can reduce the need to transfer semi-processed material between independent machines. It also allows waste handling and final product formation to be planned as a single production system.
Efficient waste conversion has both economic and environmental benefits. Usable production scrap can become a feedstock instead of a disposal cost. Recycled fiber can replace part of the virgin material requirement, depending on the performance specification. The manufacturer can also develop products that contain higher recycled content for customers with sustainability objectives.
4.4 High Product Thickness and GSM Flexibility
The stated product range of 500 to 7,500 GSM and 5 to 200 millimeters in thickness provides considerable flexibility for heavy felt production. This is relevant to insulation boards, automotive cushioning, protective pads, transport packaging, and other applications in which a thick three-dimensional structure is required.
Many nonwoven producers need to serve more than one market. A line that can be configured for different basis weights and thicknesses may allow a factory to move between product categories without purchasing a completely separate production system for every application. The practical changeover range depends on the equipment configuration and material recipe, but customization provides a foundation for multi-product manufacturing.
4.5 Customizable Working Width
Working widths from approximately 1,500 to 2,800 millimeters cover a range of production requirements. A narrower line may be suitable for a smaller factory or specialized product, while a wider line can improve output for broad rolls and large-format automotive or insulation materials.
Width customization also helps customers match the line to their existing plant layout, roll dimensions, downstream cutting equipment, and target markets. Instead of selecting a machine based only on a standard catalog size, a buyer can discuss the relationship between width, capacity, product GSM, and available factory space.
4.6 Better Suitability for Recycled PET and Mixed Fiber Products
Recycled PET fibers are increasingly used in nonwoven products because they can provide useful mechanical and thermal characteristics while supporting recycled-content objectives. The HYL line can process recycled polyester together with other fibers, including low-melt fibers where thermal bonding is required.
Mixed fiber recipes allow product developers to balance cost, strength, resilience, softness, thermal behavior, acoustic performance, and recycled content. For example, a blend may combine recycled polyester for structural support, natural fiber for bulk or comfort, and low-melt fiber for bonding. The final recipe should be established through laboratory and production trials, but the line’s broad material compatibility makes such development practical.
4.7 Automatic Operation and Production Consistency
Automatic control supports coordinated operation of feeding, opening, air circulation, web formation, reinforcement, thermal treatment, and winding. Automation can help operators manage speed, temperature, feed rate, and other process conditions from a central control system.
Automation does not replace process knowledge. Operators still need to understand fiber behavior, equipment maintenance, quality inspection, and safe operating procedures. However, automatic control can reduce unnecessary manual adjustments and improve repeatability when the correct process parameters have been established.
5. Applications of Airlaid Waste Felt
5.1 Automotive Interior Materials
Automotive interiors require materials that can be shaped, cut, laminated, bonded, or assembled into complex components. Felt products are used in areas where cushioning, sound absorption, insulation, surface protection, and lightweight reinforcement are required.
Potential applications include trunk liners, parcel shelves, door components, wheel housing covers, under-carpet layers, headliner backing, acoustic panels, and protective interior sections. The appropriate material design depends on the vehicle manufacturer’s requirements for odor, emissions, flammability, compression, thickness, weight, and dimensional stability.
Airlaid waste felt is particularly useful when a manufacturer wants to combine recycled content with a thick, resilient structure. Recovered textile fibers and recycled PET can be processed into products that contribute to lightweight vehicle design and resource efficiency.
5.2 Thermal and Acoustic Insulation
The open fiber structure of felt can trap air and absorb sound energy. Depending on density, thickness, fiber type, and surface treatment, the product may be used for thermal or acoustic insulation in buildings, machinery, vehicles, and industrial equipment.
Thicker products can provide increased separation and cushioning, while carefully controlled density can support acoustic absorption. Natural fibers and polyester fibers may be blended to achieve a balance between handling properties, thermal response, and product cost.
5.3 Packaging and Transport Protection
Packaging felt can protect furniture, appliances, glass, metal parts, interior panels, and other valuable products during storage and transport. Its cushioning effect can reduce scratching, surface contact, vibration, and minor impact damage.
The ability to manufacture different thicknesses and cut formats enables producers to supply rolls, sheets, pads, corner protectors, or custom inserts. Recycled fibers can be particularly suitable for protective packaging where appearance requirements are less demanding than in consumer-facing textile products.
5.4 Furniture and Surface Protection
Furniture manufacturers, logistics companies, and moving services use felt materials to separate surfaces and prevent abrasion. Thick nonwoven felt can be placed between furniture components, wrapped around finished products, or used as a temporary protective layer during warehouse handling.
Because the production line can use recycled textile material, it is well suited to economical protection products. The producer can select a heavier GSM for cushioning or a lighter structure for separation and wrapping.
5.5 Industrial and Construction Products
Industrial applications may include filtration support layers, cushioning components, equipment insulation, vibration-control structures, and protective separators. Construction-related products may include insulation mats, underlay materials, protective layers, and acoustic elements.
These applications require careful product validation. Depending on the intended use, testing may cover tensile strength, tear resistance, compressive behavior, thermal conductivity, water response, fire performance, biological resistance, and long-term dimensional stability.
6. Manufacturing Strengths and Engineering Capabilities
6.1 More Than Two Decades of Industry Experience
Changshu Hongyi Nonwoven Machinery Co., Ltd. has more than 20 years of experience in the nonwoven machinery field. This experience supports the design and integration of production lines for different fiber types, product weights, reinforcement methods, and customer markets.
Long-term experience is important in nonwoven machinery because a production line is not simply a collection of individual machines. The opening section must match the forming system. The air system must match the fiber properties. The reinforcement unit must match the web structure. The thermal section must match the bonding fiber. The winding and cutting equipment must match the customer’s delivery format.
Practical experience helps the manufacturer evaluate these relationships and propose a more coherent line configuration. It also assists with troubleshooting, commissioning, operator training, spare parts planning, and future line upgrades.
6.2 Complete Equipment Portfolio
The company supplies complete nonwoven production lines as well as individual machines. Its product range includes needle-punched geotextile lines, nonwoven carpet lines, airlaid waste felt lines, automotive interior material lines, needle-punching cleaning cloth lines, wool felt lines, jute felt lines, needle-punching machines, carding machines, airlaid machines, ironing machines, and thermal bonding wadding oven machines.
This broader equipment portfolio is an advantage for customers that need more than one process stage. A manufacturer can discuss a complete line, a replacement unit, an expansion module, or a customized combination of machines with a supplier familiar with several nonwoven technologies.
6.3 Customized Line Design
Nonwoven factories differ in raw-material supply, product range, factory height, power availability, labor structure, environmental requirements, and budget. A standard machine may not provide the best solution for every site. The HYL line therefore allows configuration according to customer needs.
Customization may involve working width, feeding equipment, dust-removal arrangements, air circulation, web-forming parameters, needle-punching capacity, thermal bonding, cutting, winding, control systems, and product-handling equipment. The exact scope should be confirmed during technical discussions and factory planning.
A responsible customization process begins with raw-material samples and target-product information. The customer should provide details about fiber type, fiber length, moisture, contamination, blend ratio, desired GSM, thickness, width, output, and finished-product use. These details help the supplier select appropriate equipment and avoid designing a line around unrealistic assumptions.
6.4 Focus on Automation and Energy Efficiency
The company emphasizes automatic control systems, energy-saving capabilities, reliability, quality, and precision engineering. In a high-capacity nonwoven plant, energy consumption is influenced by opening power, air movement, dust extraction, needle punching, heating, and downstream handling.
Energy efficiency should be considered at the design stage. Suitable motor selection, controlled air circulation, insulation, heat recovery opportunities, optimized line speed, and preventive maintenance can all contribute to lower operating costs. The best solution depends on the final configuration and local energy conditions.
Automatic control can also help avoid over-processing. When the feed rate and line speed are synchronized, the manufacturer may reduce unnecessary recycling, unstable web formation, and repeated adjustments. Consistent operation supports both productivity and material efficiency.
6.5 International Project Experience
The company reports that its products have been supplied to more than 20 countries, including markets in Latin America, the Middle East, North Africa, South Asia, Southeast Asia, and other regions. International project experience requires attention to electrical standards, documentation, installation conditions, operator training, spare parts, packaging, and after-sales communication.
For buyers outside China, these factors can be as important as the machine’s basic production parameters. A successful project depends on clear technical specifications, accurate utility requirements, well-prepared installation instructions, and timely support during commissioning.
6.6 Quality Management and Product Certification
The supplied information identifies CE and ISO9001-related certification. CE marking is associated with applicable European conformity requirements, while an ISO9001 quality management system supports controlled procedures for design, manufacturing, inspection, and service. Customers should request current certificates and confirm which components and configurations are covered by the relevant documentation.
Quality control should extend across steel fabrication, machining, electrical assembly, control programming, surface treatment, component inspection, factory testing, and final documentation. For a complete production line, coordination between mechanical and electrical departments is essential to ensure that the installed equipment performs as designed.
7. Recommended Factory Planning and Installation Considerations
Before ordering an airlaid waste felt line, the buyer should evaluate the available factory space. The layout must accommodate raw-material storage, sorting, feeding, production equipment, dust collection, electrical cabinets, finished-product handling, maintenance access, and safe operator movement.
Ceiling height may be important because airlaid systems can include elevated ducts, feeding equipment, forming units, and exhaust arrangements. Floor strength should also be checked, particularly for heavy steel equipment and high-capacity production lines.
Utilities should be reviewed in advance. These may include electrical power, compressed air, heating fuel or electrical heating capacity, cooling water where required, ventilation, dust extraction, and lighting. The required specifications depend on the final design and should be confirmed through technical documentation rather than estimated from general catalog information.
Raw-material storage should be dry, organized, and protected from contamination. Recycled textile waste should be separated by fiber type where possible. Excessive moisture can affect opening, air transport, thermal bonding, and final product quality. A well-managed warehouse improves both production stability and recipe control.
Installation should be performed according to the supplier’s mechanical drawings, foundation requirements, electrical diagrams, and commissioning procedures. Leveling and alignment are particularly important for conveyors, forming surfaces, needle-punching equipment, ovens, calendars, winders, and cutters.
8. Operation, Maintenance, and Quality Control
8.1 Daily Operation
Operators should inspect the feeding area, opening equipment, air ducts, forming surface, needles, thermal section, cutting equipment, and winding system before starting production. Abnormal noise, vibration, overheating, dust leakage, loose fasteners, and material accumulation should be corrected before continuous operation.
During production, operators should monitor feed rate, web appearance, width, thickness, GSM, temperature, line speed, and winding tension. Any variation should be recorded and compared with the approved process parameters. Production records help identify the causes of defects and support continuous improvement.
8.2 Preventive Maintenance
Preventive maintenance may include lubrication, bearing inspection, belt and chain adjustment, needle replacement, filter cleaning, dust-collector inspection, electrical cabinet cleaning, sensor verification, heater inspection, and calibration of temperature or pressure instruments.
Opening components and air ducts should be checked for wear and fiber accumulation. Needle-punching elements require special attention because damaged or worn needles can affect web appearance, strength, and thickness. Thermal equipment should be inspected for uniform heating and safe operation.
8.3 Product Inspection
Finished felt should be inspected against the customer’s specification. Basic checks may include width, length, GSM, thickness, color, surface uniformity, edge condition, moisture, and roll appearance. Performance tests depend on the product application.
For automotive products, additional checks may include odor, volatile emissions, flammability, acoustic performance, compression recovery, and dimensional stability. For insulation, thermal conductivity and acoustic absorption may be important. For packaging, compression resistance, cushioning behavior, abrasion, and surface protection may be prioritized.
8.4 Process Optimization
Process optimization should be based on measured results rather than visual judgment alone. If GSM is unstable, the manufacturer should examine feeding consistency, air distribution, forming speed, and fiber blend. If thickness varies, the cause may involve web density, reinforcement settings, thermal shrinkage, or winding pressure.
Trial production is recommended whenever the raw material changes significantly. Recycled waste from different suppliers can have different fiber lengths, finishes, moisture levels, and contamination. A recipe that performs well with one waste stream may need adjustment for another.
9. How to Select the Correct Configuration
The first selection factor is the raw material. Buyers should identify whether the line will process natural fiber, cotton, wool, polyester, recycled PET, textile scraps, waste felt, low-melt fiber, or a blend. The material’s average fiber length, maximum fragment size, moisture, contamination, and bulk density should also be documented.
The second factor is the target product. Automotive felt, insulation, packaging felt, and furniture protection materials do not necessarily require the same density, reinforcement, thermal treatment, or cutting method. A clear product specification helps the supplier determine which units are essential and which are optional.
The third factor is output. The stated capacity of 500 to 1,000 kilograms per hour provides a general reference, but actual output depends on GSM and thickness. A heavy 7,500 GSM product will naturally require a different operating condition from a lighter product. Buyers should request capacity estimates based on their actual recipe and product range.
The fourth factor is width. The desired finished width, trim allowance, roll size, downstream cutting format, and factory layout should be considered together. A wider line may increase output but also requires more space, energy, and handling capacity.
The fifth factor is the reinforcement method. Needle punching, thermal bonding, or combined methods may be selected according to the required strength, resilience, softness, surface, and dimensional stability. Where low-melt fibers are used, the thermal bonding section must be designed around their melting behavior.
The sixth factor is automation. Customers should define their expectations for automatic feeding, recipe storage, alarm systems, production data, temperature control, remote support, and integration with downstream machinery. A higher degree of automation may reduce labor requirements and improve repeatability, but it also requires trained personnel and disciplined maintenance.
10. Commercial and Environmental Value
An airlaid waste felt line can create value from materials that were previously treated as waste. Textile scraps and rejected felt may have limited value when sold without processing. After opening, forming, and reinforcement, they can become useful products for industrial and commercial markets.
The economic result depends on raw-material cost, energy consumption, labor, maintenance, product selling price, yield, and market demand. A feasibility study should include realistic assumptions about waste availability and product acceptance. Recycling is most successful when the finished product is designed around a stable market rather than produced without a defined customer requirement.
Environmental benefits may include reduced disposal, increased recycled content, lower dependence on virgin fiber, and more efficient use of industrial resources. These benefits should be measured through an appropriate assessment of material input, energy use, emissions, product life, and end-of-life options.
The use of recycled material does not automatically guarantee environmental superiority in every situation. Dust collection, energy efficiency, product durability, transportation distance, and the source of the waste stream all affect the overall result. The strongest sustainability strategy combines durable products, responsible raw-material preparation, efficient operation, and proper maintenance.
11. Why Work with an Experienced Nonwoven Machinery Manufacturer
A complete production line represents a long-term investment. The supplier’s responsibilities may include process consultation, equipment design, manufacturing, factory testing, delivery, installation guidance, commissioning, operator training, spare-parts support, and after-sales service.
An experienced manufacturer can help the customer avoid common configuration problems, such as insufficient opening capacity, unsuitable air circulation, inadequate dust removal, inappropriate thermal treatment, or a mismatch between line output and downstream handling. The supplier can also help determine whether the proposed raw material is suitable for the intended product.
Changshu Hongyi Nonwoven Machinery Co., Ltd. offers a one-year warranty according to the supplied product information. Warranty conditions, exclusions, response procedures, installation responsibilities, and spare-parts arrangements should be confirmed in the commercial contract.
The company’s ability to supply both complete lines and individual machines may also support future expansion. A customer can begin with one product category and later add a cutting unit, thermal treatment stage, needle-punching section, or additional production line as market demand develops.
12. Questions and Answers
Q1: What materials can the airlaid waste felt production line process?
The line can be configured for natural fiber, cotton fiber, wool, polyester fiber, recycled PET fiber, textile scraps, waste fiber felt, recycled waste fiber, and low-melt fiber. The exact blend depends on the intended product. Raw materials should be sorted and inspected to remove unsuitable contaminants before production.
Q2: What fiber length can be handled?
The stated operating concept is suitable for waste fibers with lengths of approximately 5 to 85 millimeters. Actual performance depends on the fiber type, opening condition, moisture, blend, and equipment settings. Very large fragments or heavily contaminated waste may require additional preparation.
Q3: What is the production capacity?
The stated capacity is approximately 500 to 1,000 kilograms per hour. Actual output depends on working width, GSM, thickness, raw material, reinforcement method, line speed, and finished-product requirements. A capacity evaluation should be based on the customer’s specific material and product samples.
Q4: What GSM range can be produced?
The stated product range is approximately 500 to 7,500 GSM. The achievable range for a particular configuration depends on the equipment arrangement and the desired thickness, density, strength, and surface condition.
Q5: What finished thickness can be achieved?
The stated thickness range is approximately 5 to 200 millimeters. The actual result depends on web bulk, fiber blend, reinforcement, thermal treatment, compression, and winding or cutting conditions.
Q6: Can the working width be customized?
Yes. The supplied information identifies a working-width range of approximately 1,500 to 2,800 millimeters. The final width should be selected according to the product size, factory layout, output target, and downstream equipment.
Q7: Is the line suitable for automotive felt?
Yes. The line is intended for automotive interior felts and can be configured for products such as trunk liners, acoustic layers, cushioning components, and protective interior materials. Automotive specifications may require additional testing for odor, emissions, flammability, mechanical performance, and dimensional stability.
Q8: Does the line use carding technology?
The production concept uses airlaid web forming rather than relying on a traditional carding process as the primary forming method. This helps broaden the range of waste fibers that can be processed and supports the recycling of short or mixed fibers.
Q9: Can low-melt fiber be used?
Low-melt fiber can be included where thermal bonding is required. The thermal bonding temperature, line speed, residence time, and blend ratio must be developed according to the specific low-melt fiber and the required product performance.
Q10: Is the line automatic?
The product information identifies the equipment as automatic. The specific automation level, control functions, sensors, recipe management, alarms, and data systems should be confirmed in the technical proposal for the selected configuration.
Q11: What should be prepared before requesting a quotation?
The buyer should prepare information about raw material type, fiber length, moisture, contamination, blend ratio, desired GSM, thickness, working width, target output, reinforcement method, finished-product format, available factory space, power supply, and required certifications. Samples of raw material and finished products are also helpful.
Q12: What after-sales service is provided?
The supplied information states a one-year warranty. Depending on the project, support may include technical documentation, installation guidance, commissioning assistance, operator training, spare-parts recommendations, and troubleshooting. The specific service scope should be written into the purchase agreement.
13. Conclusion
The airlaid waste felt production line provides a practical solution for converting diverse fiber waste into valuable nonwoven products. Its central advantage is flexibility: it can process natural fibers, cotton, wool, polyester, recycled PET, textile scraps, waste felt, and low-melt fibers while supporting a broad range of GSM values and finished thicknesses.
By integrating waste opening, dust removal, airlaid web forming, reinforcement, thermal treatment, and finished-product handling, the system provides a complete route from recycled raw material to industrial felt. Compared with a production approach that depends heavily on uniform virgin fibers and traditional carding, airlaid technology can reduce raw-material limitations, support mixed-fiber recipes, and improve the commercial potential of waste recycling.
The HYL line is suitable for automotive interior materials, thermal and acoustic insulation, packaging, furniture protection, construction products, and other heavy nonwoven applications. Its customizable working width, automatic operation, broad product range, and adaptable configuration make it suitable for different manufacturing scales.
Changshu Hongyi Nonwoven Machinery Co., Ltd. combines more than 20 years of nonwoven machinery experience with a portfolio covering complete production lines and individual machines. Its focus on customized engineering, automation, energy efficiency, international supply, quality management, and after-sales support gives customers a foundation for building reliable and expandable nonwoven manufacturing operations.
Before investment, buyers should validate the raw material, product specification, output target, factory layout, utilities, environmental requirements, and testing standards. With suitable process design and disciplined operation, an airlaid waste felt line can support both profitable product development and more responsible use of textile resources.
References
1. Product specification information for the HYL Airlaid Waste Felt Production Line, including working width, capacity, GSM range, thickness range, raw materials, and configuration options.
2. Technical information supplied by Changshu Hongyi Nonwoven Machinery Co., Ltd. regarding airlaid waste felt production, nonwoven machinery, customization, automation, and after-sales service.
3. International Organization for Standardization. ISO 9001, Quality Management Systems—Requirements.
4. European conformity assessment principles applicable to industrial machinery and production equipment.
5. General technical literature on airlaid nonwoven web formation, fiber opening, pneumatic fiber distribution, needle punching, and thermal bonding.
6. General industry guidance on recycled textile fibers, recycled polyester, nonwoven insulation materials, automotive interior felts, and protective packaging products.
7. General maintenance and safety practices for fiber-opening machinery, dust-collection systems, needle-punching equipment, thermal bonding ovens, winding systems, and cutting equipment.