

Content
- 1 1. The Role of Carding in Nonwoven Production
- 2 2. Product Overview
- 3 3. Main Structural Design
- 4 4. Performance Advantages Compared with Basic Carding Equipment
- 5 5. Manufacturing Strengths and Engineering Capabilities
- 6 6. Application Areas
- 7 7. Process Integration
- 8 8. Installation, Operation, and Maintenance Considerations
- 9 9. Quality Control and Manufacturing Process
- 10 10. Why Choose a Specialized Nonwoven Machinery Manufacturer?
- 11 11. Selecting the Correct Configuration
- 12 12. Sustainable and Economic Benefits
- 13 13. Q&A
- 13.1 Q1. What is the main function of the HYSL Carding Machine?
- 13.2 Q2. Which fibers can the machine process?
- 13.3 Q3. Is the machine available with different working widths?
- 13.4 Q4. Can customers choose single-cylinder or double-cylinder construction?
- 13.5 Q5. Does the machine support double doffers?
- 13.6 Q6. Can the machine produce a random fiber web?
- 13.7 Q7. What safety protection is included?
- 13.8 Q8. How does the anti-metal protection system work?
- 13.9 Q9. What are the main cylinder and roller dimensions?
- 13.10 Q10. What production capacity can be expected?
- 13.11 Q11. What is the maximum operating speed?
- 13.12 Q12. Can the machine be integrated into a needle-punching line?
- 13.13 Q13. Is the electrical system customizable?
- 13.14 Q14. What kind of maintenance does the machine require?
- 13.15 Q15. Does the manufacturer provide after-sales support?
- 13.16 Q16. How long is the delivery period?
- 13.17 Q17. What information should be included in an inquiry?
- 14 14. Conclusion
- 15 References
- 16 Product: HYSL Carding Machine
Carding is one of the most important stages in nonwoven fabric production. It determines how opened fibers are separated, aligned, distributed, and delivered to the following process. A stable carding operation directly influences web uniformity, fabric strength, thickness consistency, appearance, and the overall efficiency of a production line. The HYSL Carding Machine is designed to provide controlled, high-quality fiber carding for needle-punched, thermal-bonded, quilting, automotive, filtration, bedding, geotextile, carpet, and other nonwoven applications.
Developed by Changshu Hongyi Nonwoven Machinery Co., Ltd., the HYSL series combines a robust mechanical structure, variable-speed drives, automatic safety functions, flexible working widths, and configurable cylinder and doffer arrangements. The machine can be supplied in single-cylinder or double-cylinder configurations, with single or double doffers and optional randomizer rollers. This flexibility enables the equipment to be adapted to different fiber types, web structures, production targets, and downstream processes.
Unlike a basic carding unit that only opens and distributes fiber, the HYSL Carding Machine is engineered as a complete fiber-web preparation system. Its feeding section, anti-metal protection, carding units, stripping rollers, doffer section, edge-suction system, drive controls, safety guards, and maintenance platforms work together to provide stable and repeatable operation. The result is a controlled fiber web that can be transferred efficiently to a cross-lapper, needle punching machine, thermal bonding oven, quilting machine, or other subsequent equipment.
1. The Role of Carding in Nonwoven Production
Raw staple fibers generally arrive in compressed bales or fiber packages. Before carding, the material must pass through opening and blending equipment to loosen compacted fibers, remove a portion of impurities, and create a reasonably uniform fiber mixture. The carding machine then performs the more precise task of separating fibers and arranging them into a web.
During carding, fibers pass through working rollers, stripping rollers, and the main cylinder. Carding wire surfaces engage with the fibers and progressively separate them. Depending on the wire direction, roller speed, roller spacing, and machine configuration, fibers may be aligned predominantly in the machine direction or distributed in a more random arrangement. The web is then transferred by the doffer to the next stage.
A well-designed carding machine must achieve several objectives simultaneously. It must provide sufficient carding intensity without damaging the fibers, maintain a stable feed rate, prevent excessive fiber accumulation, reduce the risk of metal-related damage, and synchronize its speed with the rest of the production line. It must also be practical to operate and maintain because carding equipment contains numerous rotating components and precision surfaces.
The HYSL Carding Machine addresses these requirements through a combination of mechanical accuracy, electronic control, adaptable configuration, and protective systems. It can be integrated into complete production lines or supplied as an individual machine for upgrading an existing process.
2. Product Overview
The HYSL Carding Machine is an automatic carding system for processing polyester fiber, polypropylene staple fiber, wool, hemp, waste fiber, low-melt fiber, and other suitable materials. Depending on the model and process design, the equipment is available in working widths including approximately 1.55 meters, 1.85 meters, 2 meters, 2.5 meters, and 2.8 meters. Other dimensions may be evaluated according to the customer’s material, output, and factory requirements.
The reference HYSL-230 configuration has an effective working width of approximately 2,300 millimeters. Its standard structural description includes a single main cylinder and double doffer arrangement, five carding groups, a main cylinder diameter of approximately 1,230 millimeters, working rollers with a diameter of approximately 165 millimeters, and stripping rollers with a diameter of approximately 78 millimeters.
Depending on the selected design and material conditions, maximum production figures may reach several hundred kilograms per hour. Published equipment data includes output levels ranging from approximately 600 to 800 kilograms per hour for certain configurations, while actual production depends on fiber type, web weight, feed uniformity, carding intensity, working width, line speed, and the requirements of the final product.
For the same reason, machine speed should be treated as a configuration value rather than a universal operating guarantee. Various product descriptions refer to output speeds below 80 meters per minute, maximum speeds around 70 or 100 meters per minute, and higher production-line transport figures. The final operating speed is selected during technical design and commissioning to match the required web quality and the complete line synchronization.
| Item | Reference Specification |
| Machine model | HYSL series; reference model HYSL-230 |
| Machine function | Fiber carding and web formation |
| Working widths | Approximately 1.55 m, 1.85 m, 2.0 m, 2.5 m, and 2.8 m |
| Reference effective width | 2,300 mm |
| Machine structure | Single-cylinder or double-cylinder; single or double doffer options |
| Main cylinder diameter | Approximately 1,230 mm |
| Breast cylinder diameter | Approximately 850 mm where fitted |
| Working roller diameter | Approximately 165 mm |
| Stripping roller diameter | Approximately 78 mm |
| Number of carding groups | Five groups in the reference configuration |
| Suitable fiber | Polyester, PP, wool, hemp, waste fiber, low-melt fiber, and other compatible materials |
| Control method | Servo-motor or inverter-based drive control |
| Safety features | Transparent guards, electronic safety system, automatic stop alarm, and anti-metal protection |
| Certification information | CE and ISO 9001-related manufacturing quality documentation |
All technical values should be confirmed against the final quotation and process specification. Fiber length, denier, blend ratio, target web weight, downstream equipment, and required production rate all influence the final machine configuration.
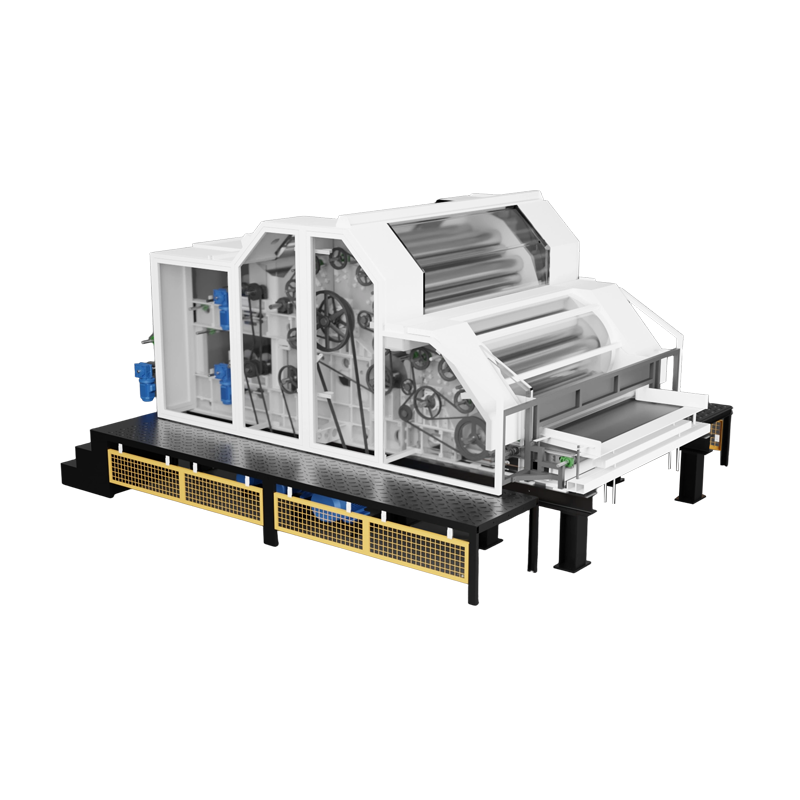
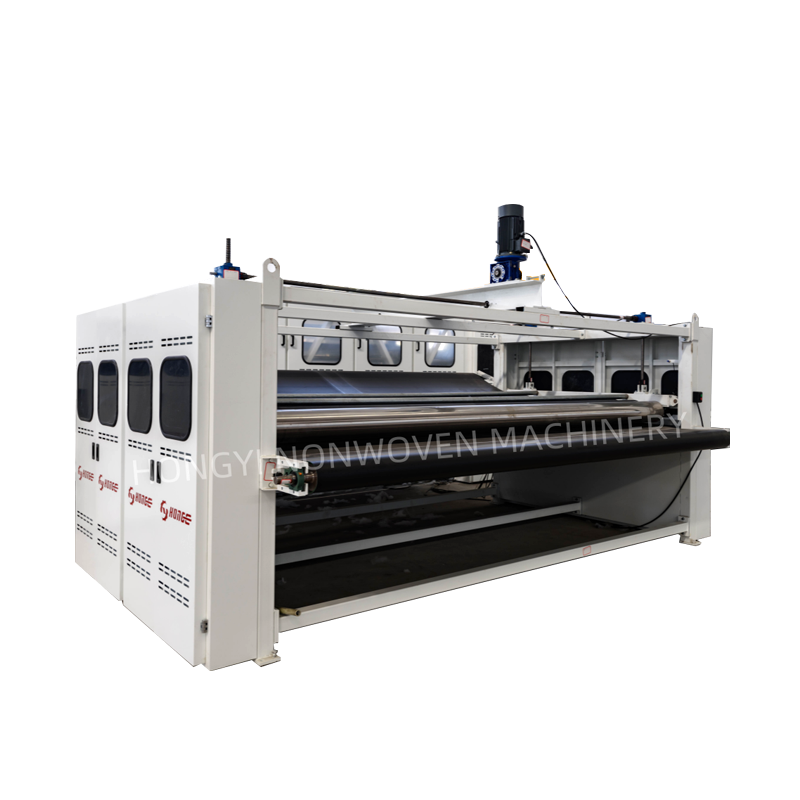
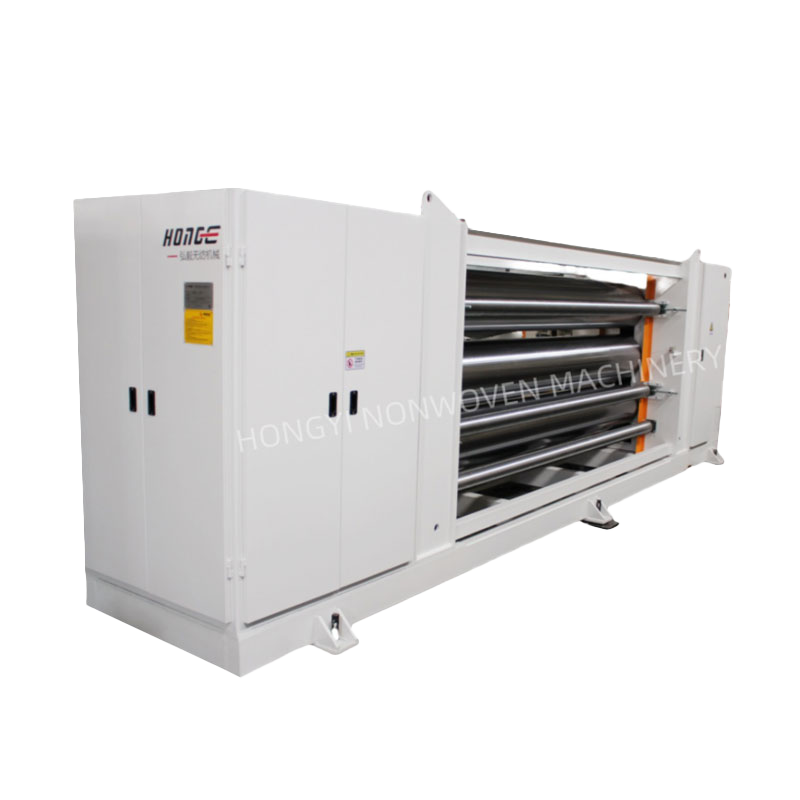
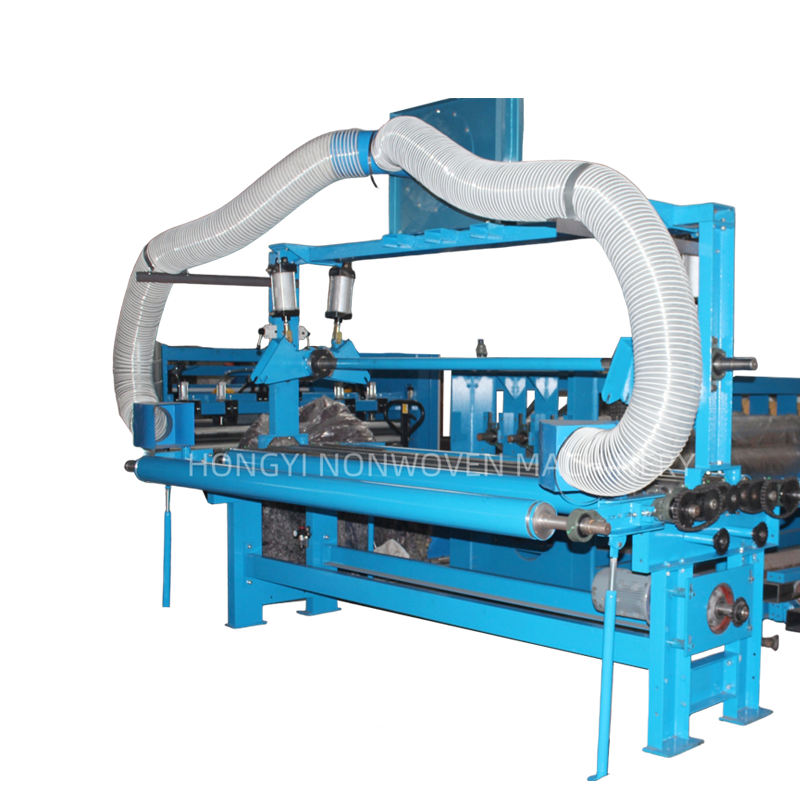
HYSL Carding Machine
3. Main Structural Design
3.1 Horizontal Feeding Lattice
The feeding section uses a horizontal PVC lattice to deliver the opened and blended fiber batt into the carding area. A pressing roller is installed to help control the incoming material and distribute it evenly across the working width. Uniform feeding is essential because irregular fiber loading can create transverse weight variation, weak areas, thick spots, and unstable carding conditions.
The feeding lattice is designed to work continuously with the upstream opening and blending equipment. Its speed can be adjusted according to the amount and type of fiber being supplied. By coordinating the feed speed with the main cylinder and doffer speeds, operators can improve web consistency while reducing unnecessary recirculation or fiber buildup.
3.2 Four-Roller Feeding System
The machine includes a four-roller feeding arrangement. The rollers help grip, compress, and guide the fiber batt before it enters the main carding zone. According to the supplied specifications, the feeding rollers have a diameter of approximately 90 millimeters. The multi-roller design supports more stable material control than a simple single-feed arrangement, especially when the incoming batt varies slightly in density.
The feeding section also includes anti-metal protection. A metal detection device is positioned near the input area to identify metallic objects that could damage carding wire or rotating components. When metal is detected, the machine can issue an alarm and stop automatically. This protective function is particularly valuable when processing recycled fiber, waste fiber, or material that may have been exposed to contaminated handling environments.
3.3 Main Cylinder and Carding Groups
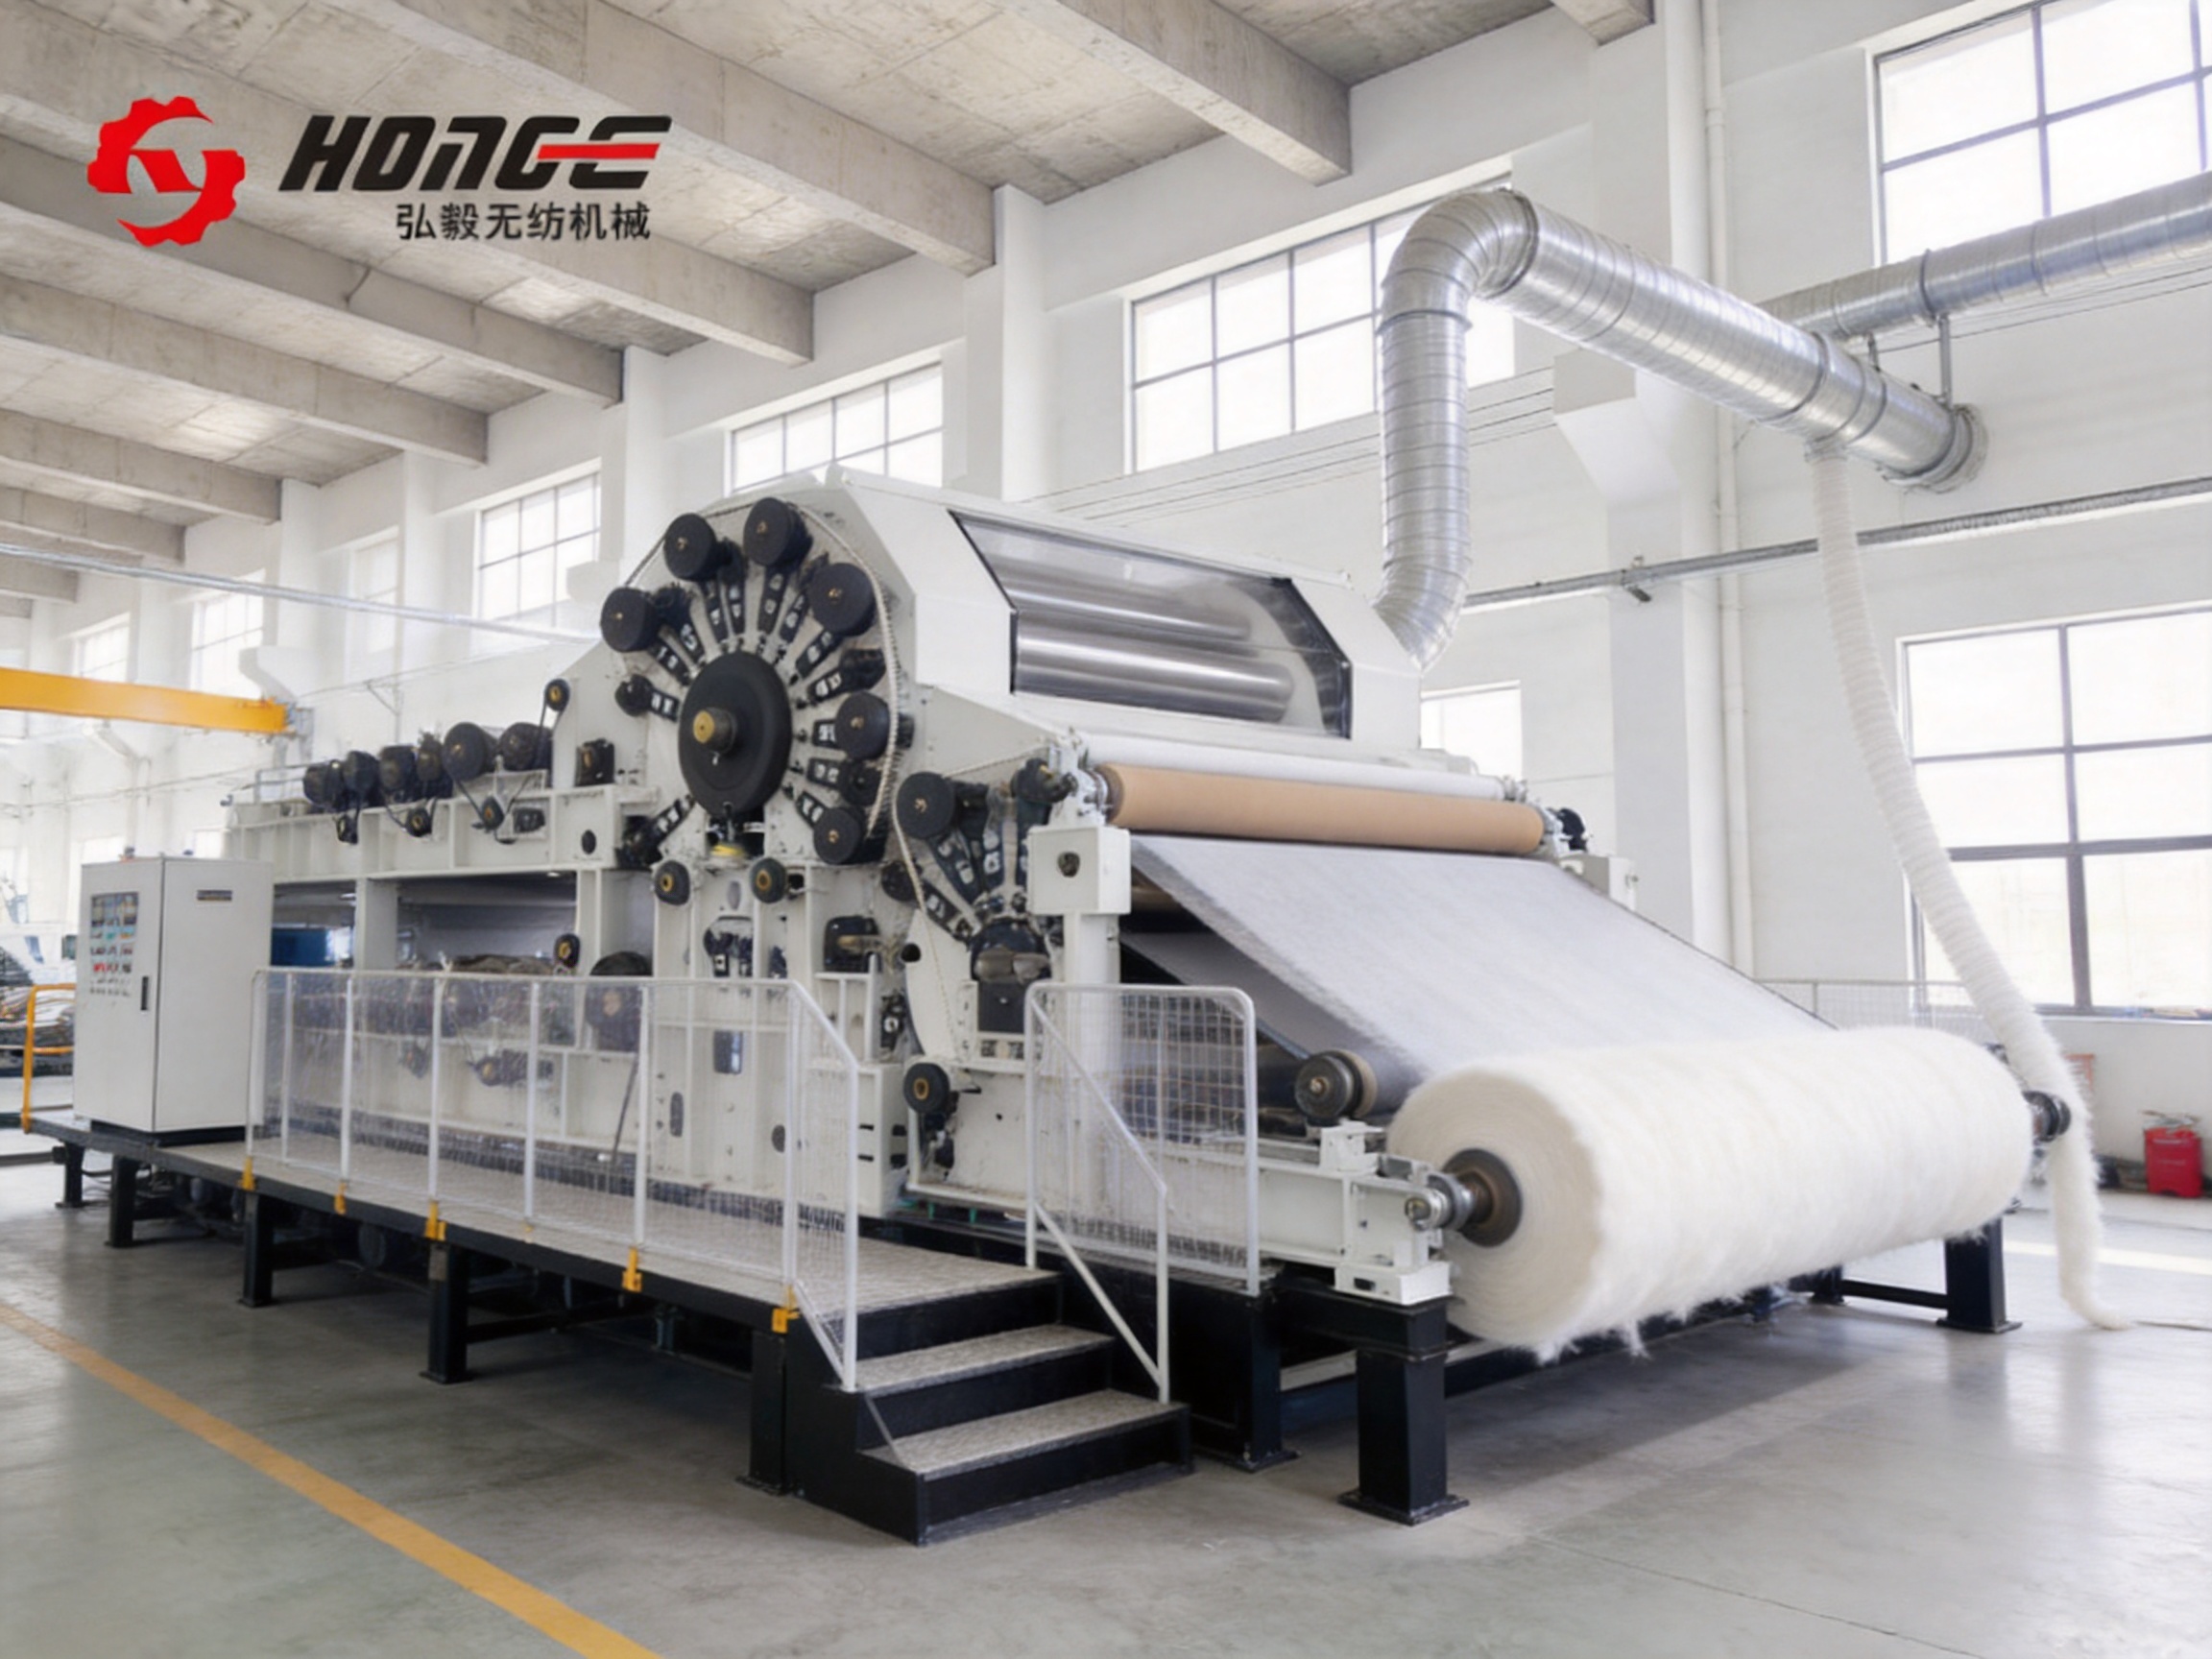
The main cylinder is the central working component of the machine. In the reference HYSL-230 design, the main cylinder has a diameter of approximately 1,230 millimeters. Its large diameter provides a substantial carding surface and supports progressive treatment of the fiber as it passes through multiple working and stripping roller groups.
Five carding groups are included in the reference structure. Each group consists of working and stripping rollers that cooperate with the main cylinder. The working rollers engage the fiber and separate or align it, while the stripping rollers transfer controlled quantities of fiber back toward the main cylinder or onward through the carding path. This staged treatment allows the machine to achieve more complete carding than a limited single-point carding arrangement.
The number of working units and the arrangement of the rollers can be selected according to the desired web characteristics. Fine, uniform webs may require a different setting from bulky wadding or heavy geotextile webs. Technical staff can evaluate the fiber properties and final product requirements before recommending the appropriate configuration.
3.4 Doffer Section
The doffer removes the formed fiber web from the main cylinder and transfers it toward the next process. The HYSL series can be supplied with single or double doffers. A double-doffer arrangement can be useful where higher transfer capacity, improved web collection, or a specific web formation effect is required.
The doffer speed is independently controllable and can be synchronized with the main cylinder, feeding system, cross-lapper, or other downstream equipment. This allows operators to adjust web density and fiber presentation without making unnecessary mechanical changes. Doffer selection and speed are important factors in achieving the desired degree of longitudinal orientation or random distribution.
3.5 Optional Randomizer Rollers
Some nonwoven products require a more random fiber arrangement to reduce excessive machine-direction orientation. The HYSL Carding Machine can be fitted with randomizer rollers when required. These components help modify fiber distribution before the web is delivered to the next process.
Randomization is especially relevant for needle-punched felts, geotextiles, automotive materials, filtration media, and other products where balanced properties in the machine and cross directions are important. The appropriate randomizer design depends on the fiber type, target basis weight, line speed, and the required tensile or tear performance.
3.6 Edge-Suction and Dust Collection
An edge-suction system is installed to remove loose fibers, dust particles, and waste accumulated near the edges of the carding zone. The removed material is transferred to a dedicated dust cage or collection system. This helps maintain a cleaner working environment and reduces the risk of fiber deposits interfering with rollers, wire surfaces, or machine sensors.
Edge suction also helps improve web edge control. Excess loose fiber near the edges can create uneven thickness or unwanted edge buildup. By managing this material continuously, the machine supports more stable web formation and simplifies cleaning around the operating area.
3.7 Maintenance Platforms and Transparent Guards
Walking platforms are provided on both sides of the machine to support inspection, cleaning, adjustment, and routine maintenance. Carding machines require regular attention to wire condition, roller surfaces, suction paths, bearings, drive components, and safety devices. Properly positioned platforms allow technicians to reach service points more safely and efficiently.
Transparent organic-glass safety covers provide visibility of major operating areas while separating personnel from moving parts. Operators can observe fiber flow and machine conditions without opening the guards during normal operation. The complete electronic safety system is designed to support compliance with applicable international machine-safety expectations, subject to the final installation and local regulatory requirements.
4. Performance Advantages Compared with Basic Carding Equipment
4.1 More Complete Fiber Separation
A basic carding machine may have a limited number of working points, which can restrict its ability to separate and distribute difficult fibers. The HYSL structure uses multiple carding groups to treat the material progressively. This increases the opportunity for fiber tufts to be opened and redistributed before the web reaches the doffer.
More complete separation can improve web appearance, reduce visible fiber lumps, and support more consistent bonding or needle penetration in subsequent processes. The exact result depends on the raw material and settings, but the multi-stage structure provides a broader adjustment range than a simple carding arrangement.
4.2 Flexible Single- and Double-Cylinder Designs
Different nonwoven products require different levels of carding intensity and production capacity. The availability of single-cylinder and double-cylinder configurations allows the equipment to be matched more closely to the customer’s process. A single-cylinder machine may be appropriate for applications with moderate carding requirements or limited floor space. A double-cylinder design can provide additional carding capacity for demanding materials or higher production targets.
This modular approach can be more economical than purchasing an oversized machine for every application. Customers can select a design that corresponds to their present requirements while preserving the possibility of process customization.
4.3 Adjustable Fiber Orientation
Fiber orientation has a major influence on the mechanical behavior of nonwoven fabric. Strong machine-direction alignment may be useful for certain products, while more random distribution may be needed for balanced tensile strength, dimensional stability, and isotropic performance. The HYSL series supports this adjustment through doffer selection, speed control, and optional randomizer rollers.
In contrast, less adaptable carding equipment may produce a fixed web structure that limits the range of downstream products. The HYSL configuration gives manufacturers greater freedom to develop several product types on one platform.
4.4 Variable-Speed Drives Throughout the Machine
Main-cylinder speed, doffer speed, working-roller speed, stripping-roller speed, and feeding-roller speed can be controlled according to the selected system design. Servo-motor or inverter-based drive systems enable gradual acceleration, controlled deceleration, and coordinated operating speeds.
Variable-speed control provides several advantages. It helps operators adapt the machine to different fiber deniers and lengths, control the degree of carding, reduce mechanical shock during startup, and coordinate the carder with other machines. It also supports stable line synchronization, which is important in a complete nonwoven production line where one machine’s output becomes another machine’s input.
4.5 Protection of Carding Wire
Carding wire is a precision working surface and one of the most important consumable or service components in the machine. Damage to the wire can reduce carding quality, increase maintenance costs, and create production downtime. The HYSL Carding Machine includes an anti-metal detection system and a protective arrangement intended to minimize the risk of hard foreign objects reaching the carding rollers.
The machine is also designed with a system that helps minimize fiber wrapping around rollers. Excessive fiber wrapping can create unbalanced rotation, heat generation, web defects, and difficult cleaning conditions. Reducing roller wrapping helps protect both the wire and the mechanical drive system.
4.6 Stable Operation at Different Working Widths
Manufacturers of nonwoven products often serve several markets and may need more than one fabric width. The HYSL series is available in multiple working widths, allowing the equipment to be selected for narrow, medium, or wide web production. A range that extends to approximately 2.8 meters supports applications such as geotextiles, industrial felt, carpet backing, bedding materials, and automotive textiles.
Working width should always be selected together with target basis weight and output. A wider machine is not automatically more productive if the fiber feed system, carding intensity, downstream equipment, or raw-material preparation cannot support it. The manufacturer’s engineering team can assess the complete process instead of selecting the carding width in isolation.
5. Manufacturing Strengths and Engineering Capabilities
Changshu Hongyi Nonwoven Machinery Co., Ltd. has more than 20 years of experience in the nonwoven machinery field. Its product range includes complete production lines and individual machines for needle-punched geotextiles, nonwoven carpets, airlaid waste felt, automotive interior materials, cleaning cloth, wool felt, jute felt, thermal-bonded wadding, and related products.
This broad product experience is important when manufacturing a carding machine because carding performance cannot be judged separately from the rest of the line. A carder designed for a lightweight thermal-bonded wadding process may require different settings from one designed for heavy needle-punched geotextile. Experience with complete lines enables the manufacturer to consider opening, blending, carding, cross-lapping, needling, thermal bonding, winding, cutting, and inspection as interconnected operations.
5.1 Precision-Balanced Rotating Components
The main cylinders and large rollers are precisely balanced before assembly. This manufacturing step is essential because carding machines operate with large rotating components at controlled speed. Poor balance can create vibration, bearing stress, uneven wire clearance, noise, and premature wear.
Precision balancing supports smoother operation and helps maintain the roller alignment required for consistent carding. It also contributes to operator comfort and equipment longevity. For wide machines, balancing becomes even more important because the weight and rotational inertia of the cylinder increase significantly.
5.2 Quality Carding Wire
The carding wire can be supplied as surface-wound or interlocking wire according to the customer’s needs. The supplied product information identifies high-quality wire from GERON as an available option. Wire selection affects fiber engagement, carding intensity, material transfer, cleaning behavior, and service life.
Different raw materials may require different wire specifications. Fine polyester fibers, coarse natural fibers, recycled fibers, and low-melt fibers do not behave identically. The choice should therefore be based on fiber denier, staple length, crimp, blend ratio, moisture, target web weight, and the desired degree of orientation.
5.3 Integrated Control Engineering
The control system can use servo motors or inverter drives. Both approaches allow variable-speed operation, while the final choice depends on the customer’s control philosophy, line architecture, precision requirements, and budget. The objective is to maintain controlled and stable starting, stopping, acceleration, and production synchronization.
An integrated control system can also provide alarm signals for abnormal conditions such as metal detection, guard opening, overload, emergency stop activation, or other safety-related events. The exact human-machine interface and communication functions can be customized during the engineering stage.
5.4 Custom Engineering Rather Than One-Size-Fits-All Supply
The company accepts customized requirements for working width, machine configuration, electrical voltage, control method, fiber type, output target, and downstream connection. This is a significant advantage for customers who have specific process conditions or who are expanding an existing production line.
Technical customization may include the selection of single or double cylinders, doffer quantity, randomizer rollers, feeding arrangement, dust-removal connection, safety layout, and control interfaces. The manufacturer can also discuss the relationship between the carding machine and cross-lapper, needle loom, thermal bonding oven, or winding system.
5.5 International Production and Service Experience
The company reports that its equipment has been supplied to more than 20 countries, including markets in Latin America, the Middle East, North Africa, Southeast Asia, and other regions. International project experience requires attention to different power standards, factory layouts, shipping conditions, documentation requirements, operator training, and after-sales support.
The standard information includes CE and ISO 9001-related certification references, video outgoing inspection, and a one-year warranty. Actual warranty scope, commissioning arrangements, spare parts, installation support, and training should be confirmed in the commercial contract.
6. Application Areas
6.1 Needle-Punched Geotextiles
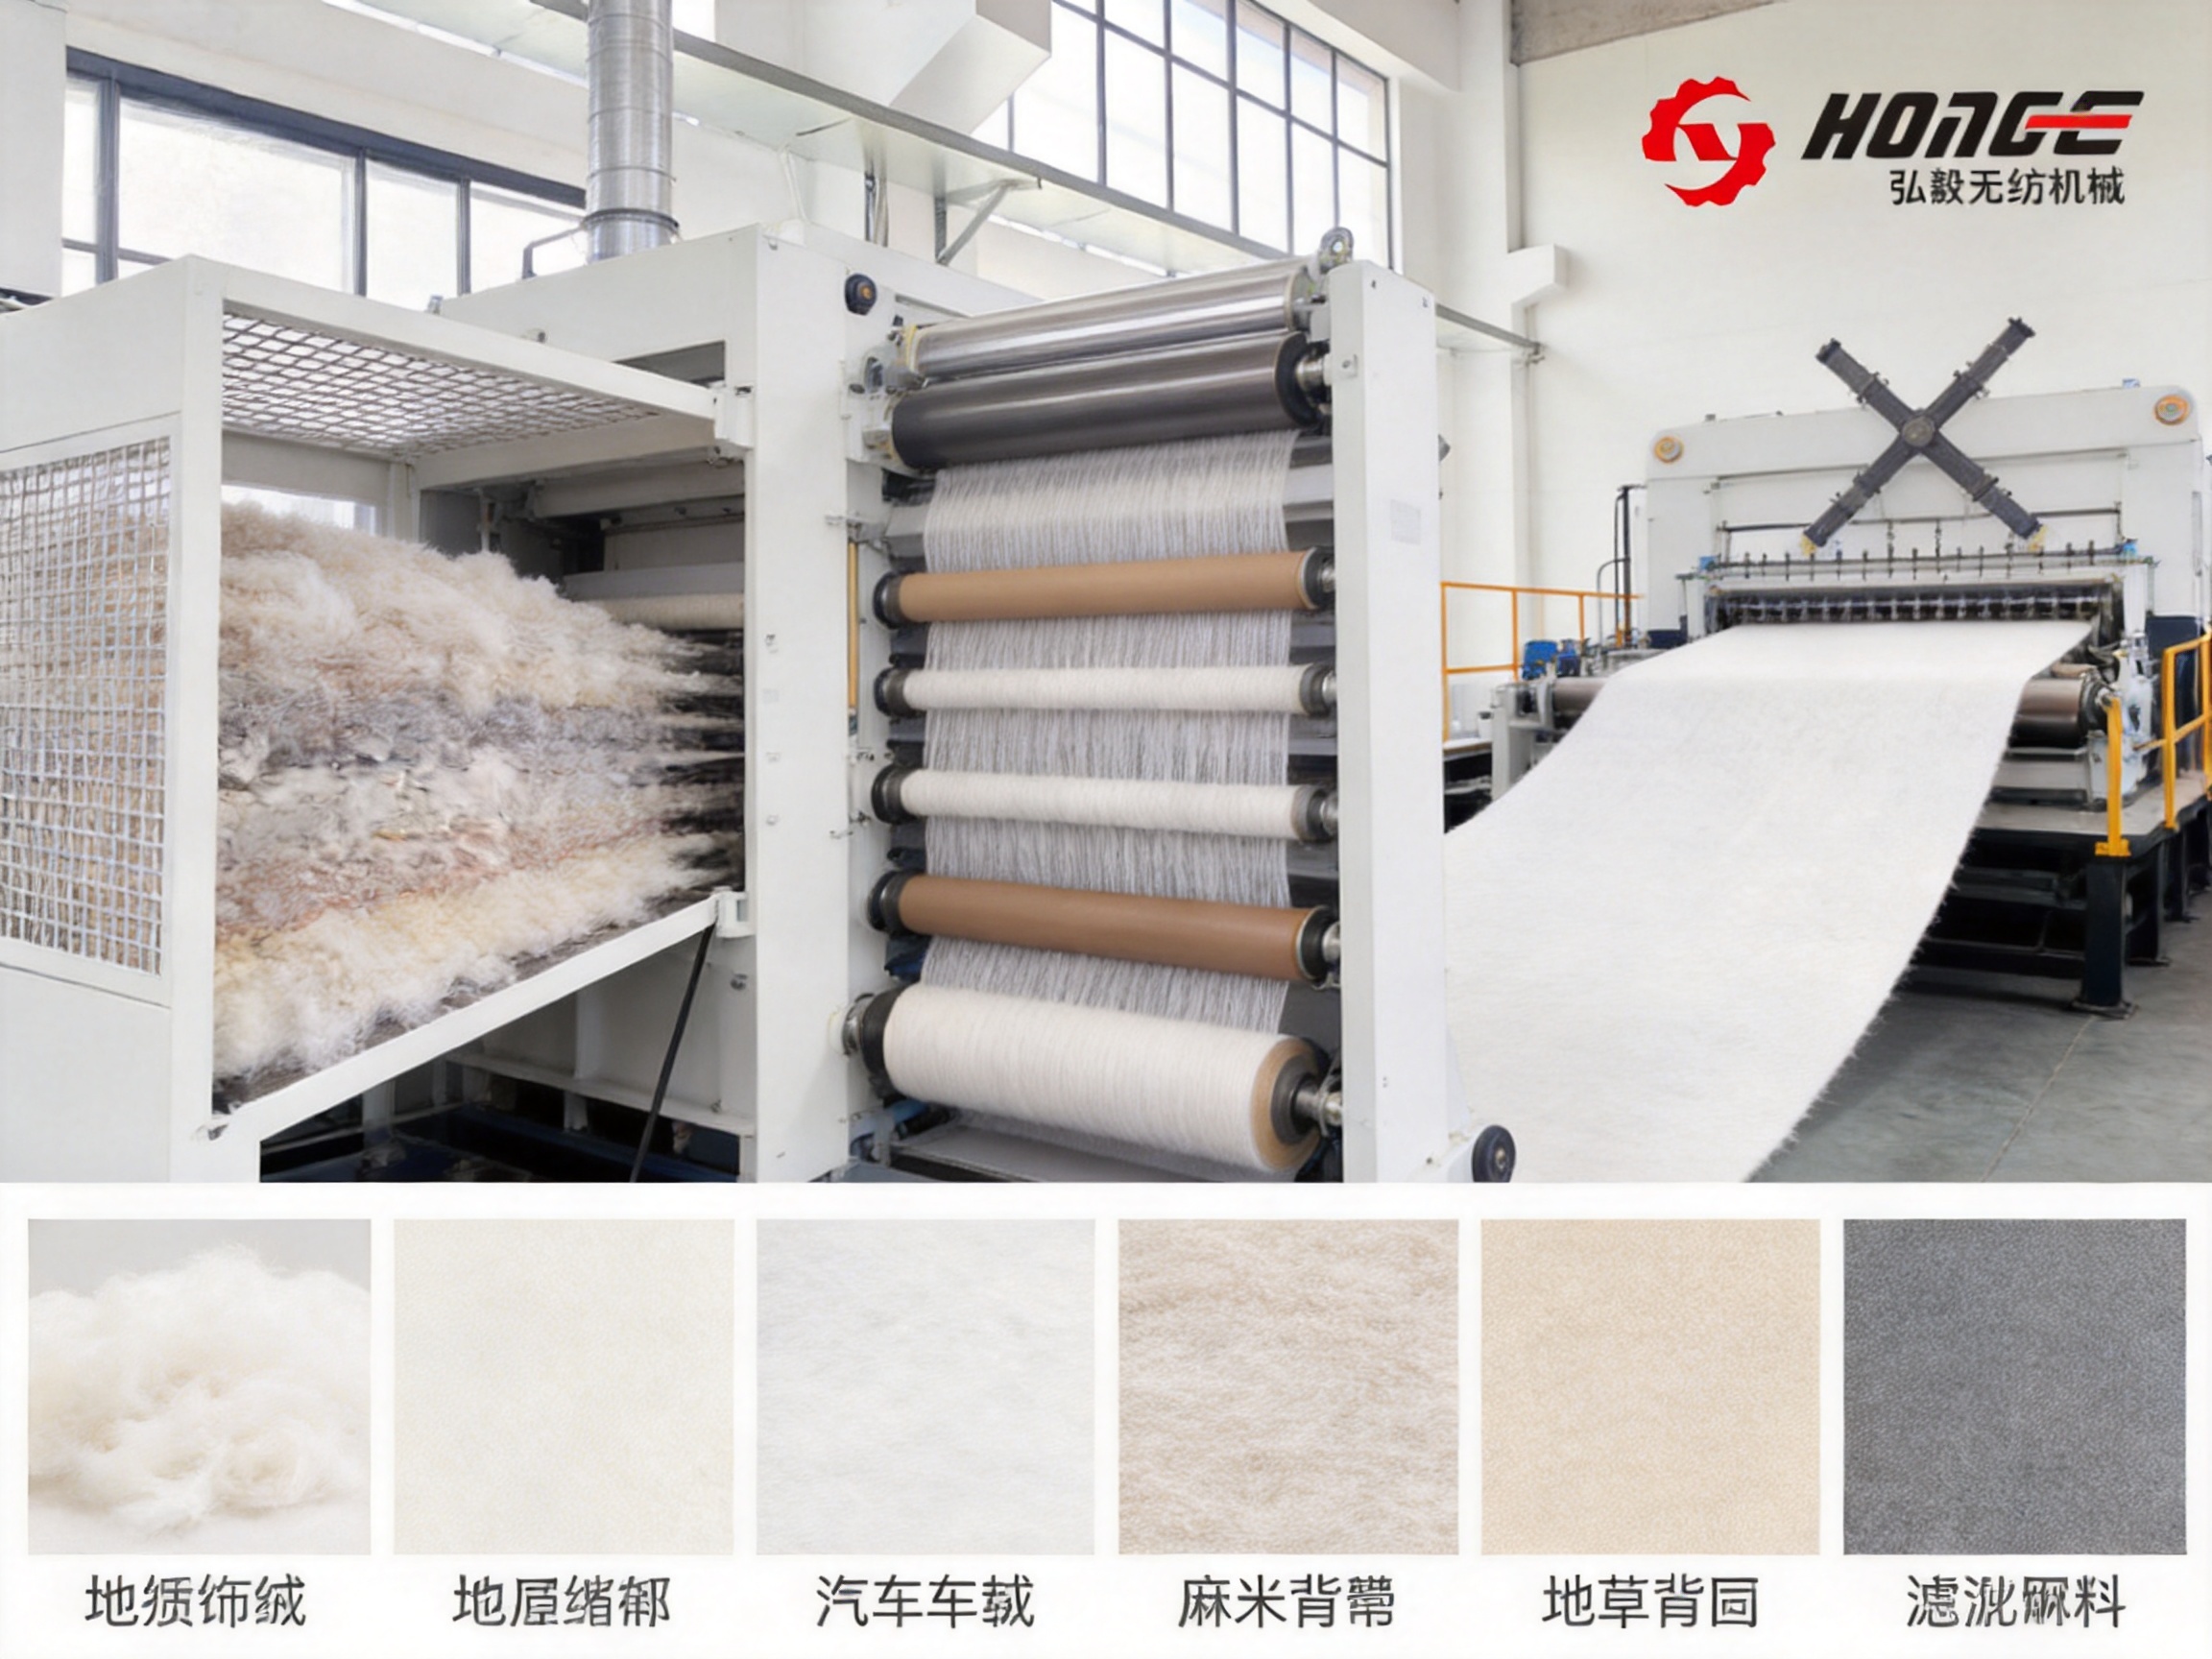
Geotextile production requires stable fiber distribution and reliable web formation because the final material may be used for drainage, filtration, separation, reinforcement, erosion control, or road construction. The HYSL Carding Machine can prepare fiber webs for subsequent cross-lapping and needle punching. Randomizer options may be selected when balanced properties are required in both principal directions.
6.2 Nonwoven Carpets and Floor Coverings
Carpet backing and felted floor materials often require high web uniformity, adequate bulk, and consistent fiber distribution across a wide working width. The machine’s multiple carding groups and controlled doffer section can support the preparation of webs for needle punching or thermal bonding.
6.3 Thermal-Bonded Wadding
Thermal-bonded wadding uses heat-sensitive fibers, often including low-melt fiber blends. The carding machine must distribute the blend evenly so that the final material bonds consistently when passing through a thermal oven. Uneven low-melt fiber distribution can cause hard spots, weak areas, or irregular thickness. Careful control of feed, carding, and doffer speeds is therefore important.
6.4 Automotive Interior Materials
Automotive interior products may include trunk liners, acoustic materials, insulation layers, wheel-arch coverings, and interior felt components. These applications often require stable basis weight, controlled bulk, low defect rates, and repeatable production. The machine can be integrated into lines that include cross-lapping, needle punching, thermal bonding, or composite processing.
6.5 Bedding and Mattress Materials
Wadding for mattresses, quilts, cushions, and other bedding products must provide even thickness and soft, consistent fiber distribution. Polyester fiber, hollow fiber, conjugate fiber, and low-melt blends may be processed depending on the final structure. The adjustable carding system allows manufacturers to develop different product weights and hand-feel characteristics.
6.6 Wool, Hemp, Jute, and Natural Fibers
Natural fibers can vary in length, fineness, moisture, and surface characteristics. They may also require gentler or more carefully adjusted carding than uniform synthetic fibers. The HYSL series can be evaluated for wool, hemp, jute, and related materials, with the final wire selection, speed, roller settings, and dust-removal requirements determined by testing.
6.7 Recycled and Waste Fiber
Recycled and waste fibers are increasingly used in nonwoven manufacturing, but they may contain more variation and a greater risk of foreign objects. The anti-metal detection system is especially useful in this application. Upstream sorting and opening remain necessary, but carding-stage protection adds an important layer of equipment security.
7. Process Integration
The HYSL Carding Machine is normally installed after opening and blending equipment. The upstream system prepares the fiber by loosening compressed bales and creating a blended feed. The carder then separates and distributes the fiber. After carding, the web may be transferred directly to a cross-lapper, needle punching machine, thermal bonding oven, quilting line, winding unit, or cutting machine.
In a needle-punched line, carded webs may pass through one or more cross-lapping stages before entering the needle loom. The carding machine affects the quality of the initial web and therefore influences lapping stability, needle penetration, thickness distribution, and final fabric strength.
In a thermal-bonded line, the carder must provide a uniform blend of bonding and structural fibers. The oven then melts or softens the bonding component to consolidate the web. Consistent carding supports even thermal bonding and reduces variation in finished thickness.
In an airlay or composite line, the carded web may be combined with other fiber layers, films, scrims, or recycled materials. Accurate web formation is important when multiple layers must be bonded or needled together.
| Production Stage | Primary Function | Relationship to Carding |
| Opening and blending | Loosens, blends, and prepares fiber | Provides a consistent batt to the feeding lattice |
| Feeding | Controls the quantity and distribution of incoming fiber | Determines the stability of carding load |
| Carding | Separates, aligns, and distributes fibers | Creates the primary web structure |
| Randomizing or doffing | Adjusts orientation and transfers the web | Controls web delivery and fiber arrangement |
| Cross-lapping | Builds thickness and balances orientation | Receives the carded web for layered formation |
| Needle punching | Entangles fibers mechanically | Consolidates the carded and lapped web |
| Thermal bonding | Uses heat to bond suitable fibers | Requires even distribution of bonding fibers |
| Winding and cutting | Creates finished rolls or cut products | Depends on stable web width and thickness |
8. Installation, Operation, and Maintenance Considerations
Correct installation is essential for carding performance. The foundation must be level and sufficiently rigid to support the machine and limit vibration. The electrical supply must match the approved design, such as 380/220 volts or another customer-specified standard. Adequate space should be provided around the machine for walking platforms, cleaning, maintenance, material flow, and safe access.
Before commissioning, the machine should be checked for mechanical alignment, roller clearance, wire condition, lubrication, electrical connections, emergency stops, safety guards, metal detection, suction connections, and communication with adjacent equipment. The upstream and downstream machines should be tested together rather than independently whenever possible.
Operators should begin with conservative speeds and a moderate fiber feed. The feed rate, main-cylinder speed, working-roller speed, stripping-roller speed, and doffer speed can then be adjusted while monitoring web quality and machine load. Sudden speed changes should be avoided because they may create unstable fiber transfer or mechanical stress.
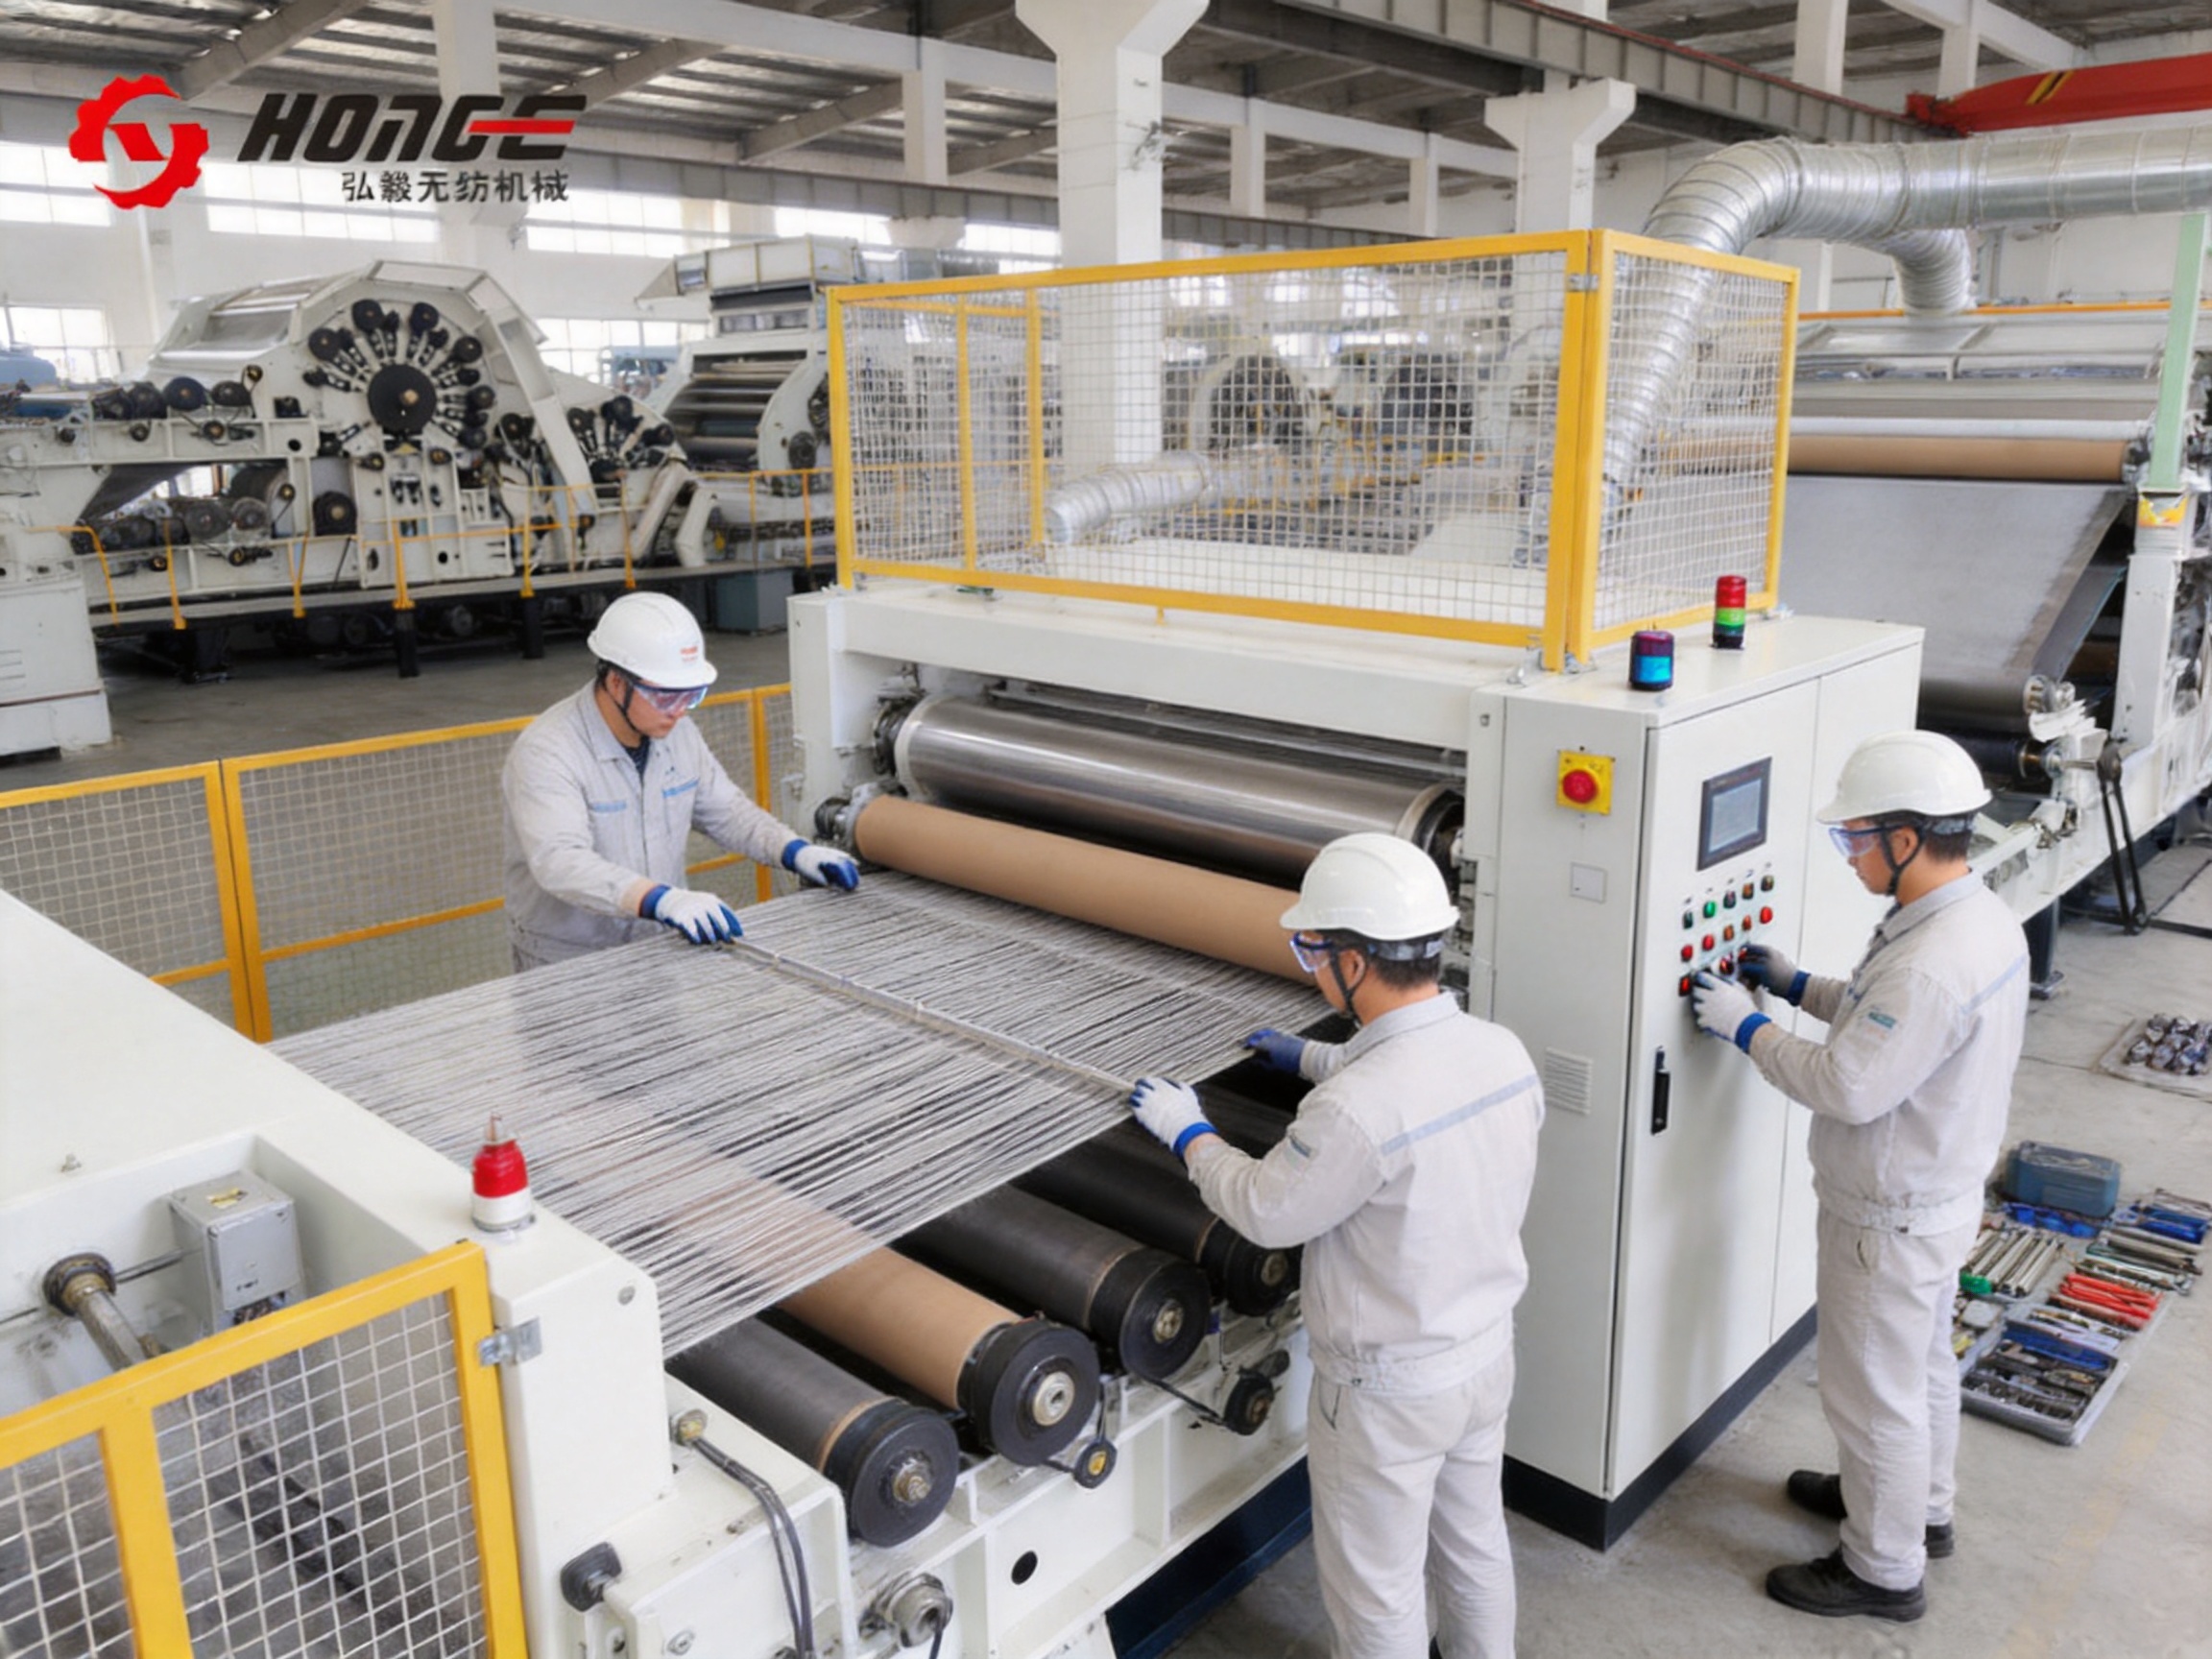
Regular maintenance should include cleaning of fiber deposits, inspection of carding wire, checking of roller surfaces, examination of bearings and drive belts, verification of suction performance, testing of alarms and emergency stops, and inspection of electrical cabinets. The machine should be stopped and isolated according to the applicable lockout and safety procedure before personnel enter guarded areas.
Carding wire should be inspected for wear, bent points, contamination, or damaged sections. The condition of the wire has a direct effect on fiber separation and web quality. A maintenance schedule based on operating hours, fiber type, production rate, and contamination level is more effective than waiting for visible quality defects to appear.
9. Quality Control and Manufacturing Process
A reliable carding machine begins with controlled manufacturing of its frame, rollers, drives, wire components, electrical system, and safety assemblies. The manufacturing process should maintain dimensional accuracy because small deviations in roller parallelism, clearance, or alignment can influence web uniformity across the machine width.
9.1 Structural Fabrication
The frame and supporting structures must be manufactured with sufficient rigidity to resist vibration and maintain alignment. Wide working widths place greater demands on the structure, especially around the main cylinder and doffer section. Welding, machining, surface treatment, and assembly inspection all contribute to the final stability of the equipment.
9.2 Roller Manufacturing and Balancing
Rollers require accurate machining and surface finishing. The main cylinder and other large rollers must be checked for concentricity and balance. Dynamic balancing before final assembly helps reduce vibration during operation and supports the precision clearances required by carding wire.
9.3 Electrical and Control Assembly
Electrical cabinets, variable-frequency drives, servo systems, sensors, emergency circuits, and operator controls should be assembled and tested according to the machine design. The control system must coordinate the feeding, carding, doffing, and downstream equipment. A properly integrated control system improves repeatability and reduces the chance of operator error during startup and shutdown.
9.4 Factory Testing
Before delivery, the machine can undergo inspection and video outgoing inspection. Factory testing may include no-load running, drive testing, alarm verification, safety-guard checks, metal detection tests, roller rotation checks, suction tests, and review of the control sequence. The extent of the test should be agreed during the order process, particularly for complete production lines.
9.5 Customer Acceptance
Customer acceptance should evaluate not only whether the machine runs, but also whether it achieves the agreed process objectives. These may include working width, output, web weight range, speed, fiber blend, safety functions, noise or vibration expectations, and compatibility with the downstream line. A clear acceptance protocol helps both parties manage technical expectations.
10. Why Choose a Specialized Nonwoven Machinery Manufacturer?
A specialized manufacturer understands that the carding machine is part of a production system rather than an isolated mechanical device. This knowledge helps with equipment selection, line layout, process matching, energy planning, installation, operator training, and troubleshooting.
Changshu Hongyi Nonwoven Machinery Co., Ltd. provides both individual machines and complete nonwoven production lines. Its experience across needle-punched, thermal-bonded, airlaid, automotive, carpet, cleaning cloth, wool felt, jute felt, and other applications supports a broader technical perspective. Customers can discuss a single carding machine or a coordinated solution that includes opening, feeding, carding, web forming, bonding, winding, and cutting.
The company’s stated strengths include factory-direct manufacturing, customization, international supply experience, automatic control options, energy-conscious design, precision engineering, CE-related product certification, and after-sales support. A one-year warranty is listed in the product information, while delivery for the reference product is stated as approximately 70 days after receipt of the balance, or approximately two to three months depending on the order arrangement.
Commercial terms may include a minimum order quantity of one set, negotiation-based pricing, naked or polyethylene-film packaging, and payment by telegraphic transfer or letter of credit. These terms are subject to the final contract, product configuration, shipping destination, and project scope.
11. Selecting the Correct Configuration
Customers should provide detailed process information before requesting a final quotation. Important factors include the fiber type, fiber length, denier, crimp, blend ratio, moisture, contamination level, target web weight, finished-product width, required output, downstream process, factory voltage, available floor space, and automation expectations.
For example, a line processing 1.5 to 3 denier polyester fiber may require a different wire and speed arrangement from a line processing 15 denier coarse fiber. A blend containing low-melt fibers may need careful control to avoid premature bonding or roller contamination. Recycled fiber may require stronger upstream cleaning and more frequent inspection of the metal detector and suction system.
The choice between single-cylinder and double-cylinder construction should be based on carding intensity, material difficulty, output expectations, and available investment. The choice between single and double doffers should consider web delivery requirements, product structure, and downstream synchronization. Randomizer rollers should be selected when the final product requires reduced machine-direction orientation.
Width selection should also consider the usable production width rather than only the nominal frame width. Edge trimming, suction zones, web control, and product tolerances can affect the practical output width. A technical layout should show the relationship between the carder and adjacent machines before the order is finalized.
12. Sustainable and Economic Benefits
Although carding machines consume energy to drive large rollers, an efficient and well-controlled design can help reduce waste and improve production economics. Variable-speed drives allow the equipment to operate at the speed required by the product rather than always running at maximum speed. Controlled startup and stopping can reduce mechanical shock and unnecessary energy consumption.
Improved web uniformity can also reduce off-specification material. When the fiber web is more consistent, downstream needle punching or thermal bonding can operate with fewer interruptions and less rework. Better protection of carding wire and rollers may extend service intervals and reduce the cost associated with unexpected damage.
The machine can process virgin and recycled fibers, depending on the final technical design. This supports manufacturers seeking to increase recycled content in their products. However, responsible processing still requires proper sorting, opening, dust management, and quality control. Recycled materials should be tested for metal, moisture, contamination, and fiber consistency before being introduced into the carding line.
13. Q&A
Q1. What is the main function of the HYSL Carding Machine?
The machine fully cards fiber batt received from opening and blending equipment. It separates and distributes the fibers, forms a parallel or partly random web, and delivers that web to the next production process.
Q2. Which fibers can the machine process?
The machine can be configured for polyester staple fiber, polypropylene staple fiber, wool, hemp, waste fiber, low-melt fiber, and other compatible materials. Final suitability depends on fiber length, denier, blend ratio, contamination, and the selected carding wire and settings.
Q3. Is the machine available with different working widths?
Yes. Listed working widths include approximately 1.55 meters, 1.85 meters, 2 meters, 2.5 meters, and 2.8 meters. The reference HYSL-230 model has an effective width of approximately 2,300 millimeters.
Q4. Can customers choose single-cylinder or double-cylinder construction?
Yes. The HYSL series can be designed with a single-cylinder or double-cylinder structure. The correct choice depends on the required carding intensity, fiber type, target output, product structure, and project budget.
Q5. Does the machine support double doffers?
Yes. Single-doffer and double-doffer configurations are available. The reference HYSL-230 description identifies a single-cylinder and double-doffer arrangement.
Q6. Can the machine produce a random fiber web?
It can be fitted with randomizer rollers when a more random fiber distribution is required. Doffer speed, carding settings, and downstream web-forming equipment also influence the final fiber orientation.
Q7. What safety protection is included?
Standard safety-related features include an anti-metal detection device at the feeding section, automatic stop and alarm functions, transparent safety covers, emergency protection, and an electronic safety system. The exact safety package should be confirmed for the final machine and destination country.
Q8. How does the anti-metal protection system work?
The detector monitors the incoming fiber stream for metallic objects. When metal is identified, the system can trigger an alarm and stop the machine to help prevent damage to carding wire, rollers, and other components.
Q9. What are the main cylinder and roller dimensions?
The reference specifications identify a main cylinder diameter of approximately 1,230 millimeters, a breast cylinder diameter of approximately 850 millimeters where fitted, working rollers of approximately 165 millimeters, and stripping rollers of approximately 78 millimeters.
Q10. What production capacity can be expected?
Published information includes maximum output values in the range of approximately 600 to 800 kilograms per hour for certain configurations. Actual output depends on fiber characteristics, working width, web weight, speed, carding intensity, and downstream conditions. A final capacity should be confirmed through technical evaluation or testing.
Q11. What is the maximum operating speed?
Different configurations are listed with speeds below 80 meters per minute, around 70 meters per minute, or up to approximately 100 meters per minute. The practical speed is selected to maintain the required web quality and stable synchronization with the complete production line.
Q12. Can the machine be integrated into a needle-punching line?
Yes. The machine is suitable for use in needle-punching lines and can be connected to cross-lapping and needle-punching equipment. It can also be used in thermal bonding, quilting, airlaid, and other nonwoven production systems.
Q13. Is the electrical system customizable?
Yes. The listed information includes 220 volts, 380/220 volts, and customized voltage options. The final electrical design should match the customer’s local power supply and the requirements of the complete line.
Q14. What kind of maintenance does the machine require?
Routine maintenance includes cleaning fiber deposits, checking wire surfaces, inspecting bearings and drives, maintaining suction paths, testing safety devices, checking roller alignment, and reviewing electrical alarms. Maintenance frequency depends on production hours, fiber type, dust level, and operating conditions.
Q15. Does the manufacturer provide after-sales support?
The product information lists a one-year warranty and video outgoing inspection. Installation assistance, commissioning, training, spare parts, and remote or on-site support should be agreed in the quotation and sales contract.
Q16. How long is the delivery period?
The listed lead time is approximately two to three months, with a reference delivery statement of about 70 days after receipt of the balance. Actual delivery depends on configuration, production scheduling, inspection, shipping, and project requirements.
Q17. What information should be included in an inquiry?
An inquiry should include the fiber type, denier, staple length, blend ratio, target web weight, working width, required output, downstream process, factory voltage, preferred cylinder and doffer arrangement, automation requirements, destination country, and any special safety or layout conditions.
14. Conclusion
The HYSL Carding Machine is a flexible solution for manufacturers seeking stable fiber preparation and reliable web formation. Its multi-stage carding structure, variable-speed drives, adaptable cylinder and doffer options, optional randomizer rollers, anti-metal protection, dust-removal system, balanced rotating components, and transparent safety guards provide a strong foundation for modern nonwoven production.
Its value is not limited to a single machine specification. The equipment can be adapted to different working widths, fibers, web weights, production lines, and finished products. By combining carding technology with customized engineering and experience in complete nonwoven systems, Changshu Hongyi Nonwoven Machinery Co., Ltd. can support projects ranging from individual machine replacement to full production-line construction.
For the best result, customers should treat the carder as part of an integrated process. Correct upstream fiber preparation, appropriate wire selection, accurate speed synchronization, effective dust removal, proper maintenance, and suitable downstream equipment are all necessary to achieve the promised performance. With these conditions in place, the HYSL series can help improve web consistency, protect valuable machine components, reduce production variation, and support the manufacture of high-quality nonwoven fabrics.
References
1. Product technical information for the HYSL Carding Machine, including structure, operating features, working widths, roller dimensions, safety functions, and application data.
2. Technical specifications for the HYSL-230 reference configuration, including single-cylinder and double-doffer construction, 2,300-millimeter working width, five carding groups, and approximately 1,230-millimeter main-cylinder diameter.
3. Manufacturer information for Changshu Hongyi Nonwoven Machinery Co., Ltd., including company history, production-line capabilities, customization services, international supply experience, and after-sales support.
4. General principles of staple-fiber carding, web formation, fiber orientation, doffing, roller operation, and nonwoven process integration.
5. General machinery engineering practices relating to roller balancing, variable-speed drives, metal detection, dust collection, machine guarding, and preventive maintenance.