

Content
- 1 1. The Role of a Vibrating Feeder in Nonwoven Production
- 2 2. Product Overview
- 3 3. Operating Principle
- 4 4. Main Advantages of the HYGM Vibrating Feeder
- 5 5. Competitive Advantages Compared with Conventional Feeding Solutions
- 6 6. Manufacturing Strengths and Engineering Capability
- 7 7. Application Areas
- 8 8. Process Benefits for Product Quality
- 9 9. Installation and Integration Considerations
- 10 10. Operation, Adjustment, and Maintenance
- 11 11. Purchasing Guidance for International Buyers
- 12 12. Why Work with an Experienced Nonwoven Machinery Manufacturer?
- 13 13. Recommended Project Workflow
- 14 14. Q&A
- 14.1 Q1: What is the main purpose of the HYGM Vibrating Feeder?
- 14.2 Q2: Which fibers can be processed?
- 14.3 Q3: Is the machine automatic?
- 14.4 Q4: How does the photoelectric control work?
- 14.5 Q5: What is the function of the evener roller?
- 14.6 Q6: Why is a vibrating cabin used?
- 14.7 Q7: What working widths are available?
- 14.8 Q8: What production capacity can the feeder achieve?
- 14.9 Q9: Can the feeder be integrated into an existing line?
- 14.10 Q10: What should operators do if hanging fiber appears?
- 14.11 Q11: What electrical supply is available?
- 14.12 Q12: Is customization available?
- 14.13 Q13: What certifications are listed?
- 14.14 Q14: What after-sales support is available?
- 14.15 Q15: Can the manufacturer supply more than a vibrating feeder?
- 15 15. Conclusion
- 16 References
- 17 Product: HYGM Vibrating Feeder
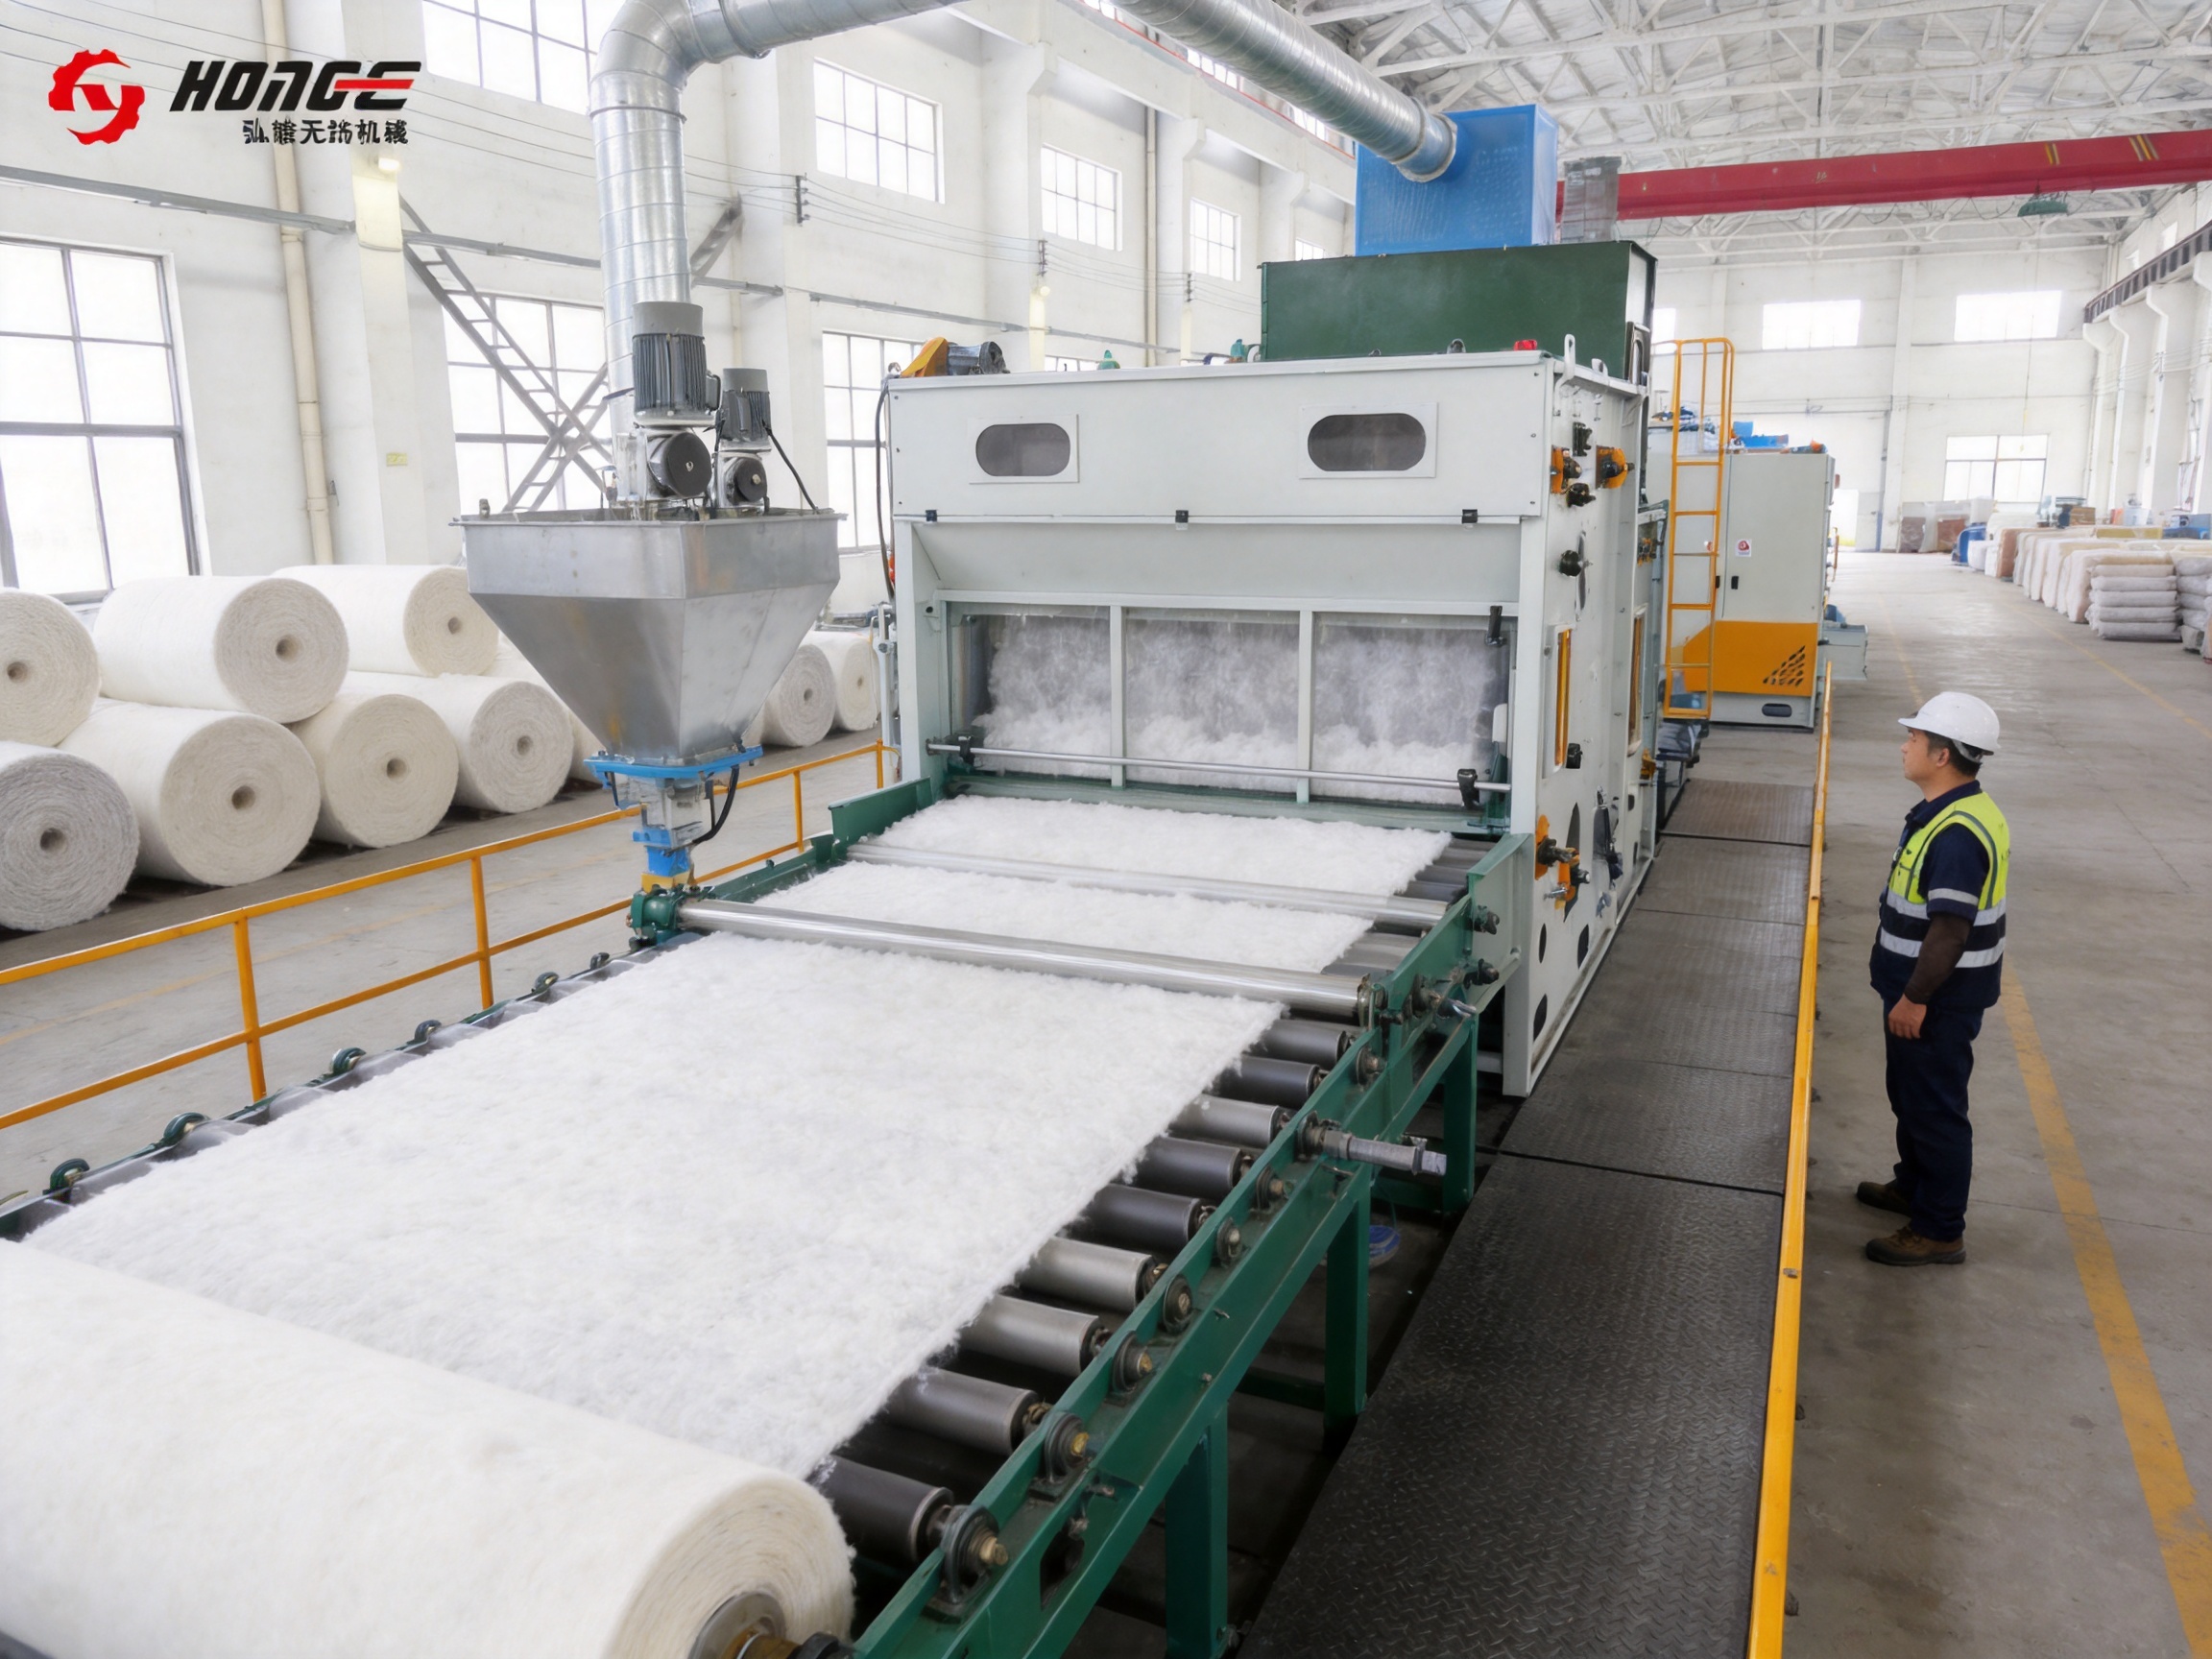
In nonwoven manufacturing, the quality of the final fabric is strongly influenced by the stability of the fiber feed at the beginning of the carding process. Even high-quality fibers can produce an uneven web if the feeding system delivers fluctuating quantities, creates widthwise concentration differences, or allows excessive fiber accumulation in the preparation section. The HYGM Vibrating Feeder is designed to address these challenges by storing opened fibers, blending them further, and transferring a more uniform layer across the working width of the next process.
Developed for medium- to coarse-denier fibers, this feeder can be integrated into nonwoven production lines using polyester, viscose, nylon, polypropylene, glass fiber, and other suitable materials. Its combination of spike and oblique lattice feeding, evener roller control, stripper operation, photoelectric storage monitoring, and vibrating delivery provides a practical solution for improving the continuity of fiber preparation.
Manufactured by Changshu Hongyi Nonwoven Machinery Co., Ltd., the equipment is intended for both individual machine installation and complete nonwoven production lines. The manufacturer has more than 20 years of experience in the nonwoven machinery field and supplies equipment to customers in Asia, Latin America, Africa, the Middle East, and other international markets.
1. The Role of a Vibrating Feeder in Nonwoven Production
A vibrating feeder is positioned between the opening section and the carding or subsequent fiber-forming process. Its main responsibility is not simply to move fiber from one machine to another. It must also help regulate the quantity, distribution, and continuity of the material being delivered.
After fibers pass through the opening process, they may still contain variations in density, length distribution, orientation, and accumulation. If these variations are sent directly into the card, the carding machine may receive an unstable feed. The result can be changes in batt weight, web uniformity, thickness, tensile strength, appearance, and production efficiency.
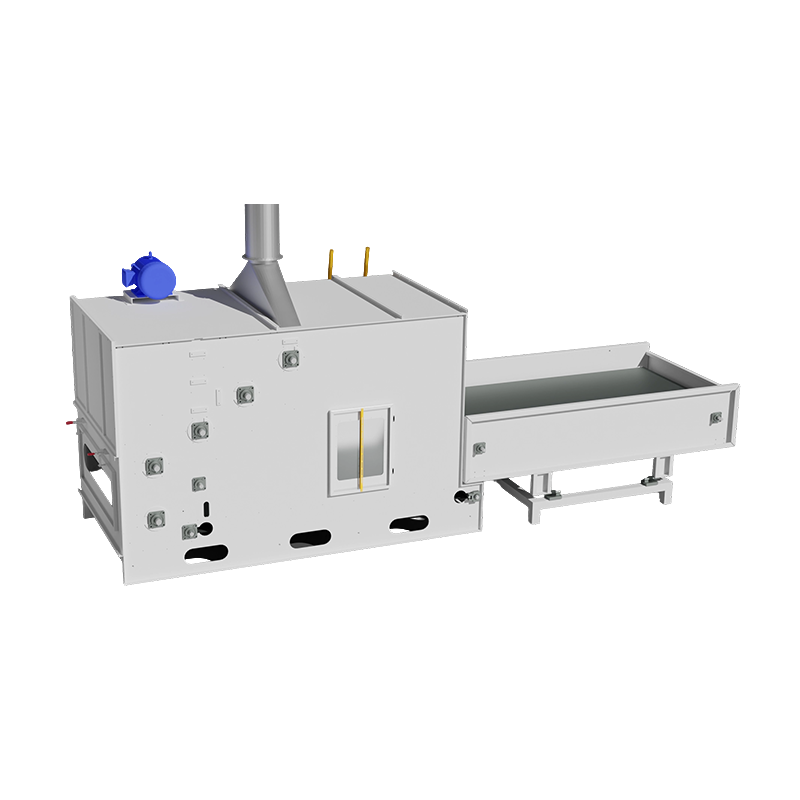
The HYGM Vibrating Feeder acts as a controlled buffer between the opener and the card. Opened fibers enter the feeder, are temporarily stored, blended, leveled, and then delivered in a more stable quantity. The vibrating cabin helps discharge the prepared material evenly toward the next process, while the photoelectric control system monitors the storage condition and helps coordinate the operating cycles of the feeding components.
This arrangement is especially useful where production lines operate continuously and where a stable fiber layer is required across a wide working width. It can help reduce sudden surges and shortages that would otherwise place additional demands on the carding machine.
2. Product Overview
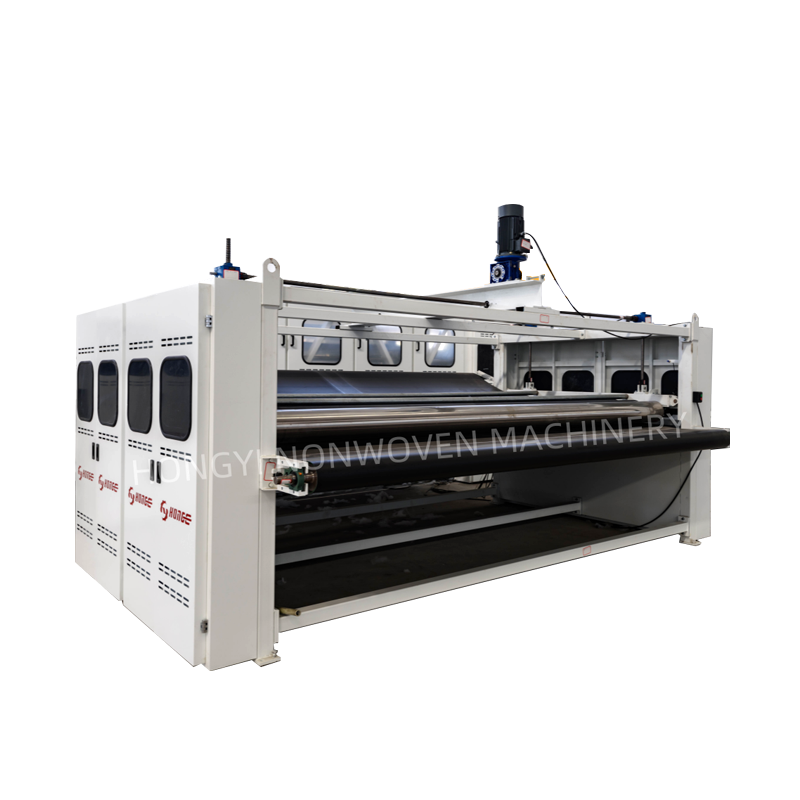
The HYGM model is an automatic vibrating feeder for nonwoven fiber preparation. It is available with different working widths and can be customized according to the layout, material characteristics, production capacity, and interface requirements of the customer’s line.
The available information identifies several working-width options, including approximately 1.4 m, 1.7 m, 1.8 m, 2 m, 2.2 m, and 2.8 m. Other supplied specifications mention widths from 1 m to 2 m and a width of approximately 1.75 m in a general configuration. Because nonwoven lines are often engineered according to the customer’s carding machine and output target, the final working width, dimensions, and configuration should be confirmed during technical quotation and order review.
The equipment is described as an electromagnetic vibrating feeder with an adjustable vibrating plate. Storage control is performed by a photosensor, and the electrical supply can be configured for AC 220 V or AC 380 V according to the installation environment. The supplied data also lists customizable dimensions and color options.
| Item | Available Information |
|---|---|
| Model | HYGM |
| Product type | Automatic vibrating feeder for nonwoven fibers |
| Main application | Nonwoven fabric production and fiber preparation |
| Suitable fibers | Polyester, viscose, nylon, polypropylene, glass fiber, and other compatible fibers |
| Working width options | Approximately 1.4 m, 1.7 m, 1.8 m, 2 m, 2.2 m, and 2.8 m; other widths may be customized |
| Control method | Photoelectric storage control with automatic feeding coordination |
| Feeding method | Spike and oblique lattice feeding, evener roller, stripper, and vibrating cabin |
| Power supply | AC 220 V or AC 380 V, subject to configuration |
| Installed power reference | Approximately 4.45 kW in the listed configuration |
| Capacity reference | Approximately 0.1–5 t/h, depending on fiber, width, density, and process conditions |
| Certification information | CE and ISO9001-related certification information supplied for the product and manufacturer |
| Warranty information | One-year after-sales warranty listed in the supplied specifications |
| Lead time reference | Approximately two to three months, depending on configuration and production schedule |
The figures above should be treated as configuration references rather than universal operating limits. Actual performance depends on the fiber type, fiber length, denier, moisture, opening condition, target batt weight, working width, line speed, and the settings of the connected equipment.
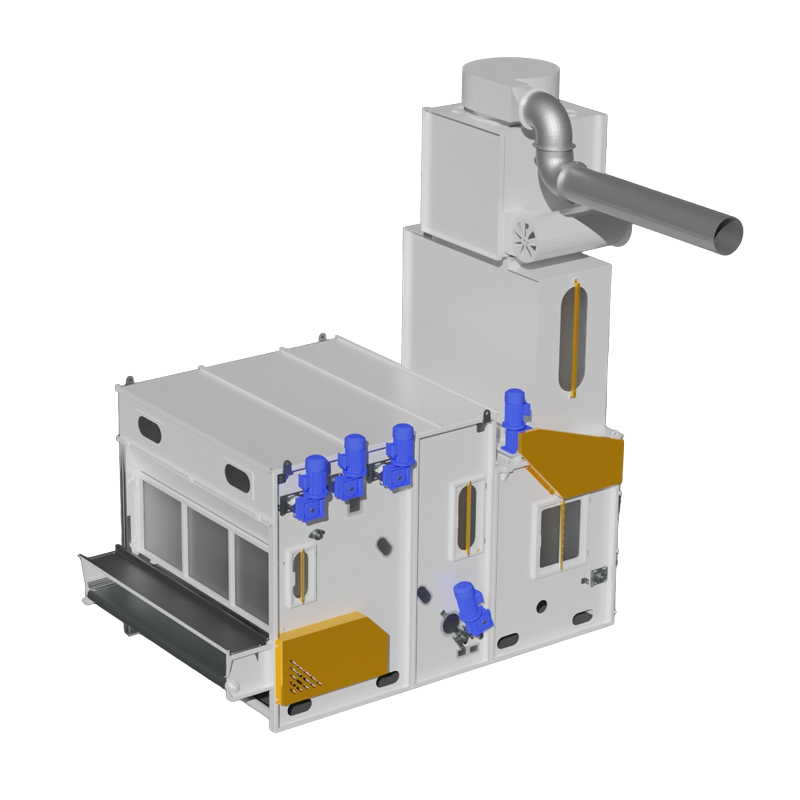
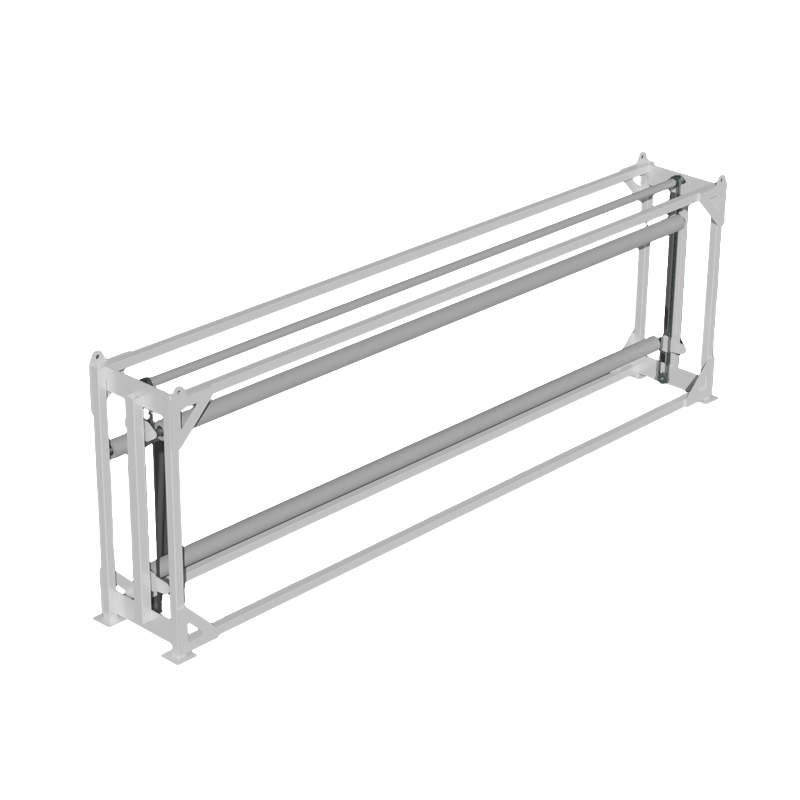
HYGM Vibrating Feeder
3. Operating Principle
The operating principle of the HYGM feeder can be understood as a sequence of receiving, leveling, monitoring, storing, blending, and delivering fiber.
3.1 Fiber Reception from the Opener
The main opener delivers opened fiber toward the feeder. At this stage, the fiber may be relatively loose but not perfectly uniform. Some fiber clusters can remain, and the amount of material entering the feeder can vary as the upstream opening equipment processes different portions of the raw material.
The feeder receives this material and provides an intermediate storage area. This buffer reduces the direct influence of short-term fluctuations from the opener on the carding process. Instead of requiring the card to respond immediately to every variation in the incoming fiber stream, the feeder helps regulate the transfer.
3.2 Spike and Oblique Lattice Feeding
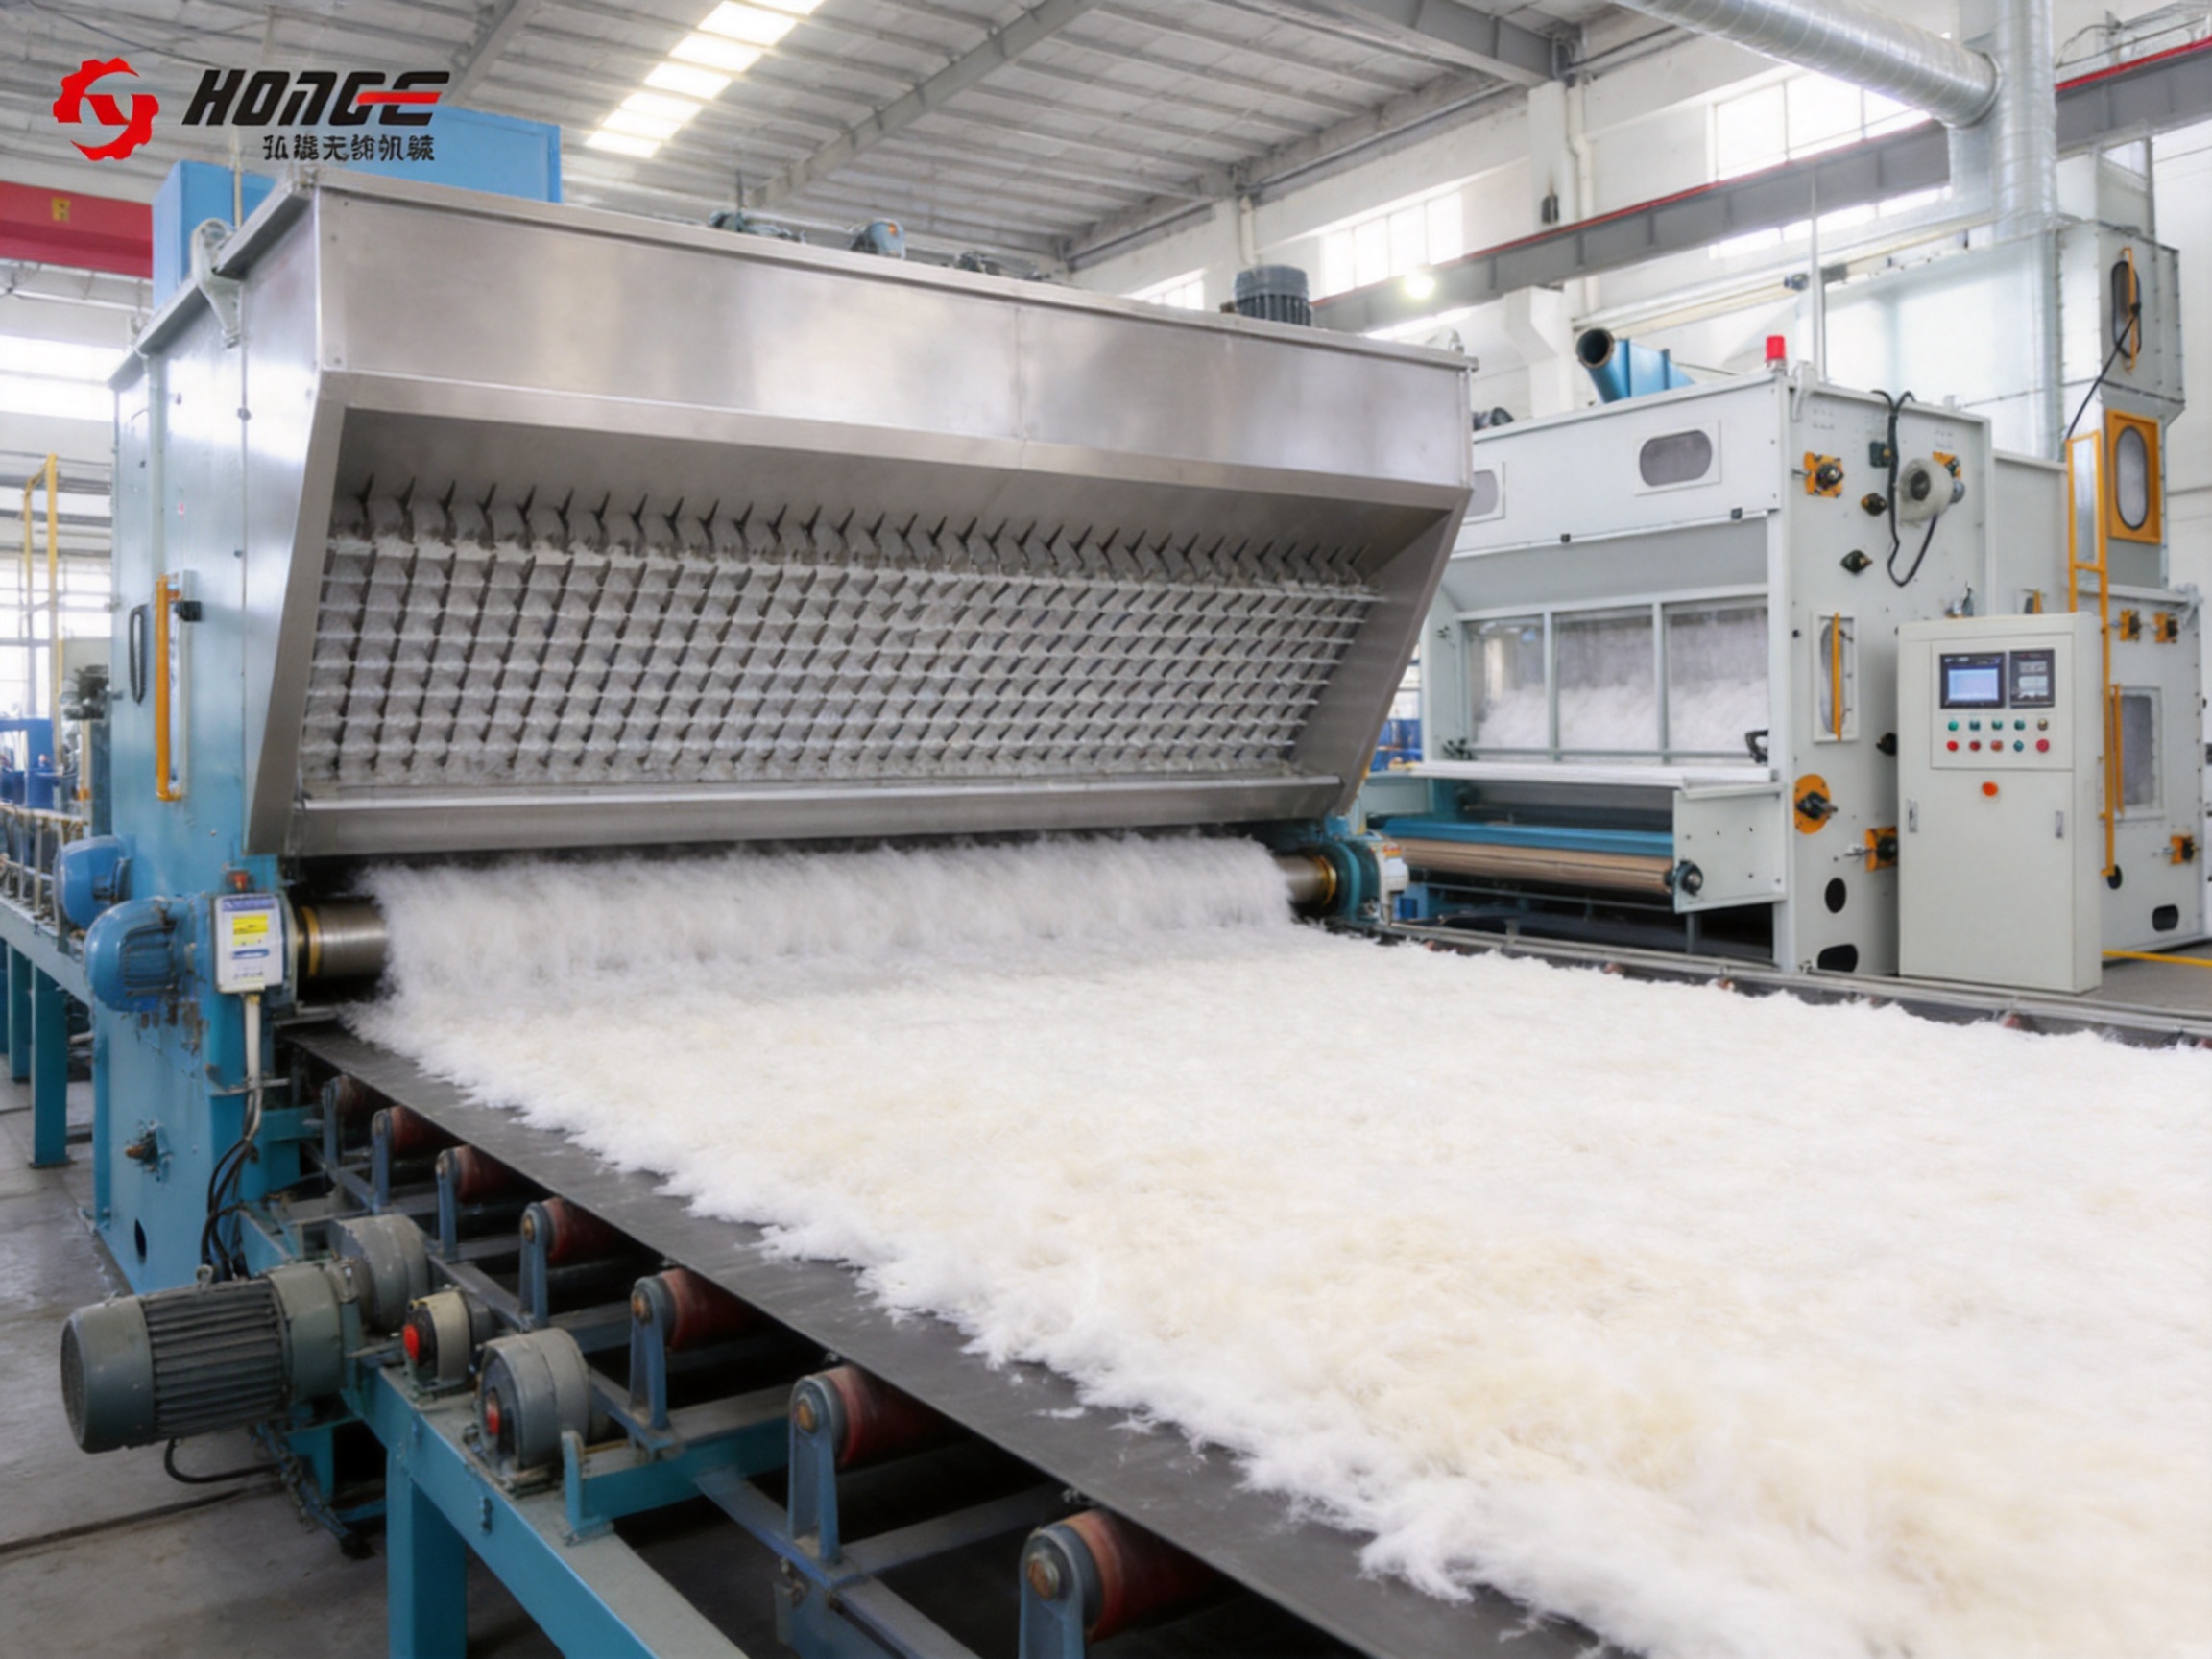
The spike and oblique lattice system moves material through the feeding section. The spikes engage the opened fiber and help convey it upward or forward, while the oblique lattice supports the controlled movement of the material. This arrangement is intended to maintain a steady flow rather than allowing loose fiber to move in an uncontrolled mass.
The start and stop operation of the spike and oblique lattice is controlled by a photoelectric system. When the monitored fiber level reaches a designated condition, the feeding components can be started or stopped to maintain a more balanced storage volume. This automatic response helps reduce manual intervention and supports more consistent operation during long production runs.
3.3 Evener Roller Function
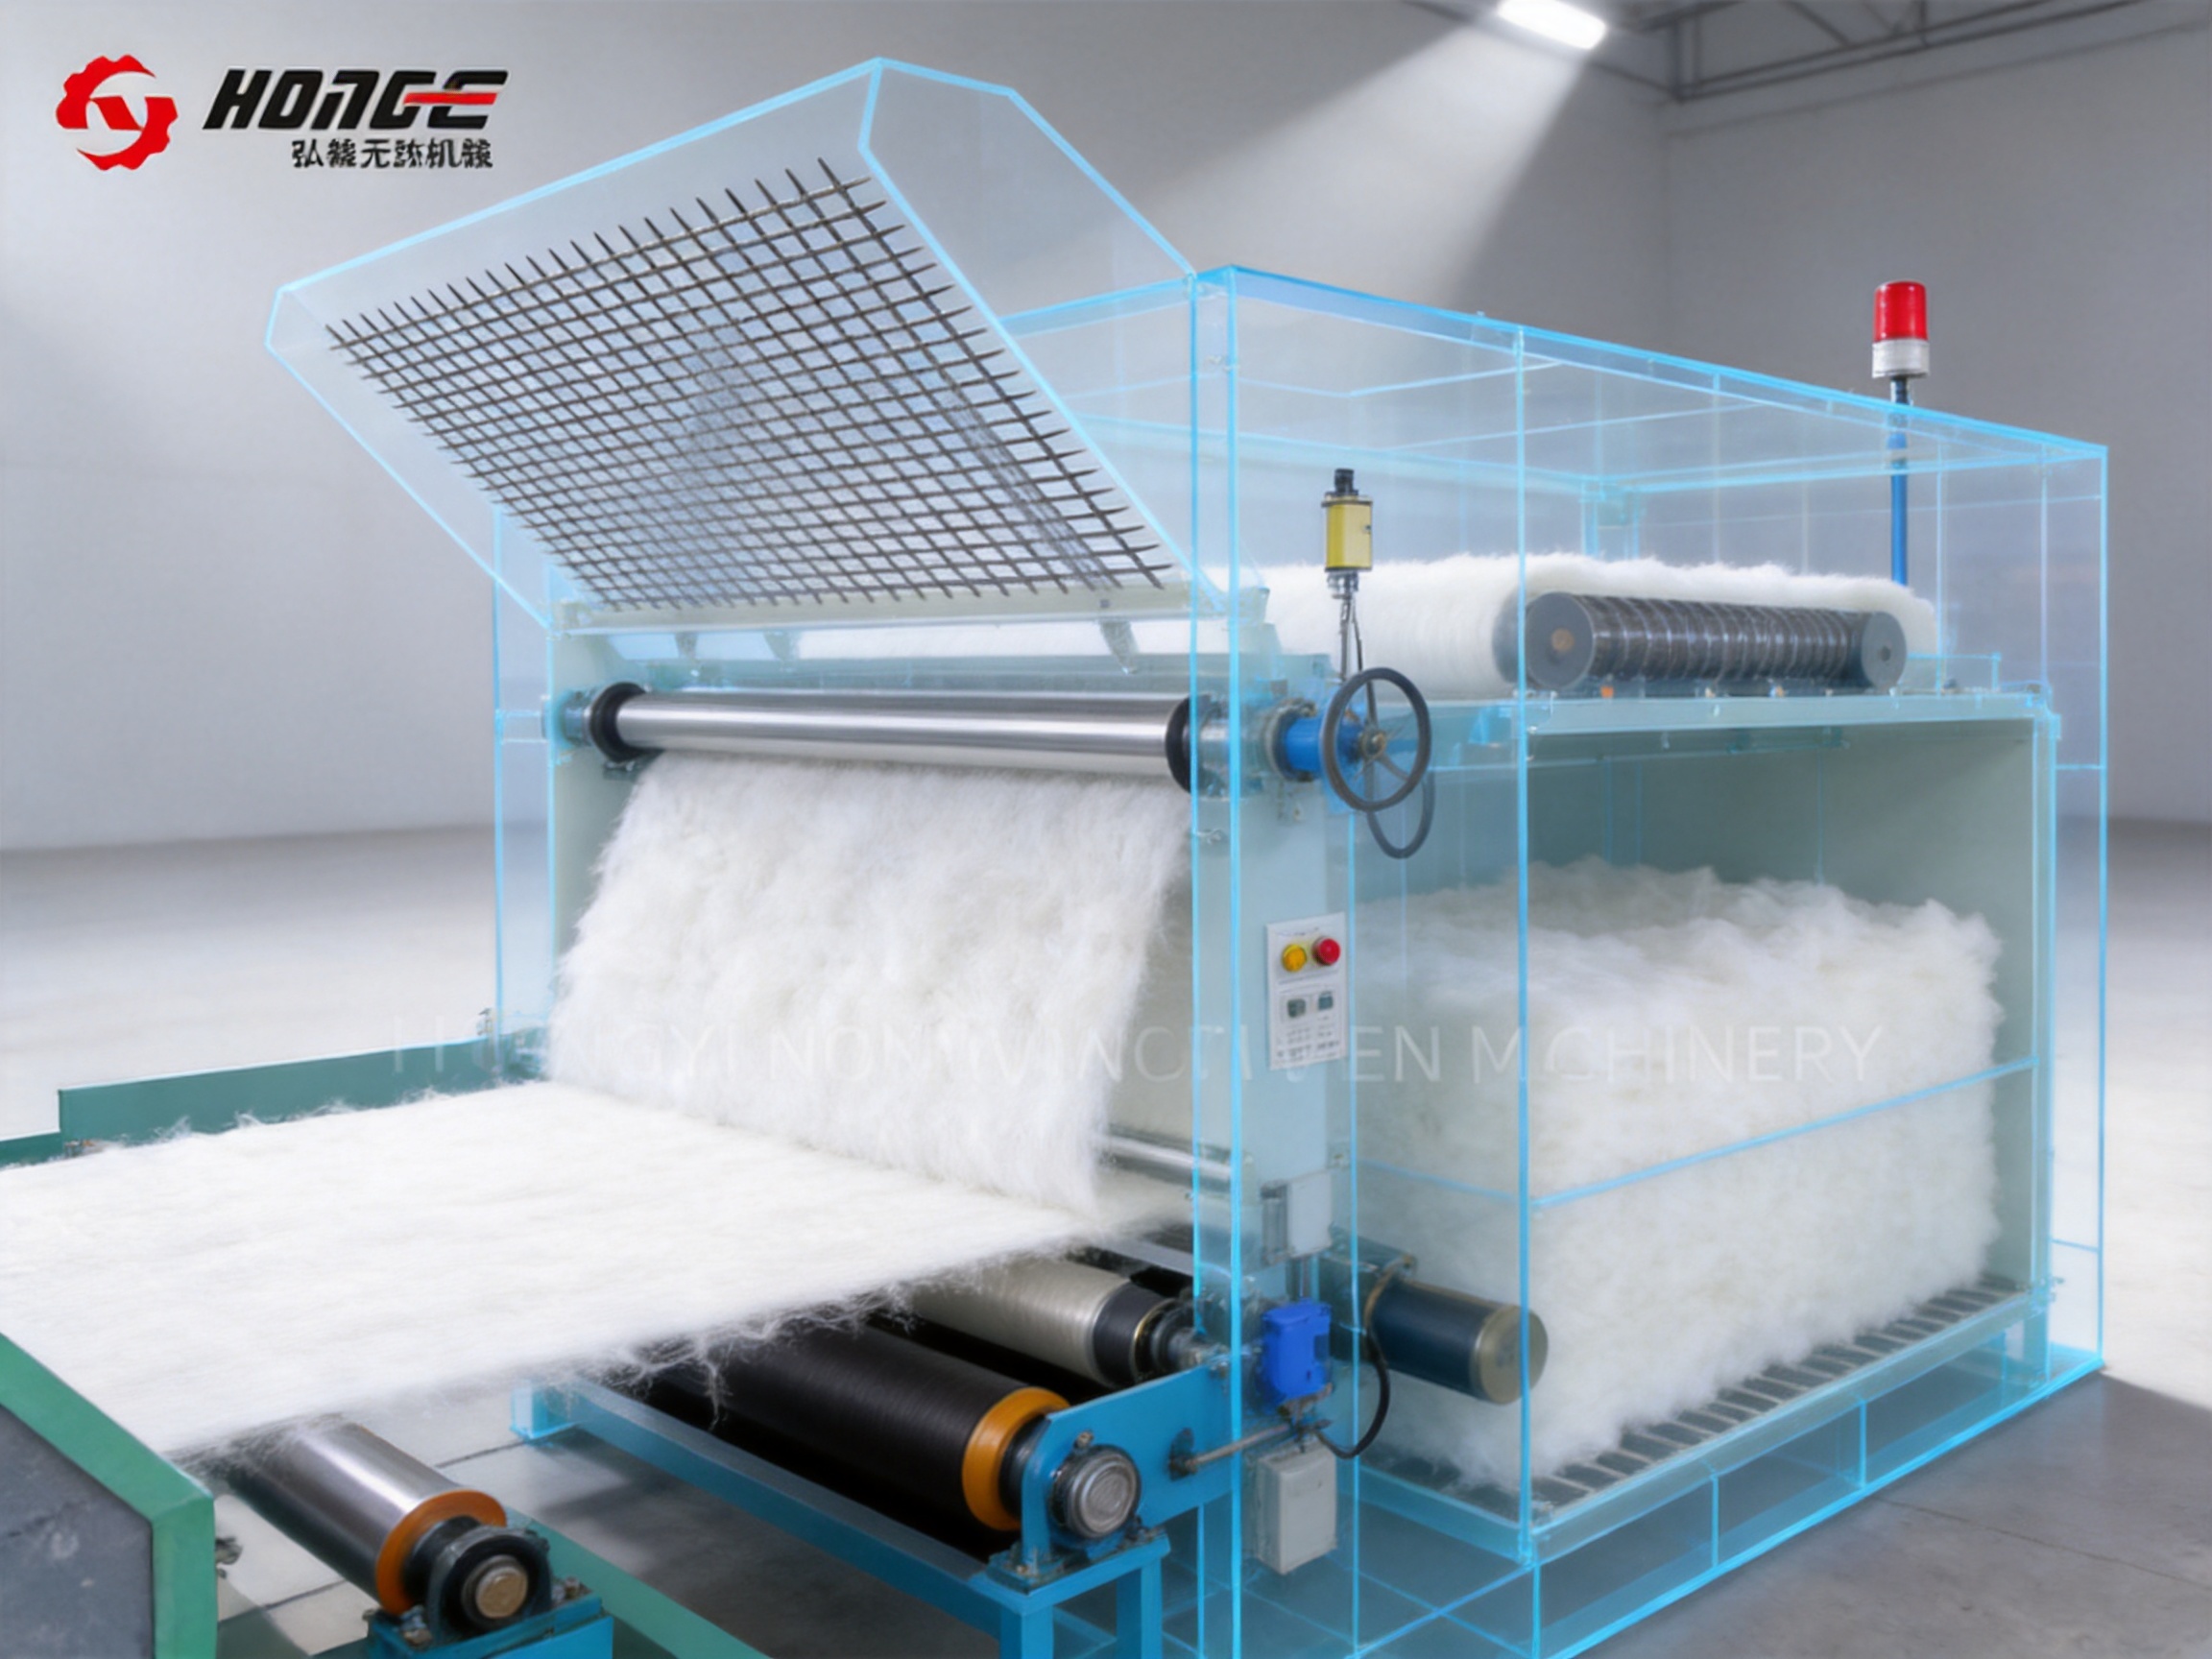
The evener roller removes excess fiber from the incoming layer. If too much fiber is carried forward, the roller helps return the process toward the intended material level. The objective is to prevent large accumulations from passing into the vibrating cabin and to improve the regularity of the fiber layer.
By controlling excess material before the final delivery stage, the evener roller can help protect the card from sudden overfeeding. It also contributes to more stable product weight and thickness when the feeder is correctly adjusted for the fiber being processed.
3.4 Stripping and Transfer to the Vibrating Cabin
After the fiber has been regulated, the stripper removes it from the relevant conveying surface and transfers it into the vibrating cabin. The stripper must work in coordination with the lattice, evener roller, and downstream vibrating section. Proper coordination prevents material from remaining attached to the working surfaces or accumulating in unwanted locations.
The vibrating cabin then distributes and transfers the fiber toward the next carding process. Vibration encourages the fiber to settle and move in a controlled manner. Rather than relying only on a fast mechanical conveying action, the system uses controlled vibration to support a more even delivery across the machine width.
3.5 Delivery to the Carding Process
The final objective is to supply the card with a stable quantity of fiber. The card can then perform its intended opening, individualization, alignment, and web-forming functions under more consistent input conditions.
The feeder does not replace the need for correct card settings. Wire condition, feed roller pressure, carding speed, worker and stripper settings, suction, and production speed still influence final quality. However, a stable feeder can provide a better foundation for these downstream adjustments.
4. Main Advantages of the HYGM Vibrating Feeder
4.1 More Even Fiber Feeding
The principal advantage of the HYGM feeder is its ability to regulate the material before it reaches the card. The combination of mechanical leveling, automatic photoelectric control, and vibration helps create a more consistent feeding condition.
More even feeding can contribute to improved longitudinal and cross-machine uniformity. It may also reduce the frequency of manual corrections required by operators, particularly when the machine is integrated with a properly matched opener and card.
4.2 Wider Fiber Compatibility
The feeder is intended for medium- to coarse-denier fibers and can be used with a range of common nonwoven raw materials. The supplied application information includes polyester, viscose, nylon, polypropylene, and glass fiber.
These materials have different friction, resilience, length, density, and static-electricity characteristics. For this reason, the feeder must be adjusted according to the selected fiber. Nevertheless, the ability to accommodate several material families gives the machine greater flexibility than a system designed for only one narrow raw-material specification.
4.3 Automatic Photoelectric Control
Photoelectric storage control is an important feature for continuous nonwoven production. It monitors the material condition in the storage area and controls the operating state of the spike and oblique lattice. This helps maintain a suitable quantity of fiber without relying entirely on visual observation.
Compared with a manually controlled feeder, an automatic photoelectric system can respond more quickly to changes in material level. It can also support a more repeatable production process across different shifts and reduce the risk of inconsistent operator intervention.
4.4 Improved Process Buffering
Opening and carding machines do not always produce or consume fiber at exactly the same instantaneous rate. The feeder functions as a buffer that helps isolate the two processes from short-term variations.
This buffering capability is particularly valuable in lines producing geotextiles, carpets, filtration materials, automotive interior products, cleaning cloths, insulation products, and other needle-punched or thermally bonded nonwovens. Stable fiber preparation can make it easier to maintain the required basis weight and production rhythm.
4.5 Adjustable and Customizable Configuration
Nonwoven production lines vary considerably in working width, output, building layout, fiber specification, and downstream technology. The HYGM feeder is offered with multiple working-width options and customizable dimensions. Electrical supply, color, and other configuration details can also be adapted to the customer’s requirements.
This flexibility is an advantage over standardized equipment that may require extensive modification before it can be connected to an existing line. A customized feeder can be designed to match the card inlet height, transfer direction, line centerline, maintenance access, and factory space.
4.6 Reduced Dependence on Manual Feeding Adjustments
Without automatic storage monitoring, operators may need to inspect the material level and manually adjust the feeding cycle. Such adjustments can vary according to operator experience and may not be consistent during a long shift.
The HYGM system uses photoelectric control to coordinate material storage and feeding. This does not eliminate the need for skilled operation, but it can reduce routine intervention and allow operators to focus on quality inspection, raw-material management, maintenance, and process optimization.
4.7 Compatibility with Complete Production Lines
The manufacturer supplies both individual machines and complete nonwoven production lines. This enables the feeder to be considered as part of a wider process rather than as an isolated unit.
When the opener, feeder, card, crosslapper, needle-punching machine, thermal bonding oven, winding machine, and cutting equipment are engineered together, the material flow and control logic can be coordinated more effectively. This can simplify installation responsibility and reduce the risks associated with combining equipment from multiple unrelated suppliers.
5. Competitive Advantages Compared with Conventional Feeding Solutions
Equipment comparisons should be based on the actual application, but several practical advantages distinguish this type of vibrating feeder from simpler or less integrated alternatives.
5.1 Compared with Simple Storage Hoppers
A basic hopper can store fiber, but storage alone does not guarantee an even feed. Fiber may bridge, form clumps, settle unevenly, or discharge in intermittent surges. The HYGM feeder combines storage with spike and oblique lattice movement, leveling, stripping, and vibration.
This integrated approach gives the operator more control over the transition from opened fiber to card feeding. It also helps the machine perform an active conditioning function rather than acting only as a passive container.
5.2 Compared with Manually Controlled Feeders
Manual systems depend heavily on the operator’s ability to observe the fiber level and adjust the feeding rate. This can be acceptable for small or intermittent operations, but it becomes less suitable as production speed and working width increase.
The photoelectric control used by the HYGM feeder supports automatic response to material-level changes. The result is a more repeatable feeding cycle and less dependence on continuous manual correction.
5.3 Compared with Narrow, Single-Width Equipment
Many nonwoven factories expand their production capacity over time. A feeder restricted to one width may become a bottleneck when the carding machine or final product specification changes. Multiple working-width options and customized dimensions make the HYGM platform more adaptable to different line designs.
The ability to configure the machine for different widths also supports production planning for customers who manufacture more than one type of nonwoven material.
5.4 Compared with Equipment without Upstream and Downstream Integration
A feeder purchased without consideration of the opener and card may create interface problems, including mismatched heights, unsuitable transfer distances, inadequate control communication, and inconsistent capacity.
A manufacturer experienced in complete nonwoven lines can assess the feeder as part of the overall process. This is particularly valuable for customers buying a new line or upgrading several connected machines at the same time.
5.5 Compared with Less Flexible Imported or Generic Designs
Generic equipment can sometimes offer a lower initial purchase price, but it may provide fewer options for working width, control configuration, local electrical standards, and process-specific adaptation. A manufacturer offering customized dimensions, voltage options, and line engineering can provide a better fit for the actual factory environment.
The most suitable choice should consider total ownership cost, installation, spare parts, commissioning, energy consumption, maintenance access, operator training, and long-term service—not only the initial price.
6. Manufacturing Strengths and Engineering Capability
The performance of a vibrating feeder depends not only on its basic design but also on how consistently it is manufactured, assembled, tested, and integrated. Changshu Hongyi Nonwoven Machinery Co., Ltd. has more than 20 years of experience in nonwoven machinery, providing a foundation for equipment development and production knowledge.
6.1 Experience in Nonwoven Machinery
The company’s product range includes opening and blending equipment, feeding and carding equipment, web-forming and needle-punching machinery, thermal bonding and heat-setting systems, airlay equipment, winding and cutting machines, auxiliary equipment, and complete nonwoven production lines.
This broad product coverage is important because fiber feeding performance is closely connected to the machines before and after it. Experience with carding, needle punching, thermal bonding, airlay production, and winding allows the manufacturer to understand how upstream feeding affects final fabric quality and production stability.
6.2 Complete-Line and Unit-Machine Supply
Customers can purchase the HYGM feeder as a unit machine or include it in a larger turnkey or semi-turnkey nonwoven project. Complete-line experience allows the supplier to consider material flow, machine spacing, control interfaces, output matching, and maintenance access during the design stage.
For a factory expansion, this approach can reduce the need for the customer to coordinate several equipment suppliers. It can also clarify responsibility during installation and commissioning.
6.3 Custom Engineering
The supplied product information identifies customized dimensions, color, voltage, and working-width options. Customization is particularly relevant in nonwoven production because factories may use different building layouts, raw materials, card models, output targets, and product widths.
A proper customization process should include review of the customer’s process flow, raw-material data, target production rate, installation drawings, electrical standard, control requirements, and downstream interface. These details help ensure that the delivered feeder is suitable for the complete production environment.
6.4 Quality Management and Certification Information
The product information lists CE and ISO9001-related certification details. CE-related compliance supports the assessment of applicable safety and conformity requirements for the intended market, while ISO9001 certification reflects a structured quality-management approach at the organizational level.
Certification does not replace application-specific engineering, installation, or operator training. However, it provides customers with useful evidence that the supplier maintains documented processes and considers applicable quality and safety requirements.
6.5 Inspection and Commissioning Support
Video outgoing inspection is listed among the product information. Factory inspection records, operating videos, and pre-shipment checks can help customers confirm the appearance, assembly, control operation, and basic movement of the equipment before dispatch.
For an industrial machine, outgoing inspection should ideally cover mechanical rotation, vibration operation, sensor response, emergency-stop function, electrical cabinet condition, guarding, fastener security, and interface dimensions. Final acceptance should be based on the agreed technical specification and, where applicable, a customer-approved factory acceptance test.
6.6 International Supply Experience
The company reports supplying products to more than 20 countries, including Mexico, Argentina, Brazil, Turkey, Algeria, Egypt, Bangladesh, Vietnam, and Thailand. International experience can support better understanding of export packing, different voltage systems, documentation, installation coordination, and customer communication across regions.
The listed transport options include nude packing or polyethylene film packing. The appropriate packing method should be selected according to the shipping route, container arrangement, humidity exposure, loading method, and destination requirements. Additional protection may be necessary for long-distance sea freight or storage in humid conditions.
7. Application Areas
7.1 Needle-Punched Geotextiles
Geotextile production often requires stable fiber feeding because changes in batt weight can affect fabric thickness, tensile properties, permeability, and dimensional stability. A vibrating feeder can support the opening and carding section before crosslapping and needle punching.
For heavy geotextiles, the appropriate feeder configuration must be selected according to fiber denier, line width, target basis weight, and required output. The feeder should be synchronized with the card and crosslapper to prevent unnecessary accumulation or starvation.
7.2 Nonwoven Carpets and Floor Coverings
Carpet substrates and felt-like floor coverings may use polyester, polypropylene, recycled fibers, or blended raw materials. Even fiber feeding helps maintain a consistent base for downstream web forming and needle punching.
Where colored or blended fibers are used, the blending performance of the complete opening and feeding system becomes especially important. Operators should confirm that the machine configuration is appropriate for the desired blend ratio and product appearance.
7.3 Automotive Interior Materials
Automotive interior materials require controlled thickness, density, acoustic performance, and appearance. They may include polyester fibers, recycled fibers, bicomponent fibers, or other engineered materials. A stable feeding stage supports the consistency required by later needle-punching, thermal bonding, laminating, or molding operations.
7.4 Cleaning Cloths and Industrial Felts
Cleaning cloths and industrial felts can require different fiber blends and basis weights. The ability to adjust feeding and use different working widths makes a flexible vibrating feeder useful for manufacturers producing multiple specifications on one line.
7.5 Thermal Bonded Wadding and Insulation Materials
For thermal bonded wadding, the feeder supplies the carding section that prepares the web before it enters an oven or heat-setting system. Consistent fiber distribution can contribute to more stable loft, thickness, and thermal performance.
7.6 Glass Fiber and Special-Fiber Processing
The supplied application information includes glass fiber among the compatible materials. Glass fiber handling requires particular attention to abrasion, dust control, worker protection, and machine wear. Before processing, customers should provide detailed material information so that contact surfaces, cleaning provisions, guarding, and maintenance procedures can be reviewed.
8. Process Benefits for Product Quality
Although the feeder is one component in a larger line, its operating condition can influence several important product-quality indicators.
8.1 Basis-Weight Stability
When the card receives a more consistent amount of fiber, the web-forming section has a better opportunity to maintain the target basis weight. This is not a guarantee of a specific tolerance, because basis weight also depends on line speed, card settings, crosslapping, drafting, and downstream control. Nevertheless, stable feeding is an important starting point.
8.2 Cross-Machine Uniformity
A feeder designed to distribute material across the full machine width can help reduce widthwise variations in fiber quantity. This is particularly important for wide products, where a narrow concentration of fiber can create weak or heavy zones after needling or thermal bonding.
8.3 Reduced Fiber Surges
Sudden fiber surges can overload the card, increase web thickness locally, or cause operating interruptions. The evener roller and photoelectric storage control help manage the amount of fiber transferred through the system.
8.4 More Stable Downstream Operation
Needle-punching machines, thermal bonding ovens, and winding systems operate more efficiently when the incoming web is consistent. A stable web can reduce the need for frequent speed changes and manual corrections. It may also support more predictable finishing and inspection results.
8.5 Better Repeatability Between Production Batches
Automatic feeding control can make it easier to reproduce an established process setting. Once the feeder, opener, card, and downstream machines have been adjusted for a specific product, the same operating logic can be applied in later batches, subject to raw-material and environmental differences.
9. Installation and Integration Considerations
Successful performance depends on correct installation. Before delivery, the customer and supplier should confirm the feeder’s working width, overall dimensions, inlet and outlet heights, transfer direction, foundation requirements, access space, electrical supply, and control connections.
The feeder should be positioned so that operators can safely inspect the storage area, remove unwanted fiber, clean the working surfaces, and access the drive and electrical components. Adequate space around the equipment is essential for maintenance and emergency response.
The carding machine should be checked for compatible feed height and width. If the feeder is too close, too high, or incorrectly centered, fiber may accumulate or fail to distribute evenly. The transfer path should be designed to avoid unnecessary drops that can disturb the fiber layer.
Electrical installation should be performed by qualified personnel. The customer should confirm the local power supply, grounding, motor protection, inverter requirements, sensor wiring, emergency-stop circuits, and communication with the line-control system.
Where the customer operates an existing production line, it is useful to provide layout drawings, photographs, machine nameplates, control-cabinet information, and process data before final engineering. These materials help the supplier prepare a more accurate customized design.
10. Operation, Adjustment, and Maintenance
10.1 Initial Operating Checks
Before starting production, operators should inspect the machine for loose fasteners, foreign objects, damaged guards, abnormal belt tension, and correct sensor positioning. The vibrating system should be tested without material to confirm normal movement and to identify unusual noise or vibration.
The spike and oblique lattice should run smoothly, and the evener roller and stripper should rotate without interference. The photoelectric sensor should respond correctly when the fiber level changes. Emergency-stop buttons and protective devices should be checked according to the site’s safety procedure.
10.2 Fiber-Specific Adjustment
Different fibers require different operating conditions. Polyester, viscose, nylon, polypropylene, and glass fiber can vary in length, denier, resilience, surface friction, static behavior, and tendency to form clumps.
Operators may need to adjust feeding speed, vibration intensity, evener-roller settings, storage level, and carding speed. Adjustments should be made gradually while observing the delivered batt, card load, machine current, and product uniformity.
10.3 Monitoring Hanging Fiber
The supplied operating guidance specifically notes that hanging fiber may appear around the stripper, evener roller, or wool board. This can occur because of the characteristics of the processed fiber or because of unsuitable operating conditions.
Hanging fiber can reduce feeding accuracy, alter the effective working surface, and affect the evenness of the delivered layer. It should be removed promptly according to a safe shutdown and lockout procedure. Operators should never reach into moving machinery.
10.4 Cleaning
Accumulated lint and fiber should be removed from accessible surfaces, sensor areas, guards, and the surrounding floor. Cleaning frequency depends on the material, production hours, dust level, and factory environment.
Compressed air should be used carefully because it may disperse fiber dust and create a respiratory or housekeeping hazard. The customer should follow the plant’s occupational-safety procedure and use suitable extraction or vacuum equipment where appropriate.
10.5 Routine Inspection
Routine maintenance should include inspection of bearings, chains, belts, fasteners, rollers, lattice components, vibration elements, sensors, electrical terminals, and safety devices. Wear parts should be monitored and replaced before they affect the fiber layer or create a safety risk.
A maintenance log can record operating hours, cleaning, lubrication, sensor checks, abnormal noise, replaced components, and process observations. This information helps identify developing problems and supports more reliable long-term operation.
11. Purchasing Guidance for International Buyers
Customers evaluating a vibrating feeder should provide detailed technical information before requesting a final quotation. The most important data includes fiber type, fiber length, denier, moisture, blend ratio, target capacity, working width, target basis weight, upstream opener model, downstream card model, factory voltage, and available installation space.
The customer should also clarify whether the machine will be used for one product or multiple product types. A line producing several fibers may require additional adjustment range, cleaning provisions, or special wear considerations.
Capacity should be evaluated carefully. The listed reference of approximately 0.1–5 t/h is not a universal output promise. Actual throughput depends on fiber density, feeding behavior, width, batt weight, line speed, and the operating settings of connected equipment. A technical offer should state the assumptions used for the capacity calculation.
The customer should request drawings showing the machine’s length, width, height, inlet and outlet positions, working height, service access, and electrical cabinet location. These details are essential for factory layout and installation planning.
Customers should also confirm what is included in the supply. Possible items include the feeder body, vibrating cabin, drive system, motor, inverter, photoelectric sensors, electrical cabinet, control panel, spare parts, manuals, foundation drawings, installation guidance, commissioning support, and operator training.
Warranty terms, lead time, spare-parts availability, remote support, and response procedures should be documented in the commercial contract. The supplied information lists a one-year warranty and a lead time of approximately two to three months, but the final terms should be confirmed for each project.
12. Why Work with an Experienced Nonwoven Machinery Manufacturer?
A feeder is a relatively compact machine, but its performance affects the entire production line. Working with a supplier experienced in nonwoven machinery can provide advantages in process matching, customization, commissioning, and after-sales support.
Changshu Hongyi Nonwoven Machinery Co., Ltd. offers equipment for opening, blending, feeding, carding, web forming, needle punching, thermal bonding, airlay processing, winding, cutting, and auxiliary functions. Its experience across these categories allows customers to discuss the feeder in relation to the entire manufacturing process.
The company’s reported international customer base demonstrates experience in export-oriented supply. This can be useful for customers requiring factory documentation, shipping coordination, electrical adaptation, remote communication, and installation support.
The manufacturer’s focus on automatic control, energy-conscious operation, reliable construction, precision engineering, and customization is consistent with the requirements of modern nonwoven production. Customers can request a configuration based on their actual production materials rather than selecting a one-size-fits-all machine.
For a new line, the supplier can help coordinate the feeder with the opener and card. For an existing factory, the supplier can review the available space and propose a machine that fits the current process. In either case, the quality of the technical information exchanged before manufacture has a major influence on the final result.
13. Recommended Project Workflow
13.1 Technical Data Collection
The project should begin with collection of raw-material, product, capacity, layout, and electrical data. Samples of the actual fiber are useful where the material is recycled, blended, unusually fine, highly static, or difficult to convey.
13.2 Preliminary Configuration
The supplier can then recommend working width, feeding arrangement, storage volume, control method, motor and inverter configuration, and interface dimensions. The preliminary design should identify any assumptions that require confirmation.
13.3 Drawing and Specification Approval
Before manufacturing, the customer should approve the technical specification, general arrangement drawing, electrical requirements, color, packing method, spare-parts list, and delivery schedule. Written approval reduces misunderstandings during production.
13.4 Factory Inspection
Factory inspection may include mechanical operation, sensor response, vibration behavior, safety functions, electrical testing, dimensions, and visual condition. Customers can use outgoing inspection videos or an agreed factory acceptance procedure where appropriate.
13.5 Installation and Commissioning
After delivery, the feeder should be installed on a suitable foundation and connected according to the approved drawings. Commissioning should begin with an empty-machine test, followed by low-rate fiber feeding and gradual adjustment to the target process speed.
13.6 Production Optimization
Final optimization should consider the complete line. The feeder should not be adjusted in isolation if changes to the opener, card, crosslapper, or downstream machine are also required. Production records can be used to establish repeatable settings for each major product type.
14. Q&A
Q1: What is the main purpose of the HYGM Vibrating Feeder?
Its main purpose is to temporarily store opened fiber, blend and level the material, and deliver a more even quantity across the machine width to the next carding process.
Q2: Which fibers can be processed?
The listed compatible materials include polyester, viscose, nylon, polypropylene, and glass fiber. Final suitability should be confirmed according to fiber denier, length, moisture, blend ratio, and other material characteristics.
Q3: Is the machine automatic?
Yes. The equipment is described as automatic and uses photoelectric storage control to coordinate the start and stop operation of the spike and oblique lattice according to the fiber level.
Q4: How does the photoelectric control work?
The photoelectric system monitors the fiber condition in the storage area. When the material reaches a preset level or changes from the required condition, the system controls the feeding components to help maintain a balanced supply.
Q5: What is the function of the evener roller?
The evener roller removes excess fiber from the incoming layer. This helps limit overfeeding and supports a more stable material condition before the fiber enters the vibrating cabin.
Q6: Why is a vibrating cabin used?
The vibrating cabin helps distribute and transfer the fiber in a controlled manner. Vibration can encourage more even settling and movement of the fiber toward the carding process.
Q7: What working widths are available?
The supplied information lists several options, including approximately 1.4 m, 1.7 m, 1.8 m, 2 m, 2.2 m, and 2.8 m. Other widths and dimensions may be customized after reviewing the customer’s line requirements.
Q8: What production capacity can the feeder achieve?
A reference capacity of approximately 0.1–5 t/h is listed. Actual capacity depends on fiber properties, working width, basis weight, line speed, feeding conditions, and the connected opener and card. A project-specific capacity should be confirmed technically.
Q9: Can the feeder be integrated into an existing line?
Yes, subject to a review of the existing line’s working width, inlet and outlet height, machine centerline, capacity, control system, electrical supply, and available installation space.
Q10: What should operators do if hanging fiber appears?
Hanging fiber around the stripper, evener roller, or wool board should be removed promptly under a safe shutdown and lockout procedure. The cause should also be investigated, including fiber characteristics, adjustment settings, surface condition, and cleaning frequency.
Q11: What electrical supply is available?
The listed information includes AC 220 V or AC 380 V. The correct voltage, frequency, motor arrangement, inverter, grounding, and control-circuit requirements should be confirmed before manufacture.
Q12: Is customization available?
Yes. The listed options include customized dimensions, color, working width, and electrical configuration. Additional customization should be evaluated according to the line layout and material requirements.
Q13: What certifications are listed?
The product information lists CE and ISO9001-related certification details. Customers should request the applicable documentation for the exact configuration and destination market.
Q14: What after-sales support is available?
The supplied information lists a one-year warranty and video outgoing inspection. Customers should confirm the complete after-sales scope, including installation guidance, commissioning, spare parts, remote support, response time, and training.
Q15: Can the manufacturer supply more than a vibrating feeder?
Yes. The company supplies individual nonwoven machines and complete production lines, including needle-punched geotextile lines, nonwoven carpet lines, airlay waste-felt lines, automotive interior-material lines, cleaning-cloth lines, wool and jute felt lines, carding machines, needle-punching machines, airlay machines, ironing machines, and thermal bonding oven systems.
15. Conclusion
The HYGM Vibrating Feeder is designed to improve the transition between fiber opening and carding by combining intermediate storage, further blending, automatic photoelectric control, mechanical leveling, stripping, and vibrating delivery. Its purpose is to provide a more stable and even fiber supply across the working width of the next process.
Its competitive strengths include compatibility with several common nonwoven fibers, multiple working-width options, automatic storage control, adjustable feeding behavior, customizable dimensions, and integration with complete nonwoven production lines. These features make it suitable for manufacturers seeking more consistent fiber preparation and reduced reliance on manual feeding adjustments.
The machine’s value also depends on the engineering and manufacturing support behind it. Changshu Hongyi Nonwoven Machinery Co., Ltd. combines more than 20 years of nonwoven machinery experience with a product range covering both individual machines and complete production lines. Its reported international supply experience, customization capability, certification information, outgoing inspection, and after-sales warranty provide a foundation for industrial project cooperation.
For the best result, customers should select the feeder according to the actual fiber, target capacity, working width, carding equipment, factory layout, and control system. When correctly specified, installed, and maintained, the HYGM Vibrating Feeder can serve as an important process-control component for reliable and efficient nonwoven fabric production.
References
1. Changshu Hongyi Nonwoven Machinery Co., Ltd., HYGM Vibrating Feeder product specifications and operating information.
2. Changshu Hongyi Nonwoven Machinery Co., Ltd., Nonwoven machinery product range and company information.
3. ISO 9001, Quality Management Systems—Requirements.
4. General principles of fiber opening, blending, feeding, carding, and web formation in nonwoven manufacturing.
5. General industrial practices for machinery safety, electrical installation, maintenance, and operator training.